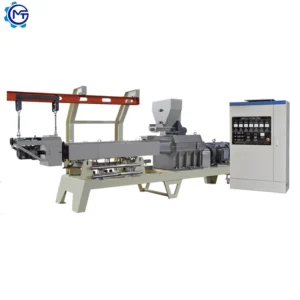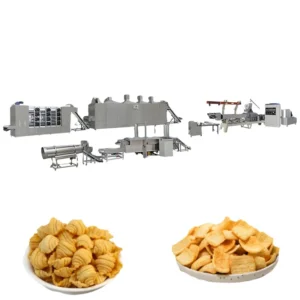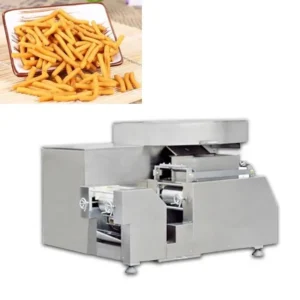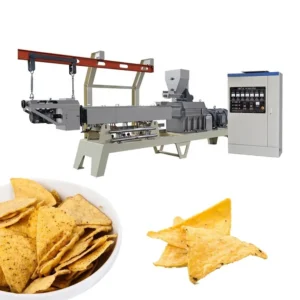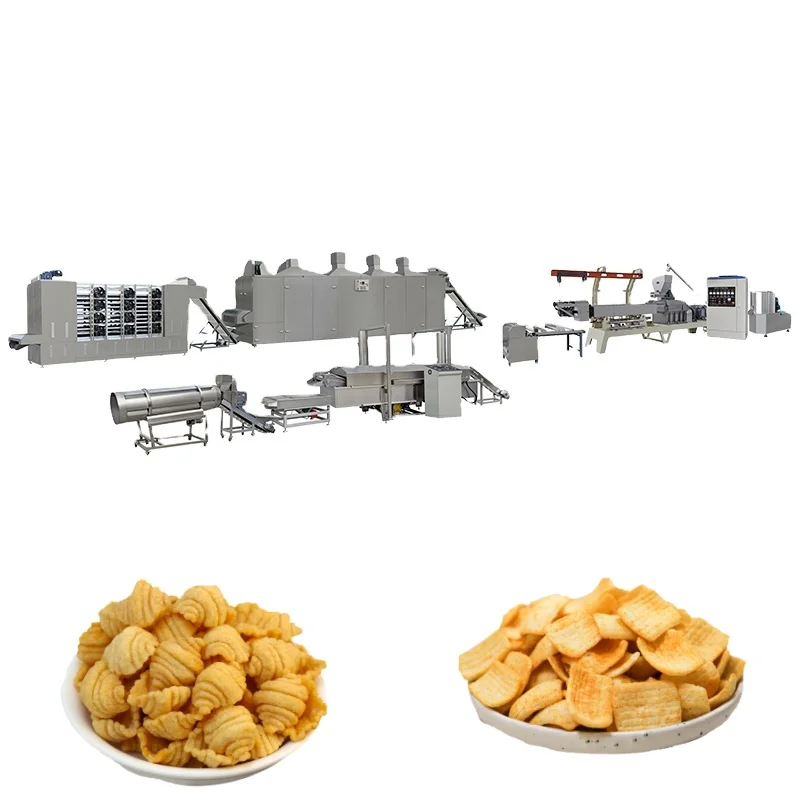
Integrated station throughput — Every mixer, extruder, cutter, fryer and flavouring drum in this fried snack food production line is sized against the others so material flow never stalls at a single bottleneck.
Technical Specifications
| Parameter | Value |
|---|---|
| Model | MT-65 / MT-70 / MT-85 / MT-75 / MT-95 |
| Product Type | Fried Snack Food Production Line (Extruded & Fried Chips / Bugles) |
| Screw Type | Twin-screw, co-rotating sectional modules |
| Main Motor (MT-65) | 100 kW |
| Main Motor (MT-70) | 130 kW |
| Main Motor (MT-85) | 180 kW |
| Main Motor (MT-75) | 185 kW |
| Main Motor (MT-95) | 280 kW |
| Output Capacity (MT-65) | 120–150 kg/h (basis not stated in source — confirm raw material, moisture and product shape) |
| Output Capacity (MT-70) | 200–250 kg/h (basis not stated in source — confirm raw material, moisture and product shape) |
| Output Capacity (MT-85) | 300–500 kg/h (basis not stated in source — confirm raw material, moisture and product shape) |
| Output Capacity (MT-75) | 400–500 kg/h (basis not stated in source — confirm raw material, moisture and product shape) |
| Output Capacity (MT-95) | 800–1000 kg/h (basis not stated in source — confirm raw material, moisture and product shape) |
| Cutter Power | 1.47 kW |
| Mixer Power Options | 4 kW / 7.5 kW / 15 kW |
| Fryer Belt Width | 600 mm stainless steel mesh belt |
| Fryer Energy Options | Electricity / Fuel / Gas |
| Drying Method (post-fry) | Gas / Electric / Diesel heating |
| Voltage & Frequency | Configurable (e.g., 3-phase 380 V 50 Hz, 415 V 60 Hz, 220 V 60 Hz) |
| Die & Roller Changeover | Interchangeable dies for sticks, square rib chips, diamond chips, wavy chips, pillow shapes, bugles, shells, tubes |
| Contact Material | Food-grade stainless steel on all product-contact surfaces |
| Assembly State | Complete line: mixing → extrusion → cutting → frying → flavouring |
| Certification | CE (since 2014), ISO certified |
| Warranty | 1-year complete warranty with lifetime maintenance service |
Application Suitability
| Application | Material or Output |
|---|---|
| Fried corn chip and bugle production | Corn powder, corn starch, wheat flour blends |
| Extruded salad stick and pillow snack lines | Wheat flour, potato starch, rice flour formulations |
| 2D/3D pellet-style fried snacks | Potato starch, corn starch, rice flour mixes for shells, screws, tubes |
| Wavy and diamond chip formats | Corn and wheat flour with adjustable moisture for sheet-forming dies |
| Snack manufacturers adding frying capability | Existing extruded snack producers integrating fryer and flavouring stations |
What "Nominal Capacity" Leaves Out About a Frying Chips Making Machine
A line is only as fast as its slowest station, and fryer belt speed often decides the real output.
I once helped a buyer in Southeast Asia commission a fried salad-stick line where the extruder was rated well above what the downstream fryer could actually handle. Material piled up at the cutter discharge, the fryer oil temperature dropped each time a surge hit, and the client spent two weeks re-tuning belt speeds and oil circulation before product colour and moisture came back within spec. When sourcing a frying chips making machine, the headline kg/h figure on the extruder nameplate means very little unless the fryer residence time, belt width and oil recovery rate have been calculated against that same throughput [NEED_CITE: line throughput matching methodology for extruded snack plants].
How the Fryer Belt Governs the Whole Line
The 600 mm stainless steel mesh belt inside the fryer is the physical constraint that every upstream station must respect. Extruder output, cutter cycle rate and conveyor transfer speed all need to feed product onto that belt at a rate the oil can absorb without temperature collapse. Automatic temperature regulation and adjustable belt speed on this frying chips making machine allow operators to fine-tune residence time for different dough densities, but the belt width itself sets the upper ceiling for uniform single-layer loading.
Die Changeover and Shape Flexibility on One Platform
Interchangeable dies and forming rollers let a single twin-screw extruder produce bugles, sticks, wavy chips, shells and tube formats without swapping the main barrel assembly. Each shape demands a different screw module arrangement and moisture target; corn-based bugles need higher shear and lower moisture than wheat-based pillow chips. The sectional co-rotating screw design means modules can be rearranged to match the gelatinisation profile each formulation requires [NEED_CITE: twin-screw extrusion screw configuration principles for starch-based snacks].
Reading the Power and Capacity Tiers
Motor ratings scale from 100 kW on the MT-65 to 280 kW on the MT-95, reflecting the increasing barrel volume and torque needed to push higher mass flow rates through the die plate. Mixer power options of 4 kW, 7.5 kW and 15 kW correspond to batch sizes that keep the extruder hopper continuously supplied without material bridging. Output figures listed for each model should be validated against the buyer’s specific raw material blend, moisture content and target chip geometry, because a dense wheat-flour dough will process at a different mass rate than a light corn-starch formulation. Fryer energy options — electricity, fuel or gas — must be chosen to match the thermal load implied by that same throughput, not merely the lowest local utility cost.
The Hidden Cost of Mismatched Station Sizing
When a fryer is undersized relative to extruder output, operators compensate by slowing the extruder, which drops barrel fill ratio and alters starch gelatinisation. The resulting chips absorb oil unevenly, develop soft spots and fail shelf-life tests weeks later. Conversely, an oversized fryer running half-empty wastes thermal energy and accelerates oil degradation, raising consumable costs across every shift [NEED_CITE: oil degradation rate in continuous industrial fryers under partial load]. These downstream quality problems trace back to a single procurement decision: buying stations from different vendors without a unified throughput calculation.
Why Sourcing the Full Line from One Manufacturer Matters Here
Every station in this fried snack food production line is specified under one engineering responsibility, so the mixer batch cycle, extruder screw speed, cutter timing, fryer belt load and flavouring drum rotation are calculated as a single system. The in-house testing workshop runs trial production on the buyer’s actual raw material before shipment, generating a report that confirms real output, chip density and shape fidelity. Screw and die configuration records are documented per order, not copied from a generic build. Electrical schematics carry the confirmed voltage and frequency of the destination facility, avoiding rewiring delays during commissioning [NEED_CITE: CE machinery directive documentation requirements for food processing equipment].
Documentation & Verification
- Line layout and capacity calculation showing throughput match from mixer through flavouring drum
- Screw and die configuration record specifying module arrangement for buyer’s target chip shape
- Trial run report on buyer’s actual corn or wheat formulation conducted before shipment
- Electrical schematic with destination voltage and frequency confirmed prior to production
- Factory test record documenting running parameters across every station
- Wear parts list covering screws, dies, cutter blades and fryer belt sections
Installation, Commissioning & Support
- Foundation plan accounts for the 22–30 m line footprint depending on model tier
- Dedicated electrical circuit sized to the selected main motor rating up to 280 kW
- Line arrives in modular sections; on-site assembly aligns extruder discharge to cutter infeed
- First-run commissioning includes fryer oil temperature profiling against actual chip moisture
- Operator training covers die changeover sequence and fryer belt speed adjustment
- Free wearing parts shipped with initial order; additional screw and die sets available for multi-year coverage
- Scheduled maintenance checklist covers fryer oil filtration and belt tension inspection
What to Prepare Before Requesting a Quotation
Share your primary raw material — corn flour, wheat flour, potato starch or a blend — along with the target chip shape and approximate daily output in kilograms. Confirm the voltage and frequency available at your facility, the preferred fryer energy source and the language required on the control panel. If you already operate upstream or downstream equipment, provide model details so the new frying chips making machine line can be configured to integrate with existing conveyors or packing stations.
Frequently Asked Questions
Q: How is the stated output capacity verified before delivery?
A: Each line undergoes a trial run in the manufacturer’s testing workshop using the buyer’s actual raw material formulation. The resulting report documents real mass throughput, chip density and shape accuracy under production conditions, rather than relying on a generic nameplate figure. Buyers receive this report alongside the screw configuration record.
Q: Can the electrical system be customised for different export markets?
A: Voltage and frequency are confirmed during the specification stage and can be set to common industrial standards such as 380 V 50 Hz, 415 V 60 Hz or 220 V 60 Hz. Control panel language is also specified before production begins so operators can read instructions in their local language from day one.
Q: Is throughput balanced across every station in the frying chips making machine line?
A: Yes. The mixer batch cycle, extruder output, cutter speed, fryer belt load and flavouring drum rotation are calculated together under a single engineering scope. This prevents any individual station from becoming a bottleneck and avoids the integration gaps that arise when equipment is sourced from separate vendors.
Q: How does the die changeover process work when switching chip shapes?
A: Dies and forming rollers are interchangeable on the twin-screw extruder platform. Operators disconnect the die plate, swap to the target shape die and adjust the screw module arrangement if the new formulation requires a different shear profile. The changeover is documented in the configuration record supplied with each order.
Q: What spare wearing parts are included, and how are replacements sourced?
A: The initial shipment includes a set of free wearing parts covering common replacement items. Additional screw modules, dies, cutter blades and fryer belt sections can be ordered for two to three years of coverage. Replacement parts are manufactured to the same specification as the originals and ship against the documented configuration record.