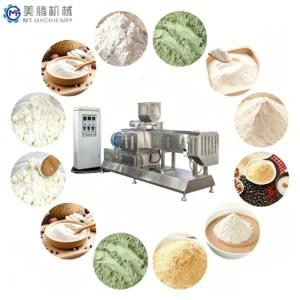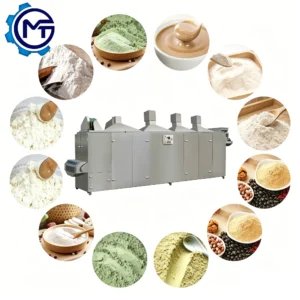
Twin-Screw Extrusion Expertise — screw configuration and barrel profile specified to the buyer’s raw material, not copied from a generic nutritional powder build.
Technical Specifications
| Parameter | Value |
|---|---|
| Model | MT65 / MT70 / MT85 |
| Product Type | Nutritional Powder Processing Line |
| Screw Type | Twin-screw |
| Installed Power | MT65 — 85 kW; MT70 — 120 kW; MT85 — 195 kW |
| Actual Power Consumption | MT65 — 65 kW; MT70 — 90 kW; MT85 — 165 kW |
| Output Capacity | MT65 — 150–200 kg/h (basis to be confirmed); MT70 — 200–300 kg/h (basis to be confirmed); MT85 — 600–800 kg/h (basis to be confirmed) |
| Extruder Main Motor Power | 30 kW |
| Extruder Dimension | 2800 × 830 × 1875 mm |
| High-Temperature Roaster Effective Belt Length | 3.5 m |
| High-Temperature Roaster Far Infrared Heater | 3.9 kW × 24 |
| Powder Mixer Tank Volume | 150 kg |
| Powder Mixer Rotary Speed | 385 rpm |
| Powder Mixer Mixing Time | 10 min per batch |
| Construction Material | Stainless steel food-contact surfaces |
| Control System | Configurable PLC or MCC (basis to be confirmed) |
| Line Stations | Mixing → Air Conveying → Twin-Screw Extrusion → Roasting → Crushing → Blending |
| Certification | CE (since 2014), ISO |
Application Suitability
| Application | Material or Output |
|---|---|
| Infant nutritional powder | Rice, corn, and soy-based grain blends processed into baby food powder |
| Fortified breakfast powder | Sesame paste, soybean powder, and mixed cereal formulations |
| Modified starch | Adjusted screw and barrel configuration for textile, papermaking, and building material grades |
| Grain-based nutritional blends | Rice grits, corn flour, and bean meal as primary raw material inputs |
What a Nominal Capacity Figure Leaves Out on a Nutritional Powder Processing Line
The rated output means nothing until it is validated on your exact formulation.
When a nutritional powder processing line is quoted at a single throughput number, that figure usually comes from a test on standard corn grits or rice flour at controlled moisture. Real formulations for infant food or fortified powder include whey protein isolates, vitamin premixes, and micronutrient carriers that change how starch gelatinises inside the barrel. The expansion rate drops, the bulk density shifts, and the roaster has to work longer to drive off residual moisture — all of which pull actual output well below the nameplate [NEED_CITE: starch gelatinisation behaviour under protein-enriched formulations].
I watched a Southeast Asian buyer receive a line that ran perfectly on plain rice flour in the factory trial, then spent weeks on-site re-tuning every parameter once whey protein and trace minerals entered the mix. Since that job, I do not schedule production until the customer’s actual formulation — including every additive — has been tested in our workshop.
How Each Station Connects in the Full Equipment Range
A nutritional powder processing line at this site is presented as a catalogue of individual stations rather than a bundled black box. The powder mixer blends raw material in 150 kg batches at 385 rpm with a ten-minute cycle, the air conveyor lifts the blend into the extruder hopper, and the twin-screw unit handles gelatinisation and initial expansion. Downstream, the high-temperature roaster with 3.5 m effective belt length and twenty-four far-infrared heaters dries the extrudate before it enters the crusher and the final blending station. Each station carries its own motor rating and footprint so the buyer can cross-check throughput continuity before the line is assembled.
Barrel Temperature Zones and Screw Element Arrangement
The twin-screw extruder in this nutritional powder processing line uses segmented barrel zones with independent heating, allowing operators to set a rising temperature profile that matches starch gelatinisation onset to the specific grain blend. Screw elements can be reconfigured — conveying sections lengthened for longer residence time, or kneading blocks added for higher shear when processing tougher legume flours. The die plate determines strand diameter going into the roaster, and swapping dies is the first adjustment when moving from a fine infant powder to a coarser fortified cereal blend [NEED_CITE: twin-screw element arrangement for varying raw material rheology].
Reading the Power Draw Against Real Operating Conditions
The gap between installed power and actual consumption — for example 120 kW installed versus 90 kW actual on the MT70 — reflects motor sizing headroom for peak torque during start-up and heavy-load moments. On a nutritional powder formulation with high fat or protein content, extruder amperage can climb noticeably during the first minutes of a run as the barrel fills. Roaster gas consumption at 6.8 m³ per cycle shifts upward when ambient humidity is high, because the belt must carry moisture-laden extrudate longer to reach target dryness. Buyers should use actual consumption figures, not installed power, when sizing workshop electrical panels and gas supply lines.
What Happens When Line Stations Are Not Throughput-Matched
An extruder that pushes out more material than the roaster belt can dry creates a bottleneck where partially dried strands pile up, developing surface case-hardening that traps internal moisture. On the other side, an undersized powder mixer starves the extruder hopper, forcing the screws to run partially empty — a condition that accelerates wear on the screw flights and produces inconsistent expansion. These mismatches surface only after the line is installed and running on the buyer’s actual recipe, which is why reviewing every station’s rated output before ordering matters [NEED_CITE: extrusion line bottleneck diagnostics].
Why Sourcing the Complete Range Here Reduces Integration Risk
Every station from the powder mixer through the air conveyor, twin-screw extruder, high-temperature roaster, crusher, and final blender is documented individually, so throughput can be matched on paper before metal is cut. Screw configuration and die selection are specified against the buyer’s raw material rather than carried over from a previous order. An in-house testing workshop runs trial batches on customer-supplied formulation before shipment, catching gelatinisation or density issues before the line reaches the factory floor. CE and ISO certification covers the full assembly, and electrical schematics include voltage and frequency confirmation for the destination market.
Documentation & Verification
- Machine specification sheet listing each station’s motor rating, dimensions, and power draw
- Screw and die configuration record matched to the buyer’s grain and additive blend
- Trial run report produced on customer-supplied nutritional powder formulation before dispatch
- Electrical schematic confirming voltage, frequency, and control language for destination market
- CE declaration of conformity and ISO certificate covering the full line assembly
- Wear parts list identifying screw elements, dies, and roaster belt replacements
Installation, Commissioning & Support
- Foundation plan accounts for MT85 line footprint at 24,000 × 3,500 × 4,300 mm and total actual load of 165 kW
- Dedicated electrical circuits sized for extruder 30 kW main motor and roaster 93.6 kW heater bank
- Equipment ships in modular station units for sequential on-site assembly and belt alignment
- Commissioning includes first-batch parameter tuning on the buyer’s actual raw material formulation
- Operator training covers PLC or MCC interface navigation, screw speed adjustment, and roaster belt tracking
- Spare screw segments, die plates, and roaster belts stocked for first scheduled replacement cycle
What We Need Before Quoting Your Line
Send the full ingredient list with percentages, including any protein concentrates, vitamin premixes, or fat sources, along with your target bulk density and particle size for the finished powder. Include workshop voltage, frequency, and the control language your operators will use. If you already run upstream milling or downstream packing equipment, share those interface points so we can size the air conveyor and final blender accordingly.
Frequently Asked Questions
Q: What stations are included in the nutritional powder processing line?
A: The line covers a powder mixer, air conveyor, twin-screw extruder, high-temperature roaster, crusher, and a final nutritional powder blending station. Each unit is specified individually with its own motor rating and dimensions so throughput can be matched across every station before the layout is finalised.
Q: How do I choose between MT65, MT70, and MT85 for my capacity target?
A: Selection depends on your raw material formulation and the throughput that formulation can sustain — not just the nameplate figure. We run your actual blend in the testing workshop first, then recommend the model whose screw volume and motor headroom match your confirmed output.
Q: Can the twin-screw extruder also produce modified starch?
A: Yes. By adjusting screw element arrangement and barrel temperature zones, the same extruder platform can shift from nutritional powder to modified starch production for textile, papermaking, or building material applications, subject to die and downstream equipment compatibility.
Q: Are spare wear parts available for the first replacement cycle?
A: Screw segments, die plates, and roaster belt sections are listed in the wear parts documentation supplied with the line. We confirm stock availability before shipment so that first replacements are on hand when scheduled maintenance arrives.
Q: What electrical and control options are offered for each unit?
A: Voltage and frequency are confirmed to the buyer’s destination market before production. Control systems can be configured as PLC or MCC based on the buyer’s automation preference, with operator interface language set before the electrical cabinets leave the factory.