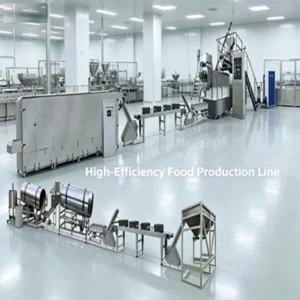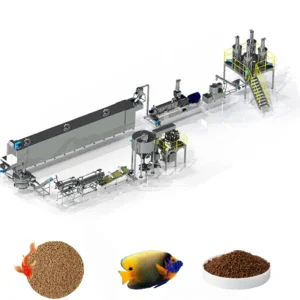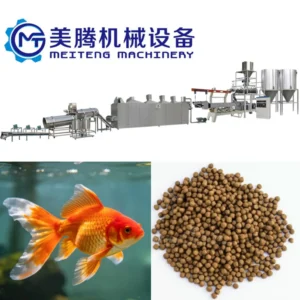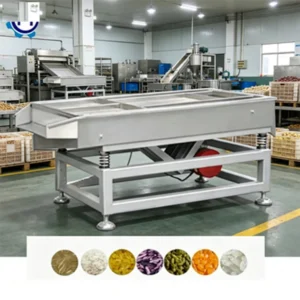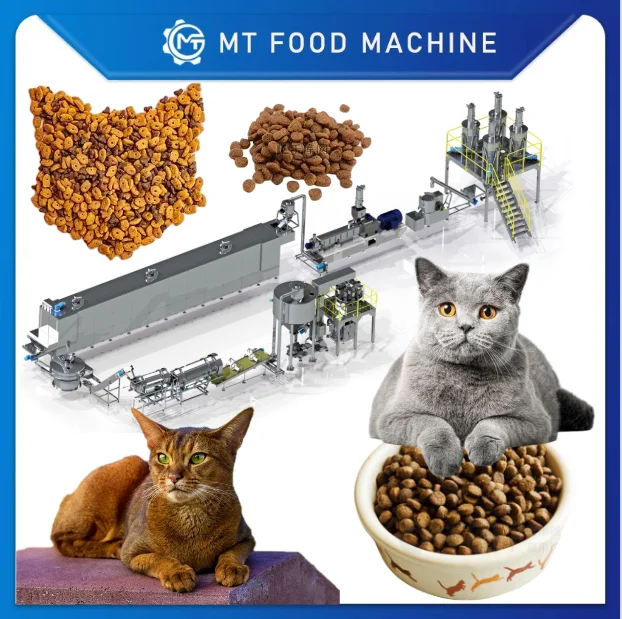
Matched Throughput Stations — Every mixer, extruder, dryer and packer in this catalogue is sized to the same duty cycle, so no single station chokes the line while the rest sit idle.
Technical Specifications
| Parameter | Value |
|---|---|
| Product Type | Pet Food Processing Line |
| Output Capacity | 250-300 kg/h (basis not stated in source — confirm raw material formulation and moisture content) |
| Control System | PLC Controlled |
| Automation Level | Full Automation |
| Recipe Adaptability | Dry kibble, semi-moist, treats |
| Target Species | Cats and multi-species pets |
| Line Scope | Mixing through extrusion to packing |
Application Suitability
| Application | Material or Output |
|---|---|
| Dry kibble for cats | Poultry meal, corn, rice, fish meal blends |
| Semi-moist pet food | High-meat slurry with humectants |
| Extruded pet treats | Starch and protein concentrate dough |
| Multi-species kibble | Variable protein-to-carbohydrate ratios |
Why the Dryer Spec Decides Your Real Output
A quoted extruder capacity means nothing when the dryer downstream cannot keep up.
I have watched lines where the extruder pushed product faster than the drying belt could handle, forcing operators to throttle feed rates and run well below nameplate throughput. On one cat food line, the multi-layer dryer was sized for a lighter kibble geometry; the denser semi-moist format required longer residence time, and the whole line slowed to match. Before you compare numbers on a pet food processing line manufacturer quotation, check that every station from the mixer to the cooler carries the same rated duty. [NEED_CITE: typical moisture reduction targets for dry versus semi-moist kibble]
How Each Station Fits the Production Flow
A cat food line is only as fast as its slowest hand-off. The batching and mixing stage must deliver uniform moisture and particle size before the product ever reaches the extruder barrel. From there, the conveying system must move kibble without breaking fragile shapes, and the dryer must remove moisture evenly so coating adhesion stays consistent. This equipment catalogue maps every station to a position in that sequence, letting you see the full pet food processing line manufacturer scope before specifying individual units or a complete build.
Matching Capacity Across Consecutive Stations
Throughput mismatches create hidden costs that only appear after commissioning. If the flavouring drum turns slower than the extruder feeds, product piles up in the conveyor transfer chute, cooling unevenly and absorbing moisture from the air. If the cooler runs ahead of the packing scale, bags are filled at inconsistent weights. Our approach is to calculate the residence time and belt speed at each station against the same raw material formulation, so the entire line holds a steady cadence rather than surging and stalling. [NEED_CITE: throughput balancing methods in continuous food extrusion lines]
Reading the Specs That Matter
The PLC control system matters because recipe changes between kibble, semi-moist and treats require different barrel temperature profiles, screw speeds and moisture injection rates — storing those parameters digitally eliminates manual re-entry errors during changeovers. Full automation across the line reduces the number of operators needed at each station, but it also demands that the electrical specification matches your facility voltage and frequency before the cabinets are wired. The stated capacity range of 250-300 kg/h must be verified against your actual recipe, because protein-heavy cat food formulations behave differently in the extruder barrel than starch-dominant dog kibble blends, affecting expansion ratio and required dryer residence time.
What Happens When Stations Are Not Balanced
Purchasing an extruder from one vendor and a dryer from another often means the interface between them was never engineered. Conveyor transfer heights mismatch, causing product damage. Control systems cannot communicate, so an emergency stop on the extruder does not halt the downstream belt. Operators spend the first weeks after installation manually adjusting feed rates at every hand-off point, which is exactly the kind of problem that erodes confidence in the line before full production ever starts. [NEED_CITE: common integration failures in multi-vendor food processing lines]
Why Source the Full Range Here
Every supporting station — mixing, conveying, drying, flavouring, coating, cooling, packing — is available from one equipment range, so throughput calculations are done across the whole line rather than patched together from separate vendor datasheets. Screw configuration and die design are specified against your raw material before the extruder ships, not guessed from a generic build. An in-house testing workshop allows trial runs on your actual recipe so kibble density and expansion are confirmed before crates are nailed shut. Pre-sales engineering covers layout, utility planning and phased installation schedules. Ongoing support includes operator training, wear parts supply and maintenance guidance long after commissioning is complete.
Documentation & Verification
- Machine specification sheet listing capacity, utility and footprint for every station
- Line layout drawing showing throughput matching between consecutive units
- Screw and die configuration record matched to your kibble geometry target
- Electrical schematic with voltage and control language confirmed before wiring
- Trial run report produced on your raw material formulation before dispatch
Installation, Commissioning & Support
- Foundation load calculations provided for extruder and dryer footprint
- Dedicated electrical circuit sizing matched to PLC panel total draw
- Equipment shipped in modular sections for standard container loading
- First-run parameter tuning against your recipe during on-site commissioning
- Operator training covering recipe changeover on the PLC interface
- Wear parts list specifying screw elements, die plates and dryer belt sections
What to Include in Your Inquiry
Send your raw material formulation with moisture percentages, your target daily output in kilograms, and the kibble shape and size your market expects. Include your facility voltage, frequency and preferred control language so the electrical cabinets are configured before production begins. If you have existing upstream or downstream equipment that must integrate, share those connection dimensions.
Frequently Asked Questions
Q: How do I confirm that quoted capacity holds on my actual raw material?
A: Request a trial run on your specific formulation in the supplier’s testing workshop. The extruder should process your blend at the quoted throughput while producing kibble that meets your density and expansion targets. A written trial report should accompany the results, documenting screw speed, barrel temperature profile and die configuration used.
Q: Can I purchase individual stations instead of a complete line?
A: Yes. Each station in the equipment range — mixer, extruder, dryer, flavouring drum, cooler, packing scale — is available separately. Provide your existing line throughput and connection dimensions so the replacement or additional unit is matched correctly to avoid bottlenecks at the integration point.
Q: What control system options exist and how do I specify the interface?
A: The line uses PLC control with a digital interface for recipe storage and process monitoring. Specify your facility voltage, electrical frequency and preferred operator language before cabinet assembly begins. Confirming these details early prevents commissioning delays caused by rewiring or software reconfiguration after delivery.
Q: How do I match extruder output with dryer and coating capacity?
A: Provide your target kibble moisture content and coating percentage so the dryer belt length and flavouring drum diameter are calculated against the same throughput figure. The supplier should show a line layout where every station carries the same rated capacity, confirmed by residence time calculations at each stage.
Q: What supporting stations are available and where does each fit?
A: The range covers mixing and batching before extrusion, conveying between stages, drying and cooling after forming, flavouring and coating drums, and packing at the end. A line layout document maps each station to its position in the production sequence with throughput values matched across the entire flow.