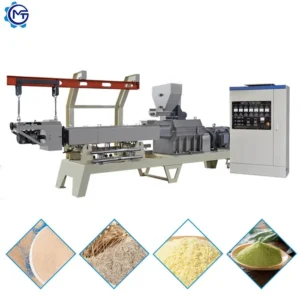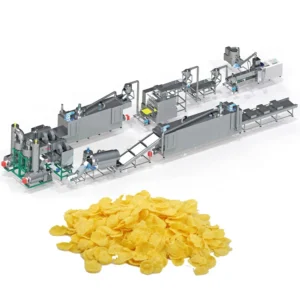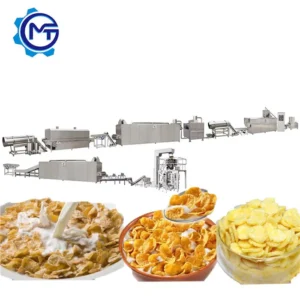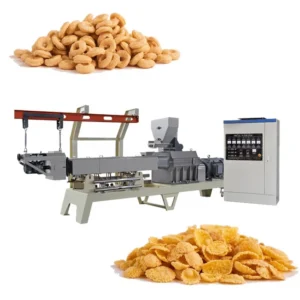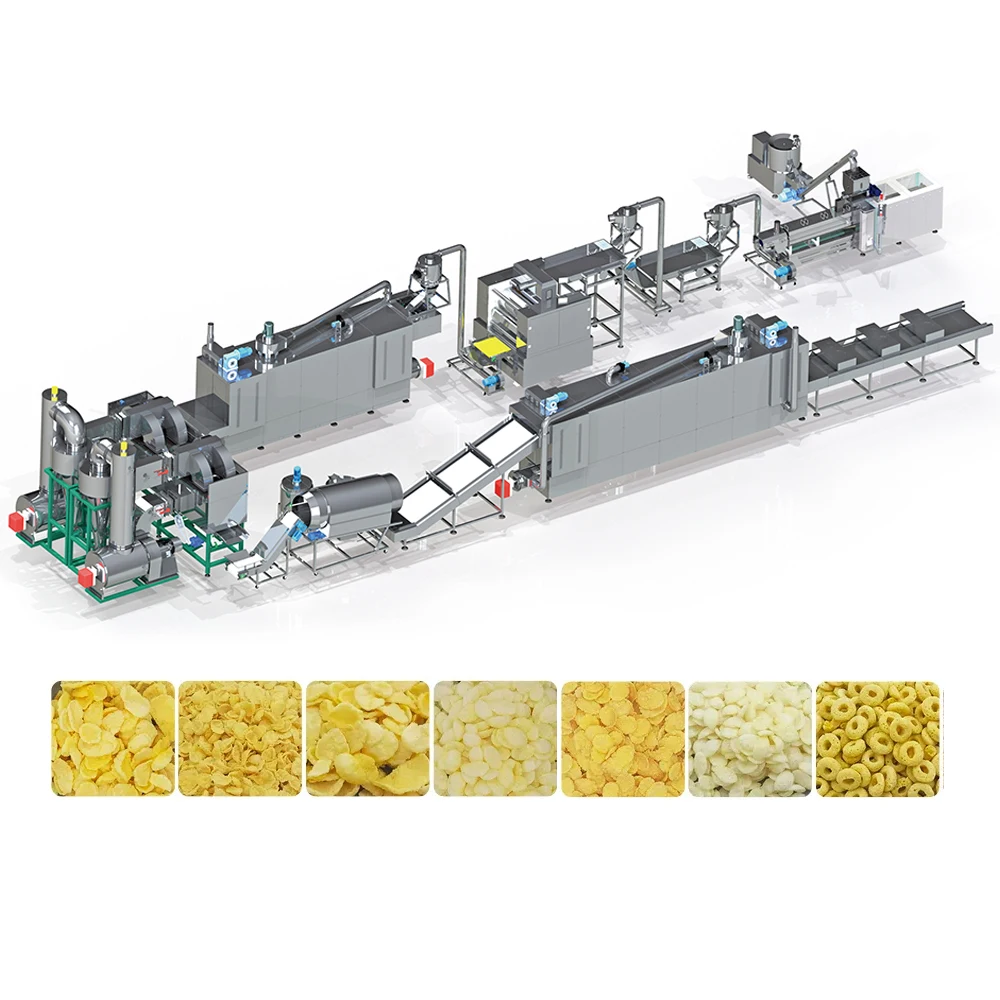
Complete Line Integration — every station from mixing to packing is sized to the same throughput, eliminating the bottleneck that happens when an extruder is paired with an undersized dryer or coater.
Technical Specifications
| Parameter | Value |
|---|---|
| Model | MT70 / MT85 / MT75 |
| Product Type | Corn Flakes Production Line / Breakfast Cereal Extrusion Line |
| Extruder Type | Twin Screw |
| Installed Power | MT70: 160 kW; MT85: 190 kW; MT75: 210 kW |
| Power Consumption | MT70: 120 kW; MT85: 140 kW; MT75: 150 kW |
| Output Capacity | MT70: 150–200 kg/hr; MT85: 300–400 kg/hr; MT75: 300–500 kg/hr (basis not stated in source — confirm raw material, moisture content and target flake thickness) |
| Overall Dimensions | MT70: 41 × 1.5 × 2.2 m; MT85: 43 × 1.5 × 3.2 m; MT75: 45 × 1.5 × 3.5 m |
| Control System | PLC control system; MCC available per customer requirement |
| Screw Material | Wear-resistant screw with special treatment |
| Lubrication | Automatic lubricating system with cooling function |
| Flaking Machinery | Hydraulic double-roller system, separate motor drive per roller, infrared sensor temperature control |
| Dryer Heating Source | Gas or Electric |
| Roasting Oven | Hot air roasting with conciliation burner, dual circulating fans, cyclone dust removal |
| Coating System | Double tumble sugar melting, elevator, coating drum, spraying nozzle |
| Final Product Shapes | Ball, tube, stick, ring, fruit loop, star, wheel, flower, heart |
| Assembly State | Complete production line |
| Customization | Factory layout designed to customer dimensions and local voltage |
| Standards | CE certified, ISO certified |
Application Suitability
| Application | Material or Output |
|---|---|
| Natural corn flakes | Corn grits or corn flour, toasted without sugar coating |
| Sugar-coated corn flakes | Corn base with sugar syrup glazing and secondary drying |
| Shaped breakfast cereals | Corn, rice, wheat, oat or barley powder formed into rings, balls, stars, fruit loops |
| Puffed cereal snacks | Grain-based formulations expanded through twin-screw extrusion |
Why the Dryer and Flaker Must Match the Extruder Before You Sign
A corn flakes production line equipment package is only as fast as its slowest station.
I have watched lines stall because the extruder pushed material faster than the flaker could press it, or because the dryer could not pull moisture down before the roasting oven received it. When each station is sourced from a different vendor, nobody takes responsibility for the gap in the middle. The breakfast cereal making machine full range you specify has to be balanced as a single system, with throughput confirmed at every hand-off point from the mixer discharge through to the packing scale [NEED_CITE: throughput balancing across sequential processing stations].
How Every Station Connects in Sequence
A natural corn flakes line follows a fixed path: mixing, extruding, flaking, drying, hot air roasting, cooling and packing. Each station must hold the same mass flow. The twin-screw extruder gelatinises the starch and forms the pellet; the hydraulic flaking machinery then presses that pellet between two rollers driven by separate motors, with infrared sensors monitoring surface temperature to keep flake thickness uniform. If the flaker cannot accept every kilogram the extruder delivers, material backs up and the entire corn flakes production line equipment set loses effective output.
Sugar Coating Adds a Second Drying Pass
When the target product is sugar-coated, the line extends past the roasting oven into a sugar spraying and coating stage, followed by a second drying pass and cooling. The double tumble system melts the sugar, an elevator feeds the coating drum, and a spraying nozzle distributes syrup across the cereal surface. This coating station must be sized to the roaster discharge rate; otherwise the corn flakes sit in the drum too long and absorb excess moisture, ruining the crispness the market expects [NEED_CITE: sugar coating residence time and moisture reabsorption in cereal processing].
Reading the Specs That Matter for Flake Quality
Twin-screw extrusion gives operators control over shear and residence time that single-screw designs cannot match, which matters when switching between corn, rice and wheat bases with different gelatinisation temperatures. The automatic lubricating system with cooling keeps barrel temperatures stable during long runs, preventing the screw clearance from drifting as bearings heat up. The hydraulic flaking station uses separate motors for each roller, so you can set different surface speeds if the formulation requires a pulling action rather than a pure crush. Infrared temperature control on the flaking rollers prevents the dough sheet from sticking or tearing when moisture content shifts between batches. The hot air roasting oven uses a conciliation burner with two separate circulating fans and a cyclone dust removal device, which keeps blistering even across the full tray width and pulls fine particulate out of the air stream before it can settle back onto the product.
What Happens When Stations Are Mismatched
An extruder quoted on nominal capacity without a corresponding dryer specification leaves you discovering the bottleneck on commissioning day. I once spent two weeks on a site where the flaking rollers could not keep up, and the operator was deliberately starving the extruder to prevent a pile-up between stations. The line never reached its intended throughput because the equipment had been assembled from separate quotes rather than designed as one system [NEED_CITE: sequential equipment mismatch and commissioning delays in food processing lines].
Why Sourcing the Full Range From One Supplier Changes the Outcome
Every station in this breakfast cereal making machine full range is specified against the same throughput target, so the extruder output, flaker acceptance rate, dryer evaporation capacity and roaster dwell time all align. Screw configuration and die design are set to the buyer’s raw material and target flake shape before the machine is built, not copied from a generic template. The in-house testing workshop runs your actual corn flour or grain blend through the extruder and flaker before shipment, so you see the flake thickness and expansion on your own material. PLC and MCC control options are confirmed for your local voltage and frequency before production starts, and the operator interface language is locked in at the same stage. CE and ISO certification covers the complete line, not just individual components.
Documentation & Verification
- Line layout and capacity calculation showing each station matched to extruder throughput
- Machine specification sheet with voltage, frequency and control language confirmed
- Screw and die configuration record specified to your grain base and target flake shape
- Trial run report on your actual raw material before shipment
- Factory test record covering full line sequential operation
- Operation and maintenance manual with wear parts list
Installation, Commissioning & Support
- Foundation planning based on the MT75 overall length of 45 m and station-by-station load
- Dedicated electrical circuits sized to the installed power draw up to 210 kW
- Assembly from shipped modules with station alignment verified on your factory floor
- First-run parameter setting for screw speed, barrel temperature and flaker roller gap
- Operator training covering PLC interface, hydraulic flaker adjustment and roaster burner tuning
- Wear parts list for screws, dies and flaker roller surfaces with recommended stock levels
What We Need to Configure Your Line
To size every station correctly, share your grain base (corn, rice, wheat, oat or barley), the flour particle size you typically mill to, and whether the target product is natural or sugar-coated. Tell us your daily production target and available shift hours so we can select the right model. We also need your factory floor dimensions and ceiling height to draft the layout, plus the local voltage and frequency so the motors and PLC are built to match.
Frequently Asked Questions
Q: How is each station in the line sized to match the extruder output?
A: Every station — flaker, dryer, roaster, coater — is calculated against the extruder’s mass flow on your specific raw material. We document the throughput at each hand-off point in the line layout so no station becomes a bottleneck, and the trial run in our workshop confirms the balance before shipment.
Q: What supporting equipment is included in the line?
A: The full range covers mixing, conveying between every station, drying, flaking, roasting, cooling and packing. Elevators and transfer chutes are part of the package, so you do not need to source conveyors or intermediate handling equipment from separate vendors.
Q: Can I start with natural corn flakes and add sugar coating later?
A: Yes. The natural line ends at cooling and packing, and the sugar coating station — double tumble melter, coating drum and second dryer — can be added as an extension. We leave the connection point in the layout so the future addition does not require repositioning the roaster or cooler.
Q: How does the flaking machinery handle different cereal bases?
A: The hydraulic flaker uses separate motors for each roller and infrared temperature control. Corn, rice and wheat doughs behave differently under pressure, so operators adjust roller gap, surface speed and temperature to match the formulation and achieve consistent flake thickness across runs.