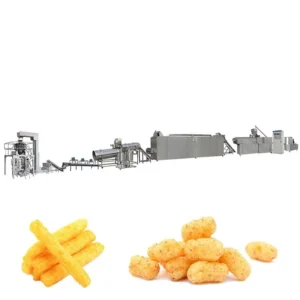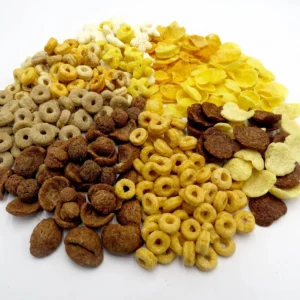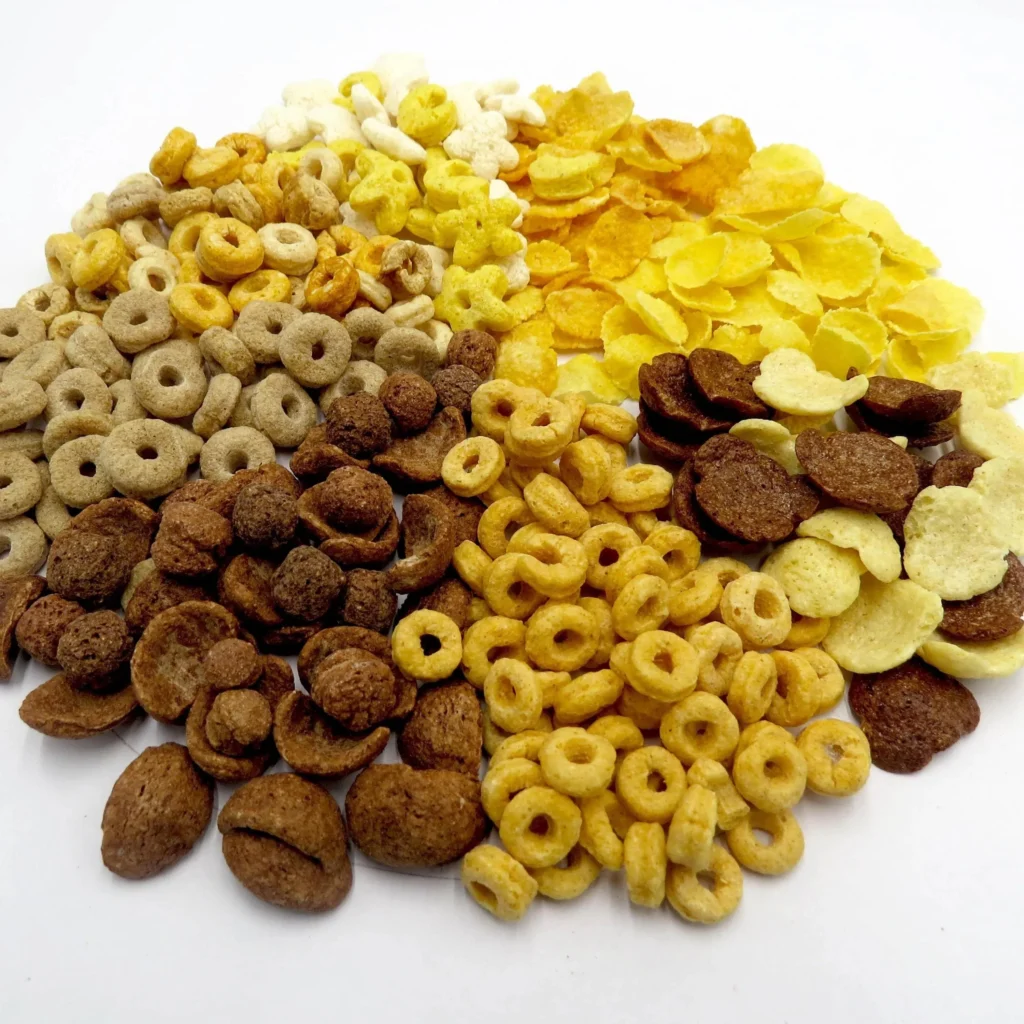
Integrated Line Throughput — Every station from mixing to packaging is capacity-matched under one supplier, preventing the bottlenecks that occur when extruders, dryers and coating drums are sourced separately.
Technical Specifications
| Parameter | Value |
|---|---|
| Product Type | Corn Flakes & Breakfast Cereals Processing Line |
| Production Mode | Fully automatic integrated line (mixing → extrusion → flaking → drying → roasting → coating → packaging) |
| Extruder Type | Twin-screw |
| Control System | PLC |
| Construction Material | Food-grade stainless steel (all food-contact parts) |
| Coating System | High-efficiency chocolate and sugar coating device |
| Drying & Roasting Method | Hot air circulation system with even heating |
| Adjustable Parameters | Flaking thickness, drying temperature, extrusion speed, coating volume |
| Line Stations | Mixing, extrusion, flaking, drying, roasting, coating, packaging |
| Output Capacity | (basis to be confirmed) |
| Voltage & Frequency | (configurable — confirm against target market) |
| Standards | CE, ISO |
Application Suitability
| Application | Material or Output |
|---|---|
| Crispy corn flakes production | Corn grits, maize flour, sugar, malt extract |
| Maize chocos production | Maize flour, cocoa powder, sugar, vitamin premix |
| Cocoa cereals production | Cocoa-blend grain formulations, chocolate coating |
| Extruded breakfast cereals | Multi-grain blends, rice flour, oat flour |
| Sweet cereals with coating | Chocolate or sugar syrup applied in dedicated coating drum |
Why Matching Dryer Capacity to the Extruder Changes Everything on a Corn Flakes Line
An extruder running at full output means nothing if the dryer cannot keep pace — the result is product pile-up, moisture inconsistency, and a coating drum that runs half-empty.
I spent most of my early career in the testing workshop before moving to line planning, and the pattern I saw repeatedly was the same: buyers focused on extruder capacity and treated every downstream station as an afterthought. On a corn flakes breakfast cereals processing line equipment range, the dryer and roaster carry the real throughput burden. If the hot air circulation system cannot remove moisture fast enough, flakes arrive at the coating station damp, sugar crystallizes unevenly, and the entire line slows to match its weakest link [NEED_CITE: thermal drying capacity calculations for cereal production lines]. I recall one project in the Middle East where a producer ordered the extruder based on a nominal figure and left the dryer undersized — the line ran at a fraction of its design output for the first month while the drying section was reworked.
How Each Station Connects Across the Full Equipment Range
On a corn flakes breakfast cereals processing line equipment range, the sequence starts at the batching and mixing station where raw materials — corn grits, sugar, malt, salt, and any vitamin premix — are blended to a uniform moisture content before entering the extruder. The twin-screw extruder then handles gelatinization under controlled barrel temperature and pressure, producing a cooked dough mass that exits through the die. From there, the product moves to the flaking station, where roller gap determines final flake thickness, a parameter that directly affects both crunch texture and drying time downstream.
Drying, Roasting and Coating — Where Consistency Is Won or Lost
The drying stage uses a hot air circulation system designed to pull moisture from the flakes evenly across the full belt width, which matters because uneven drying creates hard spots that survive roasting and show up as textural defects in the finished bowl [NEED_CITE: moisture gradient effects on flake crispness in breakfast cereal manufacturing]. Roasting follows to develop color and flavor through Maillard browning. The coating station then applies chocolate or sugar syrup at an adjustable volume, and this is where an undersized drum creates visible inconsistency — some flakes receive a heavy glaze while others pass through nearly bare. Matching the coating drum’s residence time to the upstream output rate is what separates a uniform product from one that generates customer complaints.
Reading the Specs That Actually Determine Line Behavior
The twin-screw extruder is the core of this corn flakes breakfast cereals processing line equipment range, and its screw configuration directly governs how thoroughly starch gelatinizes inside the barrel. A screw profile designed for corn grits will behave differently from one set up for a maize-cocoa blend, which is why the configuration record should be matched to the buyer’s actual formulation rather than copied from a generic build. The PLC control system ties together extrusion speed, flaking roller gap, drying temperature and coating volume into one adjustable interface — this matters because changing from plain corn flakes to a chocolate-coated variant requires coordinated parameter shifts across at least four stations, not isolated tweaks. Food-grade stainless steel across all contact surfaces ensures that sugar and cocoa residues do not corrode equipment between product changeovers, and the hot air circulation system’s evenness of heating determines whether roasting produces a consistent golden color or a mottled surface that fails visual inspection.
What Happens When the Line Is Assembled from Separate Vendors
Sourcing the extruder from one supplier and the dryer from another creates an integration gap that rarely shows up until commissioning week. The extruder may deliver product at a rate the dryer was never rated to handle, forcing the operator to throttle extrusion speed and run the line below its intended capacity [NEED_CITE: equipment integration challenges in multi-vendor food processing lines]. The flaking rollers may have a different throughput envelope than the extruder die output, causing dough accumulation or starvation cycles. When the coating drum cannot match the roaster’s discharge rate, product queues up on conveyors, cools below the temperature needed for proper sugar adhesion, and generates waste that erodes the line’s effective yield. These mismatches do not appear in individual machine specifications — they only surface when every station runs together under real production conditions.
Why Sourcing the Complete Range from One Supplier Matters Here
Every station on this line — mixing, extrusion, flaking, drying, roasting, coating and packaging — is specified together so that throughput at each stage is calculated against the others rather than assumed. The screw configuration and die design are selected based on the buyer’s raw material formulation and target flake texture, not pulled from a generic catalog. Before shipment, the testing workshop runs trial production on the buyer’s actual ingredients, generating a report that documents real output, moisture profiles and coating uniformity rather than theoretical figures. The PLC system ties all adjustable parameters — flaking thickness, extrusion speed, drying temperature, coating volume — into one control architecture, which simplifies operator training and reduces the chance of mismatched settings between stations. Voltage, frequency and control language are confirmed against the target market’s electrical standards before production begins, preventing commissioning delays that arise when a 50 Hz line arrives in a 60 Hz facility [NEED_CITE: electrical standard mismatches in exported food machinery].
Documentation & Verification
- Line layout and capacity calculation showing throughput match across mixing, extrusion, flaking, drying, roasting and coating stations
- Screw and die configuration record specifying the profile matched to your corn or maize formulation
- Electrical schematic with voltage and frequency confirmation for your facility’s power supply
- Trial run report from in-house testing workshop documenting output on your raw material before dispatch
- CE declaration of conformity and ISO certificate for the complete line
Installation, Commissioning & Support
- Foundation and floor space planning based on the full line footprint including dryer and roaster sections
- Dedicated electrical circuits sized for the combined PLC-controlled extruder, dryer and coating station loads
- Assembly and alignment of flaking rollers verified on-site to match the extruder die output rate
- First-run parameter setting covering extrusion speed, drying temperature and coating volume for your product spec
- Operator training on PLC interface covering product changeover between plain flakes and coated variants
- Wear parts list covering screws, dies and flaking roller surfaces with recommended replacement intervals
What to Include When Requesting a Line Proposal
To size a corn flakes breakfast cereals processing line equipment range accurately, share your target formulation including grain type, sugar ratio and any cocoa or vitamin premix, along with the hourly output you need the finished product to reach. Specify your facility’s voltage, frequency and available floor space so the layout can be drawn to your actual conditions. If you are replacing or extending an existing line, note the upstream and downstream equipment already in place so the new stations can be matched to your current throughput.
Frequently Asked Questions
Q: How is throughput matched between extruder, flaker, dryer and coating stations on the line?
A: Each station’s capacity is calculated during the line layout phase based on your target output and raw material. The extruder’s die output rate sets the baseline, and the flaker, dryer, roaster and coating drum are then specified to handle that rate without queuing or starvation. This matching is documented in the capacity calculation before production begins.
Q: What screw configuration is specified for corn versus maize versus cocoa formulations?
A: The screw profile is selected based on the specific raw material blend you provide. Corn grits, maize flour and cocoa-blended formulations each have different starch gelatinization behavior, so the configuration record is built around your formulation rather than a generic template. A trial run in the testing workshop validates the selection before shipment.
Q: Which line stations are included and where does each fit in the production sequence?
A: The line covers mixing, extrusion, flaking, drying, roasting, coating and packaging in sequence. Mixing prepares the raw blend, the twin-screw extruder gelatinizes the dough, the flaker sets thickness, the dryer removes moisture, the roaster develops color, the coating drum applies chocolate or sugar, and the packaging station handles final bagging.
Q: Can flaking thickness, coating volume and drying temperature be adjusted for different cereal formats?
A: Yes. The PLC system allows operators to adjust flaking roller gap, coating drum feed rate, drying temperature and extrusion speed independently. This means the same line can produce thin crispy corn flakes and thicker coated maize chocos by changing parameter sets rather than swapping hardware.
Q: What utility requirements does the full line need?
A: The line requires electrical supply at the voltage and frequency confirmed for your market, along with steam for certain drying stages and compressed air for pneumatic controls. Exact utility loads are calculated during the line layout phase and documented in the electrical schematic provided before production.