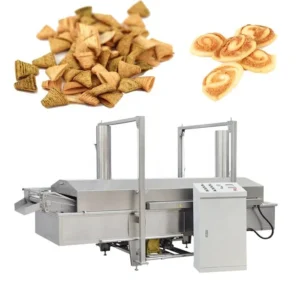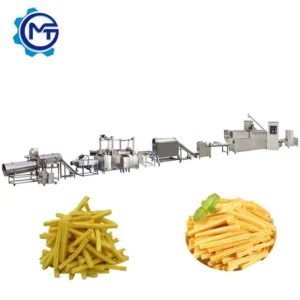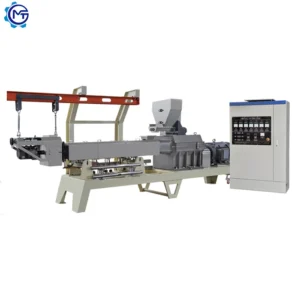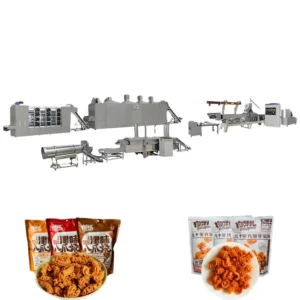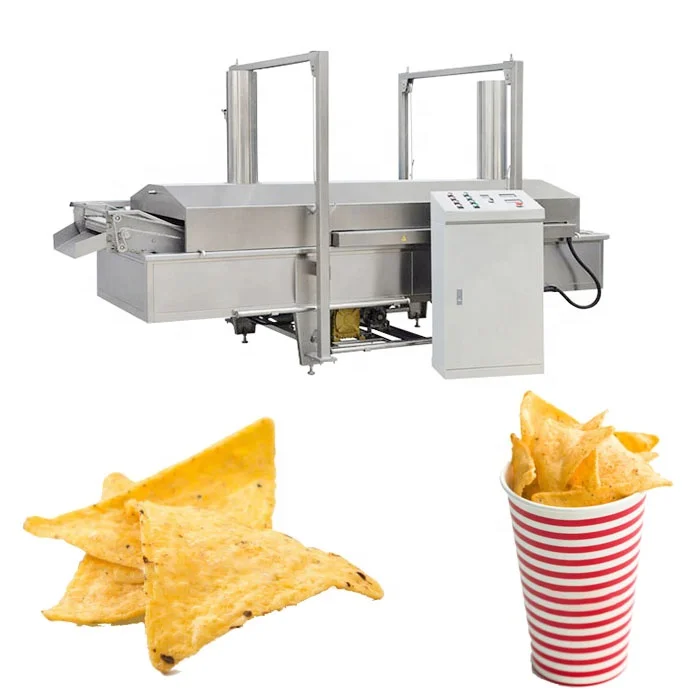
Matched Throughput Across Every Station — the mixing, extruding, frying, and flavoring units are capacity-balanced under one build, so your bugles snack production line runs without a single bottleneck holding back output.
Technical Specifications
| Parameter | Value |
|---|---|
| Model | MT65 / MT70 / MT85 / MT75 / MT95 |
| Product Type | Bugles Chips Frying Snack Production Line |
| Extruder Type | Twin Screw Extruder |
| Installed Power | 142 kW (MT65) / 185 kW (MT70) / 240 kW (MT85) / 245 kW (MT75) / 370 kW (MT95) |
| Real Power Consumption | 100 kW (MT65) / 130 kW (MT70) / 180 kW (MT85) / 185 kW (MT75) / 280 kW (MT95) |
| Output Capacity | 120–150 kg/h (MT65) / 200–250 kg/h (MT70) / 300–500 kg/h (MT85) / 400–500 kg/h (MT75) / 800–1000 kg/h (MT95) (basis not stated in source — confirm raw material formulation and moisture content) |
| Fryer Temperature Range | 0–260 °C |
| Fryer Dimension | 4500 × 1350 × 2350 mm |
| Mixer Tank Volume | 150 kg |
| Mixer Rotary Speed | 385 rpm |
| Overall Dimensions | 22000×1200×2200 mm (MT65) to 30000×1500×2800 mm (MT95) |
| Food Contact Material | 304 Stainless Steel |
| Warranty | 1 year complete warranty, life-time maintenance service |
Application Suitability
| Application | Material or Output |
|---|---|
| Bugles and corn horns | Corn flour and grits with moisture-adjusted formulation |
| Tortilla chips and rice crust | Rice flour, corn starch blends |
| Shaped fried snacks | Dough from wheat, corn, or potato starch for fish, duck, tree, and triangle shapes |
| Sala and corn curls | Corn-based meal with seasoning compatibility |
| Small-scale to high-volume production | Entry-level MT65 batch runs up to MT95 continuous output |
Why Nominal Output Figures Fail at the Fryer Stage
Many buyers discover after installation that a line rated for a certain throughput cannot sustain it when the actual raw material enters the fryer. The frying chips making machine manufacturer must verify the full chain against your specific flour blend and moisture level before dispatch. A twin-screw extruder may push dough at the stated rate, but if the fryer oil recovery time is too slow or the conveyor speed is mismatched, the finished product emerges undercooked or oil-logged. This mismatch typically surfaces only when the buyer’s own corn or rice formulation differs from the supplier’s test material [NEED_CITE: common causes of throughput loss in snack frying lines].
How the Twin-Screw Configuration Handles Diverse Snack Formulations
A twin-screw extruder gives processors the shear control needed to gelatinize starches evenly across different flour types. Corn grits, rice flour, and potato starch blends each respond differently to barrel temperature and screw speed, and the configurable screw elements allow the operator to adjust residence time and mechanical energy input. This flexibility is what makes the same frying chips making machine capable of producing dense tortilla chips on one run and light, expanded bugles on the next simply by changing the die and adjusting the moisture feed.
Die and Cutter Interchangeability for Shape Variety
The die plate at the extruder discharge determines the cross-section of the extrudate — bugles, triangles, fish, gourds, or Christmas tree shapes. Swapping a die typically involves loosening the die clamp, pulling the current insert, and seating the new one with its matching cutter assembly. For contract snack producers running multiple SKUs on a single line, this changeover speed directly affects shift utilization and the number of product formats that can be offered in a given production window [NEED_CITE: die changeover practices in extruded snack lines].
Reading the Power and Capacity Tiers
The installed power ranges from 142 kW on the MT65 to 370 kW on the MT95, but real consumption during steady-state operation is notably lower — 100 kW and 280 kW respectively. This gap reflects the startup surge needed to bring the extruder barrel up to temperature and fill the fryer with product. The fryer’s 0–260 °C range covers the lower temperatures required for gentle expansion of delicate rice-based shapes and the higher end needed for rapid moisture flash-off in dense corn bugles. Mixer capacity at 150 kg per batch with a 385 rpm rotary speed ensures that dough reaches the extruder hopper at consistent intervals, preventing starvation or surge feeding that would disrupt extrudate density.
The Hidden Cost of a Mismatched Flavoring Drum
If the flavoring drum output is not balanced with the fryer discharge rate, seasoned product piles up or the drum runs partially empty, both of which lead to uneven coating. Under-seasoned product fails sensory checks at the packing stage, while over-seasoned batches drive up raw material costs on expensive cheese or spice powders. A line where the flavor station is undersized relative to the fryer forces operators to slow the entire line back to the drum’s capacity, negating the extruder’s throughput advantage [NEED_CITE: seasoning uniformity standards in snack food processing].
Why Procurement from a Single Line Builder Matters
Sourcing the extruder, fryer, and flavoring drum from one supplier means throughput calculations are performed across every station as a system rather than assembled from individual machine ratings. The 304 stainless steel construction across all food-contact surfaces simplifies hygiene audits and meets export market requirements. Before shipment, the full line can be trial-run on the buyer’s own raw material in the testing workshop, catching formulation-specific issues like low starch gelatinization or poor expansion before the equipment reaches the factory floor. Screw configuration and die selection are documented and matched to the buyer’s target shape and flour blend, not copied from a generic template. Electrical schematics are confirmed against the destination market’s voltage and frequency standards before production begins.
Documentation & Verification
- Line layout drawing showing station-by-station throughput match for your chosen model
- Screw and die configuration record tied to your target snack shape and flour blend
- Electrical schematic with confirmed voltage and frequency for your facility
- Trial run report using your supplied raw material verifying extrudate and fried product quality
- CE declaration of conformity and ISO certificate for export compliance
- Wear parts list covering screws, dies, and cutting blades with replacement intervals
Installation, Commissioning & Support
- Foundation leveling for the longest model at 30000 mm length requiring a continuous concrete slab
- Dedicated power circuit sized to the MT95’s 370 kW installed capacity with local voltage confirmation
- Modular station delivery allowing phased assembly in facilities with limited overhead clearance
- Fryer oil fill, temperature calibration, and conveyor speed tuning during on-site commissioning
- Operator training covering die changeover, screw cleaning, and fryer oil filtration routines
- Spare screws, dies, and cutter blades shipped with the initial order to cover the first replacement cycle
Preparing Your Line Inquiry
To receive an accurate configuration, share your primary raw material formulation including flour type and moisture content, along with your target hourly output and the snack shapes you intend to produce. Specify your facility’s voltage, frequency, and any preferred control language so the electrical package can be quoted correctly. If you have existing upstream mixing or downstream packing equipment, note the interface dimensions so the new line integrates without modification.
Frequently Asked Questions
Q: How is the output capacity verified before shipment?
A: Output figures are based on specific raw material formulations and moisture levels. We run a trial in the testing workshop using your supplied flour blend, measuring actual throughput through the extruder, fryer, and flavoring drum. The trial run report documents real capacity, product texture, and expansion behavior so you know what to expect at commissioning.
Q: How do I choose between MT65, MT70, MT75, MT85, and MT95?
A: Selection depends on your target hourly output and the range of shapes you plan to run. The MT65 suits entry-level production for new snack brands, while the MT95 serves established manufacturers running continuous shifts. We match each model’s fryer and flavoring station to the extruder output so no station limits the line.
Q: What voltage and control language options are available?
A: Voltage and frequency are configured to match your facility’s supply before production starts. Control panel language is set based on your operator preference. Electrical schematics are provided for review and approval prior to manufacturing so there are no commissioning delays due to power incompatibility.
Q: Can one line produce multiple snack shapes?
A: Yes. By swapping the die insert and matching cutter assembly, the same twin-screw extruder can produce bugles, triangles, fish shapes, and other formats. Changeover involves removing the die clamp and seating the new insert, which allows contract producers to run multiple SKUs within a single shift.
Q: What spare wear parts are included with the initial order?
A: Each line ships with a documented wear parts list covering screws, dies, and cutting blades. An initial set of spares is included to cover the first replacement cycle. Ongoing supply is arranged through the after-sales channel so replacements arrive before your current parts reach end of life.