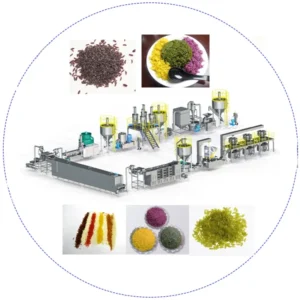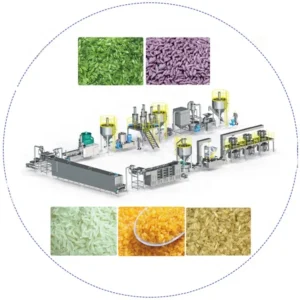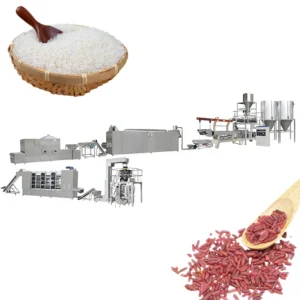
Integrated Line Throughput Matching — every station from mixer to fryer is balanced so the Fortified Nutritional Rice Production Line Full Equipment runs without bottlenecks, verified through pre-shipment trial runs on your actual grain formulation.
Technical Specifications
| Parameter | Value |
|---|---|
| Product Type | Fortified Nutritional Rice Production Line |
| Output Capacity | 70–300 kg/h (basis not stated in source — confirm raw material formulation, moisture content, product format) |
| Voltage & Frequency | 380V / 50Hz |
| Control System | Automatic control (PLC / MCC option to be confirmed) |
| Construction Material | Food-grade stainless steel contact surfaces |
| Color | Silver |
| Line Stations | Mixer, extrusion system, fryer (dryer, cooler, packing to be confirmed) |
Application Suitability
| Application | Material or Output |
|---|---|
| Fortified rice production | Rice flour blended with micronutrient premix |
| Artificial rice from broken rice | Reconstituted rice flour with starch binders |
| Grain-based nutritional rice | Multi-grain flour formulations including millet, sorghum, maize |
| Infant and weaning rice cereal | Fine rice flour with vitamin and mineral fortification |
What "300 kg/h" Leaves Out About Fortified Rice Lines
Capacity means nothing when the dryer cannot keep pace with the extruder.
I have watched lines in South Asian rice mills where the extruder pushed product faster than the downstream fryer could handle, leaving trays of half-formed rice kernels piling up on the floor. The Fortified Nutritional Rice Production Line Full Equipment spec sheet may show an attractive throughput number, but if the mixer batch size, extruder screw speed, and fryer belt length are not calculated as one system, that number collapses on day one of production [NEED_CITE: line throughput balancing principles in food extrusion]. Buyers evaluating this equipment should request a station-by-station capacity breakdown rather than accepting a single headline figure.
How Each Station Fits the Rice Extrusion Flow
The Fortified Nutritional Rice Production Line Full Equipment begins with a mixer that must achieve uniform distribution of micronutrient premix through the rice flour base before any heat is applied. Uneven blending at this stage creates hotspots of iron or zinc that survive extrusion and show up as discolored kernels in the final product. The extrusion system then gelatinizes the starch matrix under controlled moisture and temperature, forming the rice kernel shape through a dedicated die plate. After forming, the fryer sets the kernel structure and reduces moisture to a shelf-stable level, which is why fryer residence time must match the extruder output rate exactly.
Why Raw Material Behavior Dictates Station Configuration
Different grain flours absorb water at different rates and gelatinize at different temperatures, which changes what the extruder barrel profile must deliver [NEED_CITE: starch gelatinization temperature ranges for rice and millet flours]. A line configured for pure rice flour will underperform when the buyer switches to a sorghum-heavy blend because the barrel zones need higher shear to break down the tougher starch granules. This is precisely why running a trial on the buyer’s actual formulation before shipment matters — screw pitch, die aperture, and fryer temperature all shift when the raw material changes, and discovering that after installation costs weeks of wasted production.
Reading the Specs That Actually Shape Rice Kernel Quality
The 380V / 50Hz electrical supply points to a three-phase industrial installation, and buyers in regions running 60Hz or different voltage standards must confirm transformer or drive compatibility before the line ships — rewiring a control panel on-site delays commissioning and risks motor damage. Food-grade stainless steel across contact surfaces is necessary for nutritional rice because micronutrient premixes containing iron and zinc salts accelerate corrosion on untreated carbon steel. The automatic control system should maintain consistent barrel temperature and screw speed across production runs, since even minor drift in these parameters changes kernel density and causes some grains to float while others sink during cooking — a defect that consumers notice immediately.
The Cost of Skipping Station-by-Station Verification
When a line arrives with an undersized fryer, the extruder must be throttled back to match, which drops actual throughput well below the quoted figure and extends payback timelines the buyer modeled their financing around [NEED_CITE: common causes of extrusion line underperformance in emerging markets]. In one project I supported, a nutritional rice line ran at barely half its nameplate capacity for three months because the dryer belt was too short for the moisture load the extruder was delivering. The buyer had signed off on a quotation that listed every station but never showed how their capacities aligned.
Why Sourcing This Line Here Makes Sense for Buyers
Complete line coverage from mixing through frying under one supplier means throughput is matched at every station rather than assembled from separate vendors who each optimize only their own machine. Screw configuration and die design are specified to the buyer’s grain formulation and target kernel shape, not copied from a generic rice extrusion build. An in-house testing workshop allows trial runs on the buyer’s actual raw material before the line ships, so parameters are adjusted in the factory rather than during a stressful on-site commissioning. Twin-screw expertise across grain processing applications means the engineering team understands how rice flour behaves differently from maize or cassava starch inside the barrel.
Documentation & Verification
- Line layout drawing showing mixer, extruder, fryer, and supporting station positions
- Machine specification sheet listing every station with individual utility requirements
- Screw and die configuration record matched to your rice flour formulation
- Factory test record from trial run on your raw material before dispatch
- Electrical schematic confirming voltage, frequency, and control language
- Operation and maintenance manual covering all stations in the line
Installation, Commissioning & Support
- Three-phase 380V / 50Hz dedicated circuit with isolation switch rated to line power draw
- Level concrete floor with drainage provision for mixer and fryer wash-down
- Modular station delivery allowing assembly in workshops with limited access doors
- First-run commissioning with barrel temperature and screw speed profiling for your formulation
- Operator training covering die changeover, fryer belt tension, and control panel navigation
- Wear parts list identifying screws, dies, and fryer belt segments with replacement intervals
What We Need to Configure Your Line Accurately
Share the exact grain flour blend you plan to run, including the percentage of rice, millet, or other cereals and the micronutrient premix composition. Tell us your target daily output in finished kilograms, your workshop floor dimensions, and the local voltage and frequency standard at your facility. If you have existing upstream milling or downstream packing equipment, provide the model and throughput so we can match the line to your current flow.
Frequently Asked Questions
Q: What supporting stations are included beyond the extruder, mixer, and fryer?
A: The standard Fortified Nutritional Rice Production Line Full Equipment configuration covers mixing, extrusion, and frying. Additional stations such as a dryer, cooler, polishing drum, and packing system can be included depending on your target moisture level and packaging format. We confirm the full station list during the line layout proposal stage based on your product specification.
Q: How is throughput matched between each station to avoid line bottlenecks?
A: Each station is sized against the extruder output rate so that mixer batch cycles, fryer belt speed, and any intermediate conveying capacity all align. We calculate this during the layout phase and verify it during the factory trial run on your raw material, adjusting screw speed or belt length if any station falls behind.
Q: What raw material formulations are compatible with this line configuration?
A: The line processes rice flour, broken rice reconstituted into flour, and multi-grain blends incorporating millet, sorghum, or maize. Micronutrient premixes containing vitamins, iron, zinc, and folic acid are compatible. We recommend a pre-shipment trial on your specific blend to confirm screw and die settings deliver the correct kernel density.
Q: What utility connections are required for the full line?
A: The line requires a 380V / 50Hz three-phase power supply with dedicated circuits for the extruder motor and fryer heating elements. Water supply is needed for the mixer and barrel cooling zones. Steam injection may be required depending on your formulation’s gelatinization profile — we confirm this during the specification stage.
Q: Can individual stations be selected or replaced to fit an existing layout?
A: Yes. If you already operate a mixer or packing system, we can supply the extrusion and frying stations alone and match their throughput to your existing equipment. We request the specifications of your current machines to ensure interface compatibility and consistent material flow across the line.