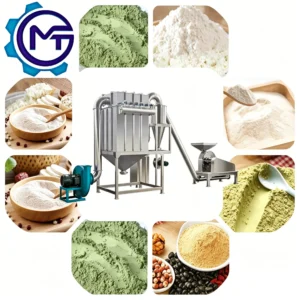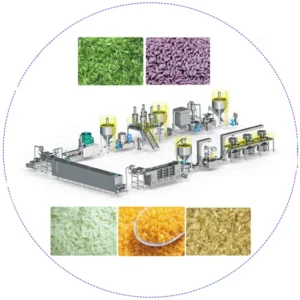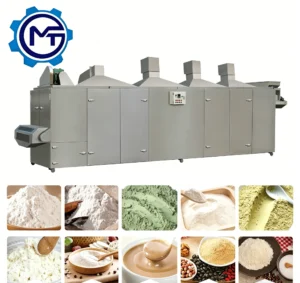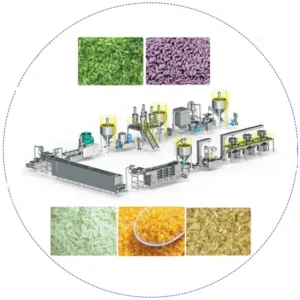
Complete Equipment Range — every station from batching to packing is specified and throughput-matched for this artificial rice line, so no single machine bottlenecks the output.
Technical Specifications
| Parameter | Value |
|---|---|
| Model | MT65 |
| Product Type | Fortified Artificial Rice Production Line |
| Screw Type | Twin Screw |
| Installed Power | 85 kW |
| Power Consumption | 60 kW |
| Output Capacity | 80–100 kg/hr (basis not stated in source — confirm raw material formulation / moisture content) |
| Overall Dimensions (L×W×H) | 28 × 1.2 × 2.2 m |
| Feeding System | Single or double screw feeding (configurable per material) |
| Control System | Frequency speed control |
| Lubrication | Automatic lubricating and cooling |
| Dryer Heating Source | Electric or gas |
| Dryer Feature | Circulation drying with frequency motor mesh belt speed control |
| Capacity Range Across Series | 100 kg/hr to 600 kg/hr (basis to be confirmed) |
| Standards | CE (referenced in company profile — verify declaration for this model) |
Application Suitability
| Application | Material or Output |
|---|---|
| Fortified rice kernel manufacturing | Broken rice, corn, millet, wheat with added vitamins and minerals |
| Artificial rice from alternative grains | Oats, buckwheat, bean, starch blends |
| Nutritional rice for food programmes | Grain-based formulations with micro-nutrient fortification |
| Grain-based extruded kernels | Multi-grain blends processed through twin-screw extrusion |
Why Bottlenecking Happens When Extruders Are Specified Alone
A Fortified Artificial Rice Production Line full equipment range only delivers its rated throughput when every downstream station is sized to match the extruder output.
I have walked onto factory floors where a well-chosen extruder sat idle for twenty minutes every hour because the cooling conveyor could not carry the volume away. The pellets piled up, moisture trapped between them, and what should have been clean, separate kernels turned into a clumped mass heading for the reject bin. Sizing the dryer, cooler, and packing station against the actual extruder discharge rate — not a catalogue headline number — is where line reliability is won or lost [NEED_CITE: industrial line throughput matching principles for food extrusion].
Matching Every Station Across the Fortified Artificial Rice Production Line
A complete Fortified Artificial Rice Production Line full equipment range covers mixing, twin-screw extrusion, vibrating separation, low-temperature drying, cooling, high-temperature roasting, a second cooling stage, and packing. Each station must handle the mass flow leaving the one before it, adjusted for moisture loss in the dryer and volume change after roasting. When any link is undersized, operators are forced to throttle the extruder back, wasting installed capacity and shifting the entire energy cost per kilogram upward.
How Raw Material Choices Shift Station Requirements
The basic materials listed for this line — broken rice, corn, millet, wheat, oats, buckwheat, bean, and starch — each carry different initial moisture levels and gelatinisation temperatures. A formulation heavy in bean flour will demand longer residence time in the dryer than one based primarily on rice grits, meaning the mesh belt speed on the circulation dryer must be adjustable rather than fixed. Frequency motor control on the dryer belt allows operators to dial in the right drying curve without swapping hardware between production runs [NEED_CITE: moisture migration rates in grain-based extruded products].
What the Specification Sheet Tells You About Real Output
The MT65 carries an installed power of 85 kW with a running consumption of 60 kW, indicating that the motors are not continuously loaded to their maximum — a margin that helps when tougher formulations briefly increase torque demand on the screws. The twin-screw configuration provides positive conveying for viscous, vitamin-fortified doughs that a single screw might stall on. Automatic lubricating and cooling keeps barrel temperatures within range during extended shifts, preventing the kind of thermal drift that pushes kernel density outside market specification. Line footprint at 28 metres long by 1.2 metres wide is compact enough for most food-grade workshops, though ceiling height of 2.2 metres must be verified against any overhead hopper or elevator installation.
The Hidden Cost of Skipping Upstream and Downstream Surveys
I once spent two days on a commissioning job where the mixer discharged faster than the extruder hopper could accept material, causing bridging and inconsistent feed density. The resulting kernels varied in size and cooking time — unacceptable for a retail pack. These problems do not show up on a quotation that lists machines one by one without a line-level capacity calculation. Buyers who skip the throughput survey end up paying for corrective conveyors, modified hoppers, and lost production weeks after the equipment arrives [NEED_CITE: common commissioning failures in grain extrusion lines].
Why Procurement Teams Source the Full Catalogue Here
Every station from batching through packing is available from a single supplier, meaning throughput matching is calculated before the first machine is built rather than discovered during installation. Screw configuration and die design are specified to the buyer’s actual raw material blend, not copied from a generic reference build. The in-house testing workshop runs trial batches on customer-supplied ingredients before shipment, so product development begins weeks earlier than it would on site. Pre-sales engineering covers line layout, utility planning, and electrical schematics with voltage confirmed to local standards, reducing commissioning surprises. Ongoing support includes operator training, wear parts supply, and maintenance guidance matched to the exact screw and barrel set installed.
Documentation & Verification
- Machine specification sheet listing installed power, consumption, and footprint for each station
- Line layout and capacity calculation showing throughput matching across extruder, dryer, and cooler
- Screw and die configuration record tied to your raw material formulation
- Electrical schematic with voltage and frequency confirmation for your local supply
- Trial run report produced on your ingredient blend before dispatch
- CE declaration of conformity with supporting factory test record
Installation, Commissioning & Support
- Foundation and floor leveling checked against the 28 × 1.2 × 2.2 m line footprint
- Dedicated electrical circuit sized for 85 kW installed power at confirmed local voltage
- Extruder barrels and screws shipped separated, reassembled on site during commissioning
- First-run parameter setting for die pressure, belt speed, and dryer temperature profile
- Operator training covering frequency speed control and automatic lubrication monitoring
- Wear parts list with recommended reorder intervals for screws, dies, and mesh belt sections
What to Prepare Before Requesting a Quotation
Share your raw material formulation including the percentage of each grain, starch, and micro-nutrient additive, along with the target kernel shape and cooking-time specification. Confirm your local voltage and frequency so the electrical schematic and control language can be set before build. Provide workshop length, width, and ceiling height to verify the line layout fits, and note any existing upstream mixers or downstream packing machines that the new stations must connect to.
Frequently Asked Questions
Q: How do I select the right extruder model from the MT65 through the larger series for my target capacity?
A: The MT65 covers the entry tier of the range. Selection depends on your target hourly output and the specific grain formulation you intend to run, because denser blends reduce effective throughput compared to lighter starch-based recipes. Sharing your formulation allows the correct model to be matched against verified capacity data rather than catalogue nominal figures.
Q: What supporting equipment is needed to match the extruder and avoid bottlenecks on the line?
A: Beyond the extruder itself, the line requires a mixer sized to the extruder’s consumption rate, a circulation dryer with adjustable belt speed, a cooling conveyor long enough to bring kernel temperature below packing threshold, and a roasting station matched to the throughput. Each station must be calculated against the actual discharge mass flow, not the nominal catalogue rating.
Q: Can the feeding system be configured for my specific raw material blend?
A: Yes. The MT65 offers single or double screw feeding, selectable based on how uniformly your ingredient blend flows. Powders with fine vitamin premixes typically benefit from double screw feeding to prevent segregation, while coarser grain mixes can run reliably on a single screw arrangement.
Q: What are the voltage and control language options for each machine in the catalogue?
A: Electrical systems are configured to the buyer’s local voltage and frequency before build. Control interfaces and frequency speed drives can be set to match the operator language requirement. Confirming these details during the quotation stage prevents commissioning delays once the line arrives on site.
Q: What is the footprint requirement for the MT65 and the full line layout?
A: The MT65 line occupies approximately 28 metres in length, 1.2 metres in width, and 2.2 metres in height. Actual floor plan depends on dryer configuration and whether the packing station is inline or offset. Providing your workshop dimensions allows a detailed layout drawing to be prepared before the order is confirmed.