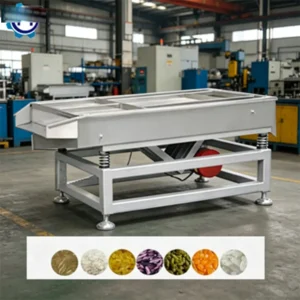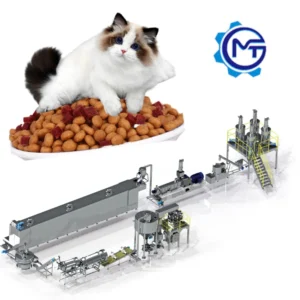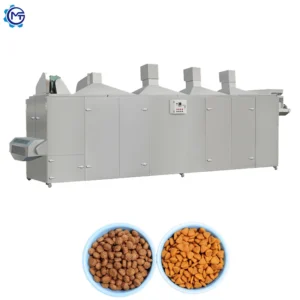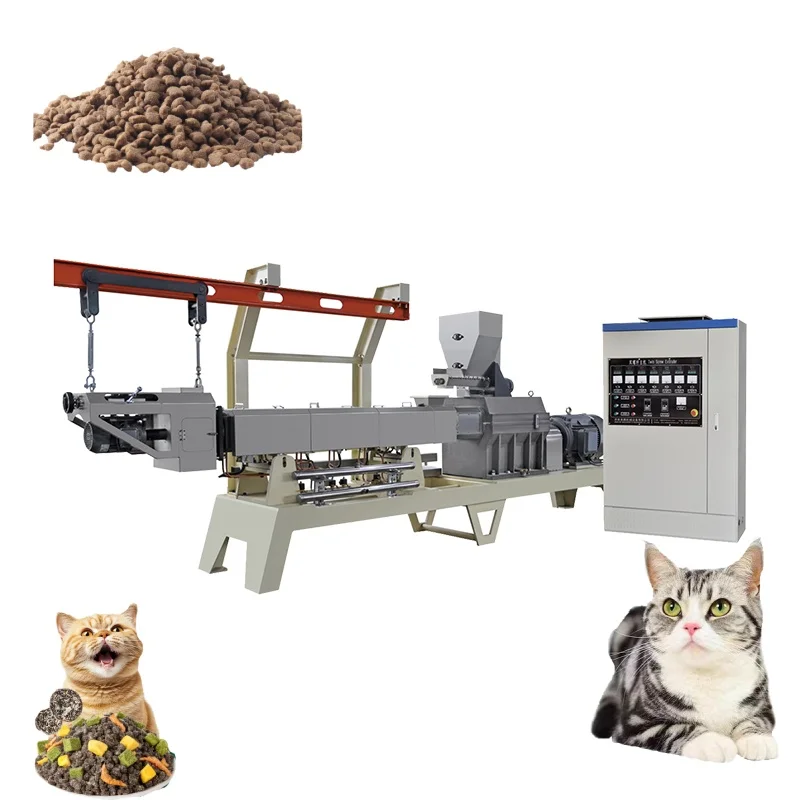
Complete Line Matching — every station from mixing to packing is specified for throughput balance, eliminating the bottleneck risk when assembling a pet food extrusion line from separate vendors.
Technical Specifications
| Parameter | Value |
|---|---|
| Product Type | Pet Food Extrusion Production Line |
| Output Capacity | Up to 3 tons per hour (basis not stated in source — confirm raw material, moisture content, pellet size and formulation) |
| Screw Type | Twin-screw |
| Applications Supported | Dog food, cat food, fish feed production |
| Line Stations | Mixing, extrusion, drying, coating/flavouring, cooling, packing |
| Control System | PLC and MCC automated control |
| Certification | CE, ISO |
| Warranty | 1-year comprehensive warranty |
| Assembly State | Complete production line with supporting equipment |
| Factory Testing | In-house testing workshop with trial runs on customer raw material before shipment |
| Process Visualization | Process drawing included for production flow clarity |
Application Suitability
| Application | Material or Output |
|---|---|
| Dry kibble for dogs | Meat meal, corn, wheat, soy with varying protein-to-starch ratios |
| Premium cat food pellets | High-protein formulations with animal-based ingredients |
| Floating aquatic feed | Fish meal, rice bran, starch blends for catfish and tilapia |
| Sinking aquatic feed | Denser formulations for bottom-feeding species and shrimp |
| Functional pet treats | Fortified blends with added vitamins, minerals and fibre |
What "Up to 3 Tons per Hour" Actually Means for Your Pet Food Processing Equipment
Capacity is a function of your recipe, not just the machine.
I have watched buyers compare Pet Food Processing Equipment manufacturer quotations based on a single output number, only to discover during commissioning that their high-problem formulation — heavy on meat meal, light on starch — pulls the real throughput well below the brochure figure. The extruder barrel fills differently, the die back-pressure changes, and the downstream dryer cannot keep up if it was sized for a lighter recipe. When the dog cat feed making machine for sale is quoted without a confirmed raw material baseline, the capacity number is essentially a placeholder. [NEED_CITE: relationship between raw material bulk density and extruder throughput in food processing]
Every Station, One Equipment Catalogue
The mtfoodmachinery.com catalogue covers every supporting station that a Pet Food Processing Equipment manufacturer must supply for a balanced line: batching and mixing systems, screw conveyors, the twin-screw extruder itself, multi-pass dryers, flavouring drums, coating lines, cooling conveyors and packing stations. When you survey the full range before specifying, you can confirm that the dryer volume matches the extruder output at your specific moisture removal rate, and that the coating drum residence time is long enough for your fat-application target.
How Throughput Matching Prevents Line Bottlenecks
A common failure mode in assembled lines is an extruder that outpaces its dryer. The kibble exits the die at high moisture and must be brought down to a shelf-stable level before packing. If the dryer was selected on nominal capacity rather than your actual evaporation load, wet product piles up on the cooling belt, mould risk increases, and the line stalls. Specifying every station from one catalogue lets the supplier calculate evaporation duty, belt speed and dwell time as linked variables rather than independent guesses. [NEED_CITE: moisture removal rate calculation in multi-pass food dryers]
Screw Geometry, Die Design and the Density Your Market Expects
The twin-screw configuration allows the screw elements to be rearranged — forward-flight, reverse-flight and kneading blocks in sequence — so that shear intensity and residence time match your raw material. A high-protein cat food recipe demands a different screw profile from a starch-heavy dog kibble. The die opening diameter and land length then determine pellet expansion ratio and final bulk density. These choices are recorded in the screw and die configuration document that accompanies each line, so reordering wear parts later is straightforward and repeatable.
The Hidden Cost of Mismatched Supporting Equipment
When a flavouring drum is undersized relative to the extruder output, the coating layer thins out and palatability drops. When the cooling conveyor is too short, residual heat drives condensation inside the bag, shortening shelf life. These are not defects in the Pet Food Processing Equipment manufacturer hardware; they are sizing errors that surface only after the line runs continuously for several shifts. The financial impact shows up as customer complaints, product returns and unplanned downtime rather than as a single visible machine failure. [NEED_CITE: condensation risk in packaged pet food due to insufficient cooling]
Why Buyers Survey the Full Range Before Specifying
The line is only as reliable as its weakest station-to-station hand-off. Meiteng engineers calculate throughput at every transfer point — from the mixer discharge into the extruder feed hopper, from the die face into the dryer belt, from the coating drum into the cooler — so that no single machine runs starved or overloaded. The PLC and MCC control architecture is designed around the same line layout, allowing interlocks that stop upstream feeding if a downstream station trips. Factory trial runs on the buyer’s actual raw material validate these calculations before the equipment leaves Jinan. The CE and ISO documentation package confirms compliance for your destination market without last-minute certification scrambles.
Documentation & Verification
- Line layout and capacity calculation showing throughput at every station for your recipe
- Screw and die configuration record matched to your raw material and target pellet density
- Electrical schematic with voltage, frequency and control language confirmed for your facility
- Trial run report generated in the testing workshop on your actual raw material before dispatch
- CE declaration of conformity and ISO certificate for customs and regulatory clearance
- Operation and maintenance manual with wear parts list specific to your line configuration
Installation, Commissioning & Support
- Foundation plan and utility drop points mapped to the PLC and MCC cabinet locations
- Power circuit sized for the twin-screw extruder main drive and dryer heating loads
- Mechanical assembly sequence with station-by-station alignment checks
- First-run parameter setting covering barrel temperature zones and screw speed ramp
- Operator training on control interface, recipe recall and emergency stop routines
- Wear parts list covering screws, dies and dryer belt sections with reorder lead times
What to Prepare Before Requesting a Quotation
Share your target kibble or pellet size, the full ingredient list with approximate ratios, and your daily output target so the line can be sized station by station. Confirm your facility voltage, frequency and preferred control language to avoid rewiring during commissioning. If you have existing upstream batching or downstream packing equipment, provide make and capacity details so the new Pet Food Extrusion Production Line integrates cleanly at the connection points.
Frequently Asked Questions
Q: What supporting equipment stations are included and how is throughput matched across the line?
A: The line covers mixing, extrusion, drying, coating, cooling and packing. Each station is sized based on your recipe moisture, density and output target so that material flow remains continuous without bottlenecks between the twin-screw extruder and downstream equipment.
Q: How do I select the right dryer, flavouring drum and coating system for my product format?
A: Selection depends on pellet moisture content at the die exit, target final moisture and fat-application rate. The dryer pass count and drum diameter are calculated from your specific evaporation and coating requirements rather than chosen from a generic table.
Q: What is the footprint and utility requirement for a complete line at my target capacity?
A: Footprint varies with dryer length, cooler configuration and packing format. A line layout drawing with utility drop points for power, water and compressed air is prepared once your capacity target and raw material formulation are confirmed.
Q: Can I see the full machine catalogue and compare configurations before specifying?
A: Yes. The equipment catalogue covers every station individually so you can review options for mixer size, dryer type, coating system and packing format before committing to a complete line configuration.
Q: How are voltage, frequency and control language confirmed for my market?
A: Electrical specifications are confirmed during the proposal stage. The PLC interface language and MCC component ratings are set to match your facility standards before production begins, avoiding rewiring or reprogramming during on-site commissioning.