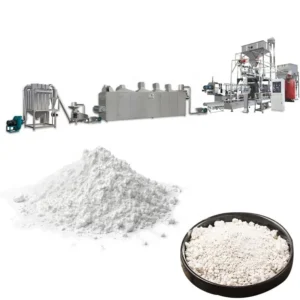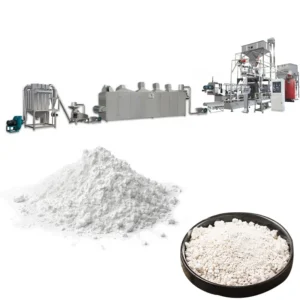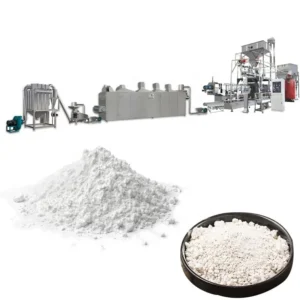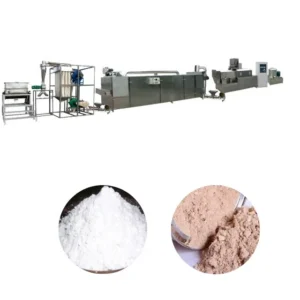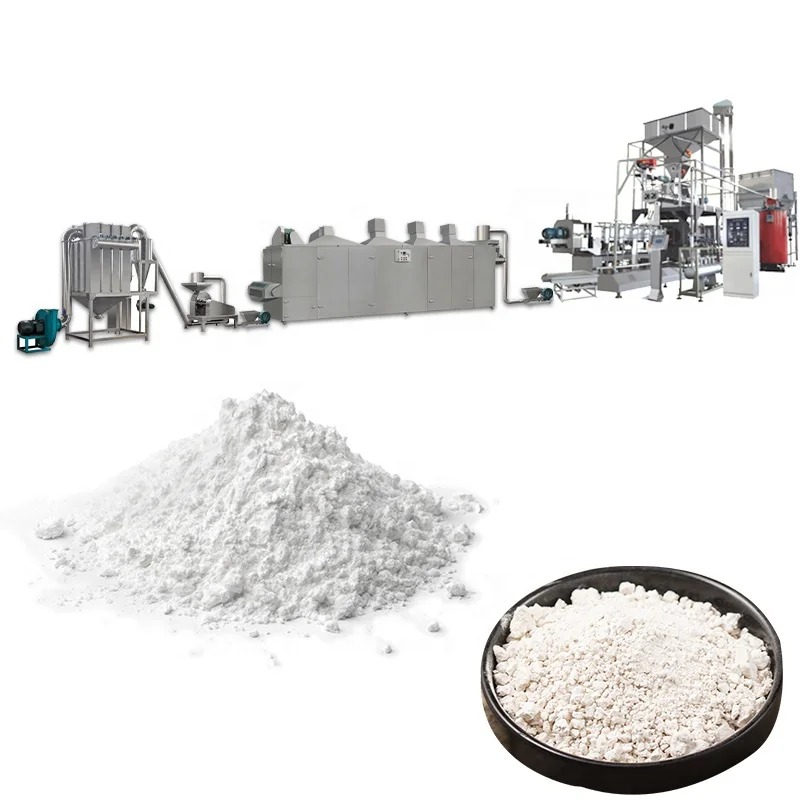
Integrated Extrusion Architecture — Every station from flour mixer to packaging machine is engineered as one matched system, ensuring throughput balance across the full modified starch processing line rather than assembling mismatched standalone units.
Technical Specifications
| Parameter | Value |
|---|---|
| Product Type | Twin Screw Modified Starch Processing Line |
| Model | MT75 |
| Installed Power | 180 kW |
| Power Consumption | 135 kW |
| Output Capacity | 200–250 kg/h (basis not stated in source — confirm raw material type, moisture content, and starch variety) |
| Overall Dimensions (L×W×H) | 32,000 × 3,500 × 4,300 mm |
| Screw Configuration | Twin Screw |
| Control System | Frequency conversion speed regulation on feeding, driving, and rotary cutting |
| Mixer Power Options | 4 kW / 7.5 kW / 15 kW |
| Mixer Batch Capacity | 20–30 kg / 70–80 kg / 170–180 kg |
| Mixer Voltage | 380 V, 50 Hz, Three Phase |
| Mixer Contact Material | Stainless Steel 201 or 304 (selectable) |
| Dryer Type | Multi-layer oven with double pitch roller chain transmission |
| Pulse Grinder Drive Motor | 15 kW |
| Pulse Grinder Mesh Range | 100–120 mesh |
| Raw Materials | Corn starch, cassava starch, potato starch, maize starch, tapioca starch |
Application Suitability
| Application | Material or Output |
|---|---|
| Pre-gelatinized starch for food additives | Cassava starch, corn starch |
| Oil drilling starch production | Maize starch, modified starch blends |
| Nutritional and infant formula powders | Rice starch, potato starch, soybean powder blends |
| Industrial modified starch processing | Tapioca starch, corn starch with chemical or physical modification |
| Baby rice powder and sesame paste production | Rice-based and multi-grain starch formulations |
Why Throughput Balance Matters More Than Extruder Capacity Alone
A Modified Starch Processing Line for sale often advertises an impressive extruder output, yet the dryer and grinder downstream cannot keep up — creating a bottleneck that forces the entire operation to run below rated speed.
Matching every station to the same throughput target is the only way a line delivers what the nameplate promises.
I spent months on a Middle East project where the extruder pushed material faster than the multi-layer oven could dry it. Moisture remained trapped inside the granules, and the pulse grinder produced uneven particle size because the feed was still partially wet. The line never reached its stated capacity until we rebalanced the dryer residence time and grinder airflow to match the extruder feed rate [NEED_CITE: extrusion line throughput balancing principles]. This is the reality behind capacity figures quoted in isolation.
Station-by-Station Equipment Coverage
The MT75 Modified Starch Processing Line for sale encompasses nine distinct processing stages under one equipment specification: flour mixing, screw conveying, twin screw extrusion, air conveying, multi-layer drying, air conveying again, pulse grinding, storage silo feeding, and final mixing before packaging. Each station connects to the next through matched conveying systems, so material flow remains continuous without manual transfer points or interim buffering.
Frequency Conversion Across Critical Drive Points
Feeding, driving, and rotary cutting systems all operate under independent frequency conversion speed regulation. This means an operator can adjust the feed screw speed to match a denser cassava starch without altering the main screw RPM, maintaining consistent residence time inside the barrel. For processors switching between corn starch and tapioca starch on the same shift, this level of independent control prevents the texture variation that fixed-speed drives produce [NEED_CITE: twin screw extrusion process control for starch gelatinization].
Reading the Specifications That Actually Shape Output
The twin screw configuration matters fundamentally for modified starch because it provides the shear profile needed to break down native granule structure uniformly. Single screw designs struggle with the viscosity swings that occur as starch passes through its gelatinization window. The 180 kW installed power across the full line ensures adequate torque headroom when processing high-amylose corn starch, which demands substantially more mechanical energy input than standard cassava varieties. The pulse grinder operating at 100–120 mesh with a 15 kW drive motor and integrated dust removal handles the dried extrudate without generating excessive fines that would require re-processing. The multi-layer oven uses a double pitch roller chain transmission, which resists the stretching and jamming that single pitch chains experience under the sustained thermal load of continuous starch drying operations. The mixer options — 4 kW, 7.5 kW, or 15 kW with batch capacities from 20–30 kg up to 170–180 kg — let the front end scale to the extruder output without over-sizing or under-sizing the batching step.
The Cost of Overlooking Downstream Equipment
When a buyer focuses negotiation entirely on extruder specifications and treats the dryer and grinder as secondary, the consequences surface within the first week of production. Wet extrudate entering the grinder produces clumping, forces unplanned cleaning shutdowns, and accelerates impeller wear far beyond normal schedules. A dryer that is undersized relative to the extruder output forces operators to slow the entire line, leaving the most expensive machine in the plant running below capacity [NEED_CITE: downstream equipment sizing for extrusion lines]. These losses accumulate quietly and rarely appear in the original purchase comparison.
What Separates a Matched Line from Assembled Components
The complete station lineup from flour mixer through packaging machine comes from a single supplier, so throughput calculations are performed across every connection point rather than within isolated machines. Screw configuration and die design are specified to the buyer’s actual starch variety and target modification, not copied from a generic build. The in-house testing workshop runs trial production on the customer’s own raw material before shipment, so parameter adjustments happen in the factory rather than on the buyer’s floor during commissioning. CE-certified construction applies across the full line. Pre-sales engineering covers line layout and capacity calculation to confirm that every station can sustain the target output together [NEED_CITE: CE machinery directive compliance for food processing equipment].
Documentation & Verification
- Line layout and capacity calculation showing throughput balance across all nine stations
- Screw and die configuration record matched to your starch variety and modification target
- Trial run report on your specific raw material from the in-house testing workshop
- Electrical schematic with voltage and frequency confirmed for your local supply
- Factory test record documenting run parameters before shipment
- Operation and maintenance manual covering every station in the line
Installation, Commissioning & Support
- Floor space planning for the 32,000 × 3,500 × 4,300 mm footprint including conveyor clearance zones
- Dedicated electrical circuit provision for the 180 kW installed load with 380 V three-phase supply
- Sequential station assembly from mixer through packaging with alignment verification at each joint
- First-run parameter setting for screw speed, barrel temperature, and dryer chain speed on your starch type
- Operator training on frequency conversion controls across feeding, driving, and rotary cutting systems
- Wear parts list covering screws, dies, grinder impellers, and chain links with recommended stock quantities
Preparing Your Inquiry With the Right Details
To receive an accurate line configuration, specify the starch variety you intend to process — cassava, corn, potato, or tapioca — along with any chemical or physical modification target. Confirm your local voltage, frequency, and preferred control language. Share your daily production target and available workshop dimensions so the layout can account for the full station sequence and material flow paths.
Frequently Asked Questions
Q: How is output capacity verified for my specific starch raw material and moisture content?
A: Capacity figures are confirmed through a trial run in the testing workshop using your actual raw material. The twin screw extruder parameters — screw speed, barrel temperature, and feed rate — are recorded during this run, and the downstream dryer and grinder are adjusted to match. A formal trial run report documents the verified throughput under those specific conditions.
Q: What voltage and frequency options are available for my target market?
A: The mixer is configured at 380 V, 50 Hz, three-phase as standard, but the full line electrical system can be adapted to match your local supply. Voltage, frequency, and control panel language are confirmed during the specification stage before production begins, preventing commissioning delays caused by incompatible power systems.
Q: How is screw configuration selected for different starch types such as cassava versus corn?
A: Screw elements and die geometry are chosen based on the gelatinization temperature, amylose content, and viscosity profile of your specific starch. High-amylose corn starch requires a different shear and compression arrangement than cassava starch. This configuration is documented and tested during the pre-shipment trial run.
Q: Can individual stations be sized independently or must they be purchased as a complete line?
A: Each station — from the flour mixer with selectable 4 kW to 15 kW motors to the pulse grinder with adjustable 100–120 mesh — can be configured to match your existing equipment. However, throughput verification across all stations is most reliable when the full line is engineered together.
Q: What wear parts and spare components are available for the twin screw extruder and pulse grinder?
A: A wear parts list is supplied with every line, covering screws, dies, grinder impellers, air circulating fans, and roller chain links. These are the components most likely to need replacement during the first production cycle, and availability is confirmed before shipment so that your first changeover does not cause unplanned downtime.