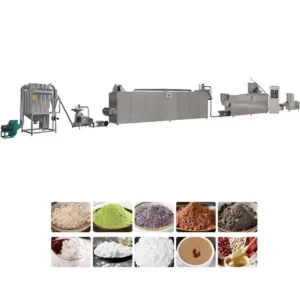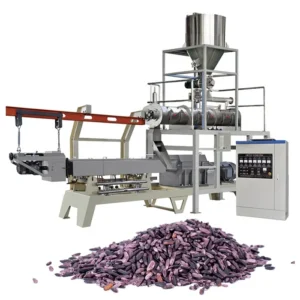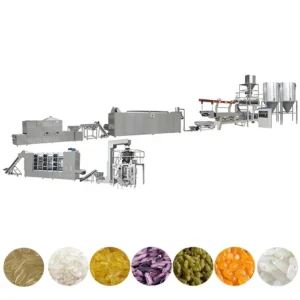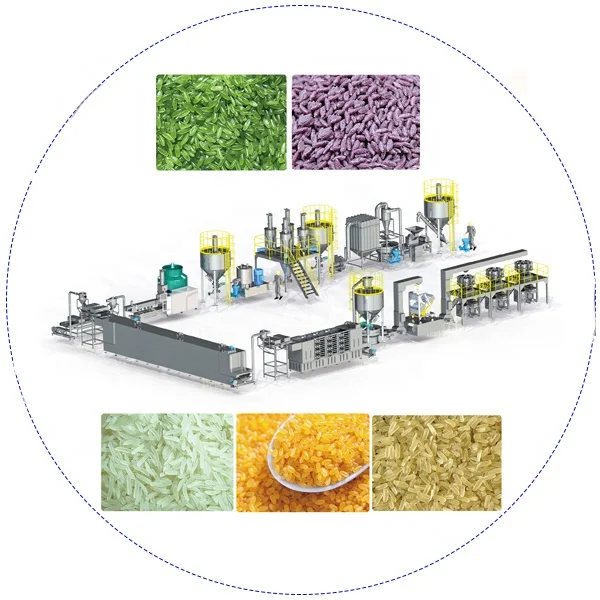
Throughput-matched station design — every mixer, dryer and cooler on this artificial rice extrusion line is sized against the extruder’s actual output curve, preventing the common bottleneck where downstream equipment chokes on upstream volume.
Technical Specifications
| Parameter | Value |
|---|---|
| Product Type | Artificial & Fortified Rice Extrusion Line |
| Line Output | 300–500 kg/h (basis not stated in source — confirm raw material formulation, moisture content & rice grain dimensions) |
| Extruder Type | Co-rotating twin-screw, sectional modules |
| Extruder Main Power | 110 kW (frequency control) |
| Feeder Power | 1.5 kW (frequency control) |
| Cutting Power | 2.2 kW (frequency control) |
| Screw Length | 2500 mm |
| Oil Pump Power | 0.75 kW |
| Mixer Power | 15 kW |
| Mixer Batch Capacity | 130–150 kg/batch (basis not stated in source — confirm bulk density of rice/corn flour blend) |
| Mixer Dimensions | 1450 × 1550 × 980 mm |
| Mixer Weight | approx. 200 kg |
| Mixing Tank Thickness | 1.5 mm |
| Stainless Steel Cover Thickness | 1.2 mm |
| Vibrating Screen Power | 0.2 kW |
| Vibrating Screen Dimensions | 1700 × 1210 × 740 mm |
| Dryer Heating Type | Electric (gas / diesel / steam options available on request) |
| Cooling Dryer Power | 2.2 kW |
| Cooling Dryer Dimensions | 5000 × 1500 × 1900 mm |
| Motor Brand | Siemens |
| Control System | Frequency control on main drives (PLC / MCC availability to be confirmed) |
| Certification | CE |
Application Suitability
| Application | Material or Output |
|---|---|
| Fortified rice production for nutrition programmes | Rice flour, corn flour, vitamin and mineral premix blends |
| Artificial rice grain manufacturing | Rice powder and corn powder reconstitution into uniform grains |
| Instant / quick-cooking rice formats | Pre-gelatinised starch blends requiring controlled expansion |
| Breakfast cereal grain additions | Extruded rice-based grains for multi-grain cereal lines |
Why "500 kg/h" Means Nothing Without the Full Material Picture
Capacity is only real when verified against your specific rice-flour formulation and target grain density.
I watched a buyer in East Africa commission an artificial rice extrusion line that was rated at a respectable hourly output on paper. Within two days the cooling belt was buried under warm, sticky grains because the dryer could not pull moisture down fast enough for the extruder’s actual throughput on his high-amylose rice blend [NEED_CITE: moisture migration rates in extruded rice products]. The extruder was never the problem — the downstream stations were undersized for his material. This fortified rice processing line equipment addresses that mismatch by specifying screw configuration, die geometry and dryer residence time against the buyer’s raw material before the build starts, not after it lands on the factory floor.
How Co-Rotating Twin-Screw Geometry Shapes the Grain
The co-rotating twin-screw extruder uses sectional screw modules that can be rearranged to control shear intensity and residence time across the 2500 mm barrel. For fortified rice, this means the starch gelatinisation window can be tuned so that vitamin and mineral premixes are incorporated without thermal degradation. The die plate at the discharge end forms the extrudate into rice-grain strands, which the frequency-controlled cutter slices to consistent length before the grains enter the vibrating screen.
Matching Dryer Residence Time to Extruder Output on the Fortified Rice Processing Line Equipment
The cooling dryer stretches 5000 mm in length, giving grains adequate belt travel to shed residual moisture after the heating zone. Electric heating is standard, with gas, diesel or steam options configurable for markets where electricity costs make thermal drying uneconomical [NEED_CITE: industrial drying energy costs by region]. A dedicated cooling stage follows, dropping grain temperature below the dew point threshold so that moisture does not re-condense during packing — a failure mode that turns a production run into a spoilage event.
Reading the Power and Drive Numbers Against Production Reality
The 110 kW main extruder drive with frequency control lets operators dial screw speed to match formulation changes — a high-fibre blend with added bran demands different shear than a pure rice-flour run. The 1.5 kW feeder, also on variable frequency, meters raw material into the barrel at a rate the screws can process without surging. The 15 kW mixer handles 130–150 kg batches with a 1.5 mm tank wall, thick enough to resist deformation under the cyclic loading of dense flour blends, while the 0.2 kW vibrating screen separates fines and oversized pieces before they reach the dryer belt.
What Happens When Stations Are Sourced From Separate Vendors
Buying the extruder from one supplier and the dryer from another is the fastest route to a line that cannot hold its quoted output. The dryer manufacturer rates his belt for a certain evaporation load; the extruder manufacturer rates his screws for a certain throughput. Nobody is responsible for the gap between those two numbers. I have seen artificial rice lines where the dryer was swapped twice before the owner accepted that the bottleneck was a system design failure, not a single bad machine [NEED_CITE: throughput matching in multi-vendor processing lines]. Sourcing the complete artificial rice extrusion line from one builder means every station — mixer, extruder, vibrating screen, dryer, cooler — is calculated against the same material balance sheet.
Why Buyers Source This Line From One Engineering Source
Screw configuration and die design are specified to the buyer’s actual rice-flour blend and target grain specification, not copied from a generic build. An in-house testing workshop runs the buyer’s raw material through the extruder before shipment, generating a trial report that confirms grain shape, density and cooking behaviour. Frequency-controlled drives across the feeder, extruder and cutter allow output adjustment without mechanical changeovers. The cooling dryer’s selectable heating source adapts to the destination market’s energy economics. Electrical schematics confirm voltage, frequency and control language to the buyer’s local standard before production begins, avoiding the commissioning delays that arise when a 380V machine arrives in a 415V facility.
Documentation & Verification
- Line layout and capacity calculation matched to your rice-flour formulation and grain dimensions
- Screw and die configuration record documenting module arrangement and die hole geometry
- Electrical schematic with destination voltage, frequency and control language confirmed before build
- Trial run report on your raw material verifying grain shape, density and cooking behaviour
- CE declaration of conformity covering the complete assembled line
- Wear parts list specifying screw segments, die plates and cutter blades with replacement intervals
Installation, Commissioning & Support
- Foundation plan accounts for the 5000 mm cooling dryer footprint and vibrating screen vibration isolation
- Dedicated circuit sized for the 110 kW extruder main drive plus auxiliary loads
- Machines ship in sectional modules for container loading and on-site assembly
- First-run parameter setting covers screw speed, feeder rate and dryer temperature for your formulation
- Operator training addresses frequency drive adjustment and cutter calibration procedures
- Spare screw segments and die plates included based on projected wear rate for rice-flour processing
What to Include With Your Inquiry
Provide your rice-flour blend composition and any vitamin or mineral premix ratios so the screw configuration can be specified before quotation. Confirm the destination facility’s voltage, frequency and preferred control-panel language to lock in the electrical design early. If you have existing upstream batching or downstream packing equipment, share the interface requirements so the line layout accounts for those connection points.
Frequently Asked Questions
Q: How is the line’s 300–500 kg/h output verified against my specific rice-flour formulation and grain size?
A: The output figure depends on your raw material’s bulk density, moisture content and target grain dimensions. Before build, we run your actual rice-flour blend through the extruder in our testing workshop and document the sustained throughput, grain density and shape in a trial report. This verified number — not the nominal range — becomes the basis for sizing every downstream station.
Q: What voltage, frequency and control-language options are confirmed before production starts?
A: We require your facility’s supply voltage, frequency and the preferred language for drive displays and control panels before the electrical design is locked. The schematic is shared for approval so that motor ratings, breaker sizing and label language match your local standard, preventing commissioning delays caused by mismatched electrical infrastructure.
Q: Can a trial run be performed on my raw material before shipment, and what does the trial report cover?
A: Yes. Your rice-flour blend is processed through the extruder with the specified screw and die configuration. The trial report records output rate, grain dimensions, density, moisture content after drying and cooking behaviour after rehydration. Any formulation adjustments needed to meet your product specification are documented before the line is released for shipment.
Q: How are the dryer and cooling stations sized to match extruder output and avoid line bottlenecks?
A: Dryer belt length, heating capacity and cooling zone dimensions are calculated from the extruder’s verified throughput on your material. The 5000 mm cooling dryer provides sufficient residence time to reduce grain moisture to packing-safe levels. The cooling stage then drops grain temperature below the condensation threshold, preventing moisture re-absorption that would compromise shelf stability.