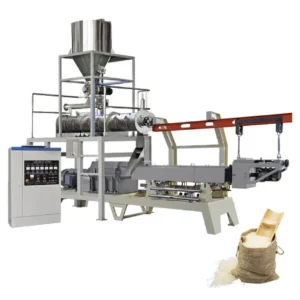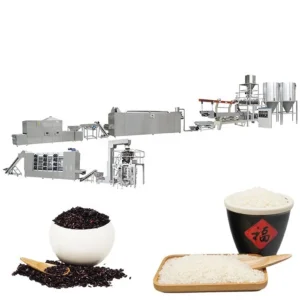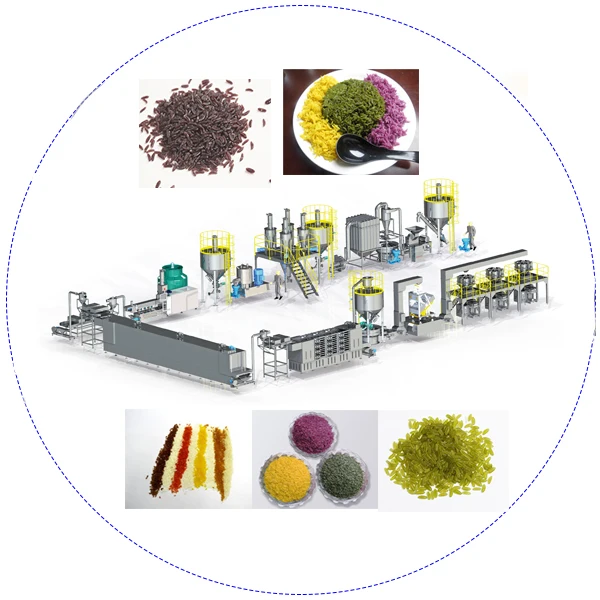
Matched Throughput Across Every Station — The artificial rice and fortified rice kernel production line balances extruder output with dryer, roaster, and packing capacity so no single station becomes a bottleneck during continuous operation.
Technical Specifications
| Parameter | Value |
|---|---|
| Model | MT65 / MT70 / MT85 / MT75 / MT95 |
| Product Type | Artificial Rice and Fortified Rice Kernel Extrusion Production Line |
| Installed Power | 85 kW (MT65) / 120 kW (MT70) / 180 kW (MT75) / 235 kW (MT85) / 260 kW (MT95) |
| Power Consumption | 60 kW (MT65) / 85 kW (MT70) / 135 kW (MT75) / 165 kW (MT85) / 195 kW (MT95) |
| Output Capacity | 80–100 kg/h (MT65) / 100–120 kg/h (MT70) / 300–500 kg/h (MT75) / 200–300 kg/h (MT85) / 800–1000 kg/h (MT95) (basis not stated in source — confirm raw material blend, moisture content and die configuration) |
| Overall Dimensions (L×W×H) | 28×1.2×2.2 m (MT65) / 30×1.5×2.2 m (MT70) / 32×3.5×4.3 m (MT75) / 34×3.5×4.3 m (MT85) / 36×3.5×4.3 m (MT95) |
| Screw Type | Twin-screw extruder |
| Feeding Option | Single-screw or twin-screw feeding depending on material |
| Control System | Frequency speed control, automated operation |
| Extruder Lubrication | Automatic lubrication and cooling system |
| Dryer Heating Source | Electric or gas |
| Line Stations | Mixing → Extruding → Vibrating → Low-temperature Drying → Cooling → High-temperature Roasting → Cooling → Packing |
| Standards | CE, ISO |
Application Suitability
| Application | Material or Output |
|---|---|
| Fortified rice kernels for nutrition programs | Broken rice, starch base blended with vitamins and minerals |
| Artificial rice from rice by-products | Broken rice, rice bran reconstituted into whole-grain-shaped kernels |
| Multi-grain nutritional rice | Corn, millet, wheat, oats, buckwheat, bean, starch blends |
| Micro-nutrient enriched rice | Cereal base with iron, zinc, vitamin A, folic acid, and B-complex additions |
Why "Rated Capacity" Means Nothing Without the Full Line Context
An extruder rated at 300 kg/h on one grain blend can drop to half that when moisture content or starch composition shifts, and a mismatched dryer downstream will choke the entire run.
Buyers sourcing an artificial rice extrusion machine often receive a quote based on a single extruder model running an ideal test material. When the actual raw material arrives at the factory — perhaps a local broken rice variety with higher bran content or a different starch gelatinisation temperature — the screw configuration and barrel temperature profile no longer match. The extruder pushes material faster than the dryer can handle, or slower than the packing station expects, and the entire line stalls. I have seen fortified rice projects in Southeast Asia lose two full production days because the dryer belt speed was fixed and could not accommodate the moisture load coming off the extruder. Specifying the nutritional rice processing equipment as a matched system rather than individual machines prevents these compounding failures [NEED_CITE: throughput matching principles in multi-station food processing lines].
Station-by-Station Throughput Alignment
Every station in this fortified rice kernel production line is specified to handle the volume delivered by the upstream extruder. The vibrating feeder distributes extrudate evenly onto the dryer belt, preventing clumping that would create uneven moisture removal. The low-temperature drying stage reduces surface moisture without case-hardening the kernels, and the subsequent high-temperature roasting stage develops the final texture and colour. Because the dryer uses a circulation process with adjustable mesh belt speed controlled by a frequency motor, operators can tune residence time to match the extruder output rate rather than forcing the extruder to slow down.
Dryer and Roaster Sizing Against Extruder Output
A common failure mode in nutritional rice processing equipment is undersized thermal stages. If the dryer cannot remove enough moisture before kernels reach the roaster, the roasting step produces cracked or hollow kernels instead of the dense, glossy grains that nutrition programs require. The line includes a dedicated cooling stage between drying and roasting, which stabilises kernel structure before the high-temperature pass. This sequencing matters especially when the raw material blend includes a high proportion of starch-rich components like corn or wheat, which release more bound water during extrusion and demand longer drying residence times [NEED_CITE: starch gelatinisation and moisture release during twin-screw extrusion].
Reading the Specification Sheet Beyond the Nameplate
The installed power figures across the model range — from 85 kW on the MT65 to 260 kW on the MT95 — reflect the mechanical energy available for screw rotation and barrel heating. However, actual power consumption runs lower: 60 kW for the MT65 and 195 kW for the MT95. The difference between installed and consumed power indicates the thermal and mechanical headroom available when processing higher-fibre or higher-protein blends that demand more torque. The twin-screw configuration provides positive conveying for sticky dough-like materials typical of fortified rice formulations, while the single-screw feeding option suits free-flowing dry blends. The automatic lubrication and cooling system on the extruder barrel reduces unplanned stops during extended production runs, which directly affects whether the stated capacity range is achievable over a full shift.
The Cost of Skipping Downstream Verification
When a buyer selects the extruder first and sources the dryer, roaster, and packing equipment separately, the interfaces between stations become the failure points. Belt widths may not match, transfer chutes may clog, and the packing scale may not cycle fast enough for the incoming kernel flow. These mismatches do not appear on any single machine’s specification sheet — they only surface during commissioning, when production schedules are already committed. Correcting them after installation means cutting and rewelding conveyors, rerouting electrical circuits, and reprogramming PLC sequences while the line sits idle. Buyers who have experienced this describe it as paying for the line twice [NEED_CITE: integration challenges in multi-vendor food processing installations].
What You Get From a Single-Source Line
The complete line from mixing through packing is engineered as one system, so the vibrating station, dryer belt width, roaster chamber length, and packing speed are all calculated against the same extruder output figure. Screw and die configurations are specified to the buyer’s actual raw material blend rather than copied from a generic build. An in-house testing workshop runs trial production on customer-supplied materials before shipment, generating a documented report that confirms output rate, kernel density, and drying parameters. The frequency speed control across stations allows operators to scale throughput up or down as a single coordinated adjustment rather than tuning each machine independently. Electrical schematics are prepared with the buyer’s local voltage and frequency confirmed before the control panels are wired [NEED_CITE: electrical standards for industrial food machinery by destination market].
Documentation & Verification
- Line layout showing throughput calculation between extruder, dryer, and packing stations
- Trial run report on customer raw material confirming kernel shape and density
- Screw and die configuration record matched to target rice kernel geometry
- Electrical schematic with voltage, frequency, and control language confirmed per destination market
- Factory test record documenting continuous run performance before dispatch
- CE declaration of conformity and ISO certificate for the complete line
Installation, Commissioning & Support
- Foundation and utility plan based on the selected model footprint, up to 36×3.5×4.3 m for the MT95
- Dedicated power circuit sizing to the line’s installed power, up to 260 kW on the largest configuration
- Dryer heating source configured as electric or gas per local utility availability
- Frequency speed control calibration across all stations during on-site commissioning
- Operator training covering screw configuration changes and die replacement procedures
- Wear parts list specifying screws, dies, and dryer belt sections with recommended replacement intervals
Before You Send the Inquiry
To receive a line configuration that matches your actual production conditions, prepare the following: your raw material formulation including base grains and fortification additives, target daily or hourly output in kilograms, available workshop floor area and ceiling height, and your local electrical supply voltage and frequency. If you are integrating this artificial rice extrusion machine into an existing facility, note any upstream milling or downstream bagging equipment already in place. Specify whether you require a trial run on your materials at the factory before shipment, and confirm the preferred language for the control interface and operation manuals.
Frequently Asked Questions
Q: How is the line capacity verified against my specific raw material blend?
A: The factory runs a trial production using your actual raw material formulation before shipment. This test confirms the achievable output rate, kernel density, and drying parameters on your specific blend of broken rice, starch, and fortification additives. The resulting trial run report documents these values and serves as the baseline for commissioning adjustments on site.
Q: Which stations are included, and how is throughput balanced between them?
A: The line covers mixing, extruding, vibrating, low-temperature drying, cooling, high-temperature roasting, a second cooling stage, and packing. Each station is sized to handle the extruder’s output so that no single stage creates a bottleneck. Dryer belt speed and roaster residence time are adjustable via frequency motors to match the upstream extrusion rate.
Q: What voltage and control language options are available?
A: Electrical schematics are prepared after confirming the destination market’s voltage and frequency standards. The control system uses frequency speed control with automated operation, and the interface language is specified during the quotation stage. This confirmation happens before the control panels are wired, avoiding costly rewiring during commissioning.
Q: Can I test my raw materials at the factory before the line ships?
A: Yes. The in-house testing workshop conducts trial runs on customer-supplied raw materials. This step validates the screw configuration, die selection, barrel temperature profile, and dryer settings against your target kernel specifications. You receive a documented report covering output rate, product density, and recommended operating parameters.
Q: What spare wear parts come with the line, and when should they be replaced?
A: The line ships with a wear parts list identifying screws, dies, and dryer belt sections subject to normal wear. Replacement intervals depend on production hours and raw material abrasiveness, which the trial run report helps estimate. Keeping critical spares on hand from the initial order avoids unplanned downtime when the first replacement becomes due.