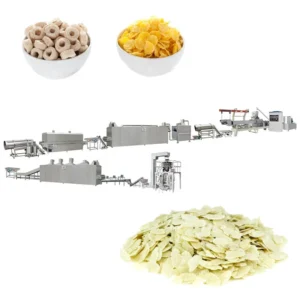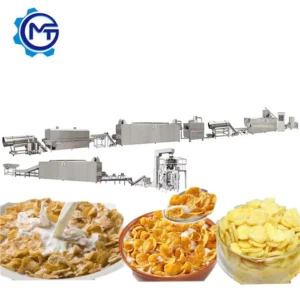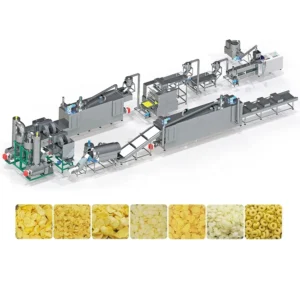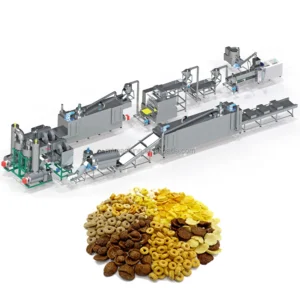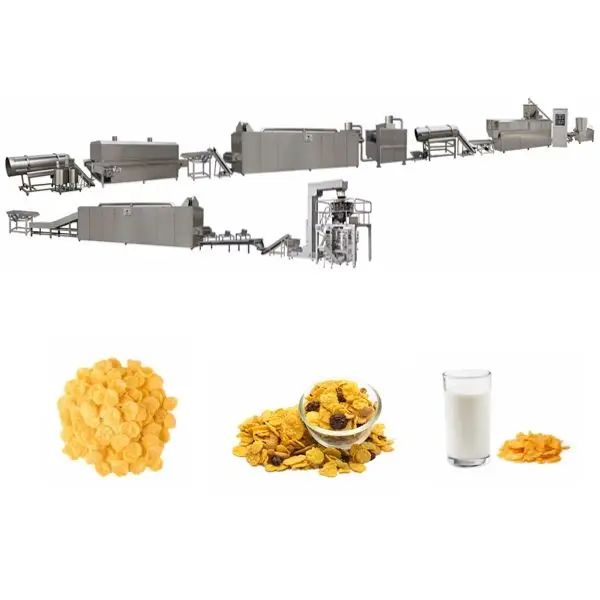
Line Capacity Matched Across Stations — Every mixer, flaker, dryer, and coater in this corn flakes production line is specified to hold the extruder’s output, so no single station throttles the rest of the line.
Technical Specifications
| Parameter | Value |
|---|---|
| Model | MT70 / MT85 / MT75 |
| Product Type | Corn Flakes Production Line |
| Extruder Type | Twin Screw |
| MT70 Installed Power | 160 kW |
| MT70 Power Consumption | 120 kW |
| MT70 Capacity | 150–200 kg/h (basis not stated in source) |
| MT70 Dimensions | 41 × 1.5 × 2.2 m |
| MT85 Installed Power | 190 kW |
| MT85 Power Consumption | 140 kW |
| MT85 Capacity | 300–400 kg/h (basis not stated in source) |
| MT85 Dimensions | 43 × 1.5 × 3.2 m |
| MT75 Installed Power | 210 kW |
| MT75 Power Consumption | 150 kW |
| MT75 Capacity | 300–500 kg/h (basis not stated in source) |
| MT75 Dimensions | 45 × 1.5 × 3.5 m |
| Flaking Machinery Control | PLC, hydraulic double-roller system, infrared sensor temperature control |
| Dryer Heating Source | Gas / Electric |
| Roasting Oven | Hot air roasting with vibrating pan, dual circulating fans, cyclone dust removal |
| Coating System | Double tumble for sugar melting, elevator, coating drum, spraying nozzle |
| Control System | PLC and MCC |
| Raw Materials | Corn, rice, wheat, oat, barley powder |
| Final Products | Natural and sugar-coated flakes, various extruded shapes |
| Standards | CE, ISO |
Application Suitability
| Application | Material or Output |
|---|---|
| Natural Corn Flake Production | Corn grits, processed through extrusion, flaking, drying and roasting |
| Sugar-Coated Cereal Manufacturing | Flaked corn or rice with sugar syrup spraying and tumble coating |
| Extruded Cereal Snack Shapes | Corn, wheat, oat or barley blends formed into rings, stars, balls, tubes |
| Multi-Grain Breakfast Cereal Lines | Blended rice, wheat, and oat flour bases for flaked or formed output |
Why the Extruder Model Is Only Half the Specification
An extruder quoted at a nominal capacity means nothing when the flaker, dryer and roaster downstream cannot keep pace. A complete corn flakes production line full equipment range must be sized station by station, not sold as a single throughput number on a brochure.
I have seen lines where a twin-screw extruder pushed material at a rate the dryer simply could not handle. The flakes piled up wet, stuck to the conveyor belts, and the whole operation shut down twice a shift for cleanup. That is not an extruder problem — it is a line design problem. Every piece of equipment in a breakfast cereal line introduces its own throughput ceiling, and the buyer who only asks about extruder output is leaving the real bottleneck undiscovered [NEED_CITE: line throughput matching in multi-station food processing].
From Mixing to Packing: Every Station in Sequence
A corn flakes production line begins at the batching and mixing station, where raw corn, rice, wheat, oat or barley powders are blended with water and minor ingredients before entering the extruder. The twin-screw extruder then gelatinises the starch under controlled temperature and shear, forcing the dough through a die to form a continuous sheet or shaped strand. The cutting system sections the extrudate before it moves into the flaking machinery, where hydraulic double rollers press the material into uniform flakes under PLC-controlled pressure and infrared temperature monitoring.
From flaking, the product enters the dryer, where excess moisture is drawn off using gas or electric heating. The hot air roasting oven follows, using a vibrating pan and high-temperature spraying tubes with two circulating fans to create the characteristic surface blister and crispness that defines a quality corn flake. Cyclone dust removal captures fine particles during roasting to maintain a clean production environment.
Sugar Coating and Downstream Finishing
For sugar-coated variants, the line routes flakes through the coating system: a double tumble unit melts the sugar, an elevator transfers the flakes, and a coating drum with a spraying nozzle applies an even syrup layer. The final stations cover cooling and packing. Each station in this corn flakes production line full equipment range connects directly to the next, and each must be configured with enough capacity to absorb what the station before it delivers [NEED_CITE: industrial cereal coating and finishing line configurations].
How Extruder Parameters Shape the Final Flake
The choice between MT70, MT85 and MT75 models sets the upper boundary for the entire line. The MT70 at 160 kW installed power suits smaller production runs, while the MT85 and MT75 at 190 kW and 210 kW respectively handle higher-volume output. Twin-screw extrusion allows these machines to process a wider range of raw materials — including higher-fat or higher-fibre blends with oat and barley — compared to single-screw designs, because the intermeshing screws self-clean and maintain more consistent shear across different formulations. The screw configuration and die design together determine how the starch gelatinises and how the extrudate behaves when it hits the flaking rollers. A die that produces too thick a sheet will result in flakes that crack rather than compress; too thin and the flakes tear during roasting.
The hydraulic double-roller flaking machinery uses infrared sensors to maintain consistent roller temperature, which directly controls flake thickness uniformity. Inconsistent thickness means some flakes over-roast while others remain doughy in the centre.
The Cost of Undersizing Downstream Stations
When a buyer selects an extruder without matching the dryer and roaster to its output, the consequences show up fast. Flakes exit the flaking rollers at a moisture level the dryer cannot reduce in a single pass, so the roaster receives a product that is still too wet to blister properly. The result is a flat, dense flake that does not meet the texture the market expects. I have walked into plants where the roaster was running at full fan speed and maximum burner output, yet the exit moisture was still too high because the upstream dryer was a size too small for the extruder feeding it. Those lines never reach stable production until the mismatch is corrected [NEED_CITE: moisture removal stages in cereal flake drying and roasting].
What Sets This Equipment Catalogue Apart
Every station in this corn flakes production line full equipment range is supplied from a single source, which means throughput calculations are done across all stations together rather than each vendor quoting independently. The screw configuration and die design are specified to the buyer’s actual raw material and target flake format, not copied from a generic build. An in-house machine testing workshop allows trial runs on customer-supplied raw materials before the line ships, so formulation adjustments happen at the factory, not on the buyer’s floor during commissioning. Twin-screw expertise spans breakfast cereals alongside pet food, aquatic feed and snack applications, which matters when buyers want to run oat-heavy or multi-grain blends that challenge simpler extruder designs. Pre-sales consultation covers line layout, and support extends through on-site installation, commissioning and ongoing maintenance.
Documentation & Verification
- Line layout drawing showing station sequence and throughput calculations for your selected capacity
- Machine specification sheet listing installed and consumed power for each station model
- Screw and die configuration record matched to your raw material blend and flake format
- Electrical schematic with voltage, frequency and control language confirmed for your market
- Trial run report on your supplied raw material documenting extrudate and flake quality
- CE declaration of conformity and ISO certificate for export documentation
Installation, Commissioning & Support
- Foundation plan accounting for the longest line configuration exceeding 45 metres in length
- Dedicated power circuit sized to the MT75 peak installed load of 210 kW where applicable
- Gas or electric dryer and roaster connections confirmed before site utilities are finalised
- PLC and MCC panel commissioning with operator language set before production trials begin
- Spare screw elements, die plates and flaking roller surfaces included for first replacement cycle
- Scheduled maintenance intervals for hydraulic flaking system and circulating fan bearings
Getting the Right Configuration for Your Project
To move from a general enquiry to a line layout that actually fits your facility, the most useful details you can provide early are your raw material formula and the target flake thickness or cereal shape. Share your available workshop dimensions including ceiling height, since the roasting oven and coating drum require vertical clearance that varies by model. Confirm your local voltage and frequency so the electrical schematic and PLC programming are correct from the start.
Frequently Asked Questions
Q: How is throughput matched between the extruder, flaker, dryer and roaster so no station bottlenecks the line?
A: Each station is sized based on the extruder model selected and the moisture reduction required at each stage. The dryer and roaster are specified to handle the mass flow exiting the flaking rollers at the target exit moisture, not just the dry product weight.
Q: What capacity range does each extruder model cover, and on what raw material basis?
A: The MT70, MT85 and MT75 cover three capacity tiers, but actual output depends on raw material composition, moisture content and target flake density. Capacity figures must be confirmed against your specific formula before the line is configured.
Q: Which heating source options are available for the dryer and roaster?
A: Both gas and electric heating are available. The choice affects utility planning, line layout dimensions, and operating cost in your market, and should be decided before the electrical schematic is drawn.
Q: Can individual stations be ordered separately to upgrade an existing line?
A: Individual stations can be supplied, but each must be evaluated against your current line throughput to confirm compatibility. A standalone flaker or coating drum needs to match the upstream feed rate to function correctly.
Q: What die and mould options produce different cereal shapes beyond standard corn flakes?
A: The extruder die can be changed to produce rings, balls, stars, tubes, wheels, and other formed shapes. The die configuration is selected based on your target shape and raw material, and is documented before production.