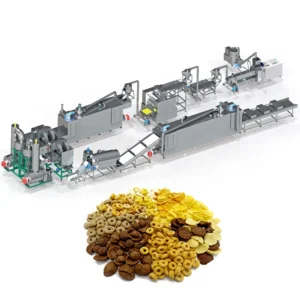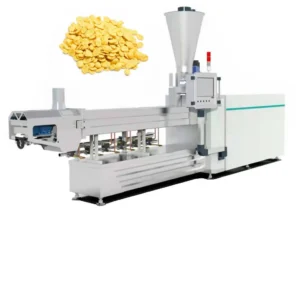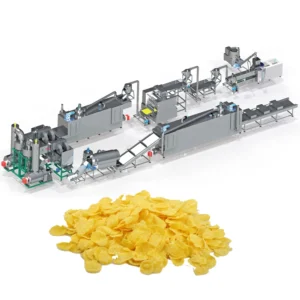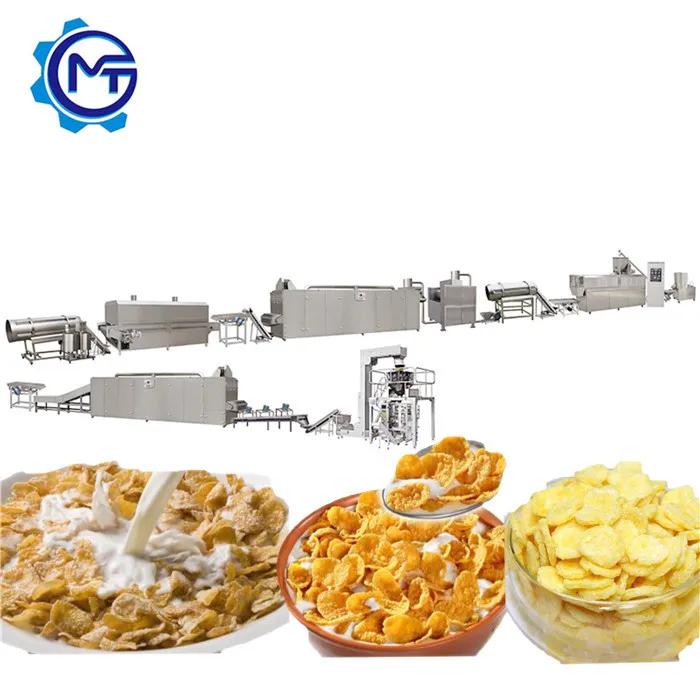
Coordinated Station Sizing — Throughput on every corn flakes processing node is calculated from the extruder forward, so flaking, drying, and roasting capacities hold under your actual grain formulation.
Technical Specifications
| Parameter | Value |
|---|---|
| Product Type | Corn Flakes Production Line |
| Model | MT70 / MT85 / MT75 |
| Screw Type | Twin-screw |
| Installed Power | MT70 — 160 kW; MT85 — 190 kW; MT75 — 210 kW |
| Power Consumption | MT70 — 120 kW; MT85 — 140 kW; MT75 — 150 kW |
| Output Capacity | MT70 — 150–200 kg/h; MT85 — 300–400 kg/h; MT75 — 300–500 kg/h (basis to be confirmed with buyer raw material and moisture content) |
| Overall Line Dimensions | MT70 — 41 × 1.5 × 2.2 m; MT85 — 43 × 1.5 × 3.2 m; MT75 — 45 × 1.5 × 3.5 m |
| Flaking Machinery Drive | Double motors for separate roller driving; hydraulic system |
| Flaking Temperature Control | Infrared sensor for even temperature pipe control |
| Control System | PLC control with MCC integration |
| Dryer Heating Source | Gas or Electric |
| Hot Air Roasting Oven | Conciliation burner; two circulating fans; cyclone dust removal; vibrating pan with high-temperature spraying tubes |
| Coating System | Double tumble sugar melting; elevator; coating drum; spraying nozzle |
| Screw Material | Special technology alloy |
| Lubrication | Automatic lubricating and cooling function |
| Standards | CE; ISO |
Application Suitability
| Application | Material or Output |
|---|---|
| Natural corn flakes production | Corn powder, corn grits |
| Sugar-coated corn flakes | Corn or rice base with sugar syrup coating |
| Multi-grain breakfast cereals | Blends of wheat, oat, barley, rice powder |
| Shaped cereal snacks | Ball, tube, stick, ring, fruit loop, star, wheel, flower, heart formats via die change |
Why Capacity Figures Mean Nothing Without a Raw Material Basis
Every throughput number on a corn flakes production line equipment sheet must be tied to a specific grain type, particle size, and moisture percentage — or it is not a number you can plan a factory around.
I learned this the hard way when a buyer in the Middle East signed for a line quoted at a given capacity, only to discover their local corn grits were coarser than what we used during testing. The extruder ran fine, but actual throughput fell well short and the dryer choked on excess moisture. That gap between brochure figures and workshop reality is where most breakfast cereal processing line manufacturer disputes start [NEED_CITE: common causes of throughput disputes in food extrusion contracts]. When stations are sourced from separate vendors, nobody owns the mismatch between the extruder output and the flaking roller intake rate.
Every Station Sized From the Extruder Forward
A corn flakes production line equipment package only performs when each downstream station can absorb what the extruder delivers at peak screw speed. On the MT70 / MT85 / MT75 range, the flaking machinery, dryer belt length, roasting oven volume, and coating drum diameter are each scaled to the chosen extruder model. This means a buyer selecting the MT85 for higher output receives proportionally wider flaking rollers and a longer dryer, not the same downstream hardware used on the smaller MT70.
How the Flaking and Roasting Sections Shape the Final Product
Flaking is where corn flakes production line equipment earns its name — the hydraulic double-roller system presses extruded pellets into thin sheets, and the infrared sensor holds roller temperature even across the full width. Downstream, the hot air roasting oven uses a conciliation burner with two circulating fans to create the characteristic surface bubbles that give corn flakes their crispness. The cyclone dust removal device keeps fine particle buildup out of the air stream, maintaining consistent heat transfer throughout a production run [NEED_CITE: role of roasting profile in breakfast cereal texture development].
Reading the Spec Sheet Like a Process Engineer
Twin-screw extrusion is chosen here because corn, wheat, and oat blends vary widely in starch and fiber content; the intermeshing screws provide the shear and mixing uniformity that a single-screw design struggles to maintain across different grain recipes. Installed power ranges from 160 kW on the MT70 to 210 kW on the MT75, reflecting the higher torque needed to push denser multi-grain formulations through the barrel. The automatic lubricating and cooling function on the screw shaft extends service intervals under continuous operation. PLC control with MCC integration lets operators store recipes for each cereal format, so switching from natural corn flakes to sugar-coated runs requires parameter recall rather than manual recalibration across the breakfast cereal processing line manufacturer offering.
The Hidden Cost of Mismatched Downstream Equipment
When a roasting oven is undersized relative to extruder output, flakes exit the dryer still holding too much moisture and enter the roaster in a semi-plastic state, resulting in flat, dense product rather than the blistered, crisp texture the market expects. A coating drum that cannot keep pace forces operators to slow the entire corn flakes production line equipment back to the drum’s limit, leaving the extruder idling below its rated screw speed and burning energy on partial loads [NEED_CITE: bottleneck effects in multi-stage food processing lines]. These mismatches rarely appear until the first full-speed production run, well after the equipment has been installed and paid for.
Why Sourcing the Full Range From One Supplier Matters
Every station on this corn flakes production line equipment range comes from a single manufacturing source, so throughput calculations are done once and applied across the entire layout rather than reconciled between unrelated vendors. The flaking machinery, roasting oven, and coating system are designed to connect mechanically and communicate through the same PLC architecture, eliminating the signal-conversion issues that arise when control systems from different factories meet on one floor. Screw configuration and die design are specified to the buyer’s grain formulation before the extruder is built, and the in-house testing workshop runs the actual raw material to confirm flake density and coating adhesion before any station ships.
Documentation & Verification
- Line layout drawing with throughput matching calculation for each station
- Screw and die configuration record matched to your grain type and target flake thickness
- Electrical schematic confirming voltage, frequency, and PLC language for your market
- Trial run report on your raw material showing actual output and flake density
- Factory test record covering extruder, flaking, roasting, and coating in sequence
Installation, Commissioning & Support
- Foundation plan accounts for the 41–45 m line length and vibration isolation at the flaking rollers
- Power supply must support up to 210 kW installed load with dedicated circuits for the roaster burner
- PLC and MCC panels arrive pre-wired; on-site connection limited to field sensors and motor feeds
- First-run commissioning includes recipe tuning for your grain blend across extruder and roaster
- Operator training covers die changes for shaped cereal formats and hydraulic roller gap adjustment
- Wear parts list identifies screw segments, flaking roller surfaces, and spraying nozzles for reorder
What to Include With Your Inquiry
To match the right extruder model and downstream configuration, share your primary grain type and particle size, the target hourly output you plan to run, and your workshop ceiling height and available line length. Specify your local voltage and frequency, preferred PLC language, and whether you need natural flakes, sugar-coated flakes, or both. If you already operate upstream milling or downstream packing equipment, include the interface dimensions so the corn flakes production line equipment layout can tie in without gap sections.
Frequently Asked Questions
Q: How is throughput matched across stations, and what raw material basis is used?
A: Each station — extruder, flaking machinery, dryer, roasting oven, coating drum — is sized from the extruder’s verified output on your specific grain blend and moisture level. We run your raw material in the testing workshop and record actual throughput before finalizing the downstream equipment specification, so quoted figures reflect your product rather than a generic benchmark.
Q: Can I order individual stations to upgrade an existing cereal line?
A: Yes. The flaking machinery, hot air roasting oven, and sugar coating system are each available as standalone units. We request the throughput and control specifications of your current line to ensure mechanical and electrical compatibility, and we supply interface drawings before manufacturing begins.
Q: What voltage and control language options are available?
A: The PLC and MCC panels are configured to your site’s voltage, frequency, and preferred operator language before shipment. Electrical schematics are confirmed during the order stage so that no rewiring or reprogramming is needed at commissioning.
Q: How is the flaking roller gap adjusted for different flake thicknesses?
A: The hydraulic system on the flaking machinery allows roller gap and pressure adjustment from the PLC screen. Infrared sensors monitor roller temperature across the full width to keep flake thickness consistent when switching between corn, wheat, or multi-grain recipes.
Q: What spare wear parts should I plan for?
A: The wear parts list included with each line identifies screw segments, die plates, flaking roller surfaces, and spraying nozzles. We recommend ordering a first replacement set before startup so that parts are on hand when the initial service interval arrives, avoiding unplanned downtime.