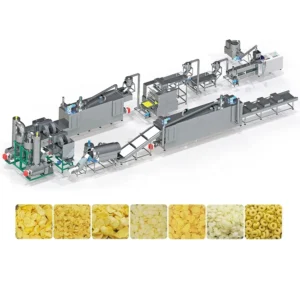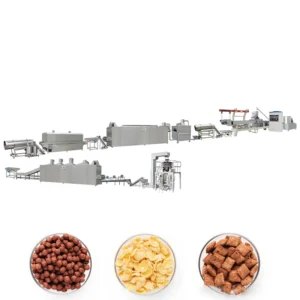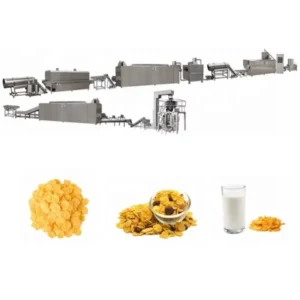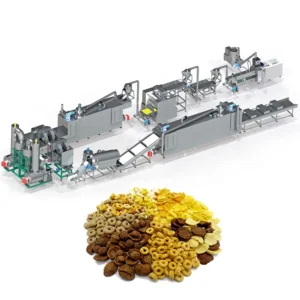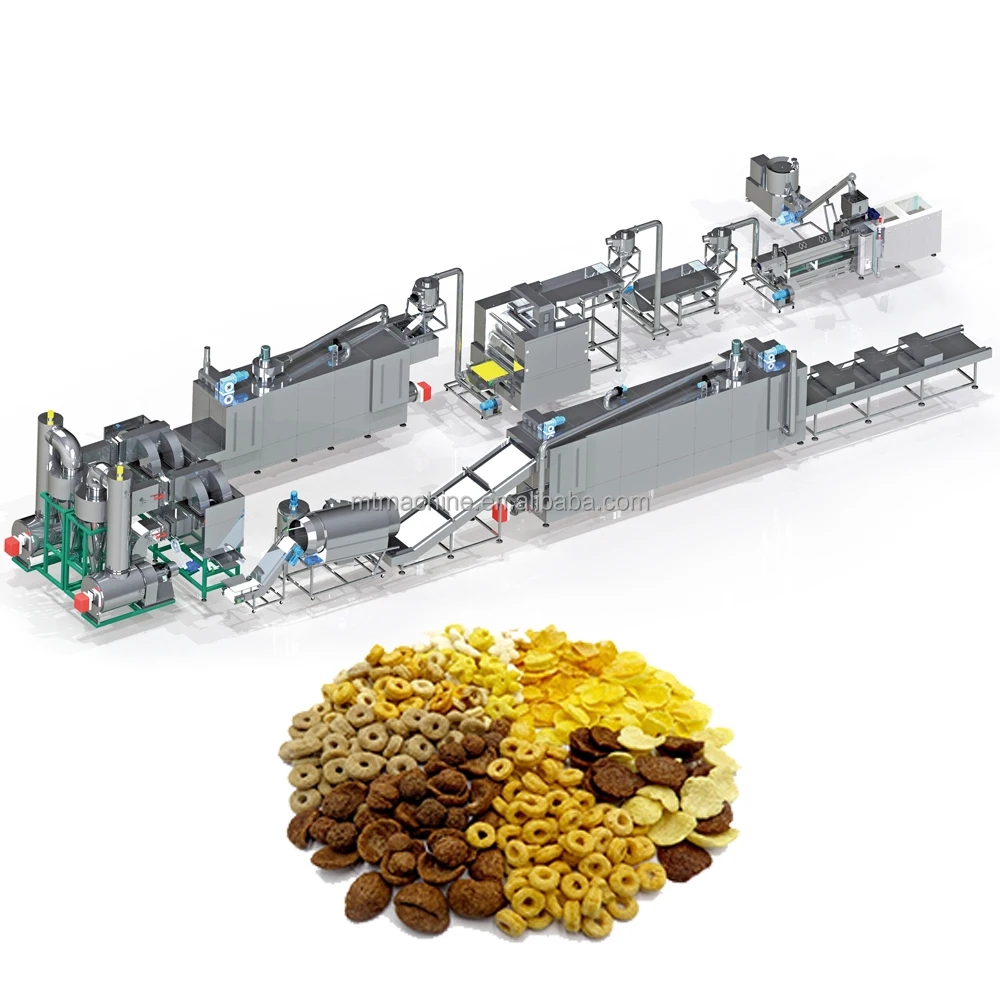
Complete Station Matching — every extruder, flaker, dryer, roaster, and coating drum is sized to the same throughput baseline so the line runs without bottlenecks from mismatched vendor equipment.
Technical Specifications
| Parameter | Value |
|---|---|
| Product Type | Corn Flakes Breakfast Cereal Production Line |
| Model Options | MT70 / MT85 / MT75 |
| Installed Power | 160 kW (MT70); 190 kW (MT85); 210 kW (MT75) |
| Power Consumption | 120 kW (MT70); 140 kW (MT85); 150 kW (MT75) |
| Output Capacity | 150–200 kg/hr (MT70); 300–400 kg/hr (MT85); 300–500 kg/hr (MT75) (basis not stated in source — confirm raw material, moisture content, and product format) |
| Overall Dimensions (L×W×H) | 41 × 1.5 × 2.2 m (MT70); 43 × 1.5 × 3.2 m (MT85); 45 × 1.5 × 3.5 m (MT75) |
| Extruder Type | Twin-screw |
| Screw Feature | Automatic lubricating and cooling function; wear-resistant construction |
| Control System | PLC control on flaking machinery; line-wide MCC/PLC available |
| Flaking Machinery | Hydraulic double-roller system; dual-motor independent drive; infrared sensor temperature control |
| Dryer Heating Source | Gas or Electric |
| Roasting Oven | Hot air roasting with vibrating pan; high-temperature spraying tubes; two separate circulating fans; cyclone dust removal |
| Coating System | Double tumble for sugar melting; elevator; coating drum; spraying nozzle |
| Line Stations (Natural) | Mixing → Extruding → Flaking → Drying → Hot Air Roasting → Cooling → Packing |
| Line Stations (Sugar-Coated) | Natural line + Sugar Spraying → Sugar Coating → Drying |
| Raw Materials | Corn, rice, wheat, oat, barley powder |
| Final Product Shapes | Ball, tube, stick, ring, fruit loop, star, wheel, flower, heart (by adjusting extruder mould) |
| Voltage & Frequency | Customized to local voltage |
| Standards | CE certified; ISO certified |
Application Suitability
| Application | Material or Output |
|---|---|
| Natural corn flakes production | Corn grits and corn flour, processed through extrusion, flaking, and roasting |
| Sugar-coated and honey-coated cereal flakes | Corn, rice, or wheat base with downstream sugar or honey tumbling |
| Shaped breakfast cereal snacks | Rings, balls, loops, stars, and wheels from corn, rice, oat, or barley blends via mould changes |
| Multi-grain and fortified cereal lines | Wheat, oat, and barley powder blends requiring adjusted screw configuration and moisture profiling |
What "300 kg/hr" Actually Means for Your Breakfast Cereal Line
A rated capacity is only valid on the exact raw material and moisture level used during testing.
I spent years running trial batches in a testing workshop before moving to line configuration. One client ordered a breakfast cereal production line full equipment range based on a brochure capacity figure. We ran standard corn grits during the factory test and everything held steady. When they started up on-site with a high-fibre whole-grain blend, the extruder could not maintain the same throughput, the flakes cracked during pressing, and commissioning took two extra weeks. Every corn flakes machine for sale carries a capacity number, but that number shifts depending on your recipe, particle size, and moisture content. Always ask which material was used when the output was measured [NEED_CITE: industrial extrusion capacity testing standards].
How Twin-Screw Design Handles Variable Cereal Grains
The twin-screw extruder in this corn flakes machine for sale platform uses an automatic lubricating and cooling function across the screw assembly, which keeps barrel temperatures stable during continuous runs. When you switch from corn to an oat-heavy blend, the shear profile inside the barrel changes, and consistent barrel cooling prevents localized overheating that would scorch the starch. Wear-resistant screw construction means the flight geometry holds its profile longer between replacements, so the gelatinisation window does not drift after a few hundred hours of operation.
Matching Dryer and Roaster Capacity to the Extruder
A common failure in breakfast cereal lines is an extruder that pushes material faster than the downstream dryer can handle, causing moisture to remain trapped inside the flake and producing a chewy rather than crispy texture. The hot air roasting oven on this line uses two separate circulating fans and a cyclone dust removal device to maintain uniform temperature distribution across the vibrating pan. The infrared sensor temperature control on the flaking machinery keeps roller surface heat within a tight band, which directly affects how evenly the sheet compresses before it enters the dryer. This station-level coordination is what separates a line that runs at its nameplate rate from one that constantly trips upstream [NEED_CITE: thermal processing uniformity in cereal manufacturing].
Reading the Specs That Actually Matter
Installed power across the MT70, MT85, and MT75 models ranges from 160 kW to 210 kW, and power consumption sits roughly 25% below installed capacity, which is typical for twin-screw extrusion systems where the motor peaks during startup and torque surges. The overall line length stretches from 41 m to 45 m depending on model, so your floor plan needs to account for the full run including the coating drum and cooling conveyor before the packing station. The hydraulic double-roller flaking system uses dual motors driving each roller independently, which allows you to set different surface speeds if the flake recipe requires a stretching action rather than pure compression. Gas or electric dryer heating options affect both your utility planning and operating cost, so confirm local fuel pricing before locking in the configuration. The PLC control on the flaking machinery can integrate with a line-wide MCC panel so one operator monitors the entire sequence from a single HMI.
The Hidden Cost of Skipping Station-Level Verification
I have seen buyers focus entirely on the extruder model and assume the rest of the line will simply follow. When the coating drum is undersized relative to the extruder output, sugar-coated flakes pile up waiting for the tumble cycle, and the syrup crystallises unevenly on the surface. When the roasting oven lacks sufficient air circulation capacity, the characteristic surface bubbles that define a quality corn flake fail to form, and the product looks flat and dense on the shelf. These mismatches do not show up in a quotation spreadsheet; they appear three weeks into production when the client cannot hit their target pack weight [NEED_CITE: downstream bottleneck effects in continuous food processing lines].
Why Source the Full Range from One Equipment Supplier
The complete breakfast cereal production line full equipment range is configured under one supplier, so throughput calculations run across every station rather than stopping at the extruder discharge. Screw configuration and die design are specified to your raw material and target flake thickness, not copied from a generic build that worked for a different grain. An in-house testing workshop allows trial runs on your actual recipe before the line ships, catching gelatinisation and flaking issues in the factory rather than on your floor. Twin-screw expertise covers corn, rice, wheat, oat, and barley applications, so recipe transitions are planned into the screw profile from the start. Pre-sales consultation extends through engineer layout design, on-site installation, commissioning, and operator training so the line is not simply delivered and abandoned.
Documentation & Verification
- Line layout and capacity calculation showing throughput at each station for your specific cereal grain
- Machine specification sheet per station with motor power, heating source, and dimensions
- Screw and die configuration record matched to your target flake shape and raw material blend
- Electrical schematic and voltage confirmation document signed off before production begins
- Trial run report on your raw material documenting flake texture, thickness, and moisture readings
- Factory test record with packing photographs and customs documentation support
Installation, Commissioning & Support
- Floor plan review against the 41–45 m line length and 1.5 m width to confirm utility routing
- Electrical panel setup for line-wide PLC and MCC control matching your local voltage and frequency
- Flaking machinery hydraulic system commissioning with roller gap calibration for target flake thickness
- Hot air roasting oven burner adjustment and circulating fan balancing during first production run
- Operator training on screw configuration changes for switching between corn, wheat, and oat recipes
- Wear parts list covering screws, dies, and roller surfaces with recommended replacement intervals
What to Prepare Before Requesting a Quotation
Send your raw material recipe with exact grain ratios and particle size distribution so the screw configuration can be matched before quoting. Confirm your local voltage, frequency, and whether you need gas or electric heating for the dryer and roaster. Provide your factory floor dimensions including ceiling height, since the MT85 and MT75 models reach over 3 m at the highest station. If you plan to run both natural and sugar-coated flakes, specify your target split between the two so the coating drum and secondary dryer are sized correctly from the start.
Frequently Asked Questions
Q: How do I match dryer and coating capacity to the extruder’s actual throughput on my raw material?
A: Provide your exact grain blend, moisture content, and target flake weight per square centimetre. The line layout calculation then sizes the dryer belt length and roaster residence time to handle the extruder’s real output on that material, not a generic corn grits baseline. This prevents moisture entrapment and uneven sugar crystallisation downstream.
Q: What voltage, frequency, and control language options are confirmed before production?
A: Voltage and frequency are customised to your local grid supply and confirmed in the electrical schematic document before production starts. The PLC and MCC control system language is set to your operator preference at the same stage. This avoids commissioning delays caused by mismatched motor ratings or unreadable HMI screens on arrival.
Q: Which extruder model fits my target capacity and factory footprint?
A: The MT70 suits lower throughput ranges with a 41 m line length, the MT85 covers mid-range output at 43 m, and the MT75 handles higher volumes at 45 m. Selection depends on your confirmed raw material test results and available floor space. Each model has different installed power and ceiling height requirements to verify against your building.
Q: Can I produce multiple breakfast cereal shapes on the same line?
A: Yes. The extruder accepts different moulds to produce balls, tubes, sticks, rings, fruit loops, stars, wheels, flowers, and heart shapes from the same twin-screw platform. Changing the mould is a mechanical swap at the die plate. The flaking station is bypassed for shaped products, and the downstream drying and roasting parameters are adjusted accordingly.
Q: Is a trial run on my raw material available before shipment?
A: The in-house testing workshop runs your actual grain blend through the extruder and flaking machinery before the line ships. This trial documents flake thickness, expansion behaviour, and surface texture, and any screw or die adjustments needed are made at the factory. You receive the trial run report with your shipment documentation.