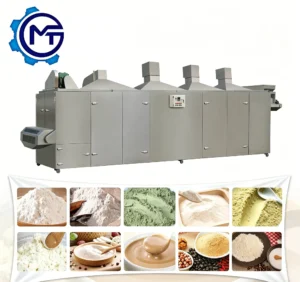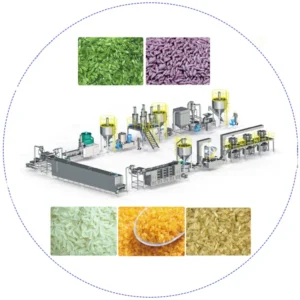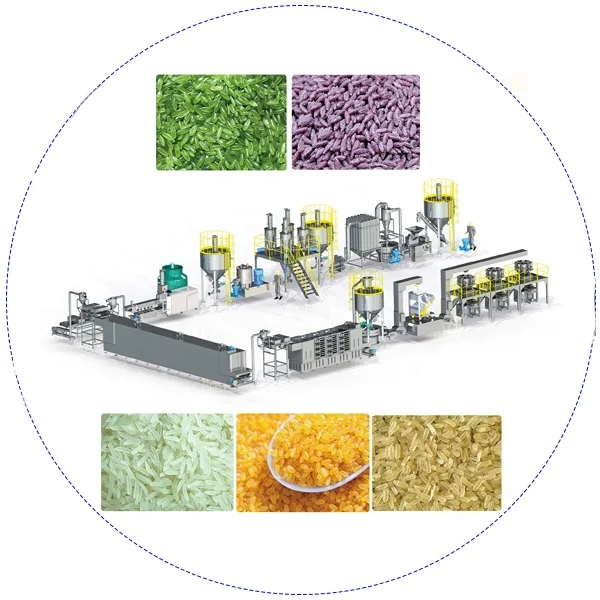
Screw and die configuration specified to your raw material — we match barrel profile, screw pitch, and die geometry to your grain formulation and target kernel shape before the line ships.
Technical Specifications
| Parameter | Value |
|---|---|
| Model | MT65, MT70, MT85, MT75, MT95 |
| Product Type | Fortified Rice Processing Line |
| Screw Type | Twin screw |
| Installed Power (MT65) | 85 kW |
| Power Consumption (MT65) | 60 kW |
| Output Capacity (MT65) | 80–100 kg/hr (basis not stated in source — confirm raw material formulation / moisture) |
| Overall Dimensions (MT65) | 28 × 1.2 × 2.2 m |
| Installed Power (MT70) | 120 kW |
| Power Consumption (MT70) | 85 kW |
| Output Capacity (MT70) | 100–120 kg/hr (basis not stated in source — confirm raw material formulation / moisture) |
| Overall Dimensions (MT70) | 30 × 1.5 × 2.2 m |
| Installed Power (MT85) | 235 kW |
| Power Consumption (MT85) | 165 kW |
| Output Capacity (MT85) | 200–300 kg/hr (basis not stated in source — confirm raw material formulation / moisture) |
| Overall Dimensions (MT85) | 34 × 3.5 × 4.3 m |
| Installed Power (MT75) | 180 kW |
| Power Consumption (MT75) | 135 kW |
| Output Capacity (MT75) | 300–500 kg/hr (basis not stated in source — confirm raw material formulation / moisture) |
| Overall Dimensions (MT75) | 32 × 3.5 × 4.3 m |
| Installed Power (MT95) | 260 kW |
| Power Consumption (MT95) | 195 kW |
| Output Capacity (MT95) | 800–1000 kg/hr (basis not stated in source — confirm raw material formulation / moisture) |
| Overall Dimensions (MT95) | 36 × 3.5 × 4.3 m |
| Control System | Frequency speed control with high automation (PLC or MCC available on request) |
| Screw Construction | Wear-resistant alloy with special surface treatment |
| Feeding System | Single or double screw feeding, selected by material characteristics |
| Lubrication | Automatic lubricating and cooling system |
| Drying Oven Heating Source | Electric or gas |
| Drying Oven Control | Frequency motor-controlled mesh belt speed |
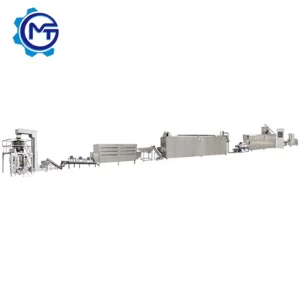
| Line Stations | Mixing → Extruding → Vibrating → Low-temperature drying → Cooling → High-temperature roasting → Cooling → Packing |
| Certification | CE, ISO |
Application Suitability
| Application | Material or Output |
|---|---|
| Fortified rice kernel production | Broken rice, rice flour blended with vitamins and minerals |
| Artificial rice manufacturing | Corn, millet, wheat, oats, buckwheat, bean, and starch bases |
| Nutritional rice for food aid programs | Grain-based formulations with added micronutrients |
| Reconstituted rice from grain by-products | Broken rice and milled grain fractions with supplemental starch |
Why Rated Capacity Means Nothing Without the Formulation
A Fortified Rice Processing Line only holds its nameplate output when the screw configuration matches the buyer’s actual grain blend and micronutrient ratio.
I have watched a buyer invest in a line quoted at full rated throughput, only to discover their multigrain formulation with a heavy bean and buckwheat ratio demanded a completely different screw pitch and barrel temperature profile. The extruder could not gelatinize the starch properly, throughput fell to a fraction of the quoted figure, and every downstream station — dryer, cooler, packing — ran empty for half each shift. The dryer was oversized for the reduced flow, wasting energy, while the packing station sat idle. [NEED_CITE: impact of raw material formulation on twin-screw extruder throughput]
This is why the Fortified Rice Processing Line full equipment range starts with a raw material trial, not a brochure number.
Matching Every Station to the Extruder Output
The Fortified Rice Processing Line full equipment range covers five twin-screw extruder models spanning 80 to 1000 kg/hr. Each model pairs with a drying oven, cooling conveyor, and packing station sized to the extruder’s actual throughput envelope. When the extruder model changes, the dryer belt width, cooling conveyor length, and roasting chamber volume change with it. This station-to-station matching prevents the common bottleneck where one segment of the line runs at capacity while another chokes or idles.
Drying Profile and Kernel Integrity
Fortified rice kernels exit the extruder at high moisture and must be dried in stages. The low-temperature drying station removes surface moisture without cracking the kernel surface, while the high-temperature roasting stage sets the final moisture content and develops the natural rice-like texture. The frequency-controlled mesh belt speed in the drying oven lets operators adjust residence time to match the kernel size and formulation density. [NEED_CITE: staged drying process for extruded rice kernel moisture control] Getting this sequence wrong — rushing through a single high-heat zone — causes surface checking and kernel breakage during packing and transport.
Reading the Power and Dimension Data Across the Model Range
The gap between installed power and actual power consumption on each model reflects motor startup loads, heater elements in the drying oven, and auxiliary drives for the feeding and conveying systems. On the MT65, the 25 kW gap between installed and consumed power is typical for a small-format line with an electrically heated dryer. On the MT85 and larger models, the gap widens because the drying oven and roasting chamber carry additional heating elements and circulation fans. The overall dimensions scale with capacity, but note that the MT75 and MT85 share the same cross-section width and height — the extra capacity comes from barrel length and screw configuration rather than a wider frame. This matters for workshop layout: if you plan to add a second line later, the floor space envelope per line stays comparable across those two models.
What Happens When Supporting Stations Are Undersized
An extruder running at capacity means little when the dryer cannot keep up. Kernels pile up on the conveyor, moisture content stays too high, and the packing station receives product that will mold in the bag within days. Similarly, if the cooling station is too short, warm kernels enter the packing bag and create condensation. These failures do not show up during a short factory test — they emerge over the first full production week. [NEED_CITE: consequences of mismatched drying capacity in extruded food lines] Sizing every station against the extruder’s confirmed output on your formulation eliminates this class of failure.
Why Source the Full Range from One Supplier
Every station in the Fortified Rice Processing Line full equipment range — mixer, feeder, extruder, vibrating screen, dryer, cooler, roaster, and packer — is specified as a matched set rather than assembled from separate vendors. The screw and die configuration is documented against your raw material before production begins. An in-house testing workshop runs your actual formulation through the extruder before the line ships, so you see kernel shape, density, and texture before committing to container loading. Electrical schematics and voltage confirmation are finalized for your target market before the control cabinets are wired. CE and ISO documentation ships with the line, and a wear parts list covers screws, dies, and dryer belt segments for your first replacement cycle.
Documentation & Verification
- Line layout drawing showing throughput matching across every station from mixer to packer
- Screw and die configuration record matched to your grain blend and target kernel shape
- Electrical schematic with voltage and frequency confirmed for your local supply standard
- Trial run report on your raw material formulation from the in-house testing workshop
- Factory test record covering all stations running together before dispatch
- Operation and maintenance manual with wear parts list for screws, dies, and mesh belt
Installation, Commissioning & Support
- Foundation plan accounts for the MT85 footprint of 34 × 3.5 m and dryer vibration isolation
- Dedicated power circuit sized to the installed power of your selected model, up to 260 kW on the MT95
- Frequency-controlled drives on feeding, extruder, and dryer belt calibrated during on-site commissioning
- First production run supervised to set barrel temperature profile and drying residence time
- Operator training covers screw changeover, die replacement, and automatic lubrication system checks
- Spare screws and dies shipped with the line based on the wear parts list for your configuration
What to Include in Your Inquiry
To configure the right Fortified Rice Processing Line from this equipment range, share your raw material formulation — including the grain base, starch ratio, and micronutrient blend — along with your target hourly output and kernel dimensions. Specify your local voltage, frequency, and preferred control language. If you have an existing packing system or upstream milling equipment, note the interface points so the line layout accounts for them.
Frequently Asked Questions
Q: How do I choose between the MT65, MT70, MT85, MT75, and MT95 for my target capacity?
A: Each model covers a different output envelope. The right selection depends on your confirmed throughput on your actual formulation, not the nameplate range. We run your raw material in the testing workshop to verify which model holds your target output, then size the dryer and downstream stations to match.
Q: What supporting stations are included beyond the extruder itself?
A: The line includes a mixer, single or double screw feeder, vibrating separator, low-temperature dryer, cooling conveyor, high-temperature roasting chamber, second cooling stage, and packing station. Each station is sized to the extruder model you select so throughput stays balanced end to end.
Q: How does the drying oven heating source choice affect my line layout?
A: Electric heating requires higher installed power capacity at your facility, while gas heating shifts the utility requirement to a gas supply line and exhaust ventilation. The choice affects both the electrical schematic and the workshop utility planning, so it should be decided before the control cabinet is wired.
Q: What grain and micronutrient formulations can each model process?
A: All five models handle broken rice, rice flour, corn, millet, wheat, oats, buckwheat, bean, and starch bases with vitamin and mineral supplements. The screw configuration and feeding system — single or double screw — are selected based on your specific formulation characteristics to ensure stable feed and proper gelatinization.
Q: How should I compare installed power versus power consumption across models?
A: Installed power covers peak loads including motor startup and all heater elements. Power consumption reflects typical running draw. The gap between the two values widens on larger models because the drying and roasting stations carry more heating zones. Use the consumption figure for operating cost estimates and the installed figure for electrical supply sizing.