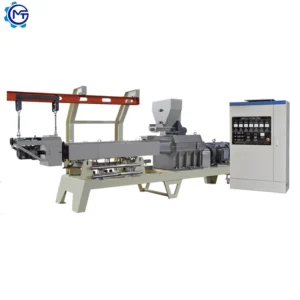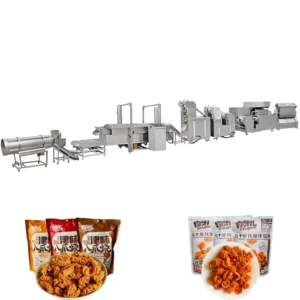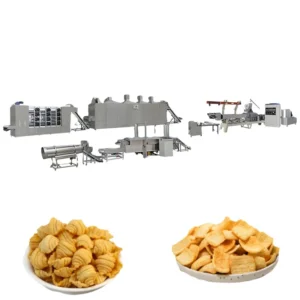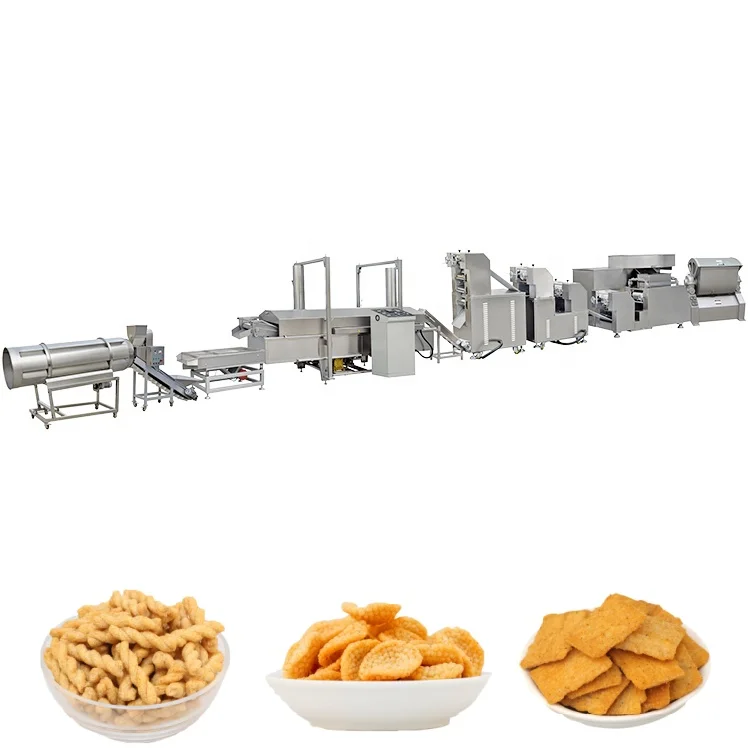
Integrated Line Sizing — throughput for the extruder, dryer and fryer is matched under one engineering scope rather than assembled from separate vendors.
Technical Specifications
| Parameter | Value |
|---|---|
| Model | MT-65 / MT-70 / MT-85 / MT-75 / MT-95 |
| Product Type | Fried Snack Food Production Line (Extruded Pellet Chips) |
| Screw Type | Twin screw, co-rotating, sectional modules |
| Main Motor Power | 100 kW (MT-65) / 130 kW (MT-70) / 185 kW (MT-75) / 180 kW (MT-85) / 280 kW (MT-95) |
| Output Capacity | 120-150 kg/h (MT-65, basis to be confirmed with raw material) |
| Output Capacity | 200-250 kg/h (MT-70, basis to be confirmed with raw material) |
| Output Capacity | 400-500 kg/h (MT-75, basis to be confirmed with raw material) |
| Output Capacity | 300-500 kg/h (MT-85, basis to be confirmed with raw material) |
| Output Capacity | 800-1000 kg/h (MT-95, basis to be confirmed with raw material) |
| Mixer Power | 4 kW / 7.5 kW / 15 kW (matched to line capacity) |
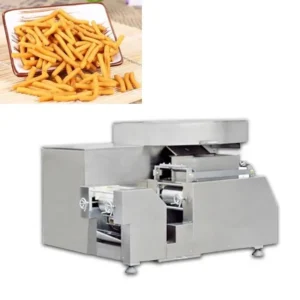
| Cutting Machine | 1.47 kW, 2500×600×1100 mm |
| Fryer Belt Width | 600 mm, stainless steel |
| Fryer Energy Options | Electricity / Fuel / Gas |
| Drying Method | Gas / Electric / Diesel heating |
| Voltage & Frequency | Configurable (e.g. 3ph 380V 50Hz, 3ph 415V 60Hz) |
| Food Contact Material | Stainless steel |
| Standards | CE, ISO |
| Warranty | 1 year complete warranty, life-time maintenance service |
Application Suitability
| Application | Material or Output |
|---|---|
| Corn bugles production | Corn powder, wheat flour blends |
| 3D pellet chips | Potato starch, potato powder, corn starch |
| Geometric extruded snacks | Diamond, wavy, pillow, shell and tube shapes from grain-based formulations |
| Contract snack packaging | Multi-SKU shape changeover on a single twin-screw extruder platform |
What the Rated Kilograms per Hour Actually Mean on Your Formulation
A capacity figure without a raw material basis is a guess, not a specification.
I remember spending two weeks on-site in Chile, re-tuning screw elements and die gaps because the local corn flour had a completely different starch-to-moisture profile than the standard test blend. The extruder was rated for a comfortable output, but on their actual feedstock the expansion collapsed and the line ran at a fraction of its paper capacity. When surveying the frying chips making machine full equipment range, the critical step is confirming throughput against your own ingredient certificate of analysis, not the supplier’s bench formula. Line capacity shifts noticeably depending on whether you run pure corn grits, a wheat-cut blend, or a high-potato-starch dough [NEED_CITE: raw material moisture and starch content effects on extrusion throughput].
How Each Station Fits the Full Equipment Catalogue
Every station in this fried snack line — from the batching mixer through the twin-screw extruder, multi-layer dryer, continuous fryer and seasoning drum — is sized against the same throughput target. The MT-65 through MT-95 models each pair with a proportionally rated dryer and a fryer built around a 600 mm stainless steel belt. This means you review the frying chips making machine full equipment range knowing that no single station will bottleneck the others.
Die and Roller Changeover Across Snack Formats
The sectional screw modules and interchangeable die plates let one extruder produce corn bugles, pillow shapes, diamond chips, wave chips and round or square tubes. Switching a product format requires swapping the die and cutting roller, not replacing the extruder barrel. For contract manufacturers running several brand SKUs on one line, that flexibility shortens changeover between production runs and keeps the frying chips making machine full equipment range relevant across shifting market demands [NEED_CITE: extruder die configuration and snack shape versatility].
Reading the Power and Dimension Data
The motor power spread — from 100 kW on the MT-65 to 280 kW on the MT-95 — reflects the torque needed to drive higher volumes of viscous, starch-rich dough through the barrel at cooking temperature. Twin-screw co-rotating geometry provides the shear and residence time required for full gelatinisation in a single pass. Fryer energy options span electricity, fuel and gas, so the thermal input can match whatever utility tariff is cheapest at the installation site. Overall line dimensions grow with model size, meaning floor planning must account for the longest configuration reaching well over twenty metres including the dryer and cooling conveyors.
When Undersized Supporting Equipment Costs You Output
An extruder that runs at spec means nothing if the downstream dryer cannot remove enough moisture before frying, or if the fryer belt cannot carry the volume without crowding. I have walked into plants where the extruder was upgraded but the original dryer stayed, causing half-cooked pellets to enter the fryer and produce dense, oil-logged chips. Matching every station to the selected extruder model prevents that kind of hidden throughput ceiling [NEED_CITE: downstream equipment bottleneck in snack extrusion lines].
Why Survey the Line from One Equipment Supplier
Complete lines from batching to packing under a single engineering scope mean throughput is calculated across every station, not guessed at each interface. Screw configuration and die design are specified to your raw material and target chip format before production begins. An in-house testing workshop allows trial runs on your actual corn, wheat or potato starch blend before the line is crated. Pre-sales consultation covers layout, utility planning and operator training so commissioning proceeds against a known baseline rather than starting from scratch on your factory floor.
Documentation & Verification
- Line layout and capacity calculation showing each station matched to your chosen extruder model
- Screw and die configuration record tied to your specific corn or potato starch formulation
- Electrical schematic with voltage, frequency and control language confirmed before production
- Trial run report generated on your raw material in the testing workshop before dispatch
- CE declaration of conformity and ISO certificate for customs and local compliance
- Wear parts list covering screws, dies and cutting rollers with recommended reorder intervals
Installation, Commissioning & Support
- Foundation and floor space planning based on the full line length, exceeding twenty metres for larger models
- Dedicated electrical circuit sized to the main motor rating, up to 280 kW for the MT-95 extruder
- Modular station delivery with on-site assembly aligned to the pre-confirmed layout drawing
- First-run parameter tuning of barrel temperature zones and fryer belt speed on your raw material
- Operator training covering screw element swaps, die changes and seasoning drum adjustment
- Scheduled wear part supply for sectional screws and die plates to maintain expansion consistency
Before You Send the Inquiry
To configure the right line from the frying chips making machine full equipment range, share your raw material specification including moisture and starch content, the target chip shapes and daily output goal, plus your factory’s voltage, frequency and preferred control panel language. If you have existing upstream mixers or downstream packing equipment, note those interfaces so the line layout accounts for them from the start.
Frequently Asked Questions
Q: What raw materials work with each extruder model in this range?
A: Corn powder, wheat flour, potato starch and potato powder are all compatible. The screw configuration and die selection are adjusted to your specific formulation. Higher starch content blends may require different moisture conditioning and barrel temperature profiles to achieve the target expansion, so sharing your ingredient certificate of analysis at inquiry stage is essential.
Q: How do I select between MT-65, MT-70, MT-75, MT-85 and MT-95?
A: Selection depends on your target output and raw material characteristics. Each model pairs with proportionally sized dryer, fryer and seasoning stations. The MT-65 suits pilot or low-volume production, while the MT-95 addresses high-volume demand. Request a capacity calculation based on your actual formulation to confirm which model holds your required throughput.
Q: Which supporting stations are matched to each extruder size?
A: Every extruder model ships with a mixer, cutting unit, multi-layer dryer, continuous fryer with a 600 mm stainless steel belt, and a flavouring drum — all rated to match that extruder’s throughput. This prevents bottlenecks where one station limits the entire line output.
Q: Can voltage and control panel language be customised?
A: Yes. Voltage and frequency are configurable to standards such as 380V 50Hz or 415V 60Hz. Control panel language is confirmed during the specification review before production. This avoids commissioning delays caused by mismatched utility supply or unreadable HMI screens on your factory floor.
Q: What spare wear parts should I plan for?
A: Sectional screw elements, die plates and cutting rollers are the primary wear items. A wear parts list with recommended reorder intervals is included with every line delivery. Planning your first reorder before the initial set reaches end of life prevents unplanned downtime and maintains consistent chip expansion and shape definition.