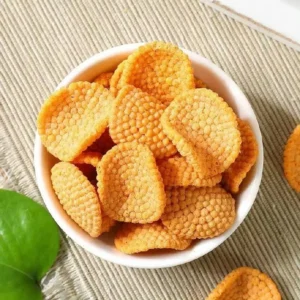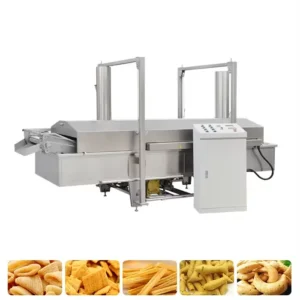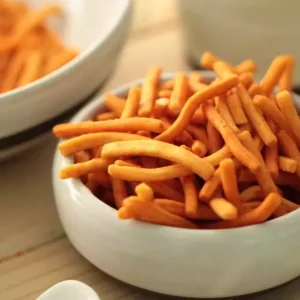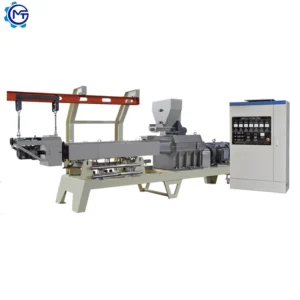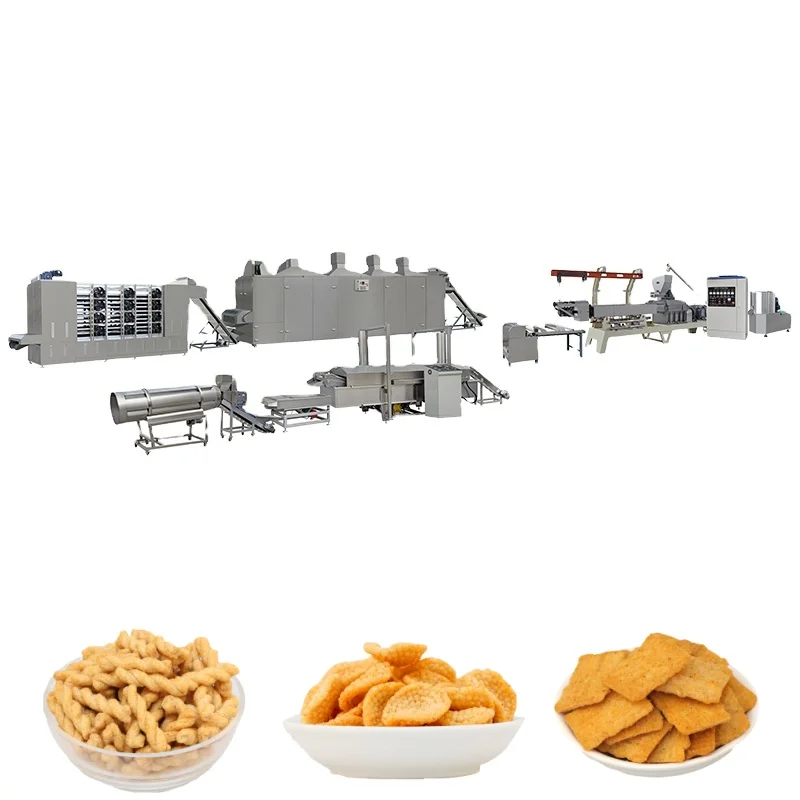
Matched Throughput Across All Stations — mixer, extruder, cutter, and fryer are engineered as one integrated system so no single station bottlenecks the line’s actual output.
Technical Specifications
| Parameter | Value |
|---|---|
| Product Type | Fried Pellet Snack Production Line |
| Model | MT-65 / MT-70 / MT-85 / MT-75 / MT-95 |
| Main Motor Power | MT-65: 100 kW; MT-70: 130 kW; MT-85: 180 kW; MT-75: 185 kW; MT-95: 280 kW |
| Screw Type | Twin screw, co-rotating sectional modules |
| Output Capacity | MT-65: 120–150 kg/h; MT-70: 200–250 kg/h; MT-85: 300–500 kg/h; MT-75: 400–500 kg/h; MT-95: 800–1000 kg/h (basis not stated in source — confirm raw material formulation and moisture) |
| Overall Dimensions (L×W×H) | MT-65: 22000×1200×2200 mm; MT-70: 24000×1500×2200 mm; MT-85/75/95: verify against manufacturer catalog |
| Cutting Machine Power | 1.47 kW |
| Cutting Machine Dimension | 2500×600×1100 mm |
| Fryer Belt Width | 600 mm stainless steel belt |
| Fryer Energy Options | Electricity / Fuel gas |
| Drying Method | Gas / Electric / Diesel heating options |
| Voltage & Frequency | Customizable (e.g., 3ph 380V 50Hz, 3ph 415V 60Hz, 3ph 220V 60Hz) |
| Key Features | Automatic fryer temperature control, adjustable belt speed, roller feeding, multi-energy options, 1-year warranty with lifetime maintenance |
Application Suitability
| Application | Material or Output |
|---|---|
| Bugles and corn chips production | Corn powder, corn starch, wheat flour blends |
| Doritos-style triangular chips | Corn flour and potato starch formulations |
| Salad sticks and crispy pea shapes | Wheat flour, potato powder, corn starch |
| Shell, screw, and tube pellet snacks | Potato starch, corn powder, wheat flour |
| Wave and pillow shaped fried snacks | Corn starch and wheat flour composite blends |
Why Quoted Output Rarely Matches Reality on a Fried Snack Line
Throughput mismatch between the extruder and the fryer is the most common reason a fried snack production line equipment manufacturer fails to deliver its quoted capacity.
When a buyer evaluates a fried snack line, the conversation usually centers on extruder output. But if the downstream fryer belt cannot handle the volume the extruder pushes, product piles up before the fryer entry, cools unevenly, and arrives at packaging with inconsistent oil absorption and texture. The extruder might genuinely produce 400 kg/h of shaped pellets, yet the fryer only processes 300 kg/h at the required residence time. That gap never shows up in a machine spec sheet [NEED_CITE: line throughput balancing methodology for extrusion-to-frying systems].
Years ago I watched a Middle East client’s corn Bugles line shut down for two weeks because the corn flour granulometry was too coarse for the extruder screw profile. The pellets never gelatinised properly, and everything that came out of the fryer was rock-hard scrap. The lesson was clear: a fried snack production line equipment manufacturer must account for the entire chain, not just individual station ratings.
How the Extruder Screw Profile Shapes the Final Chip Texture
The co-rotating twin-screw design uses sectional modules that can be rearranged along the barrel to control forward transport speed, shear intensity, and residence time. For a corn-based Bugle formulation, the screw profile must generate sufficient shear to fully gelatinise the starch before the material reaches the die. A fried snack production line equipment manufacturer that copies a generic screw build from another product category will produce pellets with uneven density, and those pellets fry into chips with hard spots and variable expansion.
Fryer Belt Speed and Oil Absorption Uniformity
The 600 mm stainless steel fryer belt moves shaped pellets through the oil bath at an adjustable speed. Roller feeding at the entry point spaces the pellets evenly so they do not clump or overlap during frying. Automatic temperature control maintains consistent oil temperature across the full belt width. If the belt moves too fast, the pellet surface seals before internal moisture escapes, trapping steam and creating a dense, greasy bite. Too slow, and the chip over-dries and fractures during packaging [NEED_CITE: frying residence time effect on moisture removal and oil uptake in extruded snacks].
Reading the Spec Sheet for What It Does Not Tell You
The main motor power ratings — from 100 kW on the MT-65 to 280 kW on the MT-95 — indicate the mechanical energy available for mixing, shearing, and cooking the raw material inside the barrel. Higher motor power supports formulations with higher starch content or greater viscosity, which demand more torque to push through the die. The customizable voltage options (3ph 380V 50Hz, 3ph 415V 60Hz, 3ph 220V 60Hz) mean the electrical cabinet must be configured before production begins. A mismatch here delays commissioning by weeks while replacement contactors and transformers are sourced. The cutting station at 1.47 kW drives interchangeable shaping rollers, which determines the range of formats the line can produce — bugles, chips, sticks, tubes, waves, or pillows — without needing a separate machine for each shape.
The Hidden Cost of Mismatched Stations in a Fried Chip Line
When the cutting machine output exceeds the fryer belt capacity, partially shaped pellets accumulate on the conveyor, lose moisture, and develop surface cracks before they reach the oil. Those cracks cause uneven oil absorption and produce chips that break during transit. Conversely, when the fryer runs below capacity waiting for the extruder, oil temperature spikes during idle periods, degrading oil quality and shortening the interval between oil changes. Neither scenario appears as a line fault in the control panel — the operator simply sees inconsistent product quality with no obvious cause [NEED_CITE: impact of station throughput mismatch on snack product consistency].
Why Sourcing the Full Line from One Equipment Builder Matters
Every station from the batching mixer through the twin-screw extruder, shaping cutter, and continuous fryer is sized under one supplier, which means throughput calculations account for real material behavior rather than theoretical maximums. Screw configuration and die design are specified to the buyer’s actual raw material formulation and target chip density, not pulled from a generic library. The in-house testing workshop runs trial production on the buyer’s flour or starch blend before shipment, catching granulometry and moisture issues while the screw modules can still be re-cut. Multi-energy drying and frying options — gas, electric, or diesel — are confirmed against the installation site’s utility infrastructure during the engineering phase, not discovered at commissioning. Pre-sales line layout documentation includes station-by-station capacity matching so the buyer can verify throughput balance before the purchase order is signed.
Documentation & Verification
- Line layout drawing showing throughput matched across mixer, extruder, cutter, and fryer stations
- Screw and die configuration record specific to your target chip shape and raw material blend
- Trial run report produced in the testing workshop on your actual corn or potato flour formulation
- Electrical schematic with confirmed voltage, frequency, and control panel language for your facility
- CE declaration of conformity and ISO certificate in electronic edition for customs and import clearance
- Wear parts list with recommended spare screw modules and die plates for sustained production
Installation, Commissioning & Support
- Foundation and floor space planning based on the full line footprint from mixer to fryer discharge
- Dedicated electrical circuit sizing matched to the selected model’s main motor power rating up to 280 kW
- Station-by-station assembly and alignment of the extruder, 2500×600×1100 mm cutter, and 600 mm fryer belt
- First-run parameter setting for barrel temperature zones, screw speed, and fryer belt speed on your raw material
- Operator training covering screw module changes, shaping roller swaps, and fryer temperature adjustment
- Spare wearing parts package including replacement screw sections, die plates, and fryer belt segments
What to Share When Requesting a Line Proposal
To receive an accurate configuration, provide your raw material specification including flour granulometry and moisture content, your target daily output in finished product weight, and the chip formats you plan to produce. Confirm your facility voltage, frequency, and the control language your operators require. If you have existing upstream batching or downstream seasoning and packing equipment, share those station capacities so the extrusion-to-frying segment can be matched to them.
Frequently Asked Questions
Q: How is the output capacity of each line model verified before quotation?
A: Output figures are based on specific raw material formulations and moisture levels. Before we quote a capacity, we request your flour sieve analysis and formulation data. A trial run in the testing workshop on your actual material produces a verified output report that accounts for real starch gelatinisation behavior, not theoretical extruder displacement.
Q: How do you ensure throughput balance between the extruder and the fryer?
A: Each station is sized as part of one integrated system. We calculate the extruder output on your formulation, then select a fryer belt speed and oil bath length that matches that volume at the required frying residence time. The line layout document shows this station-by-station balance so you can review it before production begins.
Q: Can we send our raw material for a trial run before the line ships?
A: Yes. Buyers are encouraged to send a representative sample of their corn flour, potato starch, or blended formulation. The testing workshop runs the material through the configured extruder and cutter, then fries the output. The trial run report documents product density, expansion, oil absorption, and texture against your target specification.
Q: What spare parts should we stock for the first years of operation?
A: Free wearing parts ship with the line. We recommend ordering additional spare screw modules, die plates, shaping rollers, and fryer belt segments sufficient for two to three years of sustained production. A detailed wear parts list with part numbers is included in the documentation package for easy reordering.