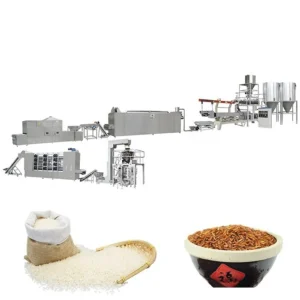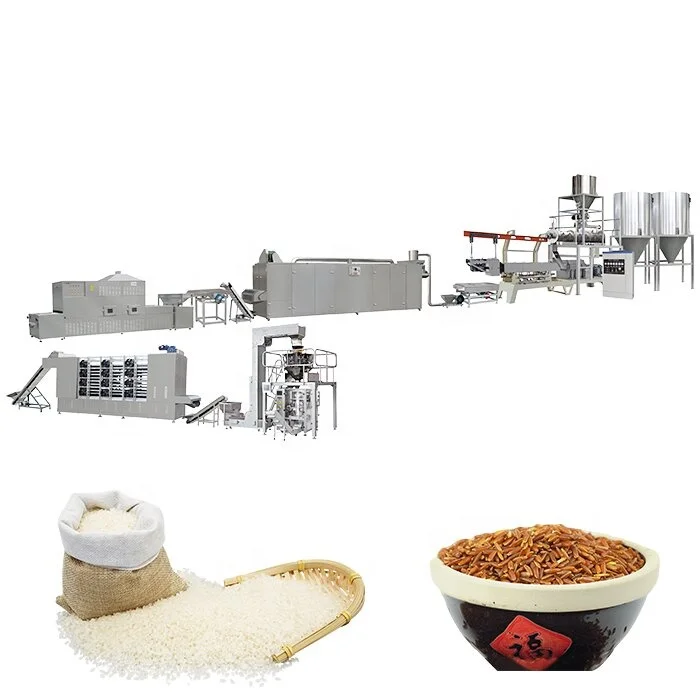
Turnkey line integration — Every station from batching to packing is throughput-matched so no single unit bottlenecks the fortified rice production line complete equipment range.
Technical Specifications
| Parameter | Value |
|---|---|
| Model | MT65 / MT70 / MT85 / MT75 / MT95 |
| Product Type | Fortified Rice and Instant Rice Production Line |
| Extruder Type | Twin-screw |
| Feeding System | Single or double screw feeding (matched to material) |
| Control System | Frequency speed control with high automation |
| Lubrication & Cooling | Automatic lubricating and cooling system |
| Drying Oven Heating Source | Electric or gas |
| Drying Oven Feature | Circulation drying, frequency motor controls mesh belt speed |
| Screw Material | Special wear-resistant technology |
| Assembly State | Complete turnkey line |
| Line Configuration | Mixing → Extruding → Vibrating → Low Temperature Drying → Cooling → High Temperature Roasting → Cooling → Packing |
| Raw Materials | Broken rice, rice, corn, millet, wheat, oats, buckwheat, bean, starch; vitamin and mineral additives |
| Final Products | Artificial rice, fortified rice kernels |
| MT65 Capacity | 80–100 kg/hr (basis not stated in source — confirm raw material and moisture content) |
| MT65 Installed Power | 85 kW |
| MT65 Power Consumption | 60 kW |
| MT65 Dimensions | 28 × 1.2 × 2.2 m |
| MT70 Capacity | 100–120 kg/hr (basis not stated in source — confirm raw material and moisture content) |
| MT70 Installed Power | 120 kW |
| MT70 Power Consumption | 85 kW |
| MT70 Dimensions | 30 × 1.5 × 2.2 m |
| MT85 Capacity | 200–300 kg/hr (basis not stated in source — confirm raw material and moisture content) |
| MT85 Installed Power | 235 kW |
| MT85 Power Consumption | 165 kW |
| MT85 Dimensions | 34 × 3.5 × 4.3 m |
| MT75 Capacity | 300–500 kg/hr (basis not stated in source — confirm raw material and moisture content) |
| MT75 Installed Power | 180 kW |
| MT75 Power Consumption | 135 kW |
| MT75 Dimensions | 32 × 3.5 × 4.3 m |
| MT95 Capacity | 800–1000 kg/hr (basis not stated in source — confirm raw material and moisture content) |
| MT95 Installed Power | 260 kW |
| MT95 Power Consumption | 195 kW |
| MT95 Dimensions | 36 × 3.5 × 4.3 m |
| Standards | CE, ISO |
Application Suitability
| Application | Material or Output |
|---|---|
| Fortified rice for nutrition programmes | Rice flour blended with vitamin and mineral premix, extruded into kernel shape |
| Artificial rice from broken rice | Broken rice and rice bran reprocessed into reconstituted high-nutritional-value kernels |
| Instant rice manufacturing | Pre-gelatinised rice kernels for rapid rehydration in consumer packaging |
| Multigrain rice analogues | Corn, millet, wheat, oats, buckwheat, and bean blends extruded into rice-shaped kernels |
When the Extruder Outruns the Dryer
Capacity numbers on a single machine mean nothing if the next station cannot keep up.
On fortified rice lines I have seen extruders pushing product faster than the downstream dryer can handle moisture removal. The result is a backlog of wet kernels that clump on the cooling belt, surface cracks from uneven drying, and an actual throughput well below what the extruder plate says. This is where buyers evaluating a fortified rice production line complete equipment range need to look beyond individual machine ratings and examine the entire flow.
A line is only as fast as its slowest station. Matching extruder output to dryer belt speed, cooler residence time, and packing rate is what separates a line that runs at nameplate capacity from one that constantly stalls. [NEED_CITE: throughput balancing across sequential food processing stations]
Matching Each Station to the Next
The MT series twin-screw extruders span five capacity tiers, allowing the fortified rice production line complete equipment range to be scaled from pilot volumes to industrial output. Each model pairs with a circulation drying oven where a frequency-controlled motor adjusts mesh belt speed, giving operators the ability to fine-tune drying time without changing hardware. The vibrating station between extruder and dryer separates kernels before they enter the oven, reducing clumping and ensuring uniform moisture removal across the belt width.
Heating Source Selection and Drying Profile
The drying oven supports both electric and gas heating, letting buyers align with local utility costs and availability. Low temperature drying removes surface moisture without case-hardening the kernel, while the subsequent high temperature roasting stage develops the final texture and shelf stability. Two cooling stages — one after drying and one after roasting — bring the product to packing temperature gradually, preventing condensation inside the packaging. This multi-stage thermal profile is what gives reconstituted rice its ability to rehydrate quickly without turning mushy. [NEED_CITE: starch retrogradation and rehydration kinetics in extruded rice]
Reading the Spec Sheet for Production Impact
The twin-screw design handles a wider range of raw material blends compared to single-screw extruders, which is important when the recipe includes high-fat vitamin premixes or bean flours that alter friction inside the barrel. The automatic lubrication and cooling system keeps barrel temperature stable during long runs, reducing the chance of gelatinisation inconsistency between the first batch and the fiftieth. Frequency speed control on both the feeding system and the main screw allows operators to adjust shear and residence time without stopping the machine, which matters when switching between a pure rice formula and a multigrain blend. Screw material uses wear-resistant technology to extend service intervals, a practical advantage when processing mineral-fortified mixes that are more abrasive than plain starch.
The Cost of Skipping Station-Level Matching
I worked on a project in the Gulf region where the buyer ordered an extruder rated for a certain throughput but selected a dryer one tier smaller. Within the first week, wet kernels piled up at the dryer infeed, forcing the operator to cut extruder speed in half. The line never recovered its planned output, and the buyer spent additional capital retrofitting a larger oven. Bottlenecks like this are not visible on a quotation that lists machines individually without showing the throughput relationship between them. [NEED_CITE: hidden cost of mismatched sequential processing equipment]
Why Source the Full Line Here
Every station in the fortified rice production line complete equipment range is selected so throughput aligns across mixing, extruding, vibrating, drying, cooling, roasting, and packing. Screw configuration and die design are specified to the buyer’s actual raw material blend rather than copied from a generic build. An in-house testing workshop runs the buyer’s recipe before shipment, producing a trial run report that confirms kernel shape, density, and drying behaviour. Electrical schematics and voltage are confirmed for the destination market before production begins. Pre-sales engineering covers line layout and utility planning, with on-site installation and operator training included in the project scope.
Documentation & Verification
- Line layout and capacity calculation showing throughput matching across every station
- Machine specification sheet with screw and die configuration record per model
- Electrical schematic and voltage confirmation matched to destination market
- Trial run report on buyer’s raw material from in-house testing workshop
- CE declaration of conformity and ISO certificate included with shipment
- Factory test record and packing photographs for customs documentation
Installation, Commissioning & Support
- Foundation and floor space planning based on line dimensions up to 36 × 3.5 × 4.3 m for the MT95 configuration
- Power supply specification covering installed power requirements from 85 kW to 260 kW depending on model
- Frequency-controlled feeding and extruder drives configured to local voltage and frequency before dispatch
- First-run parameter setting including barrel temperature profile and mesh belt speed for the buyer’s recipe
- Operator training covering screw configuration changes and automatic lubrication system maintenance
- Wear parts list with screw and die replacement schedule provided at commissioning
What to Prepare Before Requesting a Quote
To size the right extruder model and supporting stations, share your raw material recipe including the percentage of vitamin or mineral premix, your target hourly output, and the local voltage and frequency at the installation site. If you have an existing packing system upstream or downstream, provide its speed rating so the line can be matched accordingly. Let us know whether you need a trial run on your specific blend before the equipment leaves the factory.
Frequently Asked Questions
Q: How do I select the correct extruder model for my target output?
A: The MT series covers five capacity tiers. Selection depends on your raw material recipe, target moisture after extrusion, and desired daily output. We cross-reference your formula against each model’s screw configuration and power rating, then confirm with a trial run in the testing workshop before finalising the quotation.
Q: What supporting equipment is needed to prevent line bottlenecks?
A: Every station — mixer, extruder, vibrating separator, dryer, cooler, roaster, and packing unit — must match in throughput. We provide a line layout and capacity calculation document that shows the rated flow at each stage so no single machine restricts the overall output of the fortified rice production line complete equipment range.
Q: Can the voltage and control language be configured for my country?
A: Yes. Electrical schematics, motor ratings, and control panel language are confirmed during the specification stage before production begins. This covers voltage, frequency, and plug standards for the destination market, avoiding commissioning delays caused by mismatched electrical supply.
Q: How are screw and die configurations matched to my raw material?
A: We collect your exact formula including starch type, protein content, and premix ratio. The screw elements and die geometry are then selected to achieve the correct kernel density and shape. A trial run on your material in our testing workshop validates the configuration before the machine ships.
Q: What documentation comes with the shipment?
A: Each delivery includes the machine specification sheet, screw and die configuration record, electrical schematic, CE declaration, ISO certificate, factory test record, trial run report, operation and maintenance manual, wear parts list, and packing photographs to support customs clearance.