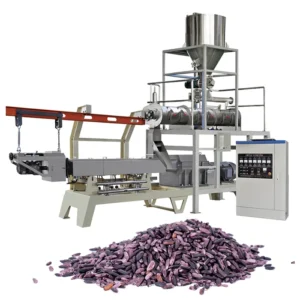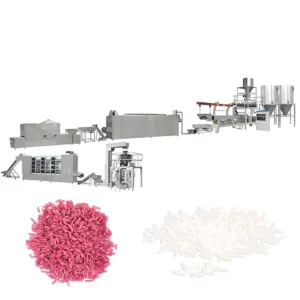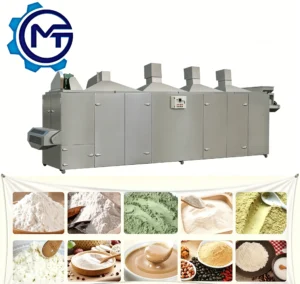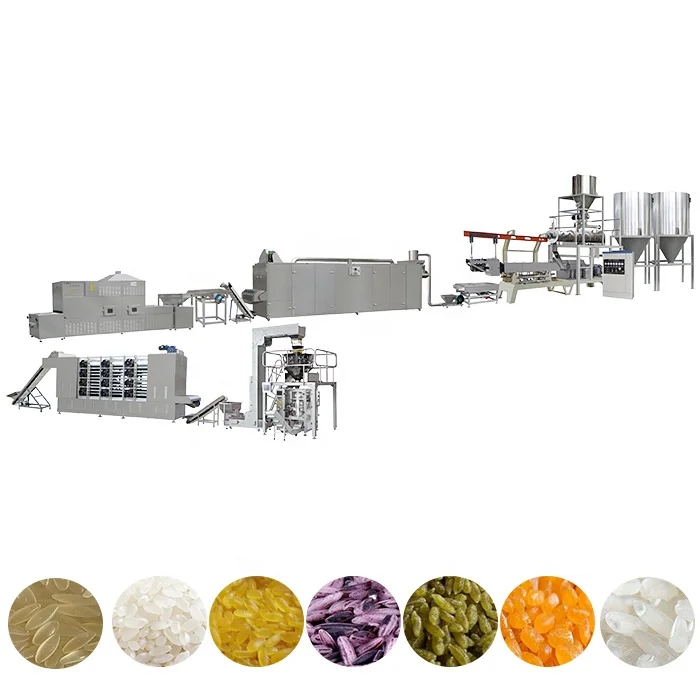
Integrated station throughput — Every machine from mixing through polishing is sized against your raw material characteristics rather than a generic nameplate capacity.
Technical Specifications
| Parameter | Value |
|---|---|
| Product Type | Twin Screw Extrusion Line for Fortified Instant Rice Porridge |
| Extruder Type | Double screw extruder machine |
| Construction Material | Food grade stainless steel 201/304 |
| Energy Source Options | Electricity, gas, diesel, or steam |
| Motor Brand | Siemens (made in China) or China top brand |
| Inverter Brand | Delixi or Delta |
| Control System | Special control cabinet |
| Oven Type | Multi-layer electric oven, stainless steel double-layer mesh belt |
| Oven Temperature Range | 0–200°C (adjustable via control cabinet) |
| Drying Configuration | Seven-layer, 8-meter dryer |
| Line Stations | Mixing → Screw Conveying → Extruding → Vibrating Screen → Blower/Air Conveying → Multi-layer Oven → Cooling Conveyor → Polisher |
| Certification | CE, ISO |
| Warranty | One year free warranty |
Application Suitability
| Application | Material or Output |
|---|---|
| Fortified instant rice porridge | Rice flour, broken rice, rice bran with added vitamins and minerals |
| Multigrain instant porridge | Black rice, buckwheat, oat, and blended cereal grains |
| Artificial and reformed rice | Starch-based formulations with trace element fortification |
| Nutrition programme products | Blended food formulations for institutional and aid distribution |
| Value-added grain processing | Repurposed broken rice and bran into shelf-stable instant formats |
Why the Dryer Footprint Matters More Than Extruder Nameplate
A seven-layer drying section must be matched to the extruder’s actual discharge rate on your specific formulation, not its catalogue rating.
When buyers compare lines, the first number they see is extruder output. But instant rice porridge requires thorough moisture removal across multiple drying stages. If the dryer is undersized for the actual throughput — especially on high-fibre or high-moisture formulations — product backs up on the mesh belt, residence time drops, and you get unevenly dried granules that clump during cooling. I have watched this exact mismatch shut down packaging stations downstream because the cooling conveyor received product still carrying residual moisture [NEED_CITE: thermal drying principles for extruded food products]. A twin screw extrusion line for fortified rice porridge manufacturer that specifies the dryer in relation to real recipe behaviour avoids this cascade of stoppages.
Station Sequence and Throughput Alignment
The line moves raw blend through eight distinct stations, and each transition point is where throughput imbalances surface. After the twin screw extruder forms and expands the rice granules, a vibrating screen removes fines and oversize pieces before the blower conveys product into the seven-layer oven. The twin screw extrusion line for fortified rice porridge manufacturer configuration keeps material flow continuous by sizing the air conveying volume to the extruder discharge rate.
Mesh Belt Design and Drying Uniformity
The stainless steel double-layer mesh belt inside the eight-meter dryer allows heated air to circulate through the product bed rather than only across its surface. Temperature adjustability from ambient to 200°C means operators can set different zones — a higher temperature entry for rapid surface moisture removal and a lower final zone to bring internal moisture to target without case hardening. This zoning matters when formulations contain varying ratios of rice bran or buckwheat, which release moisture at different rates during thermal exposure [NEED_CITE: drying kinetics of cereal-based extrudates].
Screw Configuration and Die Selection for Granule Geometry
The twin-screw extruder section relies on screw element arrangement and die plate geometry to control the size, density, and expansion ratio of the output granules. Rice flour behaves differently from blended formulations containing buckwheat or oat fibre — the screw compression ratio and moisture injection point shift accordingly. Die hole diameter and land length determine whether the product exits as small instant porridge granules or larger reformed rice kernels. Getting this wrong means the vibrating screen rejects a large share of output, reducing effective yield even when the extruder itself runs without interruption.
Specifying What Nameplate Data Leaves Out
Rated electrical power around 100 kW applies to a full electric-heated line configuration, while gas or diesel heating for the dryer section brings total connected load to roughly 50–60 kW for the remaining driven stations. These figures shift with the number of heating zones actually energised and the motor load on the extruder under your recipe. Voltage and frequency must be confirmed against the target market standard before the control cabinet is wired — a 50 Hz motor running on 60 Hz supply will alter screw speed and material residence time inside the barrel [NEED_CITE: industrial motor frequency conversion effects]. The Delixi or Delta inverter specification allows variable speed on the extruder drive, giving operators a tuning range once the line is running on actual material.
The Cost of Skipping the Trial Run
Lines shipped without a pre-dispatch trial on the buyer’s actual formulation often require weeks of adjustment after installation. Screw configuration that works on standard white rice flour may fail to maintain stable discharge on a recipe loaded with coarse bran or buckwheat. The dryer temperature profile set at the factory assumes a reference moisture content that your recipe may not match. These issues compound: unstable extrusion feeds the dryer unevenly, which then produces inconsistent moisture levels that confuse the cooling conveyor and polisher downstream [NEED_CITE: post-extrusion drying consistency requirements].
What Distinguishes This Equipment Range
Complete station matching under one supplier means the vibrating screen aperture, air conveying velocity, and dryer belt speed are all referenced to the same throughput calculation rather than sourced independently. Food-grade stainless steel 201/304 contact surfaces across every station meet hygiene requirements for nutritional food production. An in-house testing workshop allows trial runs on buyer-supplied raw material before the line leaves the factory. Screw configuration and die design are specified to the target product shape and density, not copied from a generic build. Pre-sales consultation covers line layout and utility planning through to commissioning and operator training on site.
Documentation & Verification
- Line layout drawing with throughput calculation across all eight stations
- Screw and die configuration record matched to your grain formulation
- Electrical schematic with voltage and frequency confirmed for your market
- Factory trial run report on your supplied raw material before dispatch
- CE declaration of conformity for the complete assembled line
- Operation and maintenance manual with wear parts schedule
Installation, Commissioning & Support
- Foundation plan accounting for the eight-meter dryer footprint and extruder vibration isolation
- Dedicated electrical circuit sized to the confirmed heating and motor load configuration
- Modular station delivery requiring on-site assembly and belt alignment
- First-run parameter logging for extruder barrel temperatures and dryer zone setpoints
- Operator training on die changeover and mesh belt tension adjustment
- Wear parts list covering screw elements, die plates, and mesh belt sections
Before You Request a Quotation
To configure a twin screw extrusion line for fortified rice porridge manufacturer proposal accurately, share your target formulation including the percentage of whole grains, bran, and fibre additions. Specify the local voltage and frequency standard, as well as your preferred energy source for the dryer section. A sample of your raw material enables a trial run in the testing workshop so the screw and die configuration can be validated before shipment.
Frequently Asked Questions
Q: What is the full equipment list in this line and where does each station fit?
A: The line includes a mixer, screw conveyor, twin screw extruder, vibrating screen, air blower conveyor, seven-layer dryer, cooling conveyor, and polisher. Each station transitions product sequentially from raw blending through forming, drying, and surface finishing. Optional packing stations can be added downstream depending on your packaging format and filling speed requirement.
Q: How do I choose between electricity, gas, diesel, or steam for the dryer?
A: The choice depends on your local utility cost structure and available infrastructure. Electric heating offers precise zone control through the cabinet. Gas or diesel heating reduces connected electrical load substantially. Steam is suitable if your facility already operates a boiler. We confirm the energy source during quotation so the dryer is built with the correct burner or element configuration.
Q: What screw and die configurations are available for different granule shapes?
A: Screw element arrangement controls shear and compression inside the barrel, which determines expansion ratio and product density. Die plates are interchangeable with varying hole diameters and land lengths to produce small porridge granules or larger reformed rice shapes. Configuration is finalised after reviewing your formulation and target product specification.
Q: How is the dryer capacity matched to extruder output?
A: The seven-layer, eight-meter dryer is sized so that product residence time on the mesh belt achieves target moisture removal at the extruder’s actual discharge rate. We calculate this based on your recipe moisture content and the thermal profile required. Undersized dryers cause backlog; oversized dryers waste energy and floor space.
Q: What supporting equipment is included and what is optional?
A: The standard line includes all stations from mixing through polishing as a complete assembly. Packing equipment is configured separately based on your bag format, fill weight, and sealing method. Upstream raw material handling such as silos or pneumatic intake systems can be added depending on your facility layout and material delivery method.