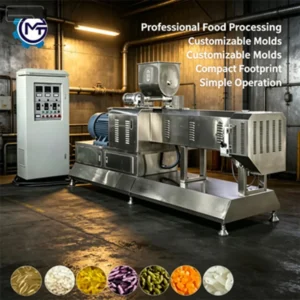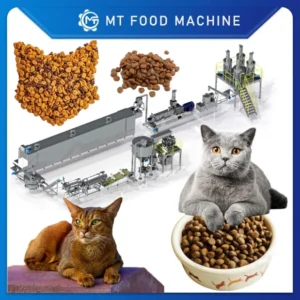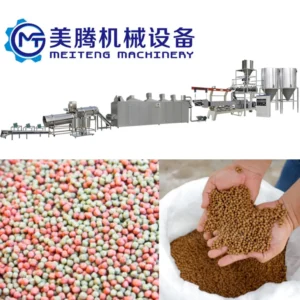
Integrated Line Matching — every station from feeding through cooling is sized to the same throughput target, eliminating the bottleneck that occurs when an extruder outpaces its dryer or cooler.
Technical Specifications
| Parameter | Value |
|---|---|
| Product Type | Complete Aquatic Feed Production Line |
| Extruder Type | Twin Screw |
| Output Capacity | 500 kg/h floating fish feed pellets (basis not stated in source — confirm raw material formulation / moisture content / pellet diameter) |
| Pellet Diameter Range | 0.5 mm – 12 mm |
| Line Stations | Feeding, mixing, extruding, pelletizing, drying, cooling |
| Construction Material | Stainless steel (main parts) |
| Control System | Simple control panel (PLC / MCC not specified in source) |
| Automation Level | Fully automatic, continuous operation |
| Power / Voltage / Frequency | Available upon request (confirm destination market requirements) |
| Certification | CE / ISO (manufacturer profile; verify against line-specific documentation) |
Application Suitability
| Application | Material or Output |
|---|---|
| Floating fish feed production | Corn, soybean meal, fish meal, rice bran blends for carp, tilapia, catfish |
| Sinking aquatic feed production | High-protein formulations for shrimp and bottom-feeding species |
| Fingerling feed manufacturing | Fine pellets at 0.5 mm – 2 mm diameter for early growth stages |
| Grow-out feed manufacturing | Standard pellets at 3 mm – 12 mm diameter for maturation stages |
| Small to medium feed mill conversion | Batch-to-continuous processing upgrade for existing aquaculture operations |
Why "500 kg/h" Means Nothing Without the Rest of the Line
A rated capacity figure is only as useful as the raw material formulation it was measured against.
When a buyer sees an aquatic feed equipment complete line quoted at a certain throughput, the immediate question should be: on what material, at what moisture, with what pellet size? I have walked into facilities where the extruder was technically capable of the stated output, but the dryer downstream was undersized by a wide margin. Pellets exited the die at high moisture, piled up waiting for drying capacity that was never going to arrive, and within hours the storage bins were generating heat from bacterial activity. The extruder was never the problem — the mismatch between stations was. [NEED_CITE: moisture content thresholds for safe aquatic feed pellet storage]
Station-by-Station Throughput Alignment
The feeding, mixing, extruding, pelletizing, drying, and cooling modules on this aquatic feed equipment complete line are specified as an integrated set. Each station is calculated against the same target output so that material flows continuously without accumulation points. This matters most when producers switch between floating and sinking feed formats, because the two products demand different residence times in the dryer and cooler. A line assembled from separate vendors rarely accounts for this shift, leaving operators to manually pace upstream equipment whenever the product format changes.
Pellet Diameter Coverage Across Growth Stages
The 0.5 mm to 12 mm die range means a single aquatic feed equipment complete line can serve hatchery through grow-out operations without requiring a second extrusion platform. Switching from fingerling feed to adult feed involves a die plate change and corresponding adjustments to barrel temperature profile and cutter speed. Stainless steel contact surfaces throughout the wet zone resist corrosion from fish meal and shrimp meal formulations, which tend to accelerate wear on carbon steel components when production runs continuously over multiple shifts. [NEED_CITE: material compatibility standards for feed processing contact surfaces]
Screw Configuration and Moisture Management
The twin-screw design handles formulations with varying fat and protein levels more predictably than single-screw alternatives, particularly when recipes include high-moisture ingredients or significant fish meal content. The screw elements and barrel zones work together to control shear and residence time, which directly governs starch gelatinisation and, in turn, pellet buoyancy. For floating feed, adequate gelatinisation traps air during expansion; for sinking feed, the screw profile is adjusted to reduce expansion and increase density. The simple control panel allows operators to set and monitor barrel zone temperatures, though buyers planning complex multi-recipe production should confirm whether PLC or MCC control is available for recipe storage and automated changeover.
What Happens When the Dryer Is an Afterthought
I worked on a project in Southeast Asia where the client received an extruder that performed well during factory testing on standard fish meal formulations. Once installed and running a high-oil shrimp feed recipe, the pellet moisture coming off the die was far higher than anticipated. The dryer — sourced separately and sized for a different product profile — could not pull the moisture down to safe storage levels. Within a single production week, stored pellets were developing mould. The line was technically complete but operationally broken. Matching dryer capacity to the actual extruder output on the buyer’s real formulation, not a generic test material, is what separates a working line from an expensive lesson. [NEED_CITE: common causes of post-extrusion moisture failure in aquatic feed lines]
Why This Supplier Configuration Differs
The twin-screw extrusion expertise here covers aquatic feed specifically, not just puffed snacks repurposed for feed production. Every station from the batching system through the cooling conveyor is sourced under one supply contract, which means throughput calculations and physical layout are produced as a single engineering document rather than stitched together from multiple vendor quotations. An in-house testing workshop allows trial runs on the buyer’s actual raw material before the line ships — this is not a demonstration on generic corn flour but a run using the exact fish meal, soybean, and additive blend the facility will use in production. Screw configuration and die design are recorded against the buyer’s formulation so that replacement parts match what was validated. Electrical schematics are confirmed against destination voltage and frequency before assembly begins, avoiding the commissioning delays that arise when a 50 Hz motor is wired into a 60 Hz plant.
Documentation & Verification
- Line layout drawing showing throughput calculation for each station from feeder to cooler
- Screw and die configuration record matched to your specific aquatic feed formulation
- Trial run report produced on your raw material blend before shipment approval
- Electrical schematic with voltage, frequency, and control language confirmed for your facility
- Factory test record documenting output rate, pellet buoyancy, and moisture at each stage
- CE declaration of conformity and ISO certificate for customs and local compliance
Installation, Commissioning & Support
- Foundation plan provided based on line footprint and dryer/cooler weight distribution
- Power supply schedule listing dedicated circuit requirements for extruder main drive and dryer heaters
- Modular shipment with reassembly supervision on site for extruder barrel and screw alignment
- First-run parameter setting covering barrel temperature zones, die pressure, and dryer belt speed
- Operator training on die changeover procedure between floating and sinking pellet formats
- Wear parts list including screws, die plates, and dryer mesh with recommended first-order quantities
What to Include in Your Inquiry
To move past generic quotations and get a line configuration that actually fits your production target, share your raw material formulation (including fish meal percentage and fat content), your target pellet diameter range, and your daily or hourly output goal. Confirm the voltage and frequency at your facility, and whether you need control panel labels in a specific language. If you have existing upstream or downstream equipment that this line needs to integrate with, include those specifications as well. Sending a sample of your actual raw material for a pre-shipment trial run eliminates the most common source of post-installation disputes.
Frequently Asked Questions
Q: How do I confirm the 500 kg/h capacity applies to my specific formulation?
A: The stated output was measured under conditions that may not match your raw material blend, moisture content, or target pellet diameter. Request a trial run in the testing workshop using your actual fish meal, soybean, and additive formulation. The resulting trial report will document real throughput, pellet buoyancy, and moisture levels on your material.
Q: Are the dryer and cooler sized to match the extruder output on my recipe?
A: Every station on this aquatic feed equipment complete line is calculated against the same throughput target. Confirm your formulation’s expected moisture at the die exit so the dryer belt length and air temperature can be verified against your specific drying curve, especially if you run high-fat shrimp feed recipes.
Q: What is involved in switching between floating and sinking pellet production?
A: Die plate replacement is the primary changeover step, along with adjustments to barrel temperature profile and screw speed. The 0.5 mm to 12 mm range covers most aquaculture stages. Ask for the documented changeover procedure and confirm whether spare die plates for your required diameters are included in the initial spare parts package.
Q: Can the control system be configured for my local voltage and operator language?
A: The simple control panel can be specified to match destination voltage and frequency before assembly. Confirm your facility’s power supply details and preferred label language during the quotation stage so that electrical schematics and panel markings are correct before the line ships, avoiding rewiring delays during commissioning.
Q: Which spare wear parts should I order with the initial shipment?
A: Screws, die plates, and dryer mesh are the primary consumables. Request the wear parts list with your quotation and plan a first-order quantity based on your expected weekly production hours. Availability after initial delivery depends on lead times, so having replacements on hand before the first changeover is strongly recommended.