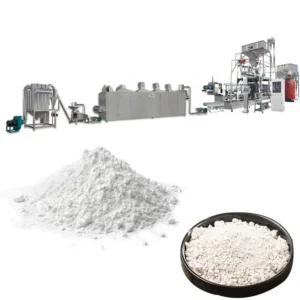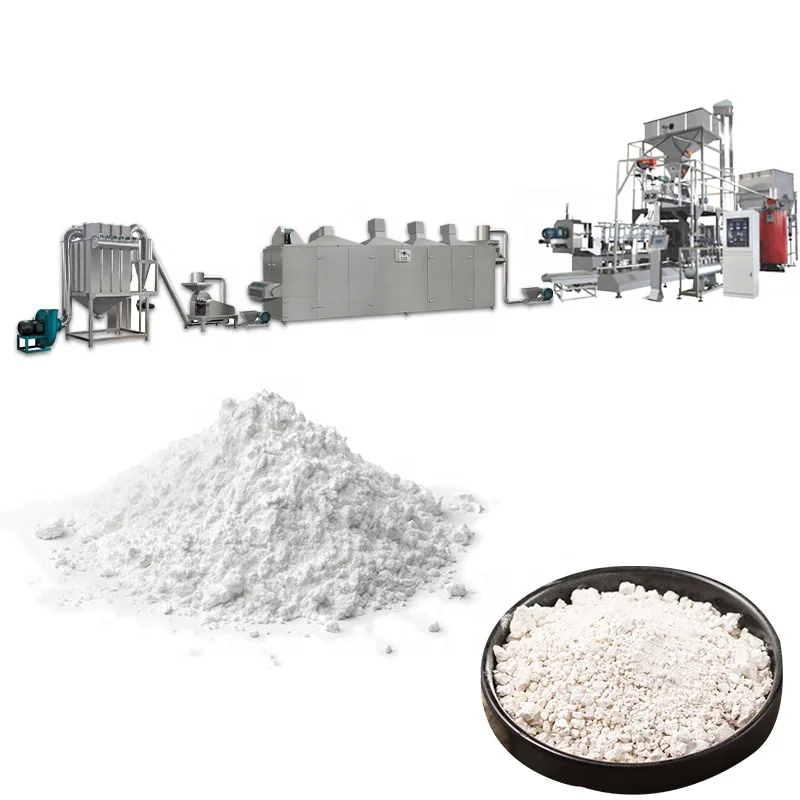
Complete Starch Line Under One Roof — every station from mixer to packing machine is capacity-matched before dispatch, so your extruder never waits on an undersized dryer.
Technical Specifications
| Parameter | Value |
|---|---|
| Model | MT65 / MT70 / MT85 |
| Product Type | Modified Starch Production Line |
| Screw Type | Twin-screw |
| Power Consumption (Line) | MT65: 60 kW; MT70: 80 kW; MT85: 145 kW |
| Output Capacity | MT65: 100–150 kg/h (basis to be confirmed); MT70: 200–250 kg/h (basis to be confirmed); MT85: 300–500 kg/h (basis to be confirmed) |
| Overall Dimensions (L×W×H) | MT65: 24000×1200×2200 mm; MT70: 26000×1500×2200 mm; MT85: 29000×3500×4300 mm |
| Mixer Output | 70–100 kg/h (basis to be confirmed) |
| Mixer Power | 3 kW |
| Extruder Power | 22 kW |
| Roasting Oven Power | 1.1 kW |
| Line Stations | Mixing → Extrusion → Drying → Grinding → Blending → Packing |
| Control System | Available with PLC or MCC control (confirm configuration) |
| Voltage & Frequency | Configurable to target market (confirm before production) |
| Certification | CE |
Application Suitability
| Application | Material or Output |
|---|---|
| Pre-gelatinized starch for food processing | Corn starch, tapioca starch, potato starch |
| Modified starch for textile sizing | Maize starch, cassava starch |
| Industrial starch for oil drilling fluids | Corn starch, potato starch |
| Modified starch for papermaking | Tapioca starch, maize starch |
| Functional starch for chemical additives | Corn starch, cassava starch |
What the Capacity Figure on a Modified Starch Production Line Equipment Range Actually Means
The kg/h number on the nameplate only holds if the raw material and moisture content match the test basis.
I once watched a modified starch line sit idle for five days because the factory trial ran on cassava starch while the buyer’s real feedstock was potato starch. Gelatinisation temperature shifted, shear behaviour changed, and the screw configuration that worked perfectly in Shandong produced half-raw output on site. Every capacity claim for a modified starch production line equipment range needs a stated raw material, a moisture percentage, and a specific screw profile to be meaningful [NEED_CITE: starch gelatinisation temperature variance across botanical sources]. Without those three data points, you are comparing numbers that were never measured under the same conditions.
How Twin-Screw Extrusion Drives Starch Modification
The twin-screw design at the heart of this modified starch production line equipment range generates the controlled shear and residence time required to break down native starch granules. Barrel zones are heated independently, letting operators set a temperature gradient that matches the gelatinisation onset of their specific feedstock. Screw elements can be rearranged to adjust shear intensity, which directly influences the degree of starch modification achieved in a single pass.
Matching Every Station to the Same Throughput Target
An extruder that pushes material faster than the dryer can handle creates a bottleneck that forces the entire modified starch production line equipment range to run below its rated output. Each station in this catalogue — mixer, extruder, dryer, grinder, blender, packing — is specified against the same throughput envelope. That alignment is confirmed in the line layout document before production begins, so no single machine dictates the ceiling for the rest [NEED_CITE: throughput balancing methodology in continuous food processing lines].
Reading the Power and Dimension Data Against Your Factory Floor
The three extruder tiers draw 60 kW, 80 kW, and 145 kW respectively across the full line, which determines transformer sizing and dedicated circuit requirements at your site. Overall line length stretches from 24 m on the MT65 to 29 m on the MT85, and the MT85 also demands 3.5 m in width and 4.3 m in height — figures that must be checked against column spacing and overhead clearance before the foundation is poured. Extruder motor rating sits at 22 kW across the range, while the mixer draws 3 kW and the roasting oven 1.1 kW; these individual loads help your electrician plan panel distribution. Confirming voltage and frequency early avoids the situation where a machine arrives wired for a supply standard that the local grid does not support.
The Hidden Cost of Skipping a Raw-Material Trial Run
When the screw configuration is copied from a generic build rather than matched to the buyer’s actual starch source, the first production run often reveals texture and solubility outside specification. Adjusting on site means days of lost output, wasted raw material, and possible damage to screw elements from repeated restarts under incorrect shear settings. A trial run on the buyer’s own feedstock inside the testing workshop catches these mismatches before the line is crated [NEED_CITE: impact of raw material variability on extrusion screw wear].
Why Procurement From a Single Equipment Catalogue Matters Here
Every station is designed and built under one supplier, so throughput calculations and mechanical interfaces are resolved in the engineering phase rather than discovered during installation. Screw configuration and die geometry are documented against the buyer’s raw material, not pulled from a default library. The in-house testing workshop allows trial runs on customer-supplied starch before the line ships, reducing on-site commissioning time. Electrical schematics and voltage confirmation are completed before production starts, preventing wiring rework after arrival. Pre-sales consultation continues through installation, operator training, and ongoing wear-part supply, keeping a single point of accountability across the project life.
Documentation & Verification
- Line layout showing matched throughput at every station from mixer to packing
- Screw and die configuration record tied to your starch type and moisture level
- Electrical schematic with voltage and frequency confirmed for your site
- Factory trial run report on your raw material before dispatch
- CE declaration of conformity for the complete line
- Operation and maintenance manual with wear parts list
Installation, Commissioning & Support
- Floor plan must accommodate up to 29 m line length and 4.3 m height on the MT85
- Dedicated circuits sized for 60–145 kW total draw depending on model selected
- Modular station delivery allows phased unloading where overhead crane access is limited
- On-site screw configuration fine-tuning against your starch feedstock during commissioning
- Operator training covers barrel zone temperature profiles and PLC or MCC interface navigation
- First-order wear parts list including screws, dies, and mixer blades supplied with the line
- Maintenance schedule aligned to production hours with remote troubleshooting support
What We Need From You to Quote the Right Configuration
To size the modified starch production line equipment range correctly, please share your starch source (corn, tapioca, potato, or other), typical moisture content at the mixer inlet, and target hourly output. Confirm your local voltage and frequency, preferred control language, and available factory floor dimensions including ceiling height. If you have existing upstream or downstream equipment that the new line must integrate with, include those specifications so the layout accounts for connection points from the start.
Frequently Asked Questions
Q: How is output capacity verified for each model?
A: Each capacity figure is based on a specific raw material and moisture content tested in the workshop. Before quoting, we request a sample of your starch so the trial run replicates your actual production conditions. The resulting throughput is documented in the trial report and becomes the guaranteed baseline for your line configuration.
Q: Which stations are included and how is throughput balanced?
A: The line covers mixing, twin-screw extrusion, drying, grinding, blending, and packing. Each station is selected so its maximum throughput matches the extruder output tier you choose. The line layout document shows the capacity envelope at every station, eliminating bottlenecks before installation begins.
Q: What voltage and control options are available?
A: Voltage and frequency are configured to your site supply before production starts. The control system is available with PLC or MCC architecture, and the operator interface language is set to your preference. Confirming these details at the quotation stage prevents electrical rework after the line arrives.
Q: How much factory floor space does the line require?
A: The MT65 needs roughly 24 m by 1.2 m with 2.2 m clearance height, the MT70 extends to 26 m by 1.5 m, and the MT85 occupies 29 m by 3.5 m with 4.3 m height. These dimensions include all stations. We recommend sharing your column grid and overhead obstructions so the layout can be adjusted before final engineering.
Q: Are spare wear parts available with the first shipment?
A: A recommended first-order wear parts list — covering screws, dies, and mixer blades — is included with every quotation. Parts are manufactured in the same workshop and can be shipped with the line or sent separately on a schedule that matches your production ramp-up.