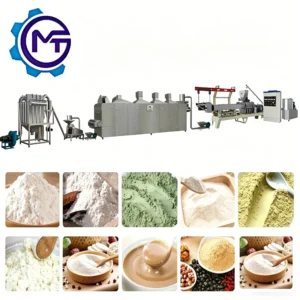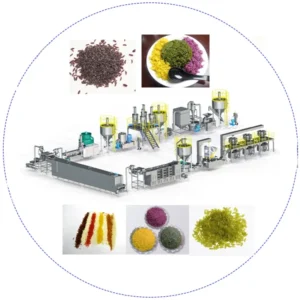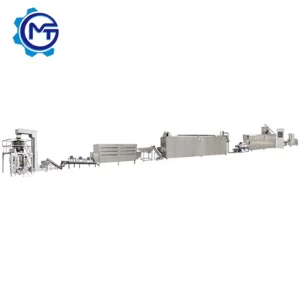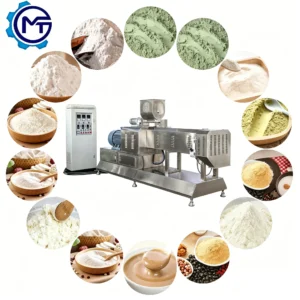
Matched Throughput Across Every Station — every unit from the twin-screw extruder through the drying and roasting ovens to the cooling and packing stations is sized as one set, eliminating the silent bottlenecks that cap line output below the quoted tonnage.
Technical Specifications
| Parameter | Value |
|---|---|
| Model | MT65 |
| Product Type | Fortified Rice Extruder Production Line |
| Screw Type | Twin screw |
| Installed Power | 85 kW (MT65) |
| Power Consumption | 60 kW (MT65) |
| Output Capacity | 80-100 kg/h (MT65, basis not stated in source — confirm raw material formulation and moisture content) |
| Overall Dimensions | 28 × 1.2 × 2.2 m (MT65) |
| Control System | Frequency speed controlling with high automation |
| Line Stations | Mixing → Extruding → Vibrating → Low temperature drying → Cooling → High temperature roasting → Cooling → Packing |
| Dryer Heating Source | Electric or gas |
| Dryer Feature | Circulation drying process with frequency motor-controlled mesh belt speed |
| Feeding System | Single or double screw feeding system selectable based on material |
| Assembly State | Complete production line |
| Certification | CE |
Application Suitability
| Application | Material or Output |
|---|---|
| Fortified food and nutrition programme supply | Vitamin- and mineral-enriched kernels from broken rice, corn, millet, wheat, oats, buckwheat, beans, and starch |
| Nutritional instant rice processing | Reconstituted grain blends formulated for rapid cooking and high dietary value |
| Artificial rice from grain by-products | Broken rice and rice bran converted into uniform, high-nutritional-value kernels |
| Snack and breakfast cereal producers expanding formats | Corn, millet, oats, or buckwheat bases shaped into extruded rice kernels |
Why the Dryer Matters More Than the Extruder Motor
An extruder sold with an undersized drying oven will quietly limit your entire line well below the rated tonnage, no matter how powerful the main motor is.
I have watched buyers focus every hour of negotiation on screw diameter and motor kilowatts, only to discover during commissioning that the drying mesh belt cannot keep up with the extruder’s output on their specific grain blend [NEED_CITE: thermal load calculations for grain-based extrusion lines]. The moisture has nowhere to go, kernels clump, and the line is manually throttled back. On a Fortified Rice Extruder Production Line, the low-temperature drying and high-temperature roasting stages are distinct stations precisely because moisture removal and final texture demand separate, controlled environments. When these stations are matched to the extruder at the design stage rather than bolted on as afterthoughts, the line holds its rated capacity on the buyer’s actual formulation.
Drying and Roasting as Separate Control Points
Low-temperature drying removes the bulk of the moisture added during extrusion without shocking the kernel surface, while high-temperature roasting develops the final colour, texture and cooking behaviour. Running both functions through a single oven forces a compromise that shows up as inconsistent kernel density across batches.
Frequency-Controlled Mesh Belt and Heating Options
The circulation drying oven uses a frequency motor-controlled mesh belt, allowing the residence time to be adjusted to the exact moisture profile of the formulation. Electric and gas heating sources are both available, and the choice affects both the line footprint and the utility infrastructure required at the buyer’s facility [NEED_CITE: industrial gas versus electric heating infrastructure requirements].
What Screw Configuration Means for Fortified Rice
The twin-screw design provides the shear and mixing intensity needed to fully gelatinise starches from broken rice, corn, and grain blends while evenly distributing vitamin and mineral pre-mixes. The screw configuration and die are specified to the buyer’s raw material, because a combination optimised for pure rice flour will behave differently when the formulation includes sticky starch binders or high-fibre bran additions.
Reading the Capacity Table Correctly
The output figures of 80-100 kg/h for the MT65, up to 800-1000 kg/h for the MT95, are tied to specific screw and motor combinations. These numbers assume a confirmed raw material formulation and moisture content; running a denser grain blend or a higher micro-nutrient loading can shift actual throughput. The line capacity calculation document shows the matched output across every station, so the bottleneck is visible before the line is built rather than discovered on the factory floor.
The Cost of Skipping the Trial Run
When a line ships without a test run on the buyer’s actual grain blend and pre-mix ratio, product development starts after installation, during commissioning, with a full production crew waiting. Screw combinations are swapped, die geometries are adjusted, and dryer settings are chased — all on the buyer’s timeline and budget [NEED_CITE: extrusion commissioning delays caused by untested formulations]. A trial run in the testing workshop on the customer’s raw material surfaces these issues before the equipment leaves the factory.
Why Procurement Teams Choose This Equipment Range
Every station from mixing through packing is supplied under one configuration, so throughput at the extruder, dryer, roasting oven, and cooling conveyor is balanced by design rather than negotiated separately with multiple vendors. The screw and die configuration record is written against the buyer’s specific raw material, not copied from a generic build. The in-house testing workshop allows trial runs on customer-supplied grain blends before shipment. Line layout and capacity calculation documents are provided so that utility planning, floor space allocation, and upstream ingredient handling can be finalised before production starts. The MT65 through MT95 series covers small-batch pilot production through to high-volume nutrition programme supply, letting buyers select the exact scale their market demands.
Documentation & Verification
- Line layout and capacity calculation showing matched throughput from mixer to packing station
- Machine specification sheet with screw and die configuration record for your grain formulation
- Electrical schematic with voltage and frequency confirmation for your market before production
- Trial run report on your raw material blend from the in-house testing workshop
- CE declaration of conformity and factory test record before dispatch
- Wear parts list covering screws, dies, and mesh belt sections
Installation, Commissioning & Support
- Floor space planning based on the line dimensions, starting at 28 × 1.2 × 2.2 m for the MT65
- Electrical supply sized to the installed power rating with dedicated circuits for each heating zone
- Frequency speed controlling system configured to the operator’s language before commissioning
- First-run parameter setting for drying temperature, mesh belt speed, and extruder screw speed on your formulation
- Operator training covering screw changes, die swaps, and mesh belt tension adjustment
- Spare wear parts package including replacement screw elements and die plates for initial production runs
Before You Request a Quote
Send the exact grain formulation, including the type and percentage of starch binders, micro-nutrient pre-mix loading, and target kernel dimensions. Confirm your facility’s voltage, frequency, and available floor length so the line layout can be drawn to scale. If your raw material blend is new or sourced locally, arrange a sample shipment for a trial run in the testing workshop before the configuration is locked.
Frequently Asked Questions
Q: How is actual line capacity verified on my specific grain formulation?
A: The quoted output figures assume a confirmed raw material and moisture content. A trial run using your grain blend and pre-mix ratio is conducted in the testing workshop, where extruder throughput, dryer residence time, and roasting oven capacity are measured together. The resulting trial run report documents the verified capacity across every station.
Q: Which stations are included and how is throughput matched between them?
A: The complete Fortified Rice Extruder Production Line covers mixing, extruding, vibrating, low-temperature drying, cooling, high-temperature roasting, a second cooling stage, and packing. Each station is sized so that its maximum handling rate meets or exceeds the extruder’s verified output on your formulation, preventing any single unit from silently capping production.
Q: What dryer heating source options are available and how do they affect planning?
A: Electric and gas heating sources are both available for the circulation drying oven. Gas heating typically requires external venting and a dedicated gas supply line, while electric heating draws from the main power distribution. The choice influences utility infrastructure, floor space allocation, and the electrical schematic prepared before production begins.
Q: Can the feeding system handle different raw materials like broken rice versus starch blends?
A: Single or double screw feeding systems are available and selected based on the flow characteristics of your material. Free-flowing broken rice grains feed consistently through a single screw system, while sticky starch blends or high-moisture pre-mixes typically require a double screw feeder to maintain uniform and stable material delivery to the extruder barrel.
Q: What voltage and control language options are confirmed before production?
A: Voltage, frequency, and control panel language are confirmed during the specification stage before the electrical schematic is finalised. This prevents commissioning delays caused by mismatched power supplies or control interfaces that operators cannot read, and it ensures the frequency speed controlling system is calibrated to the correct motor ratings for your market.