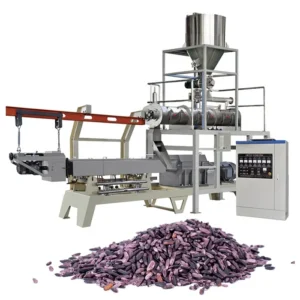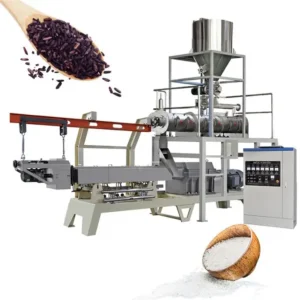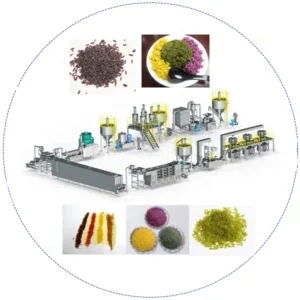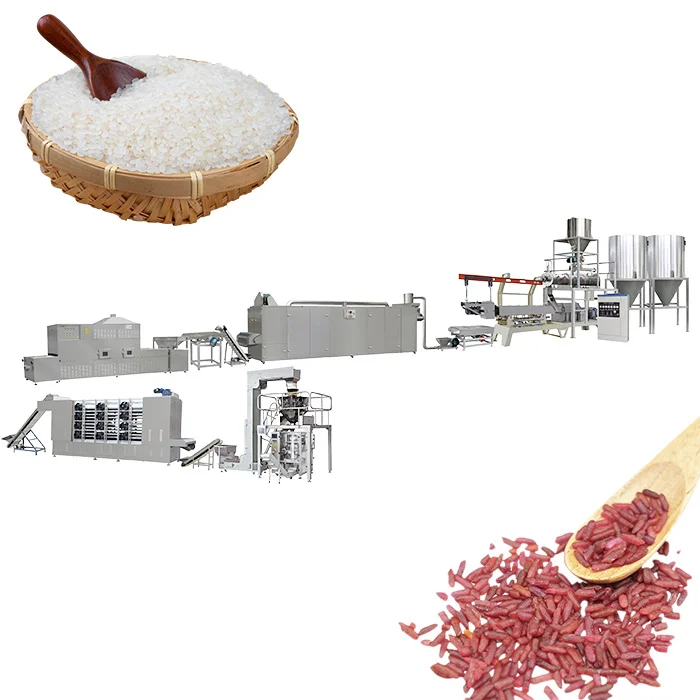
Full equipment matching — Throughput is calculated across every station from mixing to packing so the extruder, dryer, and roaster run at the same pace without one bottlenecking the rest of the line.
Technical Specifications
| Parameter | Value |
|---|---|
| Product Type | Nutritional Fortified Rice Processing Line |
| Model Range | MT65, MT70, MT85, MT75, MT95 |
| Extruder Type | Twin-screw |
| Line Stations | Mixing, Extruding, Vibrating, Low Temperature Drying, Cooling, High Temperature Roasting, Cooling, Packing |
| Feeding System | Single or double screw feeding system selected according to material |
| Screw Material | Wear-resistant special alloy |
| Control System | Frequency speed control, automated operation |
| Lubrication & Cooling | Automatic lubricating and cooling system |
| Basic Materials | Broken rice, rice, corn, millet, wheat, oats, buckwheat, bean, starch, vitamin, mineral |
| Final Products | Artificial rice, fortified rice kernels |
| Drying Oven Heating Source | Electric or gas |
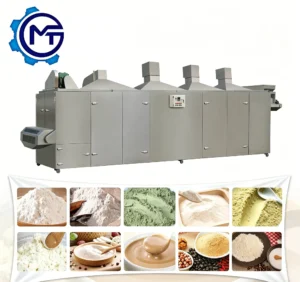
| Drying Oven Feature | Circulation drying process, frequency motor controls mesh belt speed |
| MT65 Installed Power | 85 kW |
| MT65 Power Consumption | 60 kW |
| MT65 Capacity | 80–100 kg/h (basis not stated in source — confirm raw material and moisture) |
| MT65 Size | 28 × 1.2 × 2.2 m |
| MT70 Installed Power | 120 kW |
| MT70 Power Consumption | 85 kW |
| MT70 Capacity | 100–120 kg/h (basis not stated in source — confirm raw material and moisture) |
| MT70 Size | 30 × 1.5 × 2.2 m |
| MT85 Installed Power | 235 kW |
| MT85 Power Consumption | 165 kW |
| MT85 Capacity | 200–300 kg/h (basis not stated in source — confirm raw material and moisture) |
| MT85 Size | 34 × 3.5 × 4.3 m |
| MT75 Installed Power | 180 kW |
| MT75 Power Consumption | 135 kW |
| MT75 Capacity | 300–500 kg/h (basis not stated in source — confirm raw material and moisture) |
| MT75 Size | 32 × 3.5 × 4.3 m |
| MT95 Installed Power | 260 kW |
| MT95 Power Consumption | 195 kW |
| MT95 Capacity | 800–1000 kg/h (basis not stated in source — confirm raw material and moisture) |
| MT95 Size | 36 × 3.5 × 4.3 m |
| Certifications | CE, ISO |
Application Suitability
| Application | Material or Output |
|---|---|
| Nutritional fortified rice production | Broken rice, rice bran, and cereal blends fortified with vitamins and minerals |
| Artificial rice kernel manufacturing | Rice flour, corn, millet, wheat, oats, and buckwheat mixtures |
| Fortified food programme supply | Vitamin and mineral-enriched grain kernels meeting nutritional standards |
| Cereal by-product upcycling | Broken rice and milling by-products converted into high-value nutritional rice |
| Turnkey artificial rice plant installation | Complete processing from raw grain batching through extrusion, drying, roasting, cooling, and packing |
Why Extruder Output Numbers Mislead Buyers Sourcing a Fortified Rice Processing Line Full Equipment Range
Capacity figures only mean something when tied to your exact raw material blend and moisture level.
Many equipment catalogues list a peak throughput based on standard white rice flour at ideal moisture. When a buyer switches to a blend heavy in coarse grains and micronutrient premix, the actual screw torque requirement changes entirely. The extruder may no longer hold that rated output, or the grain shape breaks apart at the die [NEED_CITE: twin-screw extrusion torque requirements for high-fiber grain blends]. A fortified rice processing line full equipment range must be evaluated on the material you actually plan to run, not the material the factory used for the brochure test.
Mapping Every Station in the Line
A complete nutritional powder processing line involves more than the extruder. The mixing station sets ingredient uniformity, the twin-screw extruder handles gelatinisation and shaping, the vibrating separator removes fines, the low-temperature dryer reduces moisture without cracking the kernels, the cooling conveyor stabilises the product, and the high-temperature roaster develops the final texture. Each station must be sized so material flows continuously without pile-ups or idle time. The fortified rice processing line full equipment range covers all these stations under one configuration.
Balancing Throughput Between Extrusion and Drying
The drying oven often becomes the constraint on an artificial rice line. Extrusion produces wet, soft kernels that must lose moisture evenly before roasting. If the mesh belt speed and oven length do not match the extruder output, kernels either exit too wet — causing deformation during cooling — or spend too long in the oven and crack. The circulation drying process with frequency-controlled belt speed allows the dryer to track the extruder rate [NEED_CITE: moisture reduction rates in multi-pass grain drying ovens]. This balancing is why sourcing the full equipment range from one supplier matters.
Reading the Specifications Against Your Raw Material
The five-model extruder series from MT65 to MT95 spans a wide capacity band, but the published kg/h values depend on raw material density and moisture content. A blend high in oat and buckwheat behaves differently under shear than pure rice flour, affecting both the power draw and the residence time inside the barrel. The wear-resistant special alloy screws handle abrasive mineral premixes that would degrade standard tooling. Frequency speed control on the main drive lets operators adjust screw RPM to compensate for seasonal raw material variation, keeping the kernel shape consistent across batches. The automatic lubricating and cooling system protects the gearbox during long production runs where micronutrient blends increase barrel friction.
What Happens When Stations Are Sourced Separately
Buyers who purchase an extruder from one vendor and a dryer from another often discover the throughput mismatch on commissioning day. The extruder pushes out more wet product than the dryer can handle, forcing the line to run below capacity. Alternatively, an oversized dryer wastes energy and floor space. Electrical incompatibilities between separately sourced machines also surface during installation, delaying startup [NEED_CITE: electrical integration challenges in multi-vendor food processing lines]. These hidden costs rarely appear in the initial quote comparison.
Why Procurement Teams Source the Complete Range Here
The testing workshop runs trial production on your actual raw material blend before the line ships, so screw configuration and die geometry are set to your formula rather than a generic rice flour standard. Line layout documents show throughput calculations at every station, confirming that the extruder, dryer, roaster, and packing system share a common capacity target. Single or double screw feeding systems are selected based on your ingredient flow characteristics rather than a default choice. Electrical schematics confirm voltage and frequency for your destination market before fabrication begins. The five-model extruder range means the line scales from pilot batches to full production volume within the same machine family.
Documentation & Verification
- Line layout showing matched throughput across mixing, extruding, drying, roasting, and packing stations
- Machine specification sheet with screw and die configuration recorded for your grain blend
- Trial run report using your actual raw material conducted in the testing workshop
- Electrical schematic with voltage, frequency, and control language confirmed for your market
- Wear parts list identifying screws, dies, and mesh belts with reorder codes
Installation, Commissioning & Support
- Floor plan with utility connection points matched to the installed power rating of your selected model
- Dedicated electrical circuit sizing based on the MT65 through MT95 power consumption specifications
- Modular station delivery allowing phased assembly in facilities with limited ceiling clearance
- First-run parameter setting on your raw material by commissioning engineers
- Operator training covering frequency speed control adjustment for different grain formulations
- Spare screw and die inventory planning aligned with your annual production schedule
Preparing Your Inquiry
When evaluating a fortified rice processing line full equipment range, share your raw material formula including grain types, vitamin premix ratios, and target moisture content. Specify the daily production volume and whether the facility runs single or multi-shift operations. Provide the local voltage and frequency standard along with the preferred control language for the HMI interface.
Frequently Asked Questions
Q: How is output capacity verified against my specific raw material blend?
A: Capacity is confirmed through a trial run in the testing workshop using your actual grain blend and micronutrient premix. The screw configuration, die geometry, and barrel temperature profile are adjusted until the extruded kernels meet shape and density targets. The resulting throughput figure is then documented in the trial report.
Q: Which stations are included, and how is throughput balanced between them?
A: The line includes mixing, twin-screw extruding, vibrating separation, low-temperature drying, cooling, high-temperature roasting, secondary cooling, and packing. Each station is sized so material flows at the same rate. The dryer mesh belt speed and oven length are calculated against the extruder output to prevent bottlenecks.
Q: What electrical configurations are available for different export markets?
A: Voltage and frequency are confirmed during the specification stage. The electrical schematic is prepared to match your facility’s power supply, whether that is 380V/50Hz, 440V/60Hz, or another industrial standard. Control panel labeling and HMI language are set before shipment.
Q: Can the feeding system handle high-fiber or coarse grain blends?
A: Yes. A single or double screw feeding system is selected based on your ingredient characteristics. Blends with high ratios of buckwheat, oats, or bran require consistent volumetric feeding to maintain extrusion stability. The system choice is documented in the line configuration proposal.