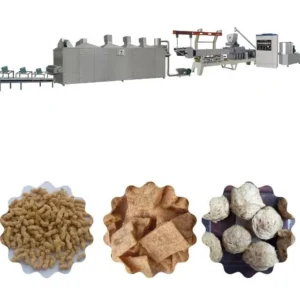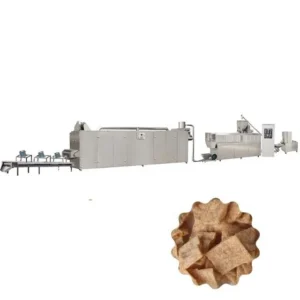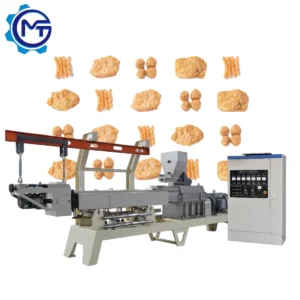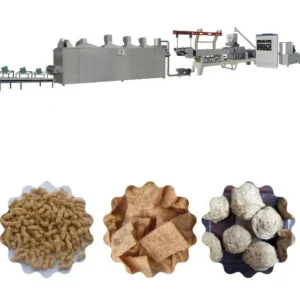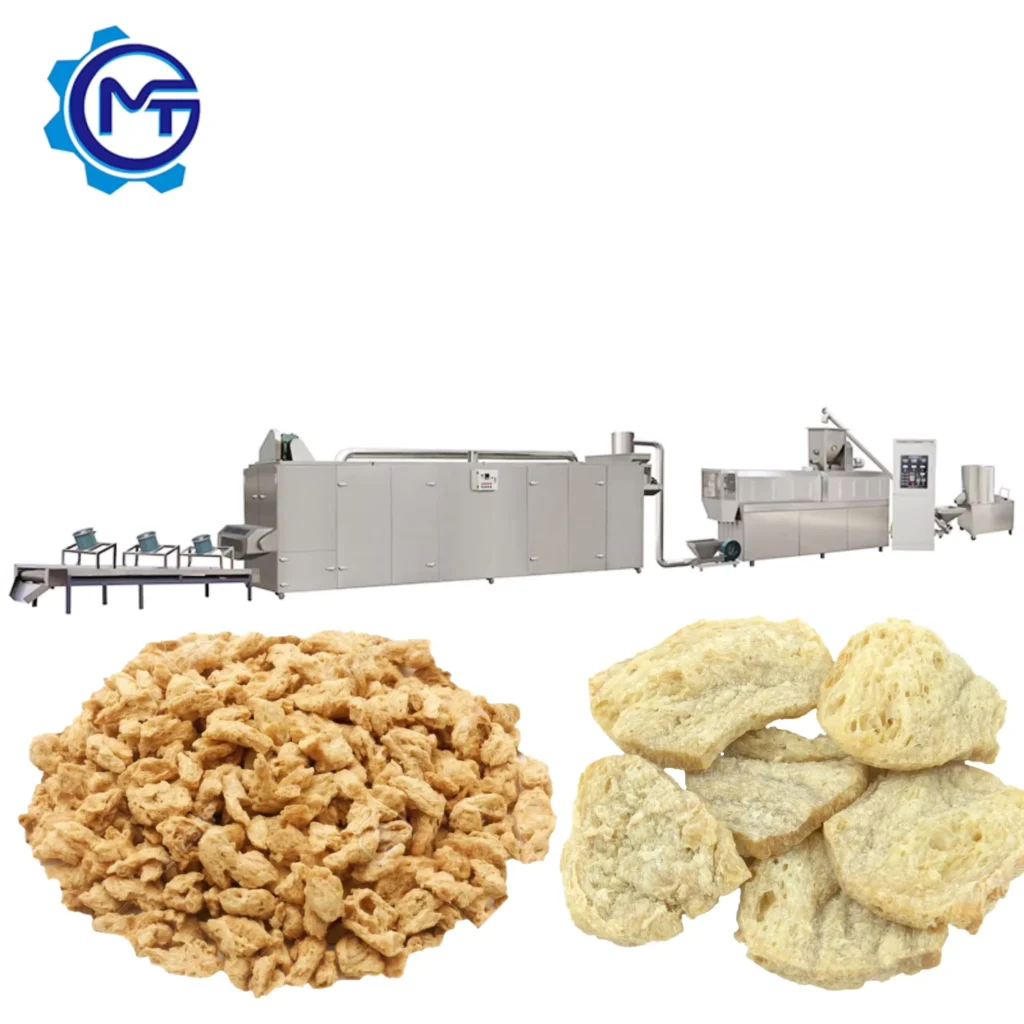
Throughput-Matched Stations — Every station from the vertical mixer through the multi-layer dryer is sized to the extruder’s actual output on your soy flour formulation, preventing the line bottlenecks that occur when stations are quoted in isolation.
Technical Specifications
| Parameter | Value |
|---|---|
| Product Type | Twin Screw Extruder Production Line for Textured Vegetable Protein (TVP/TSP) |
| Model Options | MT65 / MT70 / MT75 / MT85 |
| Screw Type | Twin Screw |
| Installed Power (MT65) | 84 kW |
| Installed Power (MT70) | 160 kW |
| Installed Power (MT75) | 190 kW |
| Installed Power (MT85) | 210 kW |
| Power Consumption (MT65) | 59 kW |
| Power Consumption (MT70) | 120 kW |
| Power Consumption (MT75) | 140 kW |
| Power Consumption (MT85) | 140 kW |
| Output Capacity (MT65) | 100–150 kg/h (basis to be confirmed against raw material formulation and moisture content) |
| Output Capacity (MT70) | 150–200 kg/h (basis to be confirmed against raw material formulation and moisture content) |
| Output Capacity (MT75) | 150–200 kg/h (basis to be confirmed against raw material formulation and moisture content) |
| Output Capacity (MT85) | 250–300 kg/h (basis to be confirmed against raw material formulation and moisture content) |
| Overall Dimensions (MT65) | 40000 × 1200 × 2200 mm |
| Overall Dimensions (MT70) | 41000 × 1500 × 2200 mm |
| Overall Dimensions (MT75) | 43000 × 1500 × 3200 mm |
| Overall Dimensions (MT85) | 45000 × 1500 × 3500 mm |
| Main Motor Power | 22 kW / 30 kW / 45 kW (mapped to model) |
| Rotary Cutting Motor Power | 0.75 kW |
| Feeding Motor Power | 0.75 kW |
| Heating Power | 10 kW / 14 kW (mapped to model) |
| Screw Length Options | 1050 mm / 1520 mm |
| Mixer Type | Vertical mixing machine with stainless steel 304 mixing ruler |
| Mixer Capacity | 20–30 kg / 70–80 kg / 170–180 kg (mapped to model) |
| Mixer Power | 4 kW / 7.5 kW / 15 kW (mapped to model) |
| Dryer Drive | Double pitch roller chain drive, round-trip drying |
| Dryer Fuel Options | Fuel, gas, or electricity (customer selectable) |
| Control System | PLC and MCC control |
| Contact Materials | Food-grade throughout |
| Line Stations | Mixer → Screw Conveyor → Twin Screw Extruder → Air Conveyor → Multi-layer Dryer → Cooling Machine |
| Certification | CE, ISO |
Application Suitability
| Application | Material or Output |
|---|---|
| Textured vegetable protein (TVP/TSP) chunks | Defatted soy flour, low-temperature soy flakes |
| Soy meat analogues and nuggets | Soy protein concentrate, soy protein isolate blends |
| Meat substitutes for frozen food production | TVP granules and strips rehydrated for forming |
| Plant-based protein snacks | High-protein extruded formats from soy and pea blends |
| Cereal and snack formats (via configuration change) | Corn grits, rice flour, oat blends with adjusted screw profile |
Why Nominal Output Figures Mislead Buyers on Protein Lines
A twin screw food extruder for sale quoted at a round-number capacity rarely holds that throughput on your specific defatted soy flour blend and moisture target.
Buyers routinely compare extruder models on a single output number without asking what raw material, moisture level, or chunk size that number assumes. Defatted soy flour behaves very differently from corn starch under shear and heat. A line rated for a starch-heavy formulation will slow down or produce inconsistent fiber structure when switched to high-protein soy material. The extruder barrel, screw pitch, and die opening all interact with the material’s viscosity profile, and a mismatch in any one of them forces the operator to reduce feed rate to maintain product quality [NEED_CITE: twin screw extrusion behavior on high-protein versus high-starch formulations].
Screw Configuration and Fiber Structure Control
The twin screw food extruder for sale in this line is available with screw lengths of 1050 mm or 1520 mm, and the selection directly affects residence time and shear history inside the barrel. Longer screws give the protein more time to align and form the layered fiber structure that TVP requires, while shorter screws suit products where less structural development is needed. The die design is matched to the target chunk size and shape, whether that is a small granule for rehydration or a larger nugget for direct use in prepared meals.
Dryer Matching and Moisture Removal
The multi-layer dryer in this line uses a double pitch roller chain drive with round-trip drying to keep the extruded TVP moving through controlled temperature zones. Drying is where many lines fail to keep pace with the extruder, because protein-rich extrudate holds moisture differently than starch-based snacks. The dryer fuel source is configurable to electricity, gas, or liquid fuel, which matters for sites where one energy source is significantly cheaper or more reliable than another [NEED_CITE: industrial dryer energy source selection for food processing facilities].
Key Parameters That Shape TVP Output
The installed power ranges from 84 kW on the MT65 to 210 kW on the MT85, and this envelope covers the mechanical and thermal energy needed to gelatinize starch and denature protein simultaneously inside the barrel. The main motor options at 22 kW, 30 kW, and 45 kW drive the screw rotation, and the selection determines the maximum torque available when processing viscous high-protein doughs. Heating power at 10 kW or 14 kW maintains barrel temperature zones, which must be precise because soy protein denatures within a narrow temperature window. The vertical mixer capacity, mapped at 20–30 kg up to 170–180 kg per batch, must align with the extruder’s hourly feed rate so that mixing does not become the rate-limiting step. Overall line dimensions reach up to 45000 mm in length, which means the installation site must accommodate a continuous linear footprint with access on both sides for maintenance.
What Happens When Line Stations Are Not Balanced
When an extruder is purchased separately and paired with a dryer or mixer from a different vendor, throughput mismatches appear at commissioning. The extruder may push out more wet extrudate than the dryer can handle in a single pass, forcing the operator to either slow the extruder or accept product with residual moisture that shortens shelf life. Similarly, a mixer that batches too slowly creates idle time on the extruder, and frequent start-stop cycles degrade screw and barrel wear life. These imbalances are not visible in individual machine specifications but emerge only when the full line runs together [NEED_CITE: throughput mismatch causes in multi-station food extrusion lines].
Why This Line Configuration Works
The complete station sequence from mixer through cooling machine is configured under one supplier, so each piece of equipment is selected to match the extruder’s actual output on soy-based formulations. The twin screw food extruder for sale here is specified with screw and die geometry matched to your target TVP fiber structure, not copied from a generic snack build. The PLC and MCC control system manages the entire line from a single interface, which means temperature, feed rate, and dryer speed are coordinated rather than adjusted independently on separate panels. Food-grade contact materials are used at every station where product is exposed, meeting the sanitation expectations of food safety audits. In-house trial runs on your actual defatted soy flour are conducted before shipment, so screw configuration and process parameters are validated before the line arrives at your facility [NEED_CITE: food-grade material requirements for extrusion equipment in protein processing].
Documentation & Verification
- Line layout showing throughput calculations for each station against your soy flour formulation
- Screw and die configuration record specifying pitch, flight depth, and die opening for your target chunk size
- Electrical schematic with voltage and frequency confirmed for your destination market
- Trial run report documenting actual throughput and product quality on your raw material
- Factory test record with photographs before crating and dispatch
- Wear parts list identifying screws, dies, and cutting blades with replacement intervals
Installation, Commissioning & Support
- Foundation plan specifying load points for the extruder and dryer based on line dimensions up to 45000 mm
- Electrical connection schedule detailing the installed power requirement from 84 kW to 210 kW per model
- On-site assembly of the multi-layer dryer and conveyor sections that ship in modular segments
- Commissioning with screw configuration fine-tuning against your actual defatted soy flour batch
- Operator training covering PLC interface navigation, temperature zone adjustment, and emergency stop procedures
- Wear parts inventory including replacement screws and die plates supplied with initial shipment
What We Need to Specify Your Line
To configure the right model and station balance, share your raw material type and supplier data sheet, the target TVP chunk dimensions and rehydration behavior you need, and your daily production target in kilograms. Include your site’s available voltage and frequency, the fuel source you prefer for the dryer, and the dimensions of the production hall so we can confirm the line footprint fits with maintenance access on both sides.
Frequently Asked Questions
Q: How do you verify the actual output capacity before shipment?
A: We run your specific defatted soy flour formulation through the twin screw food extruder for sale in our in-house testing workshop. The trial documents actual throughput, product density, fiber structure, and moisture content at the dryer exit. This report ships with the line so you have a baseline for comparison during your own commissioning.
Q: What determines which screw length and die configuration the line uses?
A: The screw length of 1050 mm or 1520 mm and the die opening geometry are selected based on your target TVP chunk size and the protein content of your raw material. Higher protein flours generally require longer residence time and specific shear profiles to develop the correct fiber layering.
Q: How is the electrical system adapted for different export markets?
A: Voltage, frequency, and control language are confirmed before production begins. The PLC and MCC panels are wired to match your site’s supply, and all labels and HMI text are set in the language your operators will use during daily production and troubleshooting.
Q: Which components require regular replacement and how are they supplied?
A: The primary wear parts are the extruder screws, die plates, and rotary cutting blades. A complete wear parts list is provided with the first shipment, and replacement components are manufactured to the same specification as the originals so they fit without modification when the first changeover is due.