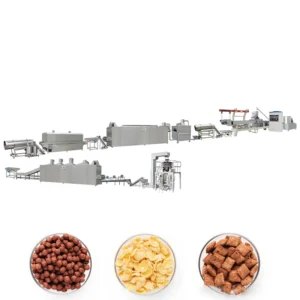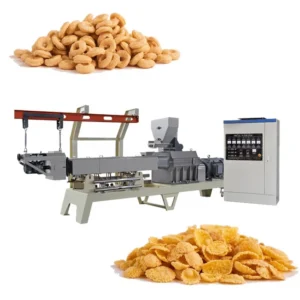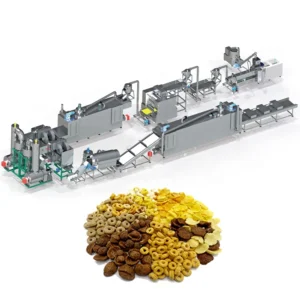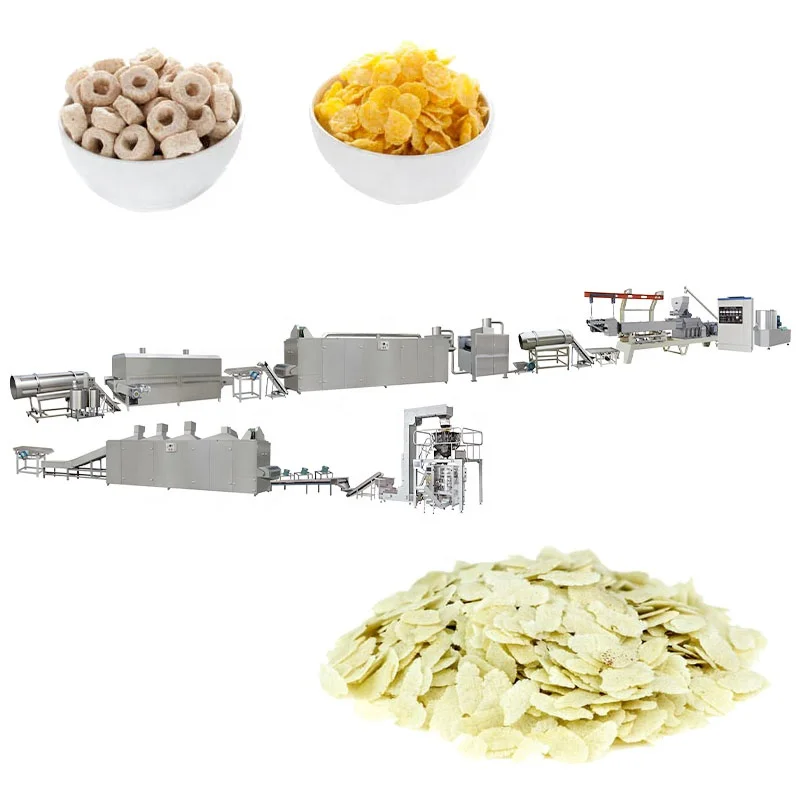
Integrated Flaking and Roasting Stations — The corn flakes production line balances extruder output with downstream drying, flaking, and roasting capacity so no single station bottlenecks the entire run.
Technical Specifications
| Parameter | Value |
|---|---|
| Product Type | Corn Flakes Production Line |
| Screw Type | Twin Screw |
| Installed Power | 160 kW (MT70); 190 kW (MT85); 210 kW (MT75) |
| Power Consumption | 120 kW (MT70); 140 kW (MT85); 150 kW (MT75) |
| Capacity | 150–200 kg/h (MT70, basis to be confirmed); 300–400 kg/h (MT85, basis to be confirmed); 300–500 kg/h (MT75, basis to be confirmed) |
| Overall Dimensions | 41 × 1.5 × 2.2 m (MT70); 43 × 1.5 × 3.2 m (MT85); 45 × 1.5 × 3.5 m (MT75) |
| Control System | PLC with MCC integration |
| Extruder Working Principle | Feeding, extruding, cutting, heating, gearing, and controlling systems |
| Dryer Heating Source | Gas or Electric |
| Flaking Machinery | Hydraulic double-roller system, separate motor drives, infrared temperature control |
| Hot Air Roasting Oven | Vibrating pan, dual circulating fans, cyclone dust removal |
| Coating System | Double tumble sugar melting, elevator, coating drum, spraying nozzle |
| Certification | CE, ISO |
Application Suitability
| Application | Material or Output |
|---|---|
| Natural corn flakes production | Corn, rice, wheat, oat, and barley powder blends |
| Sugar-coated breakfast cereals | Corn grits with sugar syrup coating and drying |
| Multi-shape cereal formats | Ball, tube, stick, ring, fruit loop, star, wheel, flower, and heart shapes via die changes |
| Fortified breakfast cereal lines | Grain powder blends with added vitamin and mineral premixes |
What Nominal Capacity Figures Leave Out on a Corn Flakes Line
A line rated at a certain throughput on standard corn grits may stall when your actual raw material carries a different moisture or fat profile.
I worked on a corn flakes project where the extruder ran fine during our workshop trial using standard corn flour. When the buyer switched to their local supplier’s corn grits, which had a noticeably higher fat content, the dough would not gelatinize properly. The flakes came out dense and the roasting oven could not achieve the surface bubbling the market expected. We had to reconfigure the screw elements and adjust the barrel temperature zones to match that specific formulation [NEED_CITE: effect of fat content on starch gelatinization in twin-screw extrusion]. This is why verifying capacity against the buyer’s actual raw material matters more than the number on a quotation.
How Each Station Connects to the Next
The corn flakes production line full equipment range moves material through mixing, extruding, flaking, drying, hot air roasting, cooling, and packing. When the extruder pushes output beyond what the flaking rollers can press, half-cooked dough piles up upstream. When the roasting oven lacks the airflow to handle the volume, flakes exit under-toasted and lose crispness within hours. Matching throughput at every transfer point prevents these pile-ups and keeps product quality stable across long runs.
Flaking and Roasting Determine Final Texture
The flaking machinery uses a hydraulic double-roller system with separate motors driving each roller. Infrared sensors monitor roller temperature so the dough sheet maintains consistent thickness entering the dryer. Downstream, the hot air roasting oven relies on a vibrating pan and two circulating fans to move heated air evenly across the flake bed [NEED_CITE: convective heat transfer principles in vibrating bed roasters]. A cyclone dust removal device pulls fine particles out of the airstream, preventing scorch marks on the flake surface.
Reading the Specs That Matter
The installed power across the MT70, MT85, and MT75 models ranges from 160 kW to 210 kW, with actual power consumption between 120 kW and 150 kW depending on the model. This gap between installed and consumed power reflects the thermal and mechanical load during steady-state extrusion. The twin-screw design gives operators control over residence time and shear intensity by adjusting screw element arrangement — a factor that directly affects starch gelatinization degree and, ultimately, flake crispness after roasting. The PLC control system stores recipes for different grain blends, reducing batch-to-batch variation when switching between corn, oat, and wheat formulations.
The Cost of Mismatched Downstream Equipment
When a buyer sources the extruder from one vendor and the roasting oven from another, the two machines rarely communicate their operating states. If the extruder ramps up but the oven temperature lags, the flakes pass through under-roasted and go stale before reaching the packing station [NEED_CITE: moisture migration in under-roasted cereal flakes]. I have seen lines where the coating drum capacity was half what the extruder produced, forcing the operator to run the front end at reduced speed and lose the efficiency the line was purchased for.
Why Source the Full Range from One Build
Every station on this corn flakes line is sized against the others during the layout phase. The flaking rollers, dryer belt width, roasting oven bed area, and coating drum volume are all calculated from the extruder model chosen for your target output. Screw configuration and die design are specified to your raw material formulation, not pulled from a generic template. Before shipment, the line can run a trial using your actual grain blend in the testing workshop, so adjustments happen before installation rather than during commissioning. The MCC and PLC control architecture is built in-house, meaning electrical schematics and programming logic stay consistent across every station.
Documentation & Verification
- Line layout drawing showing station spacing and throughput balance for your selected model
- Screw and die configuration record matched to your grain blend formulation
- Trial run report on your raw material with moisture and density readings
- Electrical schematic with voltage and frequency confirmed for your facility
- CE declaration of conformity and ISO certificate for customs clearance
- Wear parts list covering screws, dies, and flaking roller surfaces
Installation, Commissioning & Support
- Foundation plan based on the 41–45 m line length with leveling points at each station
- Dedicated power circuit sized for up to 210 kW installed load with MCC panel integration
- Flaking machinery hydraulic system filled and pressure-tested during on-site commissioning
- PLC recipe programming for your grain formulation with operator language set before training
- Spare screw elements and die plates supplied with a replacement schedule based on run hours
- Roasting oven burner calibration and airflow balancing performed during first production run
Preparing Your Inquiry
To configure a corn flakes line that holds its rated throughput, share your primary grain type, typical moisture content at the mixer, and target hourly output. Include your facility voltage and frequency, available floor length, and whether you need the natural line or the sugar-coated variant. If you can send a sample of your raw material, we can run it through the testing workshop and return a trial report with the proposed screw and die setup.
Frequently Asked Questions
Q: How is line capacity verified against my specific corn grits or grain blend?
A: We run your raw material through the extruder in our testing workshop, recording moisture content, barrel temperature profile, and flake density at each stage. The trial report documents the output rate achieved on your formulation, and any screw or die adjustments made during the test are carried into the final build specification before the line ships.
Q: Are the dryer, flaking, and roasting stations throughput-matched to the extruder I select?
A: Yes. The belt width on the dryer, roller diameter on the flaking machine, and bed area in the roasting oven are all calculated from the extruder model’s verified output on your material. This prevents bottlenecks where one station forces the entire line to run below its designed capacity.
Q: What electrical and control details are confirmed before the line is built?
A: We confirm your facility voltage, frequency, and phase configuration, then produce an electrical schematic and MCC panel layout accordingly. The PLC interface language is set to match your operators, and all motor ratings and heater elements are specified for your local power standard before production begins.
Q: Can I send raw material for a trial run before the line ships?
A: You can send a batch of your grain blend to our testing workshop. We extrude, flake, and roast it using the proposed screw configuration and die design, then share the trial report with you. Any configuration changes identified during the trial are incorporated into the final machine build at no extra design cost.
Q: What spare wear parts come with the line and when do they need replacing?
A: The initial supply includes spare screw elements, die plates, and flaking roller surface inserts. Replacement timing depends on your grain abrasiveness and daily run hours. The wear parts list documents each component with estimated service intervals based on standard corn and wheat formulations.