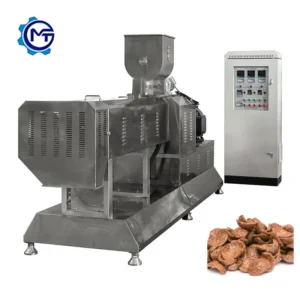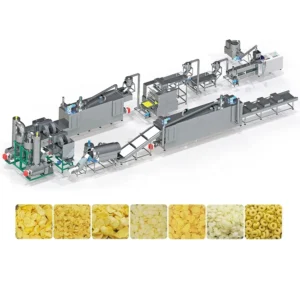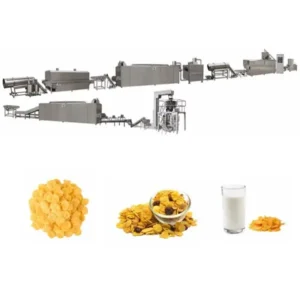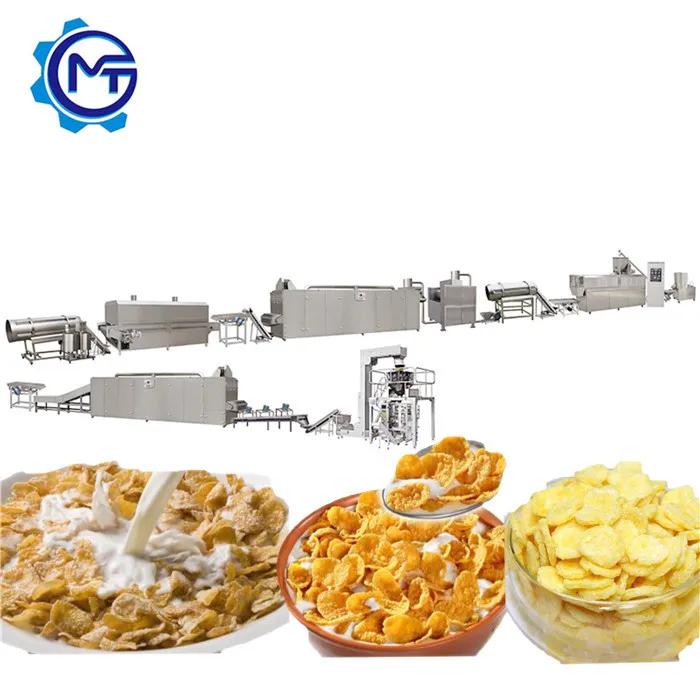
Integrated Line Matching — Every station from the twin-screw extruder through the flaking machine, roasting oven, and coating drum is sized to the same throughput basis, eliminating the bottlenecks that arise when equipment is sourced from separate vendors.
Technical Specifications
| Parameter | Value |
|---|---|
| Product Type | Corn Flakes Production Line (Twin Screw Extrusion) |
| Available Models | MT70 / MT75 / MT85 |
| MT70 Installed Power | 160 kW |
| MT70 Power Consumption | 120 kW |
| MT70 Capacity | 150–200 kg/h (basis not stated in source — confirm raw material formulation / moisture content) |
| MT70 Overall Dimensions | 41 × 1.5 × 2.2 m |
| MT75 Installed Power | 210 kW |
| MT75 Power Consumption | 150 kW |
| MT75 Capacity | 300–500 kg/h (basis not stated in source — confirm raw material formulation / moisture content) |
| MT75 Overall Dimensions | 45 × 1.5 × 3.5 m |
| MT85 Installed Power | 190 kW |
| MT85 Power Consumption | 140 kW |
| MT85 Capacity | 300–400 kg/h (basis not stated in source — confirm raw material formulation / moisture content) |
| MT85 Overall Dimensions | 43 × 1.5 × 3.2 m |
| Extruder Type | Twin Screw |
| Flaking Machine | PLC-controlled, hydraulic double rollers, dual-motor independent drive, infrared sensor temperature regulation |
| Flaking Machine Capacity | 200–300 kg/h (basis not stated in source — confirm flake thickness target / moisture content) |
| Dryer Heating Source | Gas or Electric |
| Hot Air Roasting Oven | Vibrating pan, dual circulating fans, conciliation burner, cyclone dust removal |
| Coating System | Double tumble sugar melter, elevator, coating drum, spraying nozzles |
| Control System | PLC on flaking machine; line-wide control configurable (PLC or MCC) |
| Raw Materials | Corn, rice, wheat, oat, barley powders |
| Product Shapes | Ball, tube, stick, ring, fruit loop, star, wheel, flower, heart (via die change) |
| Voltage & Frequency | Customized to local supply requirements |
| Certifications | CE; ISO |
Application Suitability
| Application | Material or Output |
|---|---|
| Natural corn flakes | Corn grits or corn flour, extruded, flaked, roasted |
| Sugar-coated breakfast cereal | Corn, rice, or wheat base with sugar glaze or honey coating |
| Multi-grain cereal flakes | Blends of oat, barley, wheat, and rice powders |
| Shaped cereal pieces | Fruit loops, stars, rings, wheels via interchangeable extruder dies |
| Fortified breakfast cereal | Grain base with added vitamin and mineral premix |
What "Rated Capacity" Leaves Out on a Corn Flakes Line
A line rated at a nominal output will only hold that figure if the screw configuration, dryer length, and flaker throughput are all matched to your actual recipe and moisture profile.
I have watched buyers specify a corn flakes machine full equipment range based on a catalog number, only to find that their formulation — perhaps a higher sugar ratio or a different starch source — produces a stickier extrudate that jams the flaking rollers or overloads the dryer. The extruder may be pushing material at nameplate volume, but the downstream stations cannot keep up. [NEED_CITE: relationship between starch gelatinisation degree and extrudate stickiness in twin-screw processing]
The breakfast cereal processing line equipment you survey on this page is configured so that every station — mixing, extruding, flaking, drying, roasting, coating — is balanced to the same material flow rate under a defined set of recipe conditions. Before any equipment leaves the factory, we run a trial on your actual raw material to confirm that the throughput holds end-to-end.
Matching Every Station from Mixer to Packer
When you evaluate a corn flakes machine full equipment range, the extruder is only one link. The mixing system must deliver a consistent moisture distribution before material enters the barrel. The pre-dryer must reduce surface stickiness enough for the flaking rollers to compress without adhesion. The hot air roasting oven must deliver the precise thermal profile that creates the surface blistering and crispness the market expects.
Each of these stations is specified here with its throughput relationship to the extruder clearly defined, so that a buyer surveying the catalogue can see where each machine fits and why its capacity matters relative to the others.
How the Flaking Machine Integrates Upstream and Downstream
The flaking machine is where extruded pellets become recognizable corn flakes. This unit uses a PLC-controlled hydraulic system to press the rollers together at a consistent gap, producing uniform flake thickness across the full roller width. Dual independent motors drive each roller separately, preventing the speed differential that causes uneven compression. [NEED_CITE: effect of flake thickness variation on roasting uniformity and final product texture]
An infrared sensor monitors the temperature of the feed pipe, ensuring the extrudate arrives at the rollers at the correct plasticity. If the material is too cool, it shatters; too hot, and it smears. This station sits between the pre-dryer and the hot air roasting oven, and its output rate must match both.
Reading the Spec Sheet Against Your Recipe
The twin-screw extruder at the core of this line relies on screw configuration and barrel temperature profiling to control starch gelatinisation, expansion, and moisture loss inside the barrel. A screw combination designed for a low-sugar corn grit recipe will behave differently when asked to process an oat-heavy blend with added sweetener. The long-diameter ratio of the barrel determines residence time, which directly affects how completely the starch cooks.
Die design controls the shape and density of the extrudate before it reaches the flaker. A ring-shaped die produces a different compression behaviour on the flaking rollers than a solid pellet die. The PLC on the flaking machine allows real-time gap and pressure adjustment, but the extruder screw profile must already be delivering a consistent feed. Moisture content entering the extruder and leaving the pre-dryer together define the window in which the flaker can operate without blockage or flake breakage.
The Hidden Cost of Mismatched Supporting Equipment
An extruder that outpaces its dryer forces operators to slow the entire line or accept flakes that retain too much internal moisture, leading to sogginess after packing. A coating drum that is undersized relative to the roaster output causes sugar buildup and uneven coverage, which triggers reject rates on the packing line. [NEED_CITE: consequences of throughput mismatch between extrusion and drying stations in cereal lines]
These failures do not show up in a specification sheet that lists only nominal capacities. They appear weeks after commissioning, when the buyer realises the line cannot sustain the output they planned their business case around.
Why Source the Full Range from One Supplier
The breakfast cereal processing line equipment shown here is built around a single throughput calculation, so the mixer batch size, extruder output, dryer residence time, roaster belt speed, and coating drum volume all reference the same material flow. Screw and die configurations are specified to your raw material formulation, not copied from a generic build.
An in-house testing workshop allows trial runs on your actual corn, rice, or multi-grain blend before the equipment ships, confirming product texture and line balance. Voltage, frequency, and control language are confirmed during the specification phase so that electrical schematics match your facility’s utility supply. Documentation covers every station from batching to packing, and on-site commissioning includes operator training on the full sequence.
Documentation & Verification
- Line layout drawing showing every station from mixer to packer with throughput balance
- Screw and die configuration record matched to your raw material formulation
- Trial run report on your actual corn or multi-grain recipe before dispatch
- Electrical schematic with confirmed voltage, frequency, and control language
- Operation and maintenance manual covering each station in the line
Installation, Commissioning & Support
- Foundation and floor space planning based on the chosen model’s overall dimensions, up to 45 m line length
- Dedicated electrical circuits sized to the selected extruder’s installed power, up to 210 kW
- Modular station delivery with sequenced assembly from mixer through packing conveyor
- First-run parameter setting on extruder barrel zones, flaker roller gap, and roaster temperature profile
- Operator training on PLC interface, die changeover, and screw cleaning procedures
- Wear parts inventory including spare screw elements, die plates, and flaker roller surfaces
Preparing Your Inquiry
To configure a breakfast cereal processing line equipment proposal that holds up under your actual production conditions, share your target product format — natural flake, sugar-coated, or shaped piece — along with your raw material formulation and moisture content. Include your facility’s available floor space, ceiling height, and local voltage and frequency. If you have existing upstream or downstream equipment that must integrate, note those station capacities as well.
Frequently Asked Questions
Q: How is throughput matched across every station to prevent bottlenecks?
A: Each station — extruder, pre-dryer, flaking machine, roasting oven, coating drum — is sized against the same material flow calculation derived from your target output and recipe. During the proposal stage, a capacity table is provided showing the rated flow at each station, so you can verify that no single machine constrains the others.
Q: What supporting equipment stations are included between the extruder and packing?
A: Between the twin-screw extruder and the packing station, the line includes a pre-dryer to reduce surface moisture and prevent sticking, a flaking machine for sheet compression, a hot air roasting oven for final crisping and surface blistering, and — for sweetened products — a sugar melting and coating system with tumble drum and spraying nozzles.
Q: How does the flaking machine integrate with upstream and downstream capacity?
A: The flaking machine receives pre-dried extrudate at a controlled temperature regulated by its infrared sensor, and its PLC-controlled hydraulic rollers compress the material at a set gap. Its output rate is matched to the roasting oven belt speed and the coating drum volume, ensuring continuous flow without accumulation or starvation at either interface.
Q: What voltage and control options are available for the complete line?
A: Voltage and frequency are configured to your facility’s local supply during the specification phase. The flaking machine uses PLC control, and the broader line can be specified with either PLC or MCC control systems. Control language and electrical schematics are confirmed before production begins to avoid delays at commissioning.
Q: Can individual stations be ordered separately or only as a full line?
A: Individual stations such as the flaking machine or hot air roasting oven can be supplied independently, though throughput matching is most effective when the full sequence is specified together. When integrating a single station into an existing line, share your upstream and downstream equipment capacities so the unit can be configured accordingly.