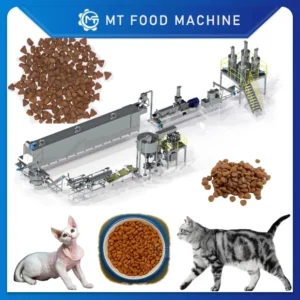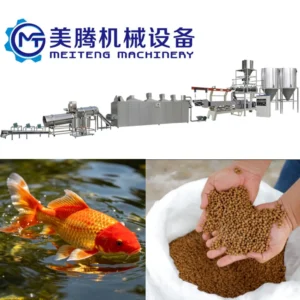
Throughput-Matched Line Design — Every station from batching to packing is sized against the extruder’s real output on your raw material, not a generic nameplate figure.
Technical Specifications
| Parameter | Value |
|---|---|
| Product Type | Twin Screw Pet Food Extrusion Line |
| Output Capacity | Up to 3 tons per hour (basis not stated in source — confirm raw material formulation, moisture content, and kibble size) |
| Screw Type | Twin-screw |
| Target Applications | Dry dog food, cat food kibble, fish feed |
| Warranty | 1 year (full line) |
| Process Documentation | Process flow drawing included |
| Standards & Certification | CE, ISO |
| Control System | Available with PLC or MCC control (confirm before production) |
| Voltage & Frequency | Configurable to destination market (confirm before production) |
| Line Stations Scope | Batching, extrusion, drying, coating, cooling, packing (confirm scope per project) |
Application Suitability
| Application | Material or Output |
|---|---|
| Dry dog food kibble | Corn, meat meal, bone meal, vitamin premix blends |
| Dry cat food kibble | High-protein formulations with fresh meat inclusion |
| Floating and sinking fish feed | Fish meal, soybean meal, starch binders for aquaculture operations |
Why "3 Tons per Hour" Means Nothing Without the Raw Material Recipe
A quoted capacity holds only when the screw configuration, barrel temperature profile, and die design match the buyer’s exact formulation.
I have watched a line rated at a respectable output collapse the moment the customer switched from a corn-heavy recipe to a high fresh-meat formula. The extruder simply could not handle the fat content and moisture differential, and what came off the die was unusable mush for the first three days. The pet food making machine full equipment range must be specified against the actual raw material the buyer intends to run, including moisture percentage, fat content, and protein ratio, otherwise the number on the quotation is decorative [NEED_CITE: twin-screw extrusion behavior across varying fat and protein formulations].
How Each Station Connects to the Next
The extruder does not work in isolation. If the dryer cannot remove moisture fast enough, kibble enters the coating drum too wet and the fat spray will not adhere. If the coating drum is undersized, seasoned product backs up and forces the extruder to slow down. When sourcing the pet food making machine full equipment range, every station — mixing, extrusion, drying, flavouring, cooling, packing — must be calculated against the same throughput target so that no single unit becomes the constraint on the others.
What the Process Flow Drawing Actually Tells You
Before any metal is cut, a process flow drawing shows the material path from raw ingredient intake through every conveying point, temperature zone, and discharge gate. This drawing is where throughput mismatches surface on paper instead of on the factory floor. Reviewing it with the supplier before production lets you verify that conveyor belt widths, dryer bed lengths, and drum volumes all align with the extruder’s output on your specific recipe [NEED_CITE: pet food production line layout engineering standards].
Screw Geometry, Barrel Zones, and the Die That Shapes the Kibble
Twin-screw extrusion gives operators independent control over shear, residence time, and temperature across multiple barrel zones. The screw configuration — the sequence of conveying, kneading, and reverse elements — determines how thoroughly starch gelatinises and how uniformly protein denatures inside the barrel. The die plate at the discharge end defines kibble shape and size, and its open area must be matched to the extruder’s volumetric output so that back-pressure stays within the range that produces consistent expansion. A die that is too restrictive will cause surging; one that is too open will yield under-expanded, dense kibble that sinks when it should float or breaks during transport. The L:D ratio and screw diameter together set the residence time available for cooking, and changing either one alters the degree of gelatinisation achievable at a given throughput.
What Happens When Stations Are Mismatched
A dryer that is one size too small will leave residual moisture above the safe storage threshold, inviting mould growth inside the bag within weeks. An undersized coating drum cannot tumble the kibble long enough for even fat distribution, producing batches with inconsistent palatability that trigger customer complaints. These failures rarely show up during a short factory acceptance test — they emerge after sustained production runs when the cumulative bottleneck forces unplanned stops and scrap [NEED_CITE: post-commissioning throughput losses in extrusion-based food lines].
Why the Equipment Range Matters from One Source
Sourcing every station from a single supplier means the line layout is engineered as one system rather than a collection of standalone machines bolted together. The screw and die configuration is specified to the buyer’s raw material and target kibble density, not copied from a generic build. An in-house testing workshop allows trial runs on the customer’s actual recipe before shipment, catching formulation-related issues early. Pre-sales consultation extends through engineer design, on-site installation, commissioning, and ongoing maintenance, keeping one accountable party responsible for the entire line’s performance.
Documentation & Verification
- Line layout and capacity calculation showing throughput at every station
- Screw and die configuration record matched to your raw material formulation
- Electrical schematic with voltage and frequency confirmation for your facility
- Trial run report on your actual recipe conducted before dispatch
- Operation and maintenance manual covering every station in the line
Installation, Commissioning & Support
- Foundation and floor space planning based on the confirmed line layout and station footprint
- Dedicated electrical circuit sized to the extruder main motor and dryer heating load
- Sequential station commissioning starting from batching through to packing
- Operator training on screw speed, barrel temperature, and moisture adjustment for your recipe
- Wear parts list with screw elements, die plates, and dryer belt spares identified before first production run
- Scheduled maintenance intervals documented per station for belt tension, bearing lubrication, and electrical inspection
What We Need Before Quoting Your Line
Share your target kibble shape, size, and density specification along with the raw material formulation you plan to run, including moisture and fat percentages. Confirm your facility’s voltage, frequency, and preferred control language so the electrical package is correct from the start. Let us know whether you need the full pet food making machine full equipment range from batching to packing, or only specific stations to integrate with existing equipment.
Frequently Asked Questions
Q: What does the full equipment range include beyond the extruder itself?
A: The range covers mixing and batching systems, conveying equipment, the twin-screw extruder, multi-pass dryers, flavouring and coating drums, cooling conveyors, and packing stations. Each unit is sized so throughput is balanced across the entire line, preventing any single station from constraining output.
Q: How is throughput matched between the extruder, dryer, and coating drum?
A: Throughput matching begins with the extruder’s confirmed output on your raw material. The dryer bed length and airflow are then calculated to remove the required moisture within the residence time available. The coating drum volume and rotation speed are set to handle that same mass flow without accumulation or spillage.
Q: Can the same line handle both pet food and fish feed with a screw and die change?
A: The twin-screw platform can produce both dry kibble and aquatic feed on the same line architecture. Switching between products requires changing the screw configuration, die plate, and process parameters such as barrel temperature and moisture addition. The dryer and coating drum typically remain the same across both applications.
Q: What utility requirements does the complete line need?
A: The line requires electrical supply at your confirmed voltage and frequency, steam for preconditioning and dryer heating, compressed air for pneumatic gates and controls, and process water for moisture addition at the extruder barrel. Exact consumption figures are provided in the line layout and capacity calculation document.