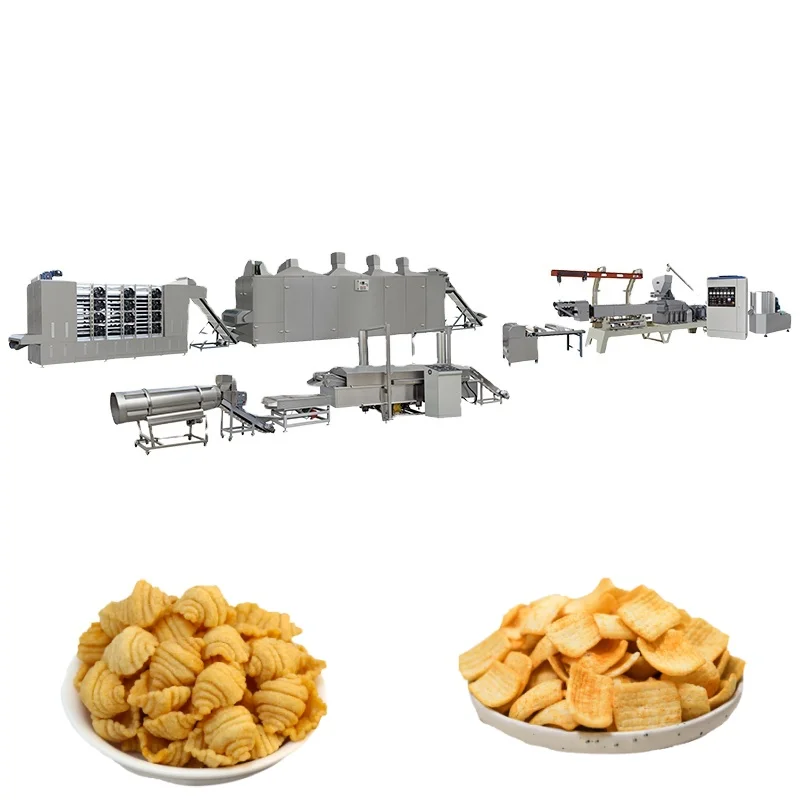
Station-by-station throughput matching — every mixer, extruder, cutter, fryer, and coating drum in the fried snack food processing line is specified under one supplier so bottlenecks are designed out before the line ships.
Technical Specifications
| Parameter | Value |
|---|---|
| Product Type | Fried Pellet Snack Food Production Line |
| Extruder Screw Type | Co-rotating twin-screw |
| Models Available | MT-65 / MT-70 / MT-85 / MT-75 / MT-95 |
| Rated Power | 100 kW (MT-65) / 130 kW (MT-70) / 180 kW (MT-85) / 185 kW (MT-75) / 280 kW (MT-95) |
| Output Capacity | 120–150 kg/h (MT-65, basis not stated in source) / 200–250 kg/h (MT-70, basis not stated in source) / 300–500 kg/h (MT-85, basis not stated in source) / 400–500 kg/h (MT-75, basis not stated in source) / 800–1000 kg/h (MT-95, basis not stated in source) |
| Drying / Heating Source | Gas / Electric / Diesel heating |
| Control System | PLC and MCC, language configurable |
| Voltage & Frequency | Customizable (e.g., 3ph 380V 50Hz, 3ph 415V 60Hz, 3ph 220V 60Hz) |
| Fryer Belt Width | 600 mm stainless steel |
| Cutting Machine Power | 1.47 kW |
| Cutting Machine Dimensions | 2500 × 600 × 1100 mm |
| Mixer Power Options | 4 kW / 7.5 kW / 15 kW (matched to extruder model) |
| Die Configuration | Interchangeable — sticks, square sheet, rib chips, diamond chips, wavy chips, pillow shapes, bugles, shell, screw, square tube, round tube, wave |
| Food-Grade Contact Materials | Stainless steel on all product-contact surfaces |
| Assembly State | Complete production line |
| Warranty | 1 year complete with lifetime maintenance support |
| Certifications | CE (since 2014), ISO |
Application Suitability
| Application | Material or Output |
|---|---|
| Fried pellet chip production | Corn flour, wheat flour, potato starch, potato powder, corn starch blends |
| Bugles-type horn snack manufacturing | Corn-based extrudate with thin-wall die forming |
| 2D and 3D pellet snacks | Shell, screw, tube, wave, pillow, diamond, and wavy chip formats from interchangeable dies |
| New format launches for snack producers | Multiple shape outputs from a single extrusion platform before frying |
What "Nominal Capacity" Means When Your Raw Material Arrives
The rated output only holds if the extruder screw profile and die geometry match the starch, fat, and moisture content of the flour you actually feed in.
Buyers often receive a fried snack food processing line quoted at a specific hourly tonnage, then discover during commissioning that local corn flour or potato starch behaves differently from the standard test material used at the factory. The extruder runs, but the cutter produces misshapen pellets, the fryer yields uneven colour, and the line never reaches its nameplate rate. I have seen this on multiple installations across West Africa and South Asia — the gap between lab-sample throughput and real-batch throughput is where most commissioning delays live [NEED_CITE: raw material variability in extruded snack production].
How Each Station Connects on the Full Equipment Range
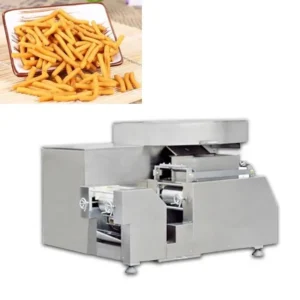
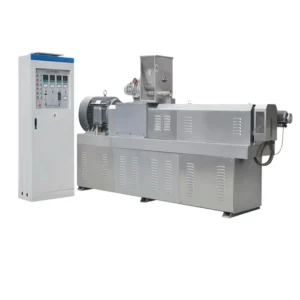
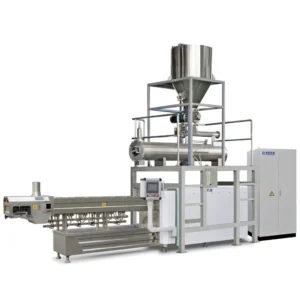
The fried snack food processing line full equipment range starts at the mixer, where flour and water are blended to a target moisture before entering the twin-screw extruder barrel. The co-rotating screw modules handle forward transport, mixing, de-gassing, cooking, and forming in sequential zones. From the die face, the extrudate passes through a cutting machine that shapes pellets before they enter the fryer.
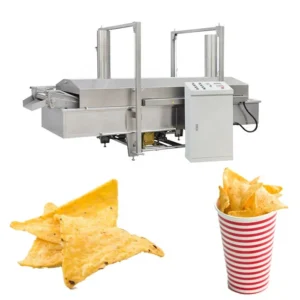
A 600 mm stainless steel fryer belt carries pellets through heated oil with adjustable speed and automatic temperature control. After frying, the product moves to a flavouring or coating drum where seasoning is applied. Every station is specified so that its throughput envelope overlaps with the extruder output, preventing the common problem where one station runs faster than the next can accept [NEED_CITE: throughput balancing across extrusion line stations].
Die and Cutter Options Across Snack Formats
Interchangeable dies and cutting rollers let a single extrusion platform produce bugles, shells, screws, tubes, waves, pillows, diamond chips, and wavy chips. Switching formats means changing the die plate and adjusting the cutter roller gap — the barrel and screw configuration may also need a module swap depending on the target wall thickness and expansion ratio.
This flexibility matters for snack manufacturers entering a market with multiple SKU formats from one capital investment. The die configuration record is documented against your target product shape and raw material blend before the line enters production.
Reading the Specs for Actual Production Impact
The co-rotating twin-screw design provides the shear and residence time needed to fully gelatinise starch at the moisture levels typical of pellet snack dough. Barrel sections are modular, so screw elements can be rearranged for different formulations — higher fat content may require altered kneading block placement to maintain dough consistency at the die face.
Power ratings span from 100 kW on the MT-65 to 280 kW on the MT-95, reflecting the increasing torque and thermal energy needed at higher throughputs. The PLC and MCC control system manages barrel temperature zones, screw speed, and fryer temperature from a central panel, reducing operator-dependent variation between shifts. Voltage and frequency are configurable to match the destination market — a 415V 60Hz installation requires different motor winding and heater element specifications than a 380V 50Hz site, and confirming this before production avoids rewiring during commissioning. Food-grade stainless steel on all contact surfaces meets hygiene expectations for export-market snack production [NEED_CITE: food contact material standards for extruded snack machinery].
The Cost of Skipping the Trial Run
When a fried snack food processing line is shipped without a factory trial on the buyer’s actual raw material, the first real production run happens on the customer’s floor — with the customer’s time, energy, and raw material budget absorbing every adjustment. Misshapen pellets jam the cutter, unevenly fried chips reject at packing, and the flavouring drum may over-season a surface that did not expand to the expected area.
These issues are solvable, but solving them on-site extends commissioning from days into weeks and strains the relationship between buyer and supplier. An in-house testing workshop that runs the buyer’s shipped raw material before dispatch catches die mismatches, screw configuration errors, and fryer temperature gaps while corrections still cost hours rather than days [NEED_CITE: factory acceptance testing practices for food extrusion lines].
What the Full Equipment Range Means in Practice
Matched throughput across stations. The mixer, extruder, cutter, fryer, and coating drum are specified as a set — not sourced from separate vendors and bolted together with hope.
Screw and die documentation. Each build ships with a screw configuration record and die selection note tied to your raw material and target pellet shape, so reorders and replacements match the original setup.
Pre-shipment trial runs. The testing workshop processes your raw material through the assembled line before crating, producing a trial report that confirms pellet shape, fryer behaviour, and seasoning adhesion.
Electrical confirmation before production. Voltage, frequency, and control panel language are locked in during the specification stage, not discovered at uncrating.
Wear parts planning. A documented spare parts list covers screws, dies, and fryer belt components for the first two to three years of operation.
Documentation & Verification
- Line layout drawing with throughput calculations for every station on your fried snack food processing line
- Screw module arrangement and die plate record matched to your raw material formulation
- Trial run report produced on your shipped raw material in the testing workshop before dispatch
- Electrical schematic with confirmed voltage, frequency, and control panel language
- Wear parts list covering screws, dies, cutter rollers, and fryer belt components
- CE declaration of conformity and ISO certificate for customs and import compliance
Installation, Commissioning & Support
- Foundation plan accounts for the full line footprint up to 26 m length and 2.8 m height depending on model selected
- Dedicated electrical circuit sized to the extruder’s rated power, up to 280 kW on the MT-95 configuration
- Line arrives in sectional modules for sequential assembly from mixer through coating drum
- On-site commissioning includes barrel temperature profiling and fryer belt speed calibration against your raw material
- Operator training covers die and cutter roller changeover procedures for switching between pellet formats
- Recommended spare parts package covers twin-screw elements, die plates, and fryer belt links for multi-year operation
What We Need to Configure Your Line
To build a station-matched fried snack food processing line, share your target raw material blend with moisture and fat percentages, the pellet shapes you plan to run, and your target hourly output. Confirm the voltage, frequency, and control language at your facility so motor and heater specifications align before production begins. If you have existing upstream or downstream equipment, provide interface dimensions so the line layout accounts for integration points.
Frequently Asked Questions
Q: How is line capacity verified on my specific raw material before shipment?
A: You send a batch of your actual flour or starch blend to the testing workshop. The assembled line runs a trial production, and a report documents pellet shape, extruder stability, fryer colour consistency, and measured throughput before the line is crated for dispatch.
Q: Can voltage, frequency, and control panel language be matched to my country’s standard?
A: Yes. The PLC and MCC system, motor windings, and heater elements are specified during the quotation stage to match your site supply — whether that is 380V 50Hz, 415V 60Hz, or another combination. Control panel text is set to your preferred language before assembly.
Q: How are throughput rates balanced between the extruder, cutter, fryer, and coating stations?
A: Each station is selected so its capacity envelope overlaps with the extruder’s confirmed output on your raw material. The fryer belt speed, cutter cycle rate, and coating drum volume are all calculated against the same throughput baseline rather than specified independently.
Q: What die and cutting roller options are available for switching between snack shapes?
A: Interchangeable dies cover bugles, shells, screws, tubes, waves, pillows, diamond chips, and wavy chips. Switching requires changing the die plate and adjusting the cutter roller gap; the screw configuration may also be adjusted depending on the target wall thickness and expansion behaviour.
Q: What spare parts are included, and what is recommended for ongoing operation?
A: Free wearing parts ship with the line. A separate spare parts list covers twin-screw elements, die plates, cutter rollers, and fryer belt components sufficient for two to three years of production, with supply available through the after-sales channel.