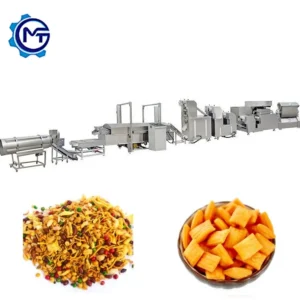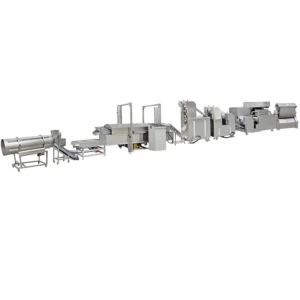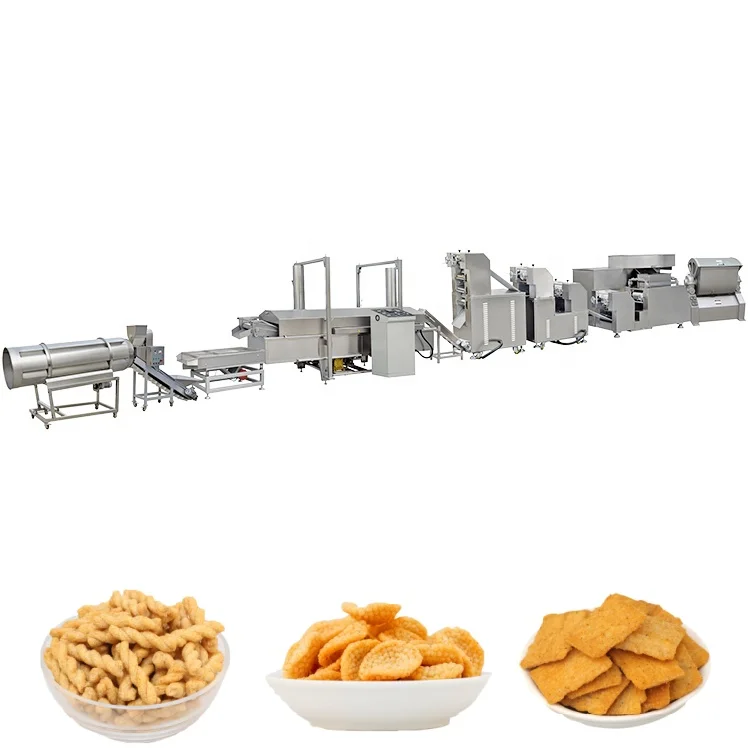
Complete equipment mapping — Every station from mixer through twin-screw extruder to continuous fryer is catalogued here so throughput mismatches surface before the line is built.
Technical Specifications
| Parameter | Value |
|---|---|
| Product Type | 3D Pellet Fried Chips Production Line |
| Extruder Models Available | MT-65 / MT-70 / MT-85 / MT-75 / MT-95 |
| Screw Type | Twin-screw, co-rotating sectional modules |
| Main Motor (MT-65) | 100 kW |
| Main Motor (MT-70) | 130 kW |
| Main Motor (MT-85) | 180 kW |
| Main Motor (MT-75) | 185 kW |
| Main Motor (MT-95) | 280 kW |
| Output Capacity (MT-65) | 120–150 kg/h (basis not stated in source — confirm raw material formulation and moisture content) |
| Output Capacity (MT-70) | 200–250 kg/h (basis not stated in source — confirm raw material formulation and moisture content) |
| Output Capacity (MT-85) | 300–500 kg/h (basis not stated in source — confirm raw material formulation and moisture content) |
| Output Capacity (MT-75) | 400–500 kg/h (basis not stated in source — confirm raw material formulation and moisture content) |
| Output Capacity (MT-95) | 800–1000 kg/h (basis not stated in source — confirm raw material formulation and moisture content) |
| Cutting Machine Power | 1.47 kW |
| Cutting Machine Dimensions | 2500 × 600 × 1100 mm |
| Fryer Belt Width | 600 mm stainless steel mesh belt |
| Fryer Energy Source Options | Electricity / Fuel gas |
| Drying Method Options | Gas / Electric / Diesel heating |
| Voltage Options | 3ph 380V 50Hz / 3ph 380V 60Hz / 3ph 415V 60Hz / 3ph 220V 60Hz (configurable) |
| Die Shapes Available | Bugles, sticks, square sheet, rib chips, diamond chips, wavy chips, pillow, shell, screw, square tube, round tube, wave, crisp pea |
| Line Stations | Mixer → Twin-screw extruder → Cutting/forming machine → Fryer |
| Warranty | 1 year complete, lifetime maintenance support |
| Certifications | CE, ISO |
Application Suitability
| Application | Material or Output |
|---|---|
| 3D pellet fried snack production | Corn powder, wheat flour, potato starch, potato powder, corn starch blends |
| Bugles and horn-shaped chips | Corn-based formulations with controlled moisture for hollow expansion |
| Flat and ribbed fried chips | Wheat flour and starch mixes cut into square, diamond, or wavy sheets |
| Pillow and tube snacks | Dual-layer or hollow extrusion through specialized die plates |
| Shell and screw-shaped pellets | High-starch formulations requiring precise shear and gelatinisation control |
Why the Extruder Is Only Half the Conversation for a Fried Chips Making Machine Full Equipment Range
Matching extruder throughput to fryer belt speed and dryer capacity is where most pellet chip lines succeed or fail.
I once walked into a snack factory where a twin-screw extruder was running fine, but the pellets piled up before the fryer because the continuous belt could not keep pace. The fryer oil temperature dropped every time a surge hit, and the chips came out unevenly coloured. That bottleneck was not visible on any single-machine quotation [NEED_CITE: throughput matching principles across extrusion and frying stations]. When buyers survey a fried chips making machine full equipment range, the goal is to see every station’s rated capacity side by side before committing to a layout.
How Each Station Connects Across the Fried Chips Making Machine Full Equipment Range
The line starts with a mixer that conditions corn powder, wheat flour, or potato starch blends to a target moisture level before feeding the twin-screw extruder. Co-rotating sectional screw modules handle forward transport, mixing, de-gassing, cooking, and forming within a single barrel. The cutting and forming machine downstream slices the extruded strand at adjustable intervals, and its 1.47 kW drive keeps pace with the extruder output without independent speed surges.
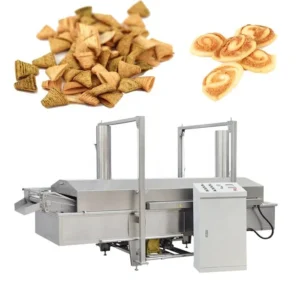
From there, pellets enter the continuous fryer on a 600 mm stainless steel mesh belt. Belt speed and oil temperature are adjustable, and the fryer supports both electric and fuel-gas heating so the thermal input can match local utility costs. Viewing the entire fried chips making machine full equipment range as a connected chain — rather than a list of standalone machines — is what prevents one station from starving or flooding the next.
Die and Roller Flexibility for Shape Variety
A single extruder platform can produce bugles, sticks, diamond chips, wavy chips, pillow shapes, shells, screws, and multiple tube formats simply by swapping die plates and roller inserts. The sectional screw modules can be rearranged to alter shear intensity and residence time, which changes how aggressively the starch gelatinises before the pellet reaches the die face [NEED_CITE: twin-screw extrusion die design and starch gelatinisation behaviour]. This flexibility matters when a snack manufacturer wants to test several shapes on one line before deciding which format to scale.
The cutting machine downstream works in tandem with the die: a ribbed chip requires a different cut interval than a pillow shape, so the cutter must be adjustable in both speed and blade position. Buyers evaluating a fried chips making machine full equipment range should confirm that die changes and cutter adjustments are documented in the screw and die configuration record supplied with the line.
Reading the Motor and Capacity Tiers
Five extruder models span from the MT-65 at 100 kW to the MT-95 at 280 kW, each tied to a different output band. The main motor rating is a reliable indicator of the thermal and mechanical energy available for cooking and forming; a higher kW value generally means the barrel can sustain the shear needed for denser raw material blends. However, actual throughput depends on the buyer’s specific formulation and moisture content, which is why capacity figures should always be confirmed against trial-run data rather than taken from a nameplate alone.
The line dimensions grow with the model tier, from roughly 22 metres in length for the MT-65 configuration to over 30 metres for the MT-95 layout. Workshop ceiling height must accommodate the tallest station — typically the fryer exhaust hood and any overhead cooling conveyors — so overall dimensions should be cross-checked against the building envelope before the layout is finalised. Voltage and frequency are configurable across common industrial standards, but the control panel language and component ratings must be confirmed before production begins to avoid commissioning delays [NEED_CITE: industrial voltage and frequency standards for food processing exports].
The Hidden Cost of Ordering Stations Separately
When an extruder arrives with no matching fryer capacity, the buyer scrambles to source a belt fryer from a different vendor, often discovering that the belt width, oil volume, or heating method does not align with the pellet output rate. I have seen lines sit idle for weeks while a correctly sized fryer was fabricated and shipped. Ordering from a unified fried chips making machine full equipment range eliminates that gap because throughput is calculated station by station before any steel is cut.
Mismatched voltage is another silent delay. If the extruder is wired for 380V 50Hz but the local grid runs at 415V 60Hz, motor speeds shift, heating elements overperform, and control boards can fail during the first week of operation. Confirming electrical specifications early — and getting them in writing on the machine specification sheet — is the cheapest insurance a buyer can purchase.
Why Sourcing the Full Range Here Reduces Line-Build Risk
Complete line configuration under one supplier means throughput at every station is calculated against the same raw material formulation, not patched together from separate vendor datasheets. Screw configuration and die design are specified to the buyer’s actual starch-to-flour ratio and target chip density, rather than copied from a generic build. An in-house testing workshop allows trial runs on the buyer’s own raw material before shipment, so product development begins with data, not guesswork.
Pre-sales consultation covers line layout, utility planning, and phased installation scheduling so that foundation work and electrical rough-in happen before machines arrive. On-site commissioning includes operator training on die changes, cutter adjustments, and fryer belt speed tuning. Ongoing maintenance support and a documented wear parts list mean that replacement screws, die plates, and cutter blades are available when the first changeover is due.
Documentation & Verification
- Line layout drawing showing station-by-station throughput for your chip formulation
- Machine specification sheet for each station with confirmed voltage and frequency
- Screw and die configuration record matched to your raw material and target shape
- Factory test record from trial run on your supplied raw material before dispatch
- CE declaration of conformity and ISO certificate for export clearance
- Operation and maintenance manual covering die changes, fryer belt tension, and cutter blade replacement
Installation, Commissioning & Support
- Foundation plan accounts for overall line length up to 30 metres and fryer oil load
- Dedicated electrical circuit sized to the selected extruder main motor, up to 280 kW
- Stations shipped in modular sections for sequential assembly inside the workshop
- First-run parameter setting covers barrel temperature profile, cutter interval, and fryer belt speed
- Operator training on die plate swaps across all available chip shapes
- Wear parts list with recommended two-to-three-year stock of screw modules and die inserts
What to Share When Requesting a Quotation
To configure a line that actually holds its rated output, start by sharing your raw material formulation — the flour-to-starch ratio and target moisture content at the mixer outlet. Confirm your local voltage, frequency, and preferred control panel language so electrical components are ordered correctly. If you have an existing packing line or flavouring drum, provide the throughput and connection height so the new fryer discharge can feed straight into your current setup.
Frequently Asked Questions
Q: How should extruder output be matched with fryer and drying capacity across the line?
A: Each station’s throughput is calculated against the same raw material formulation and moisture target. The extruder output band is compared to the fryer belt speed and oil volume, and the dryer residence time is sized so pellets reach the fryer at the correct moisture. Mismatches are identified during the layout stage, not after installation.
Q: Which extruder model fits a given production volume and raw material blend?
A: The five model tiers — MT-65 through MT-95 — cover different motor power and output bands. Selection depends on your daily target, formulation density, and the starch gelatinisation behaviour of your specific blend. A trial run on your raw material confirms which model holds the required throughput without compromising chip texture.
Q: What voltage, frequency, and control options are available for different export markets?
A: Configurations include 3ph 380V 50Hz, 3ph 380V 60Hz, 3ph 415V 60Hz, and 3ph 220V 60Hz. Control panel language and component ratings are confirmed before production. The machine specification sheet documents every electrical parameter so local electricians can prepare the site before the line arrives.
Q: How do die and roller changes enable shape variety on the same extruder?
A: Interchangeable die plates and roller inserts allow the line to produce bugles, sticks, diamond chips, wavy chips, pillow shapes, shells, screws, and tube formats. Each shape change requires a documented adjustment to the screw configuration, die plate, and cutter interval. The configuration record supplied with the line covers every approved shape.
Q: What spare wearing parts are included, and what additional stock is recommended?
A: Freely wearing parts are included with the initial shipment. For continuous operation, a two-to-three-year stock of screw modules, die plates, and cutter blades is recommended. The wear parts list specifies part numbers and replacement intervals so procurement can be planned before the first changeover is due.