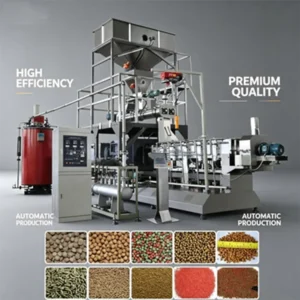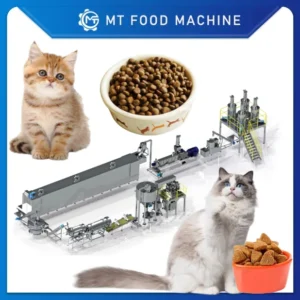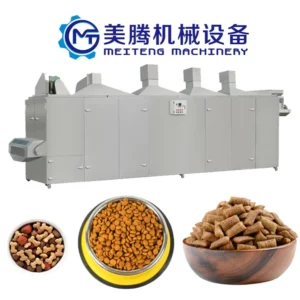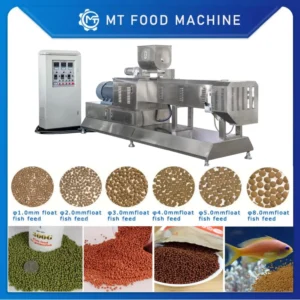
Throughput-Matched Equipment Catalogues — every supporting station in this pet food making machine full equipment range is balanced against the extruder so no single node bottlenecks the line.
Technical Specifications
| Parameter | Value |
|---|---|
| Product Type | Pet Food Extrusion Production Line |
| Application Scope | Dry kibble for dog and cat; floating and sinking aquatic feed for fish |
| Output Capacity | Up to 3 tons per hour (basis not stated in source — confirm raw material type, moisture content, and product formulation) |
| Screw Type | Single or twin screw (configuration to be confirmed against target product) |
| Control System | PLC or MCC control (selection depends on automation requirement) |
| Process Documentation | Fish feed process drawing and line layout provided before order |
| Warranty | 1 year |
| Voltage and Frequency | Configurable to target market electrical standard (to be confirmed) |
| Assembly State | Complete line or standalone extruder (scope to be confirmed per project) |
| Certification | CE and ISO certified (documentation available on request) |
Application Suitability
| Application | Material or Output |
|---|---|
| Dry dog and cat kibble production | Corn flour, meat meal, poultry by-product, bone meal, fish meal blends |
| Floating fish feed pellets | Soybean meal, rice bran, fish meal, wheat flour with controlled expansion |
| Sinking aquatic feed | High-protein formulations requiring dense pellet structure and slow water disintegration |
| Multi-species feed manufacturing | Shared extrusion platform switching between pet and aquatic formulations via screw and die changeover |
What "3 Tons per Hour" Actually Means for Your Pet Food Making Machine Line
A rated capacity figure is only as honest as the raw material and moisture condition behind it.
I have walked through commissioning sessions where the buyer placed an order based on a brochure number tested on standard corn grits, then switched to a high-moisture fresh chicken slurry recipe once the line arrived at their plant. The screw combination that worked perfectly in our workshop could not hold expansion or density on the new formulation. Output dropped, kibble texture drifted outside specification, and we spent nearly two weeks reconfiguring the screw elements and die geometry on-site before production stabilized [NEED_CITE: raw material impact on extrusion throughput]. This is the gap between a nameplate number and a working capacity — and it is why I always push for a trial run on the buyer’s actual recipe before the machine leaves the factory.
How Every Station Fits Into the Equipment Catalogue
When you survey the pet food making machine full equipment range, the extruder is only the starting point. Upstream, the batching and mixing system must deliver a homogeneous blend at the exact moisture level the screw profile expects. Downstream, the dryer must have enough belt area and residence time to pull moisture from kibble at the rate the extruder discharges it. If the dryer is undersized, the line backs up regardless of how fast the extruder runs. The flavouring drum and coating station then need to match that same throughput so seasoning coverage stays uniform across every batch.
Balancing Capacity Across the Full Equipment Range
The real engineering question is not how much a single extruder can push, but whether every station from mixer to packer can sustain that rate simultaneously. A dryer that handles only half the extruder output becomes the constraint. A cooling conveyor that is too short causes condensation inside the packaging bag. When evaluating the pet food making machine full equipment range, the line layout document should show calculated throughput at each node — not just the extruder [NEED_CITE: throughput balancing principles in food extrusion lines]. That calculation is what separates a line that runs at nameplate from one that stalls every twenty minutes.
Reading the Specification Sheet Against Your Recipe
The screw type — single or twin — determines how well the machine handles your specific raw material profile. Twin-screw configurations offer self-wiping action and broader formulation tolerance, which matters when recipes include sticky meat slurries or high-fat blends. The length-to-diameter ratio of the barrel governs residence time and shear history, directly influencing starch gelatinisation and therefore the expansion ratio of the finished kibble. Die selection controls pellet geometry and density — a floating fish feed die differs fundamentally from a dense sinking pellet die. Moisture content at the barrel inlet shifts the entire expansion curve, so the control system must allow precise adjustment of barrel temperature zones and feed rate. Without confirming these parameters against your actual formulation, the specification sheet remains a theoretical document rather than a production guarantee.
The Hidden Cost of Ordering an Extruder Without Its Line
Buying the extruder alone and sourcing dryers, conveyors, and flavouring drums from separate vendors often leads to interface mismatches. One supplier’s discharge height does not align with the next supplier’s infeed. Electrical interlocks are missing, so a downstream jam does not stop the extruder, and product piles up on the floor. Wear parts from different manufacturers carry incompatible part numbers, forcing the maintenance team to stock two inventories [NEED_CITE: equipment integration challenges in multi-vendor food lines]. These problems do not appear in the quotation stage — they surface during commissioning, when every day of delay costs production revenue.
Why Procuring the Full Range From One Source Matters
Every station in this catalogue — mixer, extruder, dryer, flavouring drum, cooler, packer — is designed with the adjacent station’s throughput in mind, so belt speeds and residence times align from the first run. Screw and die configurations are specified after reviewing your raw material sheet, not copied from a generic build that may not match your formulation. The testing workshop allows us to run your actual recipe before shipment, identifying screw adjustments needed for fresh meat inclusions or unusual starch blends. Process drawings and electrical schematics are confirmed with your local voltage and frequency before production starts, avoiding rewiring costs on arrival. Documentation — from the line layout calculation to the wear parts list — travels with the shipment so your maintenance team has references from day one.
Documentation & Verification
- Line layout and throughput calculation confirming capacity balance across every station for your target output
- Machine specification sheet recording screw element arrangement and die geometry matched to your recipe
- Electrical schematic with confirmed voltage, frequency, and control language for your market
- Trial run report produced on your actual raw material documenting expansion, density, and moisture results
- CE declaration of conformity and ISO certificate included with the shipping documentation package
- Wear parts list with part numbers for screws, dies, and cutter blades to simplify reorder planning
Installation, Commissioning & Support
- Foundation plan showing load points and drainage requirements based on the dryer and extruder footprint
- Dedicated electrical circuit specification matching the confirmed motor power and voltage of your extruder configuration
- Assembly sequence for the full line, from extruder barrel alignment through dryer belt tensioning
- First-run parameter logging covering barrel zone temperatures, screw speed, and feed rate on your recipe
- Operator training on PLC or MCC interface language confirmed for your production team
- Spare screw elements and die plates shipped with the initial order to cover the first replacement cycle
Before You Send an Inquiry
Share the raw material list with moisture percentages and the target kibble or pellet specification — density, size, and whether the aquatic feed must float or sink. Confirm the local voltage and frequency at your plant so the electrical package is built correctly the first time. Provide workshop dimensions including ceiling height, because the dryer and cooling conveyor length depend on available floor space. If you are switching from an existing line, tell us which upstream and downstream equipment you plan to keep so the new pet food making machine full equipment range interfaces cleanly with what you already have.
Frequently Asked Questions
Q: How is the output capacity verified against my raw material and formulation?
A: We run a trial in the testing workshop using your actual recipe, measuring expansion ratio, kibble density, and moisture at discharge. The trial run report records screw speed, barrel temperatures, and feed rate, so the capacity figure you receive is tied to your specific blend rather than a generic corn flour benchmark.
Q: Which supporting stations are included, and how is throughput matched?
A: The line can include batching, mixing, extrusion, drying, flavouring, cooling, and packing stations. Each station is sized so its rated throughput equals or slightly exceeds the extruder output confirmed during the trial run, preventing any single node from becoming a bottleneck.
Q: What voltage and frequency options are available?
A: The electrical package is configured to your plant supply — common ranges include 380V/50Hz, 415V/50Hz, and 440V/60Hz. We confirm the exact requirement during the specification stage and reflect it on the electrical schematic before production begins [NEED_CITE: industrial voltage standards by region].
Q: Can I review process drawings and line layout before ordering?
A: Yes. A fish feed process drawing and full line layout are provided during the proposal stage, showing equipment placement, throughput at each station, utility connection points, and operator access paths so you can evaluate fit within your facility before committing.
Q: What does the warranty cover, and how are spare wear parts handled?
A: The one-year warranty covers manufacturing defects across the full line. A wear parts list with part numbers for screws, dies, and cutter blades ships with the order, and replacement elements can be reordered directly using those numbers to ensure dimensional compatibility.