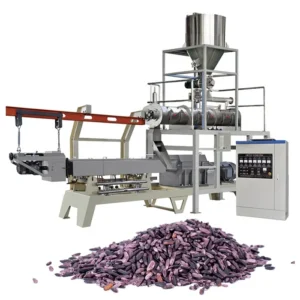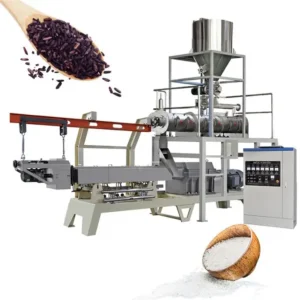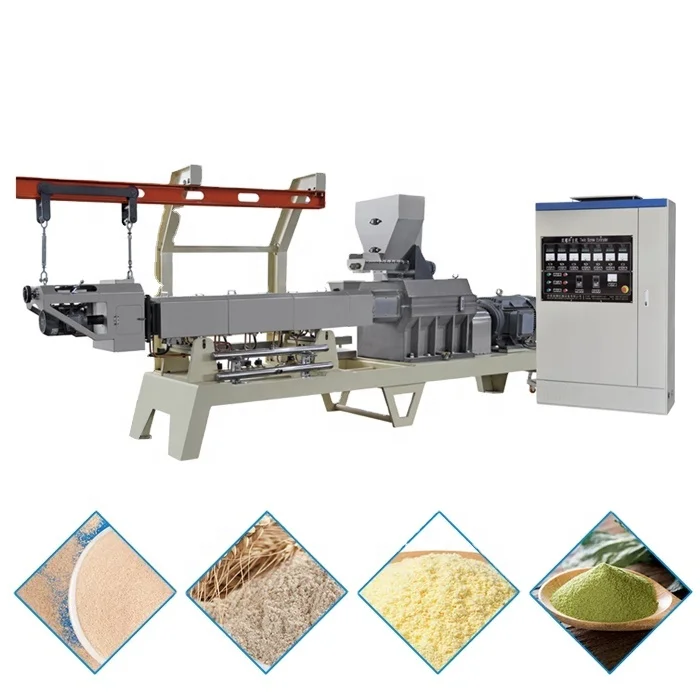
Complete Equipment Catalogue — Every station in this nutritional powder processing line equipment, from the twin-screw extruder to the high-temperature roaster and powder mixer, is specified with individual output, power and footprint data so buyers can survey throughput matching before committing to a line configuration.
Technical Specifications
| Parameter | Value |
|---|---|
| Product Type | Nutritional Powder Processing Line |
| Extruder Model | MT65 (MT70 and MT85 also available) |
| Installed Power | 85 kW (MT65); 120 kW (MT70); 195 kW (MT85) |
| Real Power Consumption | 65 kW (MT65); 90 kW (MT70); 165 kW (MT85) |
| Line Output Capacity | 150–200 kg/h (MT65); 200–300 kg/h (MT70); 600–800 kg/h (MT85) (basis not stated in source — confirm raw material, moisture content and particle size) |
| Overall Dimensions | 18000×1300×2300 mm (MT65) |
| Screw Configuration | Twin-screw |
| Extruder Main Motor Power | 30 kW (MT65 extruder) |
| Extruder Actual Power | 30–35 kW |
| High-temperature Roaster Output | 300–400 kg/h (basis not stated in source — confirm material and target moisture) |
| Roaster Belt Effective Length | 3.5 m |
| Roaster Heater Power | 3.9 kW × 24 far infrared heaters |
| Powder Mixer Tank Volume | 150 kg per batch |
| Powder Mixer Rotary Speed | 385 rpm |
| Powder Mixer Mixing Time | 10 min per batch |
| Contact Material | Stainless steel 304 |
| Standards | CE, ISO |
| Warranty | 1 year complete warranty, lifetime maintenance service |
Application Suitability
| Application | Material or Output |
|---|---|
| Baby rice noodles and infant nutrition powder | Rice, corn and grain blends requiring gelatinisation and fine milling |
| Meal replacement and instant grain paste | Oat, soybean, sesame and multi-grain formulations |
| Modified starch for industrial use | Corn and tuber starch for textile, papermaking and building material applications |
| Instant corn paste and breakfast drink powder | Corn grits and roasted grain mixtures needing high-temperature roasting before milling |
What "150 kg/h Output" Leaves Out About Line Matching
A single station running slower than the rest caps the entire line, regardless of what the extruder plate says.
When buyers evaluate nutritional powder processing line equipment, the headline number is usually the extruder output. But if the downstream roaster cannot handle that throughput at the required moisture reduction, material piles up on the belt, residence time drops, and the powder leaves the dryer still too wet to mill properly. I have watched lines stall not because the extruder failed, but because the roaster belt speed and heater capacity were never reconciled with the upstream feed rate. Matching throughput across every station — mixer, extruder, roaster, grinder and blender — is the step that separates a working line from a bottlenecked one [NEED_CITE: throughput matching methodology for multi-station food processing lines].
Station-by-Station Throughput Alignment
A nutritional powder processing line equipment catalogue that lists every station’s rated output side by side lets process engineers spot mismatches before the order is placed. The MT65 extruder and the high-temperature roaster each carry separate output ratings, and the powder mixer operates on a batch cycle rather than a continuous flow. These differences must be reconciled in the line layout calculation so that the roaster belt speed, mixer batch frequency and air conveyor capacity all align with the extruder’s continuous feed.
Far Infrared Roasting and Moisture Control
The roaster uses 24 far infrared heater elements across a 3.5 m effective belt length to drive moisture out of the extruded pellets before milling. Residence time on the belt and heater zone temperature together determine the final moisture content, which directly affects milling efficiency and powder particle size distribution. The roaster also carries a gas consumption rating, and the gas type and operating duration must be confirmed for the destination market before the burner jets are sized [NEED_CITE: far infrared drying parameters for grain-based food powders].
How Screw Configuration and Die Design Shape the Powder
The twin-screw extruder in this line handles grain-based formulations where starch gelatinisation and protein denaturation must occur within a controlled residence time. Screw element sequencing — conveying, kneading and reverse-screw sections — determines the shear profile inside the barrel, which in turn governs how completely the starch granules break down. The die plate aperture and open area control pellet density and size, setting the starting geometry that the roaster and mill will later reduce to powder. Choosing the wrong screw profile for a high-protein formulation like oat and whey can cause surging at the die, uneven pellet density, and a final powder that fails dissolution tests.
The Cost of Skipping a Raw-Material Trial Run
Every grain blend behaves differently under heat and shear. A line configured on standard corn grits may run cleanly during the factory acceptance test, yet block the die or produce uneven pellets when the buyer’s actual oat-whey or multi-grain mix is introduced. Two days of unplanned downtime on a new installation, while engineers re-profile screw elements and adjust barrel temperatures, is a common consequence of skipping the pre-shipment trial. That is why I now insist that every buyer ships a representative batch of their raw material to the testing workshop so the screw configuration and die design are locked to the real formulation before the machines leave the factory [NEED_CITE: common commissioning failures in grain extrusion lines].
Why Procurement Here Differs from Assembling Vendors
Each station in this nutritional powder processing line equipment range comes from a single production facility, meaning throughput calculations, electrical schematics and control language are coordinated under one engineering team rather than negotiated across separate suppliers. Screw and die configurations are specified to the buyer’s raw material, not copied from a generic build. An in-house testing workshop allows trial runs on the actual grain blend before shipment. Stainless steel 304 contact materials are used across all stations. Documentation — from line layout to wear parts lists — is issued as one integrated package.
Documentation & Verification
- Line layout and capacity calculation showing throughput matching between extruder, roaster and mixer
- Screw and die configuration record matched to buyer’s specific grain formulation
- Electrical schematic with voltage and frequency confirmation for destination market
- Trial run report on customer raw material conducted in the testing workshop before dispatch
- CE declaration of conformity and ISO certificate included with shipment documentation
Installation, Commissioning & Support
- Floor plan and utility drawing provided for the 18 m line footprint so foundations and cable trays are prepared before arrival
- Voltage and frequency verified per destination market; control panel language confirmed before the electrical cabinet is wired
- Extruder barrel sections and roaster belt shipped in matched sets for straightforward on-site assembly
- First-run commissioning includes screw speed, barrel temperature profile and roaster belt speed adjustment to target powder moisture
- Operator training covers batch mixer cycle timing, extruder feed rate and roaster zone temperature management
- Wear parts list for screws, dies and roaster belt components supplied with recommended first-replacement intervals
Before You Request a Quote
To configure a nutritional powder processing line equipment package that matches your production target, share your raw material formulation including grain type, protein content and incoming moisture level. Specify the daily output target and the shift pattern you plan to run. Confirm the voltage, frequency and preferred control language at your facility, and indicate whether you can send a sample batch for a pre-shipment trial run in the testing workshop.
Frequently Asked Questions
Q: How do I verify each station’s output capacity against my raw material?
A: Output ratings for the extruder, roaster and mixer are listed with the caveat that actual throughput depends on material density, moisture and particle size. Request a capacity calculation that uses your specific grain formulation, and schedule a trial run in the testing workshop to validate the numbers on your real raw material before the line ships.
Q: Which screw and die configuration fits a high-protein grain blend?
A: High-protein blends such as oat-whey or soybean-corn require a screw profile with adjusted kneading block angles and a die plate with larger apertures to prevent surging. The configuration record is built after the trial run on your sample material, and the final specification is documented before the extruder leaves the factory.
Q: What electrical details must be confirmed before shipment?
A: Voltage, frequency and phase must match your facility supply, and the control panel language should be set to your operator team’s preference. The electrical schematic is issued for your review and sign-off before the cabinet is wired, preventing commissioning delays caused by mismatched power specifications.
Q: How is throughput matched between the batch mixer and continuous extruder?
A: The powder mixer runs on a 10-minute batch cycle with a 150 kg tank, while the extruder feeds continuously. The line layout calculation sets the mixer batch frequency and air conveyor speed so that material supply never starves the extruder hopper or overfills the buffer bin between the two stations.
Q: What spare wear parts should I order with the initial shipment?
A: Screws, die plates and roaster belt components are the primary wear items. A complete wear parts list with part numbers is included in the shipment documentation, and ordering the first replacement set alongside the line avoids production stoppages when initial wear reaches the replacement threshold.