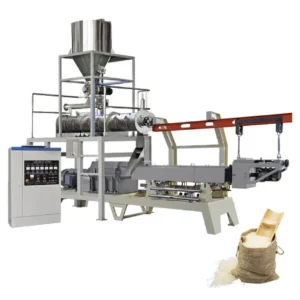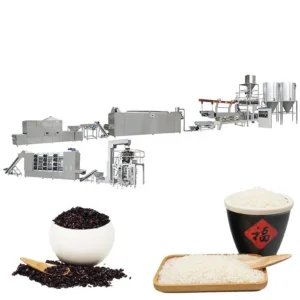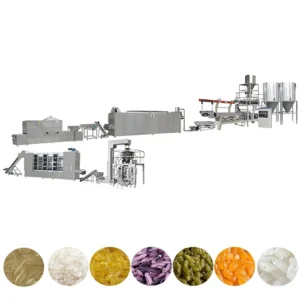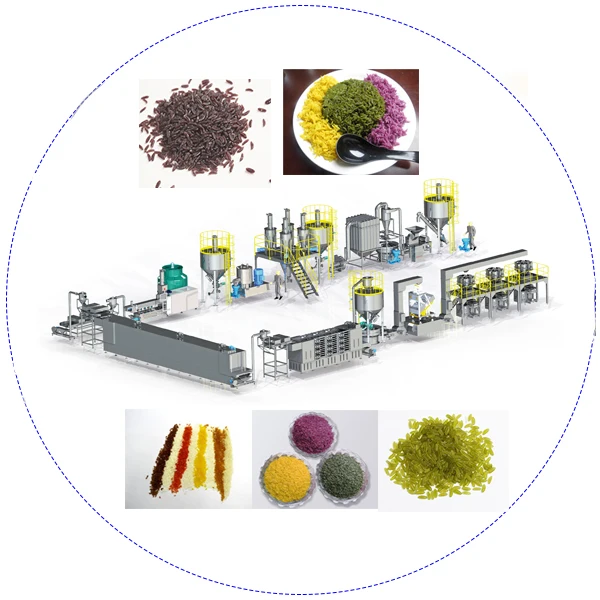
Throughput-Matched Engineering — Every station from mixer to packer is sized against your grain blend and moisture targets, preventing the bottleneck failures common in multi-vendor assemblies.
Technical Specifications
| Parameter | Value |
|---|---|
| Product Type | Fortified Rice Kernel Processing Line |
| Model Range | MT65 / MT70 / MT85 / MT75 / MT95 |
| Screw Configuration | Twin-screw extruder |
| Feeding System | Single or double screw feeding system selectable per material |
| Control Interface | Frequency speed control with high automation |
| Lubrication | Automatic lubricating and cooling system |
| Installed Power | 85 kW (MT65) / 120 kW (MT70) / 235 kW (MT85) / 180 kW (MT75) / 260 kW (MT95) |
| Power Consumption | 60 kW (MT65) / 85 kW (MT70) / 165 kW (MT85) / 135 kW (MT75) / 195 kW (MT95) |
| Output Capacity | 80–100 kg/h (MT65)¹ / 100–120 kg/h (MT70)¹ / 200–300 kg/h (MT85)¹ / 300–500 kg/h (MT75)¹ / 800–1000 kg/h (MT95)¹ |
| Overall Dimensions | 28 × 1.2 × 2.2 m (MT65) to 36 × 3.5 × 4.3 m (MT95) |
| Drying Oven Heating | Electric or gas source selectable |
| Drying Mechanism | Circulation drying with frequency motor mesh belt speed control |
| Standards | CE, ISO |
¹ Capacity basis (raw material and moisture content) to be confirmed during pre-shipment trial.
Application Suitability
| Application | Material or Output |
|---|---|
| Nutritional Rice Enrichment | Vitamin and mineral pre-mixes blended with broken rice flour |
| Artificial Rice Kernel Production | Rice starch, corn, and millet formulations shaped into whole-grain analogues |
| Grain Valorization | Reprocessing broken rice and rice bran into high-nutritional food products |
| Institutional Fortification Programs | Production of iron, zinc, and folic acid fortified kernels for public distribution |
Why Your Grain Blend Dictates the Line Speed
A fortified rice kernel extrusion line full equipment range rated for 300 kg/h on pure rice flour will drop throughput noticeably when whey protein isolate or mineral salts enter the recipe.
I have seen lines specified on catalog data fail in the field because the extruder could not maintain thermal stability against the high fat or protein content of the actual formula. The screw configuration, barrel heating zones, and die geometry must be calculated against the exact rheology of your blend. When buyers ignore this and purchase based on nominal output, they inherit a line that requires constant manual intervention to prevent torque alarms and product collapse [NEED_CITE: twin-screw extrusion rheology and shear rate calculations].
The Complete Equipment Ecosystem
Selecting a fortified rice kernel extrusion line full equipment range requires looking past the extruder. The complete system includes the batching and mixing station, the extruder, vibrating conveyors, low-temperature drying, cooling, high-temperature roasting, and final packing. If the drying oven has less surface area than the extruder’s output demands, the kernels will crack or remain too moist for stable storage.
Matching Drying Kinetics to Kernel Density
The circulation drying oven utilizes a frequency-controlled mesh belt. This allows operators to adjust the residence time of the kernels precisely. Artificial rice requires a different drying curve compared to naturally fortified varieties because the gelatinization degree in the twin-screw barrel changes how moisture migrates to the surface during the drying phase [NEED_CITE: moisture migration and drying kinetics in starch-based extrudates].
Interpreting the Power and Capacity Specifications
The installed power versus power consumption figures across the MT65 to MT95 range reveal the thermal and mechanical load each model handles. For example, moving from the MT75 (180 kW installed) to the MT95 (260 kW installed) is not just about volume; it is about the torque required to push dense, mineral-loaded dough through the die plate at high speeds. The automatic lubricating and cooling system is critical here, as continuous runs with abrasive mineral pre-mixes increase wear on the screw elements. Selecting the right model depends on the daily production target and the specific abrasiveness of your chosen fortificants.
The Cost of Unverified Voltage and Control Languages
Arriving at a job site to find the local grid operates at a frequency or voltage outside the machine’s design envelope is a delay that costs thousands in idle labor. Furthermore, if the PLC or frequency inverter menus are locked in a language the local operators cannot read, basic troubleshooting becomes impossible. These details must be confirmed in the electrical schematic before the steel is cut [NEED_CITE: industrial voltage and frequency standards by region].
Why Procurement Starts with Material Trials
- Screw and Die Configuration: We do not use generic builds; the screw elements and die holes are specified to your raw material blend and target kernel shape.
- In-House Testing Workshop: You can witness a trial run on your actual raw material in our testing workshop before the equipment is crated for shipment.
- Throughput Matching: Every station—from the ribbon mixer to the roasting drum—is calculated so that no single machine bottlenecks the quoted capacity.
- Comprehensive Documentation: You receive a full line layout and capacity calculation document, ensuring utility planning and footprint are verified before installation begins.
Documentation & Verification
- Line layout and capacity calculation confirming throughput across every station.
- Screw and die configuration record specified to your raw material blend.
- Trial run report on customer raw material conducted in the testing workshop.
- Electrical schematic with voltage, frequency, and control language confirmation.
- Operation and maintenance manual with wear parts list and lubrication schedule.
Installation, Commissioning & Support
- Site utility check verifying power supply matches the MT65 (85 kW) or MT95 (260 kW) installed load.
- Mechanical alignment of the 28-meter to 36-meter line footprint within the prepared facility floor.
- Calibration of the frequency motor mesh belt speed to achieve target kernel moisture content.
- Operator training on the automatic lubricating system and barrel temperature zones.
- Provision of spare wear parts including specific screw elements and die plates.
- Commissioning of the batching system to ensure uniform distribution of micro-ingredients.
Preparing Your Inquiry
To provide an accurate line configuration, we require the specific grain or starch base you intend to use, the target daily output, and the exact composition of any vitamin or mineral pre-mixes. Please also specify the available voltage and frequency at your facility, as well as any space constraints within the production hall.
Frequently Asked Questions
Q: How is the capacity rating verified on my specific grain blend and moisture content?
A: We require a sample of your raw material and pre-mix to run in our testing workshop. This trial establishes the actual throughput and screw configuration needed, rather than relying on nominal catalog ratings that may not account for high-protein or high-mineral formulations.
Q: What voltage, frequency, and control language options are confirmed before shipment?
A: We review your local electrical standards and specify the motors and control cabinets accordingly. The control interface language is set to match your operators’ requirements, and an electrical schematic is provided for your approval before production begins.
Q: How are the extruder, dryer, and roaster matched so no station bottlenecks the line?
A: The line is engineered as a single system. We calculate the moisture load leaving the extruder and size the drying oven surface area and airflow to handle that specific volume, ensuring the roaster and cooler also maintain the flow rate without causing product backlog.
Q: Can I run a trial with my own raw material before the line ships?
A: Yes, our in-house testing workshop is equipped to run trials on your specific ingredients. This allows us to finalize the screw configuration and process parameters, ensuring the line performs correctly from the first day of installation at your facility.
Q: What spare wear parts are included and how are replacements sourced?
A: The initial shipment includes a wear parts list and a set of high-wear items such as specific screw elements, die plates, and mesh belt sections. We maintain inventory of these components for rapid dispatch throughout the operational life of the machinery.