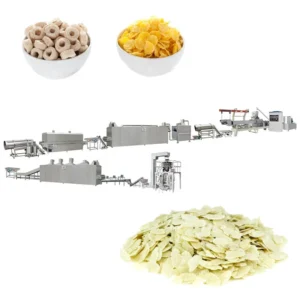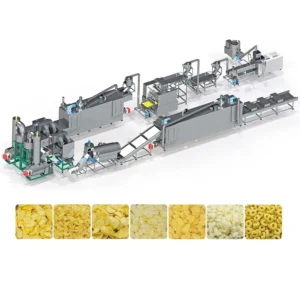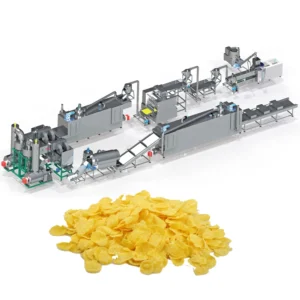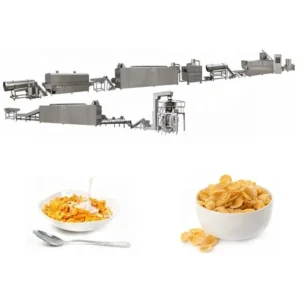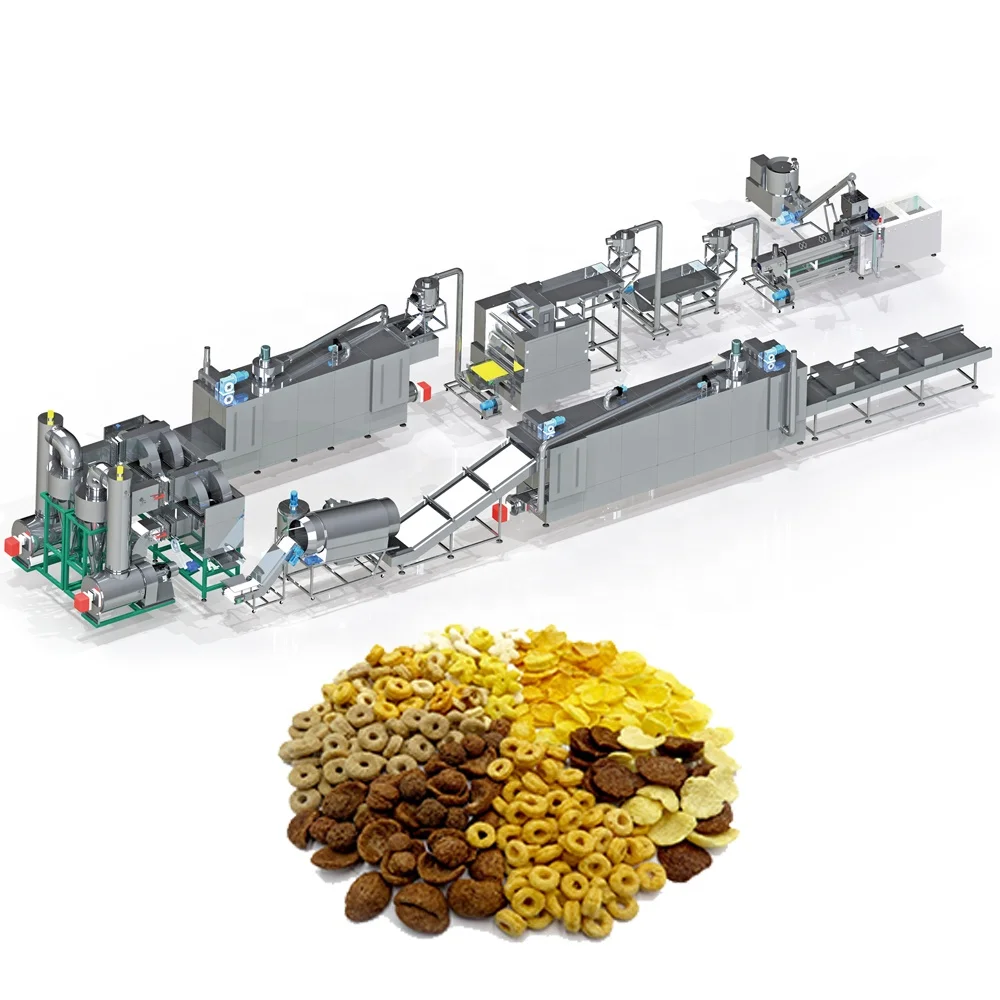
Screw and Die Matched to Your Grain — Every station on this MT70 line is specified around your raw material rather than a generic catalogue build.
Technical Specifications
| Parameter | Value |
|---|---|
| Product Type | Corn Flakes Production Line |
| Model | MT70 |
| Installed Power | 160 kW |
| Power Consumption | 120 kW |
| Output Capacity | 150-200 kg/hr (basis not stated in source — confirm raw material / moisture content) |
| Overall Dimensions | 41 x 1.5 x 2.2 m |
| Screw Type | Twin Screw |
| Basic Material | Powder of corn, rice, wheat, oat, barley, etc. |
| Production Procedure | Mixing → Extruding → Flaking → Drying → Hot Air Roasting → Cooling → Packing |
| Coated Line Option | Sugar Spraying → Sugar Coating → Drying added after roasting |
| Control System | PLC control; automated line control |
| Flaking Machinery | Hydraulic double rollers; double motors for separate roller driving; infrared sensor temperature control |
| Roasting Oven | Vibrating pan; conciliation burner; two separate circulating fans; cyclone dust removal |
| Heating Source (Dryer) | Gas, Electric |
| Coating System | Double tumble for sugar melting, elevator, coating drum, spraying nozzle |
| Extruder Systems | Feeding, extruding, cutting, heating, gearing, controlling |
| Extruder Advantage | Automatic lubricating, cooling function; screw made by special tech for grinding resistance |
| Assembly State | Complete turnkey line |
Application Suitability
| Application | Material or Output |
|---|---|
| Natural corn flakes production | Corn powder, corn grits |
| Sugar-coated breakfast cereal | Corn, rice, wheat base with sugar syrup |
| Shaped breakfast cereal | Ball, tube, stick, ring, fruit loop, star, wheel, flower, heart via die change |
| Multi-grain flake processing | Oat, barley, wheat, rice powder blends |
| Fortified breakfast cereal lines | Grain powder with added nutritional premix |
What a "150–200 kg/hr" Rating Actually Depends On
The number on the plate only holds if every downstream station can keep pace with the extruder output.
When an extruder pushes out cooked pellet at its rated speed but the flaker cannot press it thin enough, or the roasting oven cannot handle the moisture load, the entire corn flakes machine full equipment range drops below its nameplate figure. I once saw a line where the roaster was undersized — the flakes came out damp and stuck together, forcing the operator to slow the extruder and lose throughput every shift [NEED_CITE: throughput bottlenecking from mismatched station capacities]. That is why matching the flaking roller speed, dryer belt length, and oven air volume to the extruder’s actual output matters more than the headline number.
How Each Station Connects in the Corn Flakes Process
The line begins with batching and mixing, where the grain powder and any nutritional additives are blended to a uniform moisture level before entering the twin-screw extruder. The extruder cooks and forms the dough into a continuous ribbon or pellet shape, and the cutting system segments it before the flaking stage. Each station in this corn flakes machine full equipment range is selected so that material flow from one step feeds the next without backlog or starvation.
Temperature and Moisture Control Across the Line
After extrusion, the flaking machinery uses hydraulic double rollers driven by independent motors, with infrared sensors monitoring roller surface temperature to prevent sticking or tearing. The dried flakes then pass into the roasting oven, where the conciliation burner and dual circulating fans maintain an even heat profile. A cyclone dust removal device keeps fine particles from recirculating [NEED_CITE: food-grade air handling standards for cereal roasting equipment]. Getting these temperature zones right is what separates a crisp, golden flake from one that tastes burnt or remains chewy in the centre.
Reading the Specs That Matter for Grain Processing
The 160 kW installed power across the line reflects the combined draw of the extruder main motor, flaking hydraulics, dryer heating elements, and roasting oven burner fans. With 120 kW typical consumption, the electrical supply must be sized for continuous duty with a margin for start-up surges. The twin-screw configuration gives a longer residence time and better mixing action than a single screw, which is important when processing oat or barley blends that gelatinise at different rates than pure corn. The 41-metre overall line length means the floor plan needs clear space for material flow between mixing, extruding, flaking, drying, roasting, cooling, and packing stations, with access aisles for maintenance on both sides.
The Hidden Cost of Mismatched Dryer and Coating Capacity
When the dryer or coating drum cannot handle the extruder’s full output, operators either slow the whole line or accept product that is under-dried and prone to mould in storage. I have seen sugar-coated flakes clump inside the coating drum because the spray rate was set for a higher throughput than the tumbling action could distribute evenly [NEED_CITE: coating uniformity issues in breakfast cereal lines]. Over time these mismatches cause unplanned stops, product waste, and customer complaints about flake texture that no amount of parameter tuning can fix on the factory floor.
Why Source the Full Equipment Range From One Builder
Every station on the MT70 line — mixer, twin-screw extruder, hydraulic flaker, dryer, roasting oven, and coating system — is selected and tested together so throughput is balanced from batching through to packing. Screw and die configuration is specified to your grain type and target flake thickness, not copied from a generic build. The flaking rollers use independent dual motors with infrared temperature feedback to maintain consistent sheet thickness across both natural and sugar-coated runs. The roasting oven’s conciliation burner and dual fan arrangement are sized for the moisture load coming off your specific dryer, not a worst-case estimate. In-house trial runs on your actual raw material before shipment catch problems like low expansion or poor flake release before the line leaves the factory.
Documentation & Verification
- Line layout and capacity calculation matching every station to your target output
- Machine specification sheet with screw and die configuration for your grain type
- Electrical schematic confirming voltage, frequency, and PLC language for your market
- Trial run report on your raw material showing flake thickness and moisture readings
- CE declaration of conformity covering the full assembled line
- Operation and maintenance manual with wear parts list for screws, dies, and rollers
Installation, Commissioning & Support
- Floor plan for the 41-metre line footprint including utility connection points
- Dedicated electrical circuit for 160 kW installed load with start-up surge allowance
- Sectional delivery with flaking and roasting stations assembled on site
- First-run parameter setting for extruder barrel zones and roller gap
- Operator training on PLC interface and hydraulic flaking pressure adjustment
- Spare screw and die segments supplied with initial wear parts kit
Before You Send an Inquiry
To configure this line correctly, share the grain type or blend you plan to process, whether you need natural or sugar-coated output, and your target daily volume. Include your facility voltage and frequency, the control language your operators use, and the floor space available for a 41-metre layout. If you have a specific flake thickness or bowl-life requirement, send that along with a sample of your raw material so we can run a trial before the quotation is finalised.
Frequently Asked Questions
Q: How is line throughput matched between extruder, flaker, dryer and coating stations?
A: Each station is sized against the extruder’s actual output on your grain material, not a generic nameplate figure. The flaker roller speed, dryer belt length, oven air volume, and coating drum capacity are all calculated together so no single station bottlenecks the corn flakes machine full equipment range during continuous production.
Q: What voltage, frequency and control language options are confirmed before shipment?
A: The electrical schematic is prepared for your local supply — whether 380V/50Hz, 440V/60Hz, or another standard — and the PLC interface language is set to match your operators. A voltage confirmation document is signed off before the line enters production.
Q: Can the same line produce both natural and sugar-coated corn flakes?
A: Yes. The base line runs mixing through extruding, flaking, drying, roasting, cooling, and packing for natural flakes. Adding the sugar spraying, coating drum, and secondary drying module converts the output to sugar-coated product without changing the extruder or flaker setup.
Q: How are screw and die configurations selected for different grain materials?
A: Oat, barley, wheat, and rice powders gelatinise at different temperatures and moisture levels than pure corn. The screw profile, compression ratio, and die aperture are chosen after a trial run on your actual raw material to achieve the correct expansion, surface texture, and flake integrity for your target market.
Q: What spare wear parts are included and how are replacements supplied?
A: The initial shipment includes spare screw sections, die plates, and flaking roller segments sized for your production schedule. A wear parts list in the documentation identifies each component by part number so replacements can be ordered and shipped without line downtime.