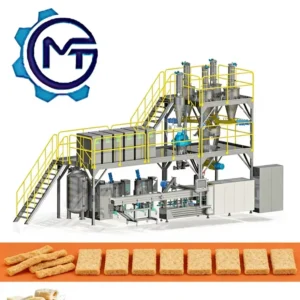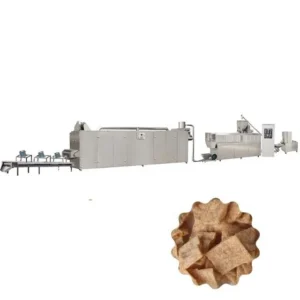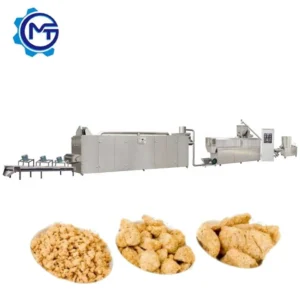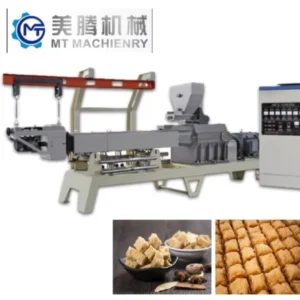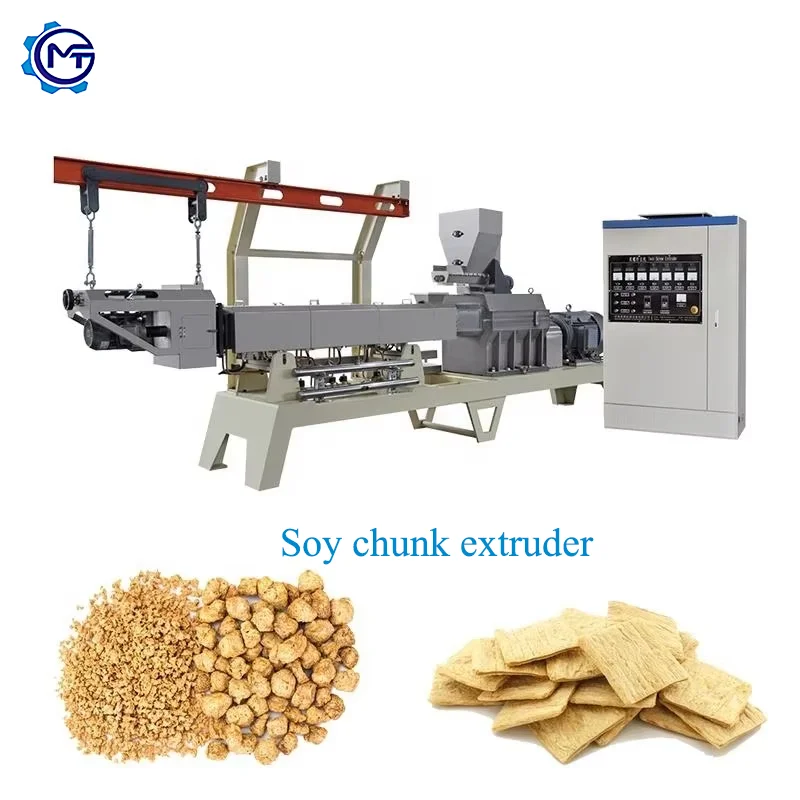
Integrated Line Throughput — every station from the powder mixer to the cooling conveyor is sized against the extruder output so material flow holds steady without upstream starvation or downstream pile-up.
Technical Specifications
| Parameter | Value |
|---|---|
| Product Type | Textured Vegetable Protein (TVP) Extrusion Production Line |
| Model Options | MT65 / MT70 / MT85 |
| Extruder Type | Twin-screw |
| Installed Power | MT65 — 85 kW; MT70 — 120 kW; MT85 — 195 kW |
| Actual Power Consumption | MT65 — 65 kW; MT70 — 90 kW; MT85 — 165 kW |
| Output Capacity | MT65 — 150–200 kg/h (basis not stated in source); MT70 — 200–300 kg/h (basis not stated in source); MT85 — 600–800 kg/h (basis not stated in source) |
| Overall Line Dimensions | MT65 — 18000×1300×2300 mm; MT70 — 20000×1500×2400 mm; MT85 — 24000×3500×4300 mm |
| Powder Mixer Tank Volume | 150 kg per batch |
| Powder Mixer Mixing Time | 10 min per batch |
| Powder Mixer Rotary Speed | 385 rpm |
| Powder Mixer Power | 4 kW |
| Dryer Effective Belt Length | 3.5 m |
| Dryer Heating | Far infrared 3.9 kW × 24 units; gas-assisted at 6.8 m³/h (gas type to be confirmed) |
| Cooling Machine Operating Range | 0–260 °C |
| Construction Material | Stainless steel (contact and non-contact surfaces) |
| Control System | PLC or MCC (configurable per order) |
| Voltage and Frequency | Configurable per destination market |
| Warranty | 1 year complete |
Application Suitability
| Application | Material or Output |
|---|---|
| Textured soybean protein for plant-based meat alternatives | Low-temperature soybean meal |
| Vegetarian meat products and analogues | Defatted soy flour and soy protein concentrate |
| Protein ingredient supply for ham and sausage processing | Peanut meal or soy-peanut blends |
| Canned and quick-frozen food protein components | TVP chunks, shreds, and granules after extrusion and drying |
| Small-to-medium plant-based meat start-up lines | MT65 configuration for pilot-scale volumes |
| Industrial-scale protein ingredient production | MT85 configuration for continuous high-volume output |
Why Matching Every Station Matters More Than the Extruder Headline
A textured vegetable protein production line is only as fast as its weakest downstream link. When the dryer cannot remove moisture quickly enough, the extrudate backs up, surface tackiness increases, and the fibrous structure collapses before cooling sets it. I have seen lines where the twin-screw extruder was rated well but the roaster belt was two meters too short — operators had to run the extruder at a fraction of its capacity just to keep the drying stage from flooding.
The consequence is not just lower throughput. Moisture trapped inside a TVP chunk causes uneven texture, short shelf life, and a product that fails the rehydration test buyers run in their labs [NEED_CITE: moisture content targets for dried TVP products in food ingredient specifications]. That is why each station in this full equipment range is sized against the extruder’s actual output on your raw material, not a generic chart value.
How Twin-Screw Shear Restructures Protein Molecules
The core of the textured vegetable protein production line sits in the barrel zone where temperature, pressure, and mechanical shear converge. Spherical protein molecules in soybean meal or peanut meal are denatured under high-temperature, high-pressure conditions and realigned into elongated, fibrous chains that mimic muscle tissue. The twin-screw configuration ensures that residence time and shear intensity are distributed evenly across the barrel length, which matters because uneven shear produces chunks with a dense core and a porous shell — a texture defect that is immediately visible when the product is rehydrated.
Screw configuration and die geometry are selected based on the raw material protein content and the target fiber orientation. Switching from soybean meal to a peanut meal blend, for instance, requires a different compression ratio inside the barrel and a different die aperture to maintain the same fibrous pull-apart feel.
What the Full Equipment Range Means for Line Balancing
Surveying every station before committing to a configuration lets you see where capacity margins exist and where they do not. The powder mixer cycles a 150 kg batch every 10 minutes, which means sustained feed to the extruder depends on whether you run single or staggered batches ahead of the hopper. The high-temperature roaster uses 24 far infrared heater units across a 3.5-meter belt to pull surface and internal moisture down to storage-stable levels, but gas type and heating value at your facility affect whether the rated 6.8 m³/h consumption figure holds [NEED_CITE: industrial gas heating value variations across export markets].
The cooling machine then brings the dried TVP to a safe handling temperature before packing. If any station in this chain is undersized, the bottleneck shows up within the first hour of production, not during the factory acceptance test.
Reading the Power and Dimension Data Against Your Factory Floor
The installed power figures — 85 kW for the MT65, 120 kW for the MT70, and 195 kW for the MT85 — represent peak draw across all stations, while actual consumption runs lower during steady-state operation. For factory electrical planning, the key number is actual power: 65 kW, 90 kW, or 165 kW depending on model, plus any auxiliary loads from dust collection or compressed air. Line length stretches from 18 meters on the MT65 to 24 meters on the MT85, with the larger configuration also requiring a wider corridor at 3.5 meters to accommodate the dryer and cooling conveyors.
Barrel temperature profiling across the twin-screw extruder zones directly affects protein gelatinization. Too low a temperature in the feed zone and the meal does not hydrate uniformly; too high in the metering zone and the die face builds carbonized deposits that require frequent stoppages. The stainless steel construction throughout all machinery contact surfaces helps maintain hygiene standards and reduces corrosion when processing high-protein materials that tend to stick and degrade on contact with mild steel.
The Hidden Cost of Skipping a Raw Material Trial
I learned this the hard way. A buyer in Southeast Asia sent a purchase order for a TVP line, and we set screw speed and barrel temperatures based on standard soybean meal specifications. When their actual raw material arrived — a defatted soy flour with a noticeably different protein ratio — the fibrous structure came out weak and the chunks crumbled during drying. We spent four days adjusting temperature profiles and screw element arrangements before the output met their texture standard. That delay would have been a week of lost production if it had happened on-site instead of in our testing workshop.
Running your raw material before shipment is not a courtesy — it is the only way to lock in screw configuration and die design against your specific input [NEED_CITE: protein content variation in commercial soybean meal batches]. Skipping this step means commissioning becomes product development, and your installation engineers leave before the line is dialed in.
Why Sourcing the Full Equipment Range from One Builder Helps
Throughput matching across every station eliminates the finger-pointing that happens when a mixer vendor, an extruder vendor, and a dryer vendor each blame the other for a bottleneck. Screw configuration records are kept against your raw material, so reordering wear parts does not require a new round of trials. The in-house testing workshop allows your material to run through the actual twin-screw extruder and dryer before the line ships. Documentation covers the electrical schematic with confirmed voltage and frequency for your market, so the local electrician does not discover a mismatch on installation day. Stainless steel construction across all stations means maintenance schedules and spare parts lists stay consistent regardless of which station you are servicing.
Documentation & Verification
- Line layout drawing with station-by-station throughput calculation for your target TVP output
- Screw and die configuration record matched to your soybean meal or peanut meal specification
- Trial run report produced on your raw material in the testing workshop before dispatch
- Electrical schematic with voltage and frequency confirmed for your destination market
- CE declaration of conformity and ISO certificate for the complete line
- Wear parts list identifying screws, dies, and heater elements with replacement intervals
Installation, Commissioning & Support
- MT85 line requires a 24-meter clear floor length with 4.3-meter headroom for the dryer exhaust routing
- Power supply must support 195 kW installed load on the MT85 with a dedicated breaker panel
- Twin-screw extruder ships with barrel sections separated; reassembly requires alignment verification on your foundation
- First production run includes barrel temperature profiling and screw speed tuning against your raw material batch
- Operator training covers die changeover, mixer batch timing, and roaster belt speed adjustment
- Spare screw elements and die plates shipped with initial order to cover the first replacement cycle
What We Need to Configure Your Line
To size each station correctly, we need your raw material specification including protein content and moisture level, your target daily output in kilograms, and the available floor length and ceiling height in your production hall. Local voltage and frequency determine motor and heater winding specifications, and your preferred control language affects the HMI configuration. If you already have upstream milling or downstream packing equipment, share the interface dimensions so we can match conveyor heights and feed rates.
Frequently Asked Questions
Q: How is output capacity verified, and what raw material conditions does each rating assume?
A: Each model’s capacity figure is based on specific raw material and moisture conditions that must be confirmed against your actual input. We run your material in our testing workshop to validate throughput, fiber structure, and moisture content at the dryer exit before quoting a firm output number for your line configuration.
Q: What supporting stations are needed to avoid bottlenecking at a given extruder capacity?
A: The powder mixer, roaster, and cooling conveyor are all sized to match the extruder model you select. The mixer batch cycle and the dryer belt length must sustain the extruder’s steady-state output without material backlog, which is verified in the line layout and capacity calculation before the order is finalized.
Q: How do screw configuration and die design change between soybean meal and peanut meal?
A: Different raw materials have different protein content, fat residue, and fiber characteristics, which affect compression ratio and shear requirements inside the barrel. We adjust screw element arrangement, barrel temperature zones, and die aperture geometry to maintain consistent fiber structure when switching between materials.
Q: What voltage and frequency options are available for different markets?
A: Voltage and frequency are confirmed during the specification stage and configured before production. Motors, heaters, and the control panel are all wound and wired to match your facility’s supply, and the HMI language is set to your preference before the line ships.
Q: What is the footprint of each configuration, and how should utilities be planned?
A: Line length ranges from 18 meters on the MT65 to 24 meters on the MT85, with width up to 3.5 meters for the larger model. Gas supply type and heating value must be confirmed for the roaster, and compressed air connections are needed for pneumatic gates and cleaning across several stations.