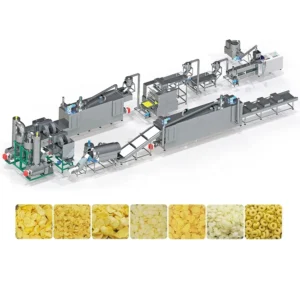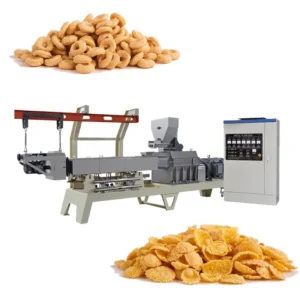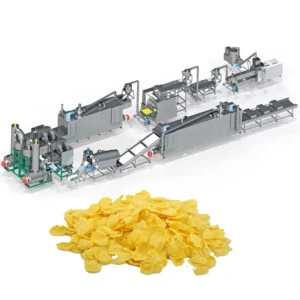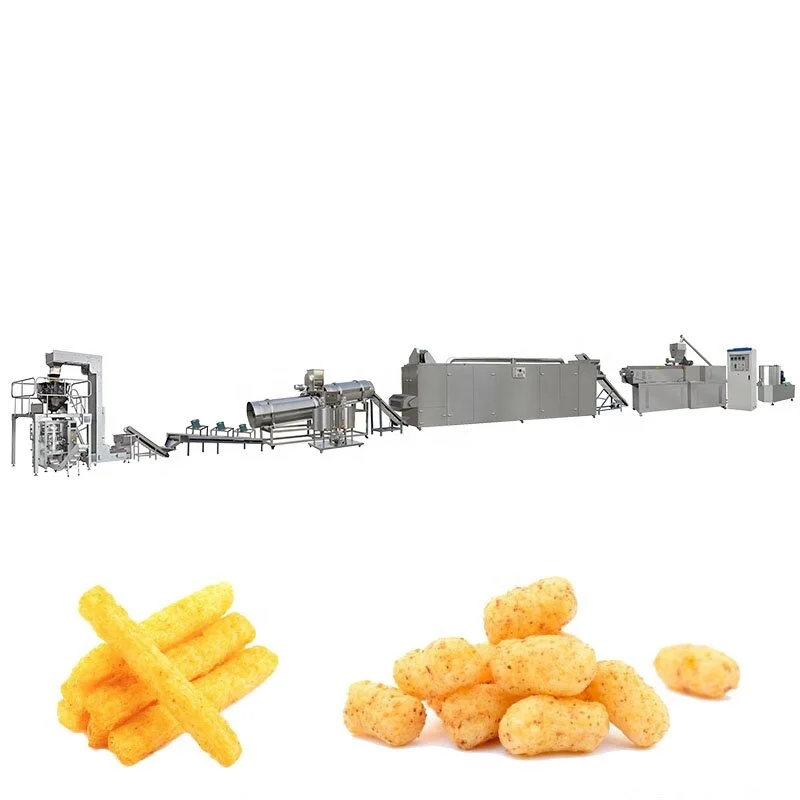
Throughput-Matched Design — Every station from the mixer to the cooling conveyor is sized to the same capacity target, so the extruder never waits on a bottleneck downstream.
Technical Specifications
| Parameter | Value |
|---|---|
| Model | MT75 |
| Product Type | Corn Flakes Extrusion Production Line |
| Screw Type | Twin Screw |
| Installed Power | 210 kW |
| Power Consumption | 150 kW |
| Output Capacity | 300–500 kg/hr (basis not stated in source — confirm raw material type, moisture content and product format) |
| Overall Dimensions | 45 × 1.5 × 3.5 m |
| Control System | PLC control system |
| Flaking Machine | Hydraulic double-roller system with infrared sensor temperature control |
| Roasting Oven | Hot air roasting with conciliation burner, dual circulating fans, cyclone dust removal |
| Dryer Heating Source | Gas or Electric |
| Coating System | Double tumble sugar melter, elevator, coating drum, spraying nozzle |
| Screw Material | Wear-resistant alloy with automatic lubrication and cooling |
| Basic Material Compatibility | Corn, rice, wheat, oat, barley powder |
| Assembly State | Complete line from mixing to packing |
Application Suitability
| Application | Material or Output |
|---|---|
| Natural corn flakes production | Corn grits or corn flour with controlled moisture |
| Sugar-coated breakfast cereal | Corn, wheat, or oat base with syrup coating |
| Multi-shape extruded cereal | Rice, wheat, or barley powder — ball, tube, ring, star, wheel formats via die swap |
| Fortified cereal for nutrition programs | Blended grain flour with vitamin and mineral premix |
| High-fiber or whole-grain flakes | Whole corn or oat flour requiring adjusted screw configuration |
Why "500 kg/hr" Means Nothing Without the Raw Material
Capacity on corn grits at 15% moisture is a different line than capacity on high-fiber oat flour at 22% moisture — and most quotations never specify which one.
I once walked into a breakfast cereal plant in Jiangsu where the extruder was running well below nameplate output. The operator had been told the line was rated for a certain throughput, but nobody had asked what their actual corn-to-oat ratio was. High-fiber material resists expansion differently, and the screw configuration installed was set up for pure corn grits. The corn flakes machine full equipment range they received was perfectly capable — just not configured for their recipe. When the supplier finally swapped the screw elements and adjusted the barrel temperature zones, throughput came back in line. That plant lost weeks of production before the mismatch was diagnosed [NEED_CITE: raw material variability and extruder throughput correlation].
Station-by-Station Throughput Alignment
A breakfast cereal production line equipment package is only as fast as its slowest station. The MT75 line addresses this by sizing the flaking machine, dryer, roasting oven, and coating drum to the same throughput window as the twin-screw extruder. The hydraulic flaking unit uses separate motors for each roller, which maintains consistent flake thickness even as material flow varies slightly across batches. If the dryer is undersized relative to the extruder, wet flakes pile up and clump; if the roasting oven is oversized, energy waste accumulates across every shift.
How the Coating and Roasting Stages Affect Final Texture
The hot air roasting oven uses a conciliation burner with two independent circulating fans and a cyclone dust removal device. This arrangement controls moisture draw-down uniformly across the pan, which is what gives the final flake its crispness rather than a leathery chew. After roasting, the sugar coating system runs a double tumble melter feeding into a dedicated spraying nozzle and coating drum. Even coverage matters here — a patchy sugar layer causes some flakes to caramelize while others remain bare, and downstream packing stations then face a product that does not meet visual spec [NEED_CITE: breakfast cereal moisture and shelf stability requirements].
Reading the Spec Sheet Beyond Nameplate Numbers
The 210 kW installed power and 150 kW consumption figures tell you two different things. Installed power is the combined motor rating across the extruder, flaking unit, dryers, and fans — the peak the electrical panel must handle. Consumption is what the line actually draws during steady-state operation, which determines your per-hour energy cost. The PLC control system ties these stations together so that barrel temperature profiles, roller pressure, and oven zones respond to real-time feedback rather than running on fixed settings. For producers switching between natural and sugar-coated formats, this means recipe changes happen at the control panel without manual valve adjustments across the line. The 45-meter overall length is a factor in workshop planning — this is not a compact footprint, and the utility runs for gas, compressed air, and electrical must be mapped before the equipment arrives.
The Hidden Cost of an Unmatched Line
I have seen lines where the extruder was correctly specified but the dryer was one size smaller to cut the quotation total. The result was a bottleneck that forced the extruder to idle every few minutes, and the wet flakes sitting in the dryer too long came out with inconsistent moisture. In another case, a roasting oven without cyclone dust removal sent fine particulate back into the product stream, creating a quality hold on every batch [NEED_CITE: food processing dust control and product contamination]. When stations are sourced from different vendors, nobody takes responsibility for the gap between them. The throughput mismatch only shows up during commissioning, and by then the equipment is already bolted to the floor.
What This Purchase Actually Includes
The line layout and capacity calculation document shows how every station’s throughput was matched before the quotation was finalized. The screw configuration and die design are specified to your raw material and target flake format, not copied from a standard build. The in-house testing workshop runs your actual corn, wheat, or oat flour before shipment, so expansion behavior and flake thickness are confirmed before the machines leave the factory. Twin-screw expertise across corn flakes, granola, and fortified cereal applications means the engineering team has seen how different grain blends behave under shear and heat. Electrical schematics and voltage confirmation are completed before production starts, so the control panel matches your local supply when it arrives.
Documentation & Verification
- Line layout showing throughput match from mixing through cooling and packing
- Screw configuration record mapped to your specific grain blend and moisture level
- Electrical schematic with voltage and frequency confirmed before production
- Trial run report on your raw material documenting flake thickness and expansion
- Factory test record with PLC screen captures at each station
- CE declaration of conformity and ISO certificate for the complete line
Installation, Commissioning & Support
- 45-meter line footprint requires level concrete floor with anchor points mapped to layout drawing
- 210 kW installed power needs dedicated breaker panel; confirm local voltage and three-phase frequency before wiring
- Arrives in modular sections; extruder, flaking unit, and oven assembled and aligned on site
- First-run commissioning includes barrel temperature profiling and hydraulic roller pressure calibration
- PLC interface language set to operator preference during training session
- Wear parts list covers screws, dies, and flaking rollers with replacement intervals documented
What to Include in Your Inquiry
Send the specific grain blend you intend to run — corn, wheat, oat, or a mix — along with the moisture content of your incoming flour. Confirm your local voltage, phase, and frequency so the electrical panel is built to match. If your workshop has height restrictions or existing upstream equipment such as a milling system, include those dimensions so the layout accounts for them.
Frequently Asked Questions
Q: How is line capacity verified against the buyer’s specific raw material and moisture level?
A: Before shipment, your raw material is run through the extruder and flaking station in the in-house testing workshop. The trial run report documents expansion ratio, flake thickness, and actual throughput at your moisture level, so capacity is confirmed on your recipe rather than quoted from a generic benchmark.
Q: What voltage, frequency, and control language options are confirmed before production?
A: The electrical schematic and voltage confirmation document is finalized before manufacturing starts. The PLC interface language is set to the operator’s preference, and the control panel components are selected to match local three-phase supply standards.
Q: How are extruder, dryer, and coating station capacities matched to avoid bottlenecks?
A: The line layout document calculates throughput for each station based on your target output and raw material. Every dryer, oven, and coating drum is sized to handle the extruder’s output with a margin, so no single machine forces the rest of the line to idle.
Q: Which spare wear parts are supplied and what is the replacement schedule?
A: The wear parts list covers twin-screw elements, extrusion dies, and flaking rollers. Replacement intervals depend on material abrasiveness and operating hours, and are documented in the operation manual after your specific raw material has been evaluated during the trial run.