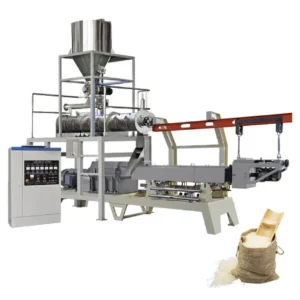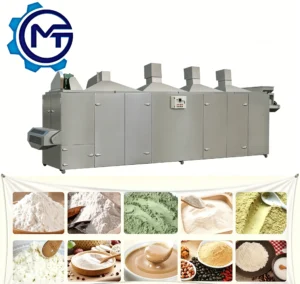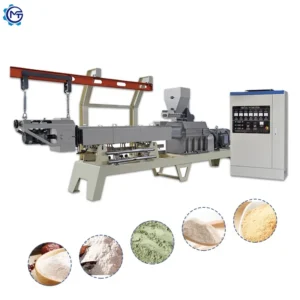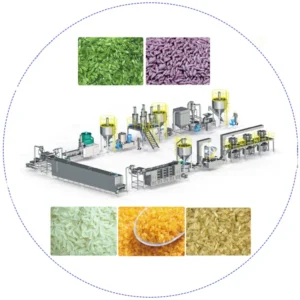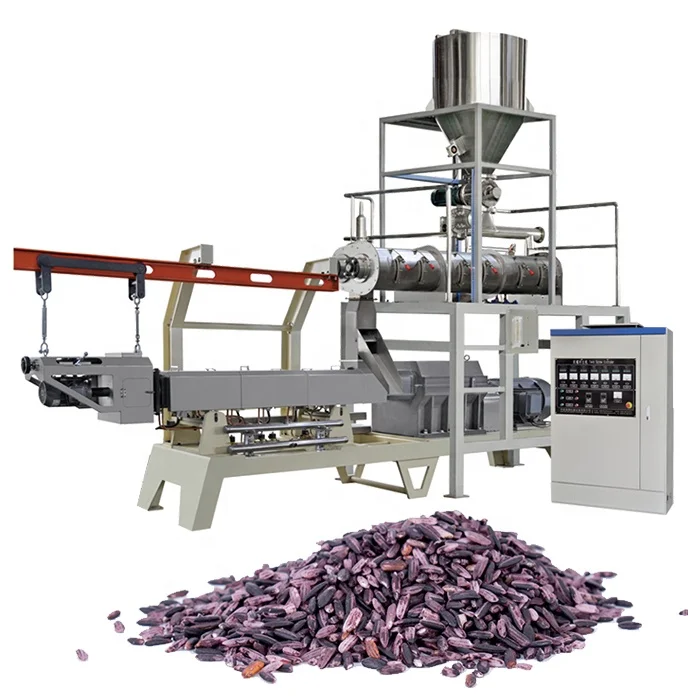
Line Throughput Matching — Every station from mixer to packer in the Fortified Rice Kernel Extrusion Line full equipment range is sized to the extruder output, preventing bottlenecks across the production sequence.
Technical Specifications
| Parameter | Value |
|---|---|
| Model | MT65 / MT70 / MT85 / MT75 / MT95 |
| Product Type | Fortified Rice Kernel Extrusion Line |
| Screw Type | Twin Screw |
| Installed Power (MT65) | 85 kW |
| Power Consumption (MT65) | 60 kW |
| Output Capacity (MT65) | 80–100 kg/h (basis not stated in source) |
| Installed Power (MT70) | 120 kW |
| Power Consumption (MT70) | 85 kW |
| Output Capacity (MT70) | 100–120 kg/h (basis not stated in source) |
| Installed Power (MT85) | 235 kW |
| Power Consumption (MT85) | 165 kW |
| Output Capacity (MT85) | 200–300 kg/h (basis not stated in source) |
| Installed Power (MT75) | 180 kW |
| Power Consumption (MT75) | 135 kW |
| Output Capacity (MT75) | 300–500 kg/h (basis not stated in source) |
| Installed Power (MT95) | 260 kW |
| Power Consumption (MT95) | 195 kW |
| Output Capacity (MT95) | 800–1000 kg/h (basis not stated in source) |
| Overall Dimensions (MT65) | 28 × 1.2 × 2.2 m |
| Overall Dimensions (MT70) | 30 × 1.5 × 2.2 m |
| Overall Dimensions (MT85) | 34 × 3.5 × 4.3 m |
| Overall Dimensions (MT75) | 32 × 3.5 × 4.3 m |
| Overall Dimensions (MT95) | 36 × 3.5 × 4.3 m |
| Control System | Frequency speed controlling; PLC / MCC availability to be confirmed |
| Feeding System | Single or twin screw feeding, selected by material type |
| Lubrication | Automatic |
| Cooling System | Automatic |
| Dryer Type | Mesh belt circulation dryer |
| Heating Source (Dryer) | Electric or gas |
| Line Stations | Mixing → Extruding → Vibrating → Low Temperature Drying → Cooling → High Temperature Roasting → Cooling → Packing |
| Raw Material Compatibility | Broken rice, rice, corn, millet, wheat, oats, buckwheat, bean, starch; vitamin and mineral as partial ingredients |
| Standards | CE, ISO |
Application Suitability
| Application | Material or Output |
|---|---|
| Fortified rice kernel production | Broken rice blended with vitamins and minerals |
| Artificial rice processing | Corn, millet, wheat, oats, buckwheat starch base |
| Nutritional rice for food security programmes | Micro-nutrient-enriched rice matrix |
| Broken rice value upgrading | Reconstituted rice kernels from milling by-products |
Why a Capacity Number Without Raw Material Context Misleads
Throughput is only meaningful when tied to the exact raw material, moisture content, and die geometry you will run.
I once stood beside a running extruder that was supposed to deliver steady output on standard rice flour, yet the actual feedstock was a pre-gelatinised starch blend with considerably higher viscosity. The barrel temperature profile collapsed, the product density drifted outside specification, and five days were lost before screw configuration and feed rate were re-calibrated on site. A capacity figure quoted in a brochure says nothing about what happens when your material behaves differently. [NEED_CITE: starch gelatinisation behaviour in twin-screw extrusion]
How the Twin-Screw Platform Handles Starch and Protein Blends
The twin-screw extruder in the Fortified Rice Kernel Extrusion Line full equipment range uses independently controlled barrel zones and interchangeable screw elements to manage the shear and residence time required for starch gelatinisation. When the recipe includes partial vitamin and mineral ingredients, the screw profile can be adjusted to prevent thermal degradation of heat-sensitive micro-nutrients while still achieving full starch cooking. Automatic lubrication and cooling keep the gearbox and barrel within safe operating windows during extended runs.
Drying and Roasting Stages That Follow the Extruder
After extrusion, the wet kernels enter a mesh belt circulation dryer where frequency-controlled belt speed sets the dwell time. Electric or gas heating is chosen according to the utility infrastructure available at the installation site. Once moisture is reduced, the kernels pass through a cooling conveyor and then a high-temperature roasting stage that develops the final texture and shelf stability. [NEED_CITE: moisture reduction targets for extruded rice analogues] Each station is selected to match the extruder throughput, so wet product does not accumulate upstream of the dryer.
Reading the Specification Sheet as a Process Engineer
Installed power on the MT65 sits at 85 kW with an operating draw around 60 kW, while the MT95 requires 260 kW installed and draws roughly 195 kW during steady production. These figures tell you the electrical service capacity needed before any cable is pulled. Overall dimensions stretch from 28 m line length on the MT65 to 36 m on the MT95, meaning floor space and utility drop points must be planned early. The feeding system switches between single and twin screw depending on whether the raw material is free-flowing granular or cohesive powder, a detail that directly affects feed consistency and therefore product density uniformity.
What Happens When Stations Are Not Capacity-Matched
Sourcing the extruder from one supplier and the dryer from another often creates a throughput mismatch where wet kernels pile up waiting for drying capacity, or the dryer runs half-empty wasting energy. The same applies to the roasting and cooling stages; undersized coolers let hot kernels reach the packing station where residual heat causes condensation inside bags. [NEED_CITE: post-drying moisture equilibration in extruded cereal products] These problems surface only after commissioning, when re-engineering is expensive and delays market launch.
Why Procurement from a Single Equipment Range Matters
The Fortified Rice Kernel Extrusion Line full equipment range keeps every station under one specification responsibility, so line layout and capacity calculation are produced as a single document rather than stitched together from separate vendor quotes. Screw configuration and die design are specified to the buyer’s raw material, not copied from a generic build. An in-house testing workshop runs trial production on the customer’s actual feedstock before shipment, catching viscosity or gelatinisation surprises at the factory instead of on the customer’s floor. Voltage, frequency, and control language are confirmed before production starts, avoiding commissioning delays. Pre-sales consultation carries through to on-site installation, operator training, and wear parts scheduling.
Documentation & Verification
- Line layout drawing with station-by-station throughput matched to your target output
- Screw and die configuration record tied to your specific raw material blend
- Electrical schematic with voltage and frequency confirmed for your local supply
- Factory trial run report produced on your actual feedstock before dispatch
- CE declaration of conformity covering the complete line assembly
- Operation and maintenance manual with wear parts replacement intervals
Installation, Commissioning & Support
- Floor space planning based on line dimensions from 28 m to 36 m depending on model selection
- Dedicated electrical circuit sized to installed power up to 260 kW for the MT95 configuration
- Equipment shipped in modular sections to fit standard container loading and site access constraints
- First-run parameter setting covering barrel temperature profile, screw speed, and feed rate calibration
- Operator training on control interface language confirmed before production begins
- Wear parts list with screw element and die replacement schedule for the first maintenance cycle
Preparing Your Inquiry
When requesting a quotation for the Fortified Rice Kernel Extrusion Line full equipment range, share the exact raw material composition including starch source and micro-nutrient addition ratios, your target daily output in kilograms, and the local voltage and frequency standard. Specify whether electric or gas heating is preferred for the dryer based on your site utility conditions, and indicate the control language your operators require.
Frequently Asked Questions
Q: What capacity range does each extruder model cover, and on what raw material basis?
A: Models range from MT65 to MT95 with varying output figures shown in the specification table, yet those figures carry a basis-to-be-confirmed note because actual throughput depends on the raw material composition, moisture content, and die geometry you will run. A trial on your feedstock establishes the real capacity.
Q: Which supporting stations are available and how are they matched to extruder throughput?
A: The line includes mixing, vibrating, low-temperature drying, cooling, high-temperature roasting, a second cooling stage, and packing. Each station is sized so that material flow remains continuous without accumulation or idle time between the extruder and the dryer.
Q: How is the dryer heating source selected between electric and gas?
A: The choice depends on the utility infrastructure at your facility. Sites with reliable natural gas supply and higher electricity tariffs typically favour gas heating, while locations with limited gas access or stricter emissions regulations opt for electric elements. Both options use the same mesh belt circulation design.
Q: What voltage, frequency, and control language options are confirmed before shipment?
A: Electrical specifications are locked during the quotation stage to match your local grid standard, whether 50 Hz or 60 Hz. Control interface language is confirmed at the same point so that operators receive documentation and HMI screens in the required language from day one.
Q: What spare wear parts should be stocked from the first production run?
A: Screw elements, die plates, and cutter bearings experience normal wear during continuous extrusion. A wear parts list is supplied with the quotation so that the first replacement set is available before the original components reach end of service life.