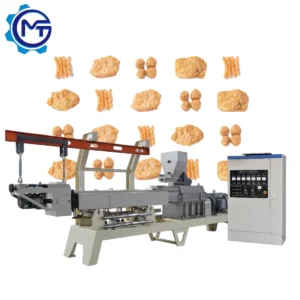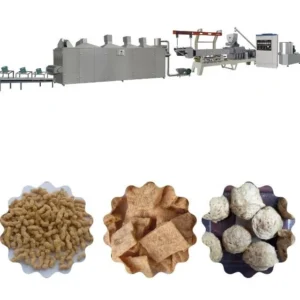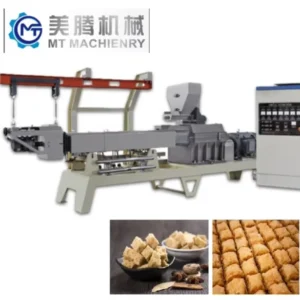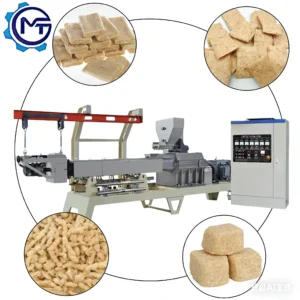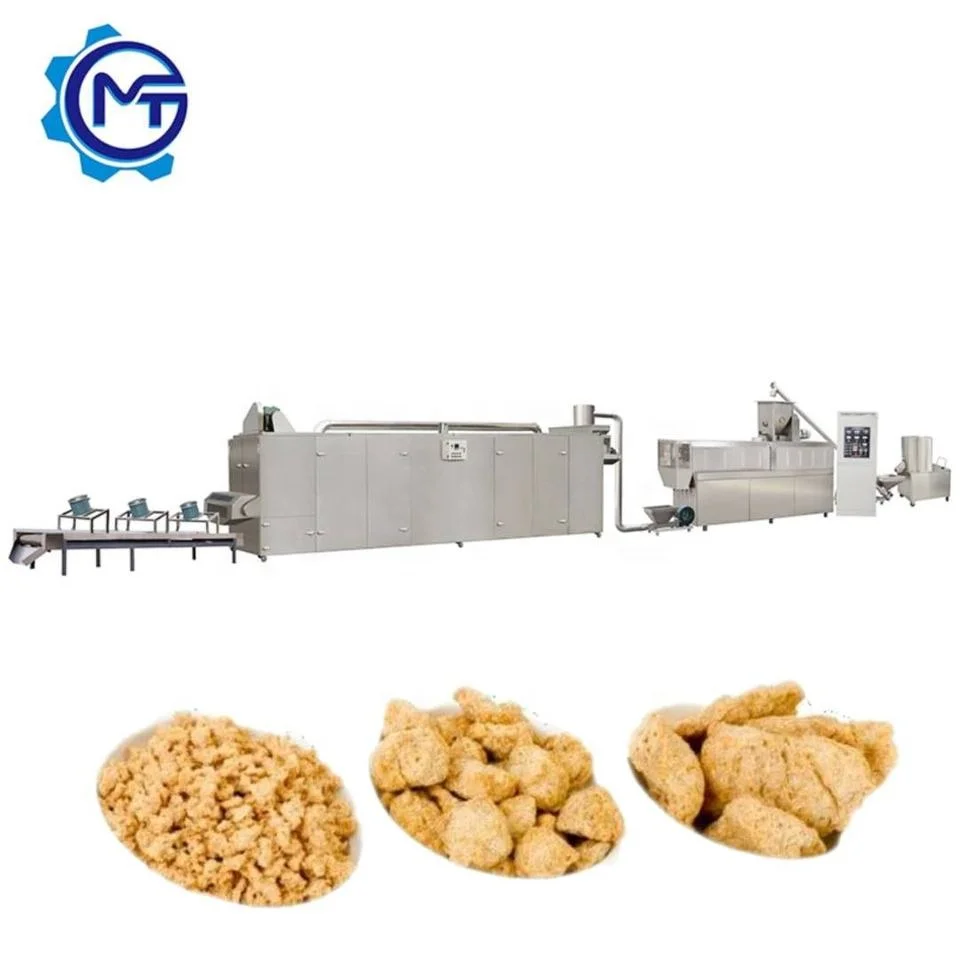
Integrated line throughput — every mixer, extruder, dryer and cooler in this TVP processing range is capacity-matched so a single station never bottlenecks the entire plant output.
Technical Specifications
| Parameter | Value |
|---|---|
| Product Type | Textured Soy Protein Extrusion Line |
| Model Options | MT65 / MT70 / MT85 |
| Screw Type | Twin-screw |
| Installed Power (MT65 / MT70 / MT85) | 85 kW / 120 kW / 195 kW |
| Real Power Consumption (MT65 / MT70 / MT85) | 65 kW / 90 kW / 165 kW |
| Overall Dimensions (MT65) | 18000 × 1300 × 2300 mm |
| Overall Dimensions (MT70) | 20000 × 1500 × 2400 mm |
| Overall Dimensions (MT85) | 24000 × 3500 × 4300 mm |
| Mixer Tank Volume | 150 kg per batch |
| Mixer Output | 300–600 kg/h |
| Mixer Rotary Speed | 385 rpm |
| Mixer Mixing Time | 10 min per batch |
| High-temperature Roaster Output | 300–400 kg/h |
| High-temperature Roaster Belt Effective Length | 3.5 m |
| High-temperature Roaster Gas Consumption | 6.8 m³/h |
| Cooling Machine Capacity | 200–300 kg/h (source value — verify against manufacturer catalog) |
| Output Capacity (MT65) | 150–200 kg/h (basis not stated in source — confirm raw material formulation and moisture content) |
| Output Capacity (MT70) | 200–300 kg/h (basis not stated in source — confirm raw material formulation and moisture content) |
| Output Capacity (MT85) | 600–800 kg/h (basis not stated in source — confirm raw material formulation and moisture content) |
| Main Construction Material | Stainless steel (food-grade contact surfaces) |
| Control System | PLC and MCC |
| Line Stations | Raw material preparation → Mixing → Conveying → Extrusion → Conveying → Drying → Cooling → Packing |
| Standards | CE, ISO |
Application Suitability
| Application | Material or Output |
|---|---|
| Plant-based meat cutlets and chunks | Low-temperature soybean meal, peanut meal |
| Vegetarian mince and crumbles | Soy protein isolate and concentrate blends |
| Textured protein for sausages and canned food | Defatted soy flour with varied moisture content |
| Meat analogues for quick-frozen meals | Soy and peanut meal blends with starch modifiers |
| Vegetarian ham and deli slices | High-protein soy meal with fibre-forming additives |
Why Nominal Output Figures Mislead on a Textured Soy Protein Production Line Full Equipment Range
Real throughput depends on your specific meal formulation, moisture level and target fibre density — not on a generic catalog number.
I spent two weeks re-tuning a plant-based protein line because the buyer’s soybean meal had a different protein concentration and particle size than the standard test material we used during the initial trial. The fibre structure came out completely different from what their downstream sausage processor expected. Every textured soy protein production line full equipment range should be validated against your exact raw material before any configuration is locked in. When a supplier quotes capacity without asking for your formulation data, that number is essentially a guess [NEED_CITE: extrusion throughput variables in high-moisture protein processing].
How Screw Configuration Defines Fibre Structure in TVP
The twin-screw design in this line allows precise control over shear, residence time and temperature gradient inside the barrel. For soy-based formulations, the screw profile determines how thoroughly the protein molecules align into the layered fibre structure that mimics animal meat. Different die geometries then shape the extrudate into chunks, flakes or granules. Each configuration is specified against the buyer’s raw material and target product rather than pulled from a generic build. A textured soy protein production line full equipment range must match screw elements to formulation — changing even one element spacing can shift fibre density noticeably.
Matching Station Capacity to Prevent Line Bottlenecks
A common failure mode in assembled lines is an extruder producing material faster than the dryer can handle, causing wet product to pile up on the conveyor and spoil. The mixer in this range processes batches of up to 150 kg with a 10-minute cycle, feeding downstream at a rate aligned with the selected extruder model. The high-temperature roaster belt provides 3.5 metres of effective drying length, and the cooling machine follows at a matched rate [NEED_CITE: thermal processing requirements for textured vegetable protein stabilisation]. When throughput is calculated across every station before build, you avoid the situation where one oversized machine sits idle while another station chokes the entire flow.
Reading the Spec Sheet: What Matters for Your Production Floor
The installed versus real power gap across the three extruder models reflects actual energy draw under load — the MT85 draws 195 kW installed but consumes around 165 kW during continuous extrusion, which affects your transformer sizing and per-shift electricity cost. Overall line length stretches from 18 metres on the MT65 up to 24 metres on the MT85, so your floor plan needs to account for the full footprint including material infeed and discharge zones. The stainless steel contact surfaces across all stations meet food-grade requirements, which matters when auditors check material traceability. PLC and MCC control gives operators recipe memory and alarm logging, so parameter changes between soy and peanut formulations can be stored and recalled rather than re-entered manually each shift.
The Cost of Skipping a Pre-Shipment Trial Run
When a textured soy protein production line full equipment range arrives at your facility and the first test run produces dense, rubbery chunks instead of layered fibres, you face weeks of screw reconfiguration and die swaps on your own production floor. That downtime burns through raw material, delays customer orders and erodes confidence in the investment. An in-house trial on your actual soybean or peanut meal formulation — with documented screw configuration, barrel temperature profile and die selection — shifts that risk to the testing workshop before the machines ever leave the factory [NEED_CITE: pre-shipment verification standards for food extrusion equipment].
What Distinguishes This Equipment Range
Every station from the 150 kg batch mixer through the twin-screw extruder to the 3.5-metre roaster belt is sourced from a single supplier, so capacity calculations span the entire line rather than individual machine datasheets. Screw configuration and die design are specified against your raw material sample and target fibre texture, not copied from a default assembly. The in-house testing workshop runs your formulation before shipment, producing a trial report you can reference during commissioning. Food-grade stainless steel contact surfaces run through mixing, extrusion, drying and cooling stations. Electrical schematics arrive with voltage, frequency and control language confirmed to your plant’s specification before production starts.
Documentation & Verification
- Line layout drawing showing capacity match across mixer, extruder, dryer and cooler stations
- Screw and die configuration record tied to your soybean or peanut meal sample
- Factory test report from in-house trial run on customer-supplied raw material
- Electrical schematic with confirmed voltage, frequency and PLC language for your facility
- CE declaration of conformity and ISO certificate for export compliance
- Wear parts list covering screws, dies and barrel liners with replacement intervals
Installation, Commissioning & Support
- Floor space allocation based on line length up to 24 m for MT85 plus infeed and discharge zones
- Dedicated power circuit sized to 195 kW installed capacity for the largest extruder model
- Modular station delivery allowing phased assembly in facilities with limited overhead clearance
- First-run parameter setting using trial report data to shorten commissioning on your actual formulation
- Operator training covering PLC recipe storage for switching between soy and peanut meal batches
- Spare screw elements and die inserts supplied with recommended replacement schedule
What to Prepare Before Requesting a Quotation
To configure the right textured soy protein production line full equipment range for your plant, share your raw material specification including protein content and particle size, your target product format such as chunks, mince or cutlets, and your daily throughput requirement. Let us know your facility voltage and frequency, preferred control language, and available floor space with ceiling height constraints. If possible, send a raw material sample so we can run a trial in the testing workshop and confirm fibre structure and density before finalising the configuration.
Frequently Asked Questions
Q: How is output capacity verified on my specific soybean or peanut meal formulation?
A: Before shipment, your raw material sample is run through the extruder in the in-house testing workshop. The trial documents screw configuration, barrel temperature profile, moisture level and die selection. A capacity figure is then confirmed based on your actual formulation rather than a generic reference material, so the quoted throughput reflects real production conditions.
Q: Which extruder model fits my target throughput and floor space?
A: Model selection depends on your required hourly output and available line length. The MT65 fits an 18-metre footprint, the MT70 extends to 20 metres, and the MT85 requires up to 24 metres. We cross-reference your target capacity against your formulation’s behaviour during the trial run to recommend the model that holds consistent output without oversized idle capacity.
Q: How are dryer and cooler capacities matched to the extruder to avoid line bottlenecks?
A: Each station’s throughput is calculated together during line design. The mixer batch cycle, extruder output, roaster belt length and cooling machine capacity are all aligned so material flows continuously. If one station processes faster than another, the configuration is adjusted before build rather than discovered during commissioning.
Q: What screw configuration and die design is used for my target fibre texture and density?
A: Screw element spacing, kneading block arrangement and die aperture are selected based on your raw material’s protein content and your target product format. The trial run tests multiple configurations on your sample to identify the combination that produces the correct layered fibre structure and density for your application.
Q: What spare wear parts are included and what is the replacement schedule?
A: The initial supply includes spare screw elements, die inserts and barrel liners. A wear parts list specifies expected service intervals based on your production volume and raw material abrasiveness. Replacement parts remain available through ongoing supply so your line does not halt waiting for components when the first changeover is due.