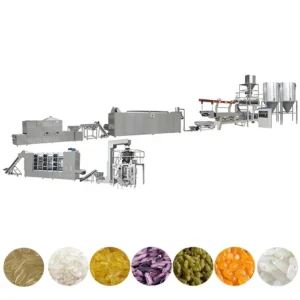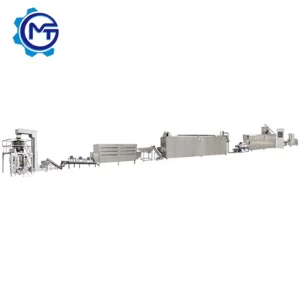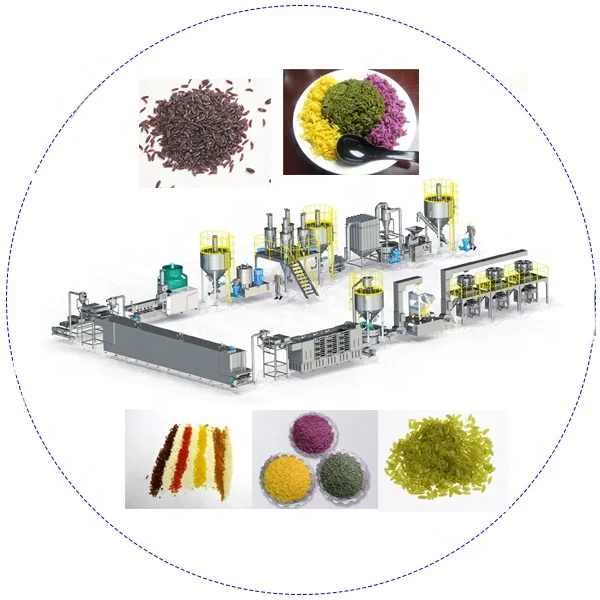
Turnkey Fortified Rice Line Integration — Every station from batching to packing is throughput-matched under one supplier, eliminating the idle capacity and bottlenecks that plague multi-vendor setups.
Technical Specifications
| Parameter | Value |
|---|---|
| Product Type | Fortified Rice Kernel Extrusion Production Line |
| Models Available | MT65 / MT70 / MT85 / MT75 / MT95 |
| Screw Type | Twin-screw |
| Installed Power | 85 kW (MT65) / 120 kW (MT70) / 235 kW (MT85) / 180 kW (MT75) / 260 kW (MT95) |
| Power Consumption | 60 kW (MT65) / 85 kW (MT70) / 165 kW (MT85) / 135 kW (MT75) / 195 kW (MT95) |
| Output Capacity | 80–100 kg/h (MT65) / 100–120 kg/h (MT70) / 200–300 kg/h (MT85) / 300–500 kg/h (MT75) / 800–1000 kg/h (MT95) (basis not stated in source — confirm raw material formulation and moisture content before quoting) |
| Overall Dimensions | 28×1.2×2.2 m (MT65) / 30×1.5×2.2 m (MT70) / 34×3.5×4.3 m (MT85) / 32×3.5×4.3 m (MT75) / 36×3.5×4.3 m (MT95) |
| Control System | Frequency speed control, automated operation (PLC/MCC availability to be verified) |
| Feeding System | Single or double screw feeding selectable by material |
| Screw Material | Wear-resistant alloy (specific grade to be confirmed) |
| Drying Oven Heating Source | Electric or gas |
| Drying Method | Circulation drying with mesh belt, frequency motor speed control |
| Line Stations | Mixing, extruding, vibrating, low-temperature drying, cooling, high-temperature roasting, cooling, packing |
| Assembly State | Complete turnkey production line |
| Voltage & Frequency | Customized to buyer’s local standard (value to be confirmed before order) |
| Standards | CE certified, ISO certified |
Application Suitability
| Application | Material or Output |
|---|---|
| Government-mandated nutrition programmes | Broken rice and rice bran blended with vitamin and mineral premix for WFP-spec fortified kernels |
| Rice mill by-product conversion | Broken rice and rice bran reprocessed into value-added artificial rice with natural cooking behaviour |
| Multi-grain and gluten-free rice analogues | Corn, buckwheat, oat, millet, and wheat formulations for specialty food markets |
| Infant and paediatric nutrition bases | Starch-rich blends with added micronutrients for porridge and weaning food production |
| Institutional feeding programme supply | High-volume fortified kernels from locally available grain bases for school meal and relief programmes |
Why "Nominal Output" Numbers Mislead Fortified Rice Kernel Extrusion Machine Manufacturer Buyers
The capacity plate on an extruder means nothing until it is tested against your specific grain blend and micronutrient load.
A fortified rice line rated at a certain throughput on pure corn starch may lose considerable output when the formulation shifts to a broken-rice base loaded with iron, zinc, and vitamin A premix. The added mineral particles change melt viscosity inside the barrel, alter the gelatinisation window, and push the die pressure outside the expected range. I watched a line in Southeast Asia stall repeatedly during the first week because the micronutrient premix contained calcium carbonate at levels the original screw configuration could not push through the die. The buyer had approved the quotation based on a capacity figure that assumed a clean starch feed [NEED_CITE: raw material formulation impact on twin-screw extruder output].
Matching Screw Geometry to Your Grain Base
Every grain formulation behaves differently inside the barrel. A broken-rice base gelatinises at a different temperature window than a corn-dominant blend, and adding fiber-rich components like oat or buckwheat shifts the shear requirement. The MT series offers five extruder tiers so the screw configuration and die design can be set to match the buyer’s exact formulation rather than forcing a generic build onto a specialized product. Getting the screw element sequence right on a fortified rice kernel extrusion machine manufacturer line determines whether kernels hold their shape during drying or crack and produce excess fines.
Throughput Matching Across Every Station
An extruder that pushes out product faster than the dryer can handle creates a queue of wet kernels that stick together and deform on the mesh belt. The line layout addresses this by sizing the vibrating conveyor, low-temperature dryer, cooling belt, and high-temperature roaster to the extruder’s verified output on the buyer’s material. Frequency-controlled motors on the drying oven belt allow moisture removal to be tuned in real time [NEED_CITE: circulation drying principles for extruded food products]. This station-to-station matching is what separates a line that runs continuously from one that requires constant operator intervention to clear jams.
Reading the Specification Sheet for Production Reality
The installed power figures across the range — from 85 kW on the MT65 up to 260 kW on the MT95 — reflect the mechanical energy available for shear and pressure inside the barrel. Higher installed power supports higher throughput and tougher formulations, but actual consumption depends on the material’s resistance to shear. The selectable feeding system, single or double screw, matters when the formulation includes fibrous or sticky components that bridge in a standard hopper. Screw material grade, listed as wear-resistant alloy, directly influences how many production hours pass before screw elements need replacement, especially when mineral premix accelerates abrasion. Dimensions scale from a compact 28-meter footprint for the MT65 to a 36-meter line for the MT95, affecting workshop layout planning and utility routing.
The Hidden Cost of Skipping the Trial Run
Buyers who approve a line based on the supplier’s standard test material often face weeks of parameter adjustment after installation. The screw speed, barrel temperature zones, and die gap that work on the factory floor with a reference starch may produce under-cooked or over-expanded kernels when the actual formulation arrives. Downtime during this commissioning extension means delayed market entry and wasted raw material [NEED_CITE: cost of unplanned commissioning delays in food processing installations]. A trial run on the buyer’s own broken-rice and micronutrient blend before shipment compresses this learning curve into the factory test phase rather than the live production phase.
Why Procurement Teams Specify Meiteng Lines
The complete line scope — from mixing through packing — under one supplier means throughput calculations are verified across every station rather than assembled from separate vendor quotes. Screw configuration and die design are specified to the buyer’s raw material and target kernel shape, not copied from a generic build. The in-house testing workshop allows trial runs on customer-provided formulations before the line ships. Twin-screw expertise spans pet food, aquatic feed, snacks, cereals, starch, and protein applications, so formulation challenges specific to fortified rice are addressed from experience rather than experimentation. Pre-sales engineering consultation covers line layout, utility planning, and phased installation scheduling.
Documentation & Verification
- Line layout and capacity calculation based on your grain blend and micronutrient load
- Screw and die configuration record matched to your target kernel shape and cooking behaviour
- Electrical schematic confirming voltage, frequency, and control panel language for your site
- Trial run report on your raw material blend verifying output and kernel integrity before dispatch
- CE declaration of conformity and ISO certificate for customs and regulatory clearance
- Wear parts list with replacement screw and die specifications for your first scheduled change-out
Installation, Commissioning & Support
- Foundation plan accounts for line length up to 36 meters and vibration isolation at the extruder station
- Dedicated power circuit sized to installed power up to 260 kW with voltage confirmed to local standard
- Equipment shipped in sectional modules for container loading and on-site reassembly
- Commissioning includes parameter mapping on buyer’s actual grain formulation and premix ratio
- Operator training covers screw speed adjustment, barrel temperature zoning, and mesh belt speed tuning
- Replacement screw elements and die plates stocked for rapid dispatch to the buyer’s production site
What to Include in Your Inquiry
Specify your primary grain base, the micronutrient premix composition, and the target kernel shape and size. Confirm your local voltage and frequency standard, the control panel language preference, and whether you need gas or electric heating for the drying oven. Provide your target daily output and available workshop dimensions so the line layout can be drafted to your facility.
Frequently Asked Questions
Q: How is output capacity verified on my specific grain and micronutrient formulation?
A: We run a trial production using your exact broken-rice blend and vitamin-mineral premix in the testing workshop. The trial run report documents verified throughput, kernel density, moisture content after drying, and micronutrient retention levels. Capacity figures in the quotation are then based on your material, not a generic reference starch.
Q: What screw configuration and die are recommended for my target kernel shape and cooking behaviour?
A: The screw element sequence and die geometry are selected based on your formulation’s starch content, fiber level, and premix particle size. The configuration record documents the chosen setup so you can replicate it during production and reorder identical wear parts when replacement is due.
Q: How are voltage, frequency, and control-panel language confirmed before production?
A: During the specification confirmation stage, we collect your local electrical standard and preferred operator interface language. The electrical schematic is reviewed and signed off before the control cabinet is wired, preventing rewiring delays and language mismatches during on-site commissioning.
Q: Is a trial run on my raw material performed before shipment, and can I witness it?
A: Yes. The trial run takes place in the in-house testing workshop using your supplied raw material. Buyers are welcome to attend in person or receive a full video record along with the written trial report covering output rate, kernel appearance, and cooking test results.
Q: What is the lead time from order confirmation to factory test, and how is the installation schedule phased?
A: Typical multi-week lead times apply from specification sign-off through production and factory testing. Installation is phased into equipment positioning, utility connection, dry commissioning, and wet commissioning with your raw material. A detailed schedule is provided at the quotation stage so your site preparation aligns with the delivery timeline.