Throughput-Matched Stations — Every mixer, extruder, dryer and grinder is sized against the others before the line is finalized, preventing bottlenecks that arise when stations are sourced separately.
Technical Specifications
| Parameter | Value |
|---|---|
| Product Type | Fortified Nutrition Powder Production Line |
| Line Flow | Raw material → Mixing → Screw conveying → Extruding → Air Conveying → Drying → Air conveyor → Pulse Grinder |
| Extruder Type | Twin-screw extruder |
| Contact Material | Food-grade 304 stainless steel (mixer, product contact surfaces) |
| Control System | PLC and MCC, configurable |
| Model MT65 | Installed Power 84 kW / Consumption 59 kW / Output 120–150 kg/h (basis not stated in source — confirm raw material formulation and moisture content) / Dimensions 20000 × 1500 × 2200 mm |
| Model MT70 | Installed Power 160 kW / Consumption 120 kW / Output 150–200 kg/h (basis to be confirmed) / Dimensions 21000 × 1500 × 2200 mm |
| Model MT75 | Installed Power 190 kW / Consumption 140 kW / Output 200–250 kg/h (basis to be confirmed) / Dimensions 23000 × 1500 × 3200 mm |
| Model MT85 | Installed Power 210 kW / Consumption 150 kW / Output 300–400 kg/h (basis to be confirmed) / Dimensions 25000 × 1500 × 3500 mm |
| Mixer | Power 4 kW / 7.5 kW / 15 kW; Batch capacity 20–30 kg / 70–80 kg / 170–180 kg per batch; 304 stainless steel |
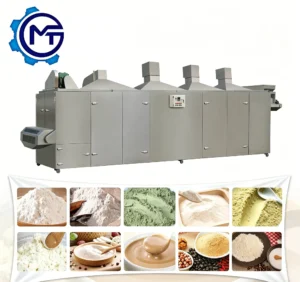
| Drying Oven | Fuel options: electricity, gas, or fuel; double pitch roller chain drive; adjustable temperature and time; configurable layers and length |
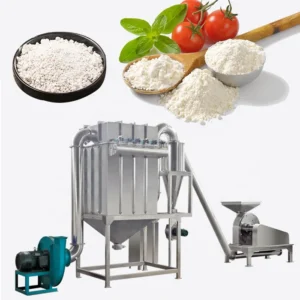
| Pulse Grinder | Power 11 kW; Weight 1500 kg; Dimensions 3000 × 900 × 2200 mm |
| Warranty | One year |
| Standards | CE, ISO |
Application Suitability
| Application | Material or Output |
|---|---|
| Infant nutrition and baby food powder | Rice flour, cereal blends with added vitamins and trace elements |
| Fortified nutritional powder | Grain bases enriched with proteins, minerals, and functional additives |
| Modified and pregelatinised starch | Corn starch, cassava starch, potato starch |
| Artificial and fortified rice granules | Broken rice, grain flour with nutrient fortification |
| Instant rice porridge powder | Pre-cooked cereal and legume formulations |
| Therapeutic and health care food powder | Specialized dietary blends requiring precise gelatinisation |
What Buyers Overlook When Quoting Nutrition Powder Lines by Extruder Model Alone
The extruder nameplate capacity means nothing until the dryer and grinder are verified to keep pace.
A common failure pattern in fortified baby food production is a line where the twin-screw extruder runs comfortably but the drying oven cannot remove moisture fast enough, forcing the operator to throttle the feed rate and run below the rated output. I have seen nutrition powder processing line full equipment range quotations where the grinder capacity was listed at roughly half the extruder output, creating a backlog of semi-finished pellets waiting to be milled [NEED_CITE: twin-screw extrusion throughput matching principles]. When every station is specified together rather than assembled from separate vendors, the throughput calculation starts from the final powder output and works backward.
Extruder Configuration for Starch Gelatinisation
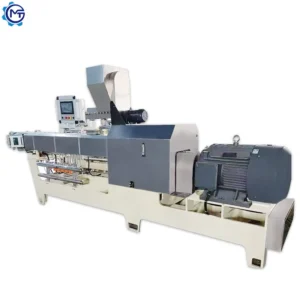
The twin-screw extruder in a fortified nutrition powder processing line performs the critical step of starch gelatinisation under controlled heat, moisture, and shear. Screw configuration and barrel temperature profile are matched to the raw material blend so that starches achieve full gelatinisation without degrading heat-sensitive nutrients. This determines how readily the final powder dissolves in water and how efficiently the body absorbs the fortified components.
Drying and Grinding as a Continuous Chain
After extrusion, the semi-finished pellets carry residual moisture that must be reduced uniformly before grinding. The drying oven uses a double pitch roller chain drive for consistent round-trip travel, and its configurable layer count and length are matched to the extruder output rate. The pulse grinder then reduces the dried pellets into a uniform powder. If any one of these three stages — extrusion, drying, grinding — is undersized, the entire nutrition powder processing line operates below its potential.
Reading the Power and Dimension Data
The installed power across the MT65 through MT85 extruder range spans 84 kW to 210 kW, with actual consumption running lower than installed figures due to intermittent load profiles. For facility planning, the overall line length extends from approximately 20 metres for the smallest configuration to 25 metres for the largest, and ceiling clearance must accommodate the tallest station at up to 3.5 metres [NEED_CITE: industrial food extrusion facility layout standards]. The mixer offers three power and batch capacity tiers, allowing buyers to match batch frequency to their extruder feed rate rather than over-sizing the blender.
The Cost of a Generic Screw and Die Build
When screw configuration and die design are copied from a generic template rather than specified to the buyer’s actual raw material, the extruder may produce pellets with inconsistent density or incomplete gelatinisation. This forces the dryer to work harder on some batches and leaves the grinder struggling with uneven particle hardness. In infant nutrition powder production, such variation translates to batches that fail dissolution or nutrient uniformity specifications. Correcting this after installation typically means ordering new screw elements and repeating commissioning trials [NEED_CITE: twin-screw element configuration for food extrusion].
Why Sourcing the Full Range from One Supplier Matters
Every station on this fortified baby food production line — mixer, screw conveyor, twin-screw extruder, air conveyor, dryer, pulse grinder — is specified against the others so throughput is balanced from raw material input to finished powder. Screw configuration and die design are selected based on the buyer’s raw material formulation and target product characteristics, not pulled from a generic build library. The in-house testing workshop runs trial batches on the customer’s actual raw material before shipment, producing a trial run report that confirms real output and product quality. All contact surfaces are food-grade 304 stainless steel, meeting the hygiene requirements for infant food production. Electrical schematics, voltage confirmation, and control language are verified before production begins.
Documentation & Verification
- Line layout drawing with throughput calculation for each station from mixer to grinder
- Screw and die configuration record matched to your raw material formulation
- Electrical schematic with voltage and frequency confirmed for your facility
- Factory trial run report produced on your actual raw material before dispatch
- CE declaration of conformity and ISO certificate for the complete line
- Wear parts list covering screws, dies, and grinder screens with replacement intervals
Installation, Commissioning & Support
- Foundation and utility planning based on the confirmed line dimensions and power requirements up to 210 kW
- Dedicated electrical circuit specification matching your local voltage and three-phase supply
- Equipment arrives in modular sections for staged assembly within the 20 to 25 metre line footprint
- On-site commissioning includes parameter setting for barrel temperature, screw speed, and dryer cycle
- Operator training covers PLC and MCC interface, batch recipes, and safety interlocks
- Spare screw elements, dies, and grinder screens supplied with recommended first replacement schedule
Before You Request a Quotation
To configure a line that actually meets your production target, we need your raw material formulation including moisture content, your target daily output of finished powder, and the ceiling height of your production area. Confirm your local voltage, frequency, and preferred control panel language. If you have existing upstream or downstream equipment that must interface with the new line, share those specifications as well.
Frequently Asked Questions
Q: On what basis are the extruder output figures for each model calculated?
A: The listed capacities are based on standard grain-based formulations at typical moisture levels, but actual output varies with raw material density, fat content, and target gelatinisation degree. We confirm real throughput by running a trial on your specific formulation in our testing workshop before finalizing the line configuration.
Q: How do you ensure the dryer and grinder do not bottleneck the extruder?
A: Each station is sized using a throughput calculation that starts from the desired final powder output. The dryer layer count, belt length, and residence time are matched to extruder output, and the pulse grinder is verified to handle the dried pellet volume without queuing.
Q: Can voltage, frequency, and control language be customized for my market?
A: Yes. The standard mixer runs on 380V 50Hz three-phase, but the full line electrical system is configurable. Voltage, frequency, control panel language, and PLC interface are confirmed during the specification stage before production begins.
Q: Is it possible to trial my raw material before the line ships?
A: Our in-house testing workshop conducts trial runs on your actual raw material formulation. The trial produces a report covering real output rate, product texture, and gelatinisation quality, which informs the final screw and die configuration.
Q: What spare wear parts should I plan for, and when is the first replacement due?
A: A wear parts list is supplied with every line, covering twin-screw elements, die plates, and grinder screens. The first replacement interval depends on the abrasiveness of your raw material and is confirmed during commissioning based on actual operating conditions.