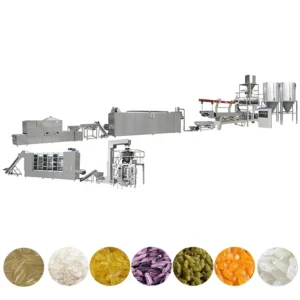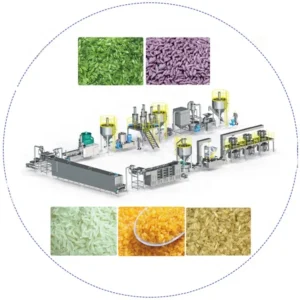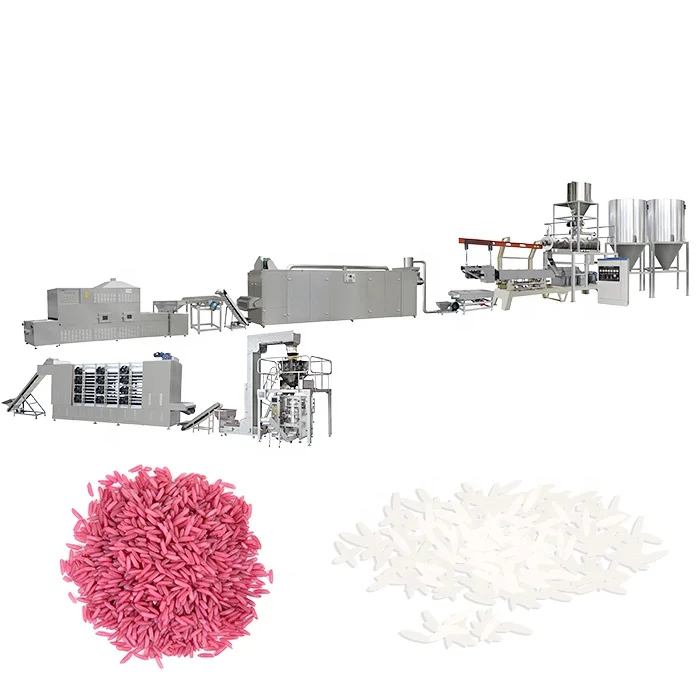
Complete Line Matching — Every station from batching through packing is sized to the extruder output so no single node chokes the throughput on your fortified rice kernel line.
Technical Specifications
| Parameter | Value |
|---|---|
| Product Type | Fortified Rice Kernel Extrusion Line |
| Models Available | MT65, MT70, MT85, MT75, MT95 |
| Screw Type | Twin-screw |
| Installed Power (MT65) | 85 kW |
| Installed Power (MT70) | 120 kW |
| Installed Power (MT85) | 235 kW |
| Installed Power (MT75) | 180 kW |
| Installed Power (MT95) | 260 kW |
| Power Consumption (MT65) | 60 kW |
| Power Consumption (MT70) | 85 kW |
| Power Consumption (MT85) | 165 kW |
| Power Consumption (MT75) | 135 kW |
| Power Consumption (MT95) | 195 kW |
| Output Capacity (MT65) | 80–100 kg/h (basis not stated in source — confirm raw material and moisture content) |
| Output Capacity (MT70) | 100–120 kg/h (basis not stated in source — confirm raw material and moisture content) |
| Output Capacity (MT85) | 200–300 kg/h (basis not stated in source — confirm raw material and moisture content) |
| Output Capacity (MT75) | 300–500 kg/h (basis not stated in source — confirm raw material and moisture content) |
| Output Capacity (MT95) | 800–1000 kg/h (basis not stated in source — confirm raw material and moisture content) |
| Overall Dimensions (MT65) | 28 × 1.2 × 2.2 m |
| Overall Dimensions (MT70) | 30 × 1.5 × 2.2 m |
| Overall Dimensions (MT85) | 34 × 3.5 × 4.3 m |
| Overall Dimensions (MT75) | 32 × 3.5 × 4.3 m |
| Overall Dimensions (MT95) | 36 × 3.5 × 4.3 m |
| Speed Control | Frequency inverter (variable speed) |
| Control System | Automated with PLC |
| Lubrication | Automatic lubricating system |
| Cooling | Integrated cooling system for extruder |
| Feeding System | Single or double screw feeding, selected per material uniformity requirement |
| Screw Material | Special wear-resistant alloy |
| Line Stations | Mixing → Extruding → Vibrating → Low-temperature drying → Cooling → High-temperature roasting → Cooling → Packing |
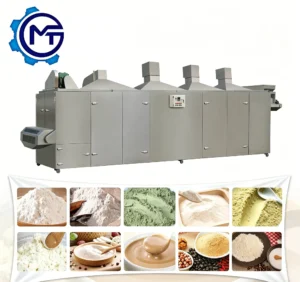
| Dryer Heating Source | Electric or gas |
| Dryer Control | Frequency motor for mesh belt speed adjustment |
| Dryer Feature | Circulation drying process, adjustable moisture differential |
| Voltage & Frequency | Customized to buyer’s local supply |
| Assembly State | Turnkey complete line |
| Standards | CE, ISO |
Application Suitability
| Application | Material or Output |
|---|---|
| Fortified rice kernel production | Broken rice, rice bran, corn, millet, wheat, oats, buckwheat, beans, starch |
| Nutritional rice enrichment | Rice base with added vitamins and minerals |
| Artificial rice for food nutrition programs | Multi-grain blends formulated for institutional feeding |
| Instant rice processing | Pre-gelatinised rice kernels for rapid rehydration |
Why the Raw Material Report Must Come Before the Line Quote
A capacity number means nothing until it is anchored to your specific grain blend and moisture level.
I once spent two full days re-configuring a screw combination because a client’s chickpea-heavy artificial rice formula behaved nothing like the standard rice flour we used during the trial. The gelatinisation temperature shifted, the extruded kernels came out hard and cracked, and the whole line rhythm fell apart. That mismatch would have been caught earlier if we had reviewed the material report before locking the specification. When buyers evaluate artificial rice machine equipment range options, the first question should always be what exactly goes into the hopper [NEED_CITE: starch gelatinisation behaviour across legume and cereal blends].
How Each Station Connects to the Next
The fortified rice processing line equipment sequence runs from mixing through extruding, vibrating, low-temperature drying, cooling, high-temperature roasting, a second cooling stage, and finally packing. Each station is selected so its throughput window overlaps the extruder’s actual output on your material. If the dryer belt runs slower than the extruder pushes product, kernels pile up and moisture becomes uneven. If the roasting oven is oversized, you waste energy cycling empty volume. This catalogue lays out the full artificial rice machine equipment range so you can see where each machine sits and how the capacities relate.
Matching the Extruder Model to Your Production Target
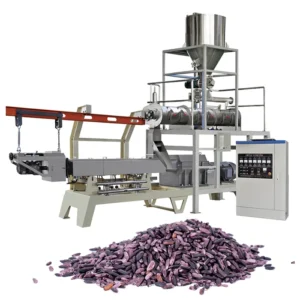
Five twin-screw models span the range from small-batch specialty runs to high-volume nutrition program supply. The MT65 starts at the lower end, suited for pilot production or regional distribution, while the MT95 handles continuous large-scale output. Frequency inverter speed control on every model lets operators fine-tune screw RPM to the dough viscosity that a particular grain blend demands. The automatic lubricating system and integrated barrel cooling keep the extruder stable across long shifts, reducing the thermal drift that causes density variation in the finished kernel [NEED_CITE: thermal management in continuous twin-screw food extrusion].
Reading the Specs That Actually Matter on a Rice Line
The twin-screw design is central to fortified rice production because it provides the shear and residence time needed to fully gelatinise starch from broken rice, corn, or multi-grain blends. Single or double screw feeding is offered depending on how uniformly your premix flows — a sticky bean-fortified formula may need the positive displacement of a double screw feeder, while free-flowing rice flour works well with a single screw. The dryer’s circulation process with adjustable moisture differential lets you set a gentle low-temperature pass first to stabilise kernel shape, followed by the high-temperature roasting stage that develops the final colour and bite. Voltage and frequency are configured to your local supply before production begins, so the PLC, motors, and heating elements all arrive matched to the site electrical infrastructure.
The Hidden Cost of Mismatched Station Capacity
I have walked into plants where the extruder was running at half speed because the downstream dryer could not keep up. The buyer had sourced the extruder from one vendor and the dryer from another, and nobody had calculated the belt loading rate against the extruder’s actual output on fortified rice dough. The result was a line that technically worked but never reached the throughput the buyer had budgeted for. Similar bottlenecks appear when the cooling conveyor is too short to bring kernel temperature down before packing, causing condensation inside the bags and shortened shelf life [NEED_CITE: moisture migration in packaged extruded rice kernels].
What Sets This Equipment Range Apart
Every station is specified under one supplier, which means the throughput calculation runs across the entire line rather than stopping at each machine boundary. Screw configuration and die design are matched to your raw material report, not copied from a generic build. The in-house testing workshop runs trial production on your actual grain blend before the line ships, catching gelatinisation and density issues at the factory rather than on your floor. Electrical schematics arrive with voltage and frequency already confirmed for your market, so commissioning starts with power-on rather with rewiring. The PLC control language is set before dispatch, matching the operators who will run the line daily.
Documentation & Verification
- Machine specification sheet listing screw and die configuration for your grain blend
- Line layout drawing with throughput calculated at every station
- Electrical schematic confirming voltage, frequency, and control language for your site
- Trial run report produced on your raw material in the testing workshop before shipment
- CE declaration of conformity and ISO certificate included with shipping documents
- Wear parts list with part numbers for screws, dies, and dryer belt sections
Installation, Commissioning & Support
- Foundation plan provided based on the selected model’s overall dimensions and weight distribution
- Dedicated electrical circuit sized to the extruder’s installed power rating up to 260 kW
- Line arrives in modular sections for staged assembly inside existing facility clearances
- First-run parameter setting covers screw speed, barrel temperature zones, and dryer belt velocity
- Operator training addresses PLC navigation, feeding rate adjustment, and moisture monitoring
- Spare screw elements and die plates shipped with the line for the first replacement cycle
What to Prepare Before Requesting a Quote
To specify the right artificial rice machine equipment range for your project, share your grain formulation with moisture percentages, the target kernel size and density, and the daily output you need to hit. Include your facility’s available floor length and ceiling height so the line layout can be drafted to fit. Confirm the local voltage and frequency, and let us know the control language your operators prefer. If you have existing upstream mixers or downstream packing machines, send their capacity data so the new stations can be matched to them.
Frequently Asked Questions
Q: Which extruder model fits my target output capacity?
A: The five models cover different production scales. Selection depends on your raw material and desired kernel output per hour. We confirm the match by running your actual grain blend in the testing workshop and measuring throughput before finalising the quotation. Share your formulation and target volume so we can recommend the correct model.
Q: How is each station sized to avoid throughput bottlenecks?
A: Every station — mixer, extruder, dryer, roaster, cooler, and packer — is calculated against the extruder’s real output on your material. Belt speeds, drying residence time, and cooling conveyor length are all set so product flows continuously without pile-up or idle gaps at any point.
Q: Can the dryer be configured for electric or gas heating?
A: Yes. The circulation drying oven supports both electric and gas heating sources. The choice depends on your local utility availability and energy cost structure. We confirm the heating configuration during the specification stage so the correct burner or element package is installed before shipment.
Q: What is the difference between single-screw and twin-screw feeding options?
A: Single-screw feeding suits free-flowing materials like plain rice flour. Twin-screw feeding provides positive displacement for sticky or uneven blends that contain bean flour, bran, or added vitamin premix. The selection is based on your raw material flow characteristics, which we evaluate before finalising the line.
Q: How do I confirm voltage, frequency, and control language before production?
A: During the specification confirmation step, we collect your site electrical data and operator language preference. The electrical schematic, motor ratings, heating elements, and PLC interface are all configured accordingly. This confirmation is completed and signed off before the line enters production.