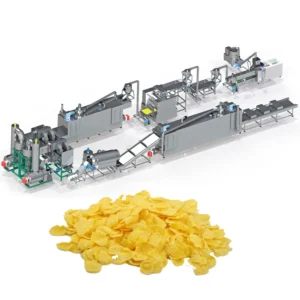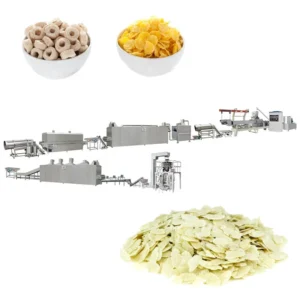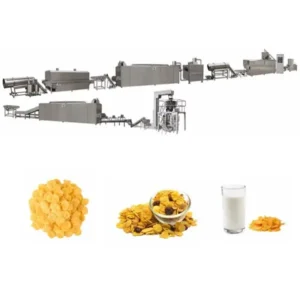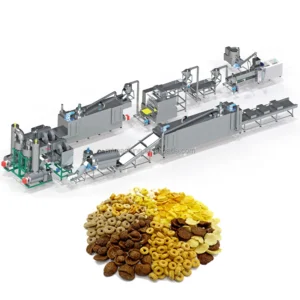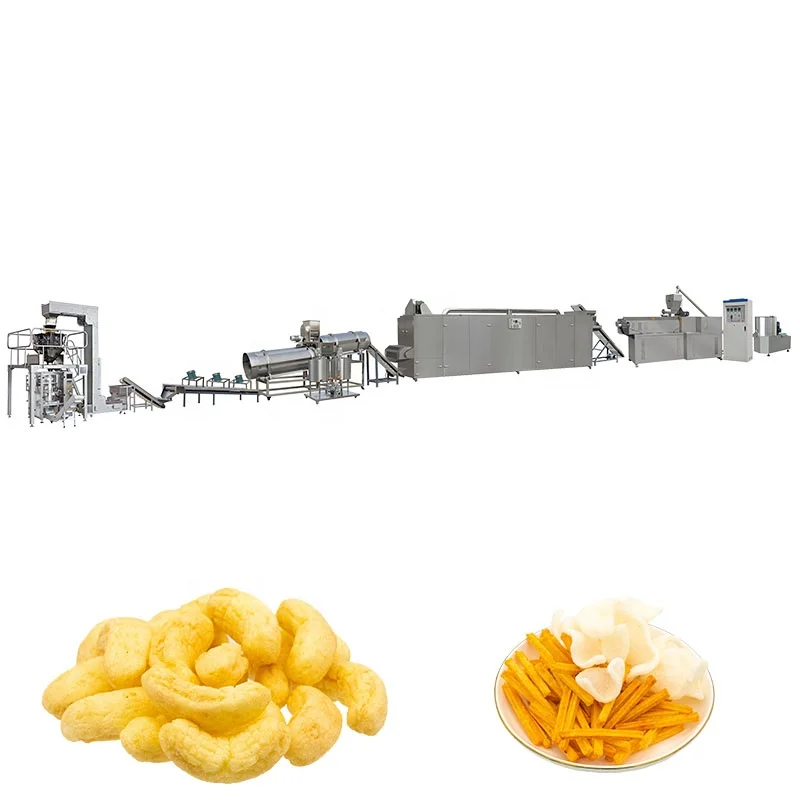
Matched Throughput Across Every Station — the extruder, flaking rolls, dryer and coating drum are engineered as one system so no single unit holds back the line’s actual output.
Technical Specifications
| Parameter | Value |
|---|---|
| Product Type | Corn Flakes Making Machine and Production Line |
| Model Options | MT70 / MT85 / MT75 |
| Installed Power | MT70 160 kW; MT85 190 kW; MT75 210 kW |
| Power Consumption | MT70 120 kW; MT85 140 kW; MT75 150 kW |
| Capacity | MT70 150–200 kg/hr; MT85 300–400 kg/hr; MT75 300–500 kg/hr (basis to be confirmed against raw material and moisture) |
| Extruder Type | Twin-screw |
| MT-75 Extruder Capacity | 200–300 kg/hr (basis to be confirmed) |
| Overall Dimensions (L×W×H) | MT70 41×1.5×2.2 m; MT85 43×1.5×3.2 m; MT75 45×1.5×3.5 m |
| Control System | PLC automated line control |
| Dryer Heating Source | Gas or electric |
| Flaking Machinery | Hydraulic double-roller, dual independent motors, infrared-sensor temperature control |
| Roasting Oven | Vibrating pan, high-temperature spraying tubes, dual circulating fans, cyclone dust removal |
| Coating System | Double tumble sugar melter, elevator, coating drum, spraying nozzle |
| Basic Raw Materials | Corn, rice, wheat, oat, barley powder |
| Assembly State | Complete production line |
| Certification | CE, ISO |
Application Suitability
| Application | Material or Output |
|---|---|
| Natural corn flakes production | Corn grits and corn flour blends |
| Sugar-coated breakfast cereal | Corn, rice, wheat, or oat base with sugar or honey coating |
| Shaped cereal formats | Rings, balls, tubes, stars, wheels, fruit loops from mixed grain powders |
| Fortified breakfast cereal | Grain powder blended with vitamin and mineral premix |
| Multi-grain flaked cereal | Barley, oat, and wheat combinations |
What "300 kg/hr" Really Means for Your Corn Flakes Line
Capacity is only real when measured against your exact raw material and recipe.
A corn flakes making machine full equipment range quoted at a nominal throughput can behave very differently once your local grain supply enters the hopper. I have stood on factory floors in the Middle East watching a line rated for high output deliver barely sixty percent usable product because the regional corn flour had a coarser grind than the test standard. The extruder could not achieve sufficient gelatinisation, and the flakes crumbled at the press rolls [NEED_CITE: starch gelatinisation thresholds in twin-screw extrusion].
This is why every capacity figure in the table above carries a confirmation note. The actual throughput depends on moisture content, particle size, and starch composition of the specific grain you run.
Matching Stations from the Mixer to the Packing Belt
When you survey a corn flakes making machine full equipment range, each station must handle the volume the previous one delivers. An extruder pushing 400 kg/hr into a dryer rated for 250 kg/hr means wet product piles up, sticks to conveyor belts, and degrades before it reaches the roasting oven. The line layout provided with every MT70, MT85, and MT75 configuration calculates residence time and belt load at each transfer point to prevent that mismatch.
Flaking Precision and the Role of Hydraulic Pressure
The flaking station uses a hydraulic double-roller system with independent motors driving each roll. This arrangement lets the operator set roll gap and pressure separately, which matters when switching between a thin breakfast flake and a thicker snack format. Infrared sensors monitor roll surface temperature in real time, keeping the gap thermally stable through long production runs [NEED_CITE: hydraulic roll gap control in cereal flaking machinery].
Reading the Spec Sheet Against Your Production Target
Installed power tells you the electrical infrastructure you need — the MT75 draws up to 210 kW, so a dedicated transformer circuit is typical. The twin-screw extruder relies on automatic lubrication and cooling to sustain continuous shifts without barrel scoring. Screw elements are manufactured with wear-resistant treatment to extend service intervals when running abrasive grain blends. The PLC control system coordinates extruder speed, dryer temperature, and roasting oven fan speed from a single interface, which reduces operator error during recipe changeovers.
The Hidden Cost of Skipping a Raw Material Trial
Lines shipped without a factory trial on the buyer’s actual grain often need weeks of on-site adjustment. I once spent ten days in a Dubai plant reconfiguring screw elements and moisture parameters because the local corn grits did not match the standard test sample. Flakes broke apart at the roasting stage, and the sugar coating clumped unevenly. Running your raw material through the testing workshop before shipment compresses that commissioning window dramatically [NEED_CITE: pre-shipment trial testing for food extrusion lines].
Why Procure the Full Range from One Equipment Source
Every station — mixing, extruding, flaking, drying, roasting, and coating — comes from a single manufacturer, eliminating the integration gaps that appear when you assemble from separate vendors. Screw configuration and die design are specified to your raw material rather than copied from a generic template. The in-house testing workshop allows trial runs on your grain before the line ships. Voltage, frequency, and control language are confirmed to your local grid standard before production begins. Ongoing support covers operator training, wear parts supply, and maintenance scheduling from the same engineering team that built the line.
Documentation & Verification
- Line layout showing throughput calculations between extruder, dryer, flaking rolls, and roasting oven
- Screw and die configuration record matched to your grain type and target flake thickness
- Electrical schematic confirming voltage, frequency, and PLC language for your facility
- Trial run report on your raw material conducted in the testing workshop before dispatch
- CE declaration of conformity and ISO certificate for customs and regulatory clearance
- Wear parts list with part numbers for screws, dies, and roller surfaces
Installation, Commissioning & Support
- Floor plan and foundation load data based on the selected model’s overall dimensions and weight
- Dedicated power circuit sizing for the MT75’s 210 kW installed load or equivalent model requirement
- Modular station delivery with on-site assembly alignment of extruder, flaking, and roasting units
- First-run parameter logging covering barrel temperature, roll gap, and dryer residence time
- Operator training on PLC interface covering recipe storage, alarm response, and daily shutdown sequence
- Initial spare set of screw elements, die plates, and flaking roll surfaces included with shipment
- Scheduled maintenance intervals for automatic lubrication system and infrared sensor calibration
What to Include in Your Inquiry
To size the line correctly, share your primary grain type and its typical particle size or mesh specification, along with the moisture range you expect at the extruder inlet. Provide your target daily output in kilograms and the number of operating shifts, so throughput can be calculated against realistic uptime. Confirm your facility voltage and frequency, the control language your operators need, and whether you would like to send a raw material sample for a pre-shipment trial run.
Frequently Asked Questions
Q: How is line capacity verified against my specific raw material and recipe?
A: We request a sample of your grain or flour blend and run it through the extruder and flaking station in our testing workshop. The trial produces actual throughput data, flake integrity measurements, and moisture readings. A full report accompanies the quotation so you see verified numbers rather than generic estimates.
Q: What voltage, frequency, and control language options are confirmed before shipment?
A: Before production starts, we confirm your local voltage and frequency — whether 380 V / 50 Hz, 440 V / 60 Hz, or another standard — and program the PLC interface in your preferred language. The electrical schematic reflects these settings so your electrician can prepare the facility without guesswork.
Q: How is throughput matched between the extruder, dryer, flaking unit, and coating drum?
A: Each station is selected based on the extruder’s verified output on your raw material. The dryer belt length, flaking roll width, and coating drum volume are all calculated so that product flow remains continuous. The line layout document shows the capacity match at every transfer point.
Q: Can I run a trial on my own raw material before the line ships?
A: Yes. Sending a representative sample of your grain to our testing workshop allows us to configure screw elements, adjust moisture targets, and record actual product quality before the equipment leaves the factory. The trial results are shared in a written report and discussed before final acceptance.
Q: What spare wear parts are included and how are replacements supplied?
A: The initial shipment includes a set of replacement screw elements, die plates, and flaking roll surfaces. A detailed wear parts list with part numbers is provided so you can reorder directly. Replacement components are manufactured to the same specifications as the originals.