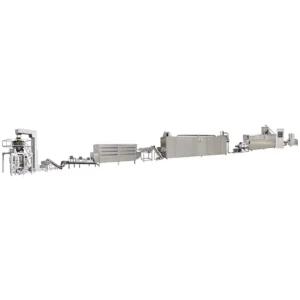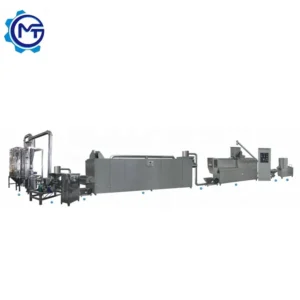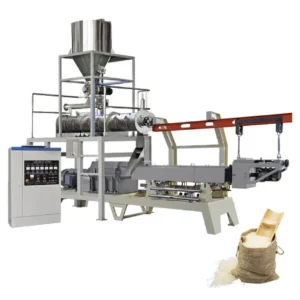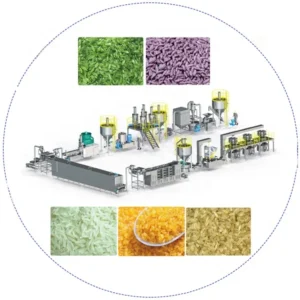
Complete Line from Batching to Packing Under One Supplier — Throughput matching across mixing, extrusion, drying and packing stations prevents the bottleneck failures that occur when a nutrition powder line is assembled from separate vendors.
Technical Specifications
| Parameter | Value |
|---|---|
| Product Type | Nutrition Powder Processing Line |
| Output Capacity | 200-500 kg/h (basis not stated in source — confirm raw material / moisture / formulation) |
| Construction Material | Food-Grade 304 Stainless Steel |
| Control System | Touch Control Panel with Digital System (PLC controlled) |
| Heat Source Options | Electric / Gas / Steam |
| Key Line Stations | Baking Oven, Mixer |
| Warranty | 1 Year |
| After-Sales Service | Overseas Engineer Service Available |
| Assembly State | Complete Production Line |
| Standards | Confirm CE / ISO status from manufacturer |
Application Suitability
| Application | Material or Output |
|---|---|
| Baby food and infant nutrition powder production | Rice, corn, and grain blends with added micronutrients |
| Fortified rice cereal manufacturing | Milled rice flour and iron-fortified grain mixes |
| Porridge and instant cereal mix processing | Multi-grain formulations including beans and corn |
| Nutritional and infant formula powders | Pre-cooked starch bases with vitamin and mineral premixes |
What a Capacity Rating Hides Before Your Raw Material Arrives
A 500 kg/h label means nothing if your actual rice flour has lower starch content than the test material.
I once spent half a month on-site in West Africa reconfiguring screw combinations and temperature curves because the local rice flour the customer sourced had a noticeably different starch profile from our factory trial material. The gelatinisation degree never reached specification until we adjusted every heating zone to match their actual grain. Buyers surveying a Nutrition Powder Processing Line Full Equipment Range need to see how each station — mixer, extruder, dryer — is sized to the specific raw material they will actually feed into the hopper, not to a generic lab sample. [NEED_CITE: starch gelatinisation behaviour varies across rice cultivars and milling grades]
Matching Every Station to Prevent Mid-Line Choke Points
When one vendor supplies the extruder and another supplies the dryer, the throughput rarely aligns. A dryer that is too small creates a pile-up of semi-finished product cooling unevenly on trays; a dryer that is oversized wastes floor space and energy. The Nutrition Powder Processing Line Full Equipment Range catalogues each station with its rated throughput so buyers can verify that the mixer output, extruder capacity, baking oven residence time, and downstream packing speed all operate at the same cadence without manual buffering.
Material Contact Integrity Across the Full Equipment Chain
Fortified infant cereal is held to tight contamination standards. Every contact surface on this line — from the mixing bowl interior through the extruder barrel to the baking oven trays — uses food-grade 304 stainless steel. This matters particularly at station transitions: where product drops from the mixer discharge into the extruder feed hopper, and again where baked product exits the oven onto the cooling conveyor. Unsealed gaps or dissimilar metals at those handoff points are where iron contamination and cleaning failures most often originate. [NEED_CITE: food contact material regulations for infant food processing equipment]
How the Specification Sheet Translates to Daily Production
The touch control panel with digital PLC system governs barrel temperature profiles, screw speed, and oven zone temperatures from a single interface. For a factory operator running different grain formulations on consecutive shifts — rice cereal in the morning, a corn-bean porridge mix in the afternoon — the ability to save and recall recipe parameters directly affects batch-to-batch consistency in gelatinisation degree and powder fineness. The heat source options — electric, gas, or steam — determine not only operating cost but also the oven footprint and the utility infrastructure the buyer must prepare before installation. A gas-fired baking oven, for instance, requires local combustion venting that an electric oven does not. Choosing the wrong heat source after the foundation is poured leads to expensive retrofit work or compromised drying uniformity across the tray width.
The Hidden Cost of Specifying Stations in Isolation
Purchasing an extruder rated at the target output and then pairing it with a separately sourced dryer often results in moisture content that drifts outside specification. The powder may leave the extruder correctly gelatinised but arrive at the packing station too moist for shelf stability, or over-dried to the point of flavour degradation. Buyers who have experienced this mismatch report spending weeks on-site recalibrating temperatures and conveyor speeds across equipment that was never designed to communicate with each other. [NEED_CITE: post-extrusion moisture control requirements for shelf-stable nutrition powders]
Why Procurement Through a Single Equipment Range Matters
Sourcing from the Nutrition Powder Processing Line Full Equipment Range means throughput calculations are performed across every station before the line is built, not after it is installed. Screw configuration and die design are specified to the buyer’s actual raw material and target powder texture. The in-house testing workshop runs the customer’s own grain flour before shipment, so temperature curves and screw combinations are confirmed in advance rather than debugged on the factory floor. Line layout and capacity documentation are provided as one integrated package rather than a pile of mismatched datasheets from different vendors.
Documentation & Verification
- Line layout and capacity calculation showing throughput at every station from mixer to packing
- Machine specification sheet with confirmed voltage, frequency, and control language
- Screw and die configuration record matched to your grain formulation
- Factory test record and trial run report on your actual raw material before dispatch
- Wear parts list identifying screws, dies, and seals with replacement intervals
- Packing photographs for shipment verification and customs documentation
Installation, Commissioning & Support
- Foundation and floor space plan based on the baking oven dimensions and heat source selection
- Electrical specification confirming PLC panel voltage and dedicated circuit requirements for your site
- Overseas engineer service for on-site assembly, station alignment, and first-run parameter setting
- Operator training covering recipe storage on the touch control panel for different grain formulations
- Spare wear parts supply for screws, dies, and oven seals with lead time guidance
- Maintenance schedule for stainless steel contact surfaces and drive components
What to Include in Your Inquiry
Buyers evaluating a nutrition powder processing line should provide the exact grain types and flour mesh size they intend to process, along with the target daily output in their local operating shifts. Factory floor dimensions and ceiling height determine the baking oven configuration and conveyor routing. Confirm your site voltage, frequency, and the preferred heat source — electric, gas, or steam — so the utility plan matches the equipment selection before production begins.
Frequently Asked Questions
Q: What supporting stations are included and how is throughput matched across them?
A: The line covers mixing, extrusion, baking, cooling, and packing. Each station is sized during the layout phase so that the mixer batch cycle, extruder output, and oven residence time all align to the same hourly throughput, preventing mid-line accumulation or starvation that occurs when stations are sourced separately.
Q: Which heat source options are available and how do they affect line footprint?
A: Electric, gas, and steam options are available for the baking oven. Gas requires combustion venting infrastructure and may increase ceiling height requirements. Steam needs a boiler plant on site. Electric is the most compact but depends on sufficient installed capacity at the facility.
Q: How do I confirm voltage, frequency and control language before shipment?
A: The specification sheet records your site voltage, frequency, and preferred PLC display language. This confirmation happens before production begins so the electrical cabinet and touch panel firmware match your local standards and operator requirements.
Q: Can I run a trial on my own raw material before the line ships?
A: The in-house testing workshop accepts customer-supplied grain flour for trial runs. Screw configuration, barrel temperature profile, and baking oven settings are adjusted to achieve the target gelatinisation degree and powder texture, and a trial run report is issued before dispatch.
Q: What spare wear parts are included and how are replacements supplied?
A: A wear parts list identifies screws, dies, seals, and oven components with expected service intervals. Initial spares ship with the line, and replacement parts are supplied with confirmed lead times based on the configuration record for your specific line.