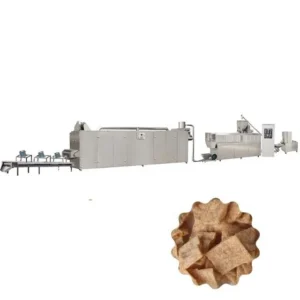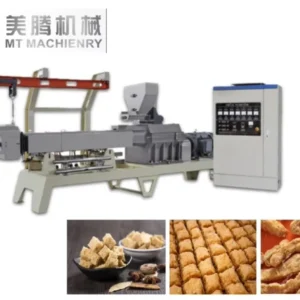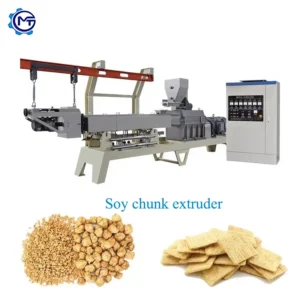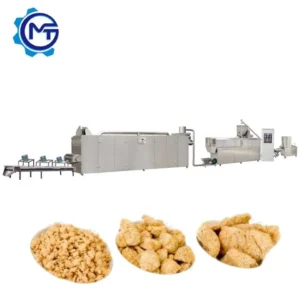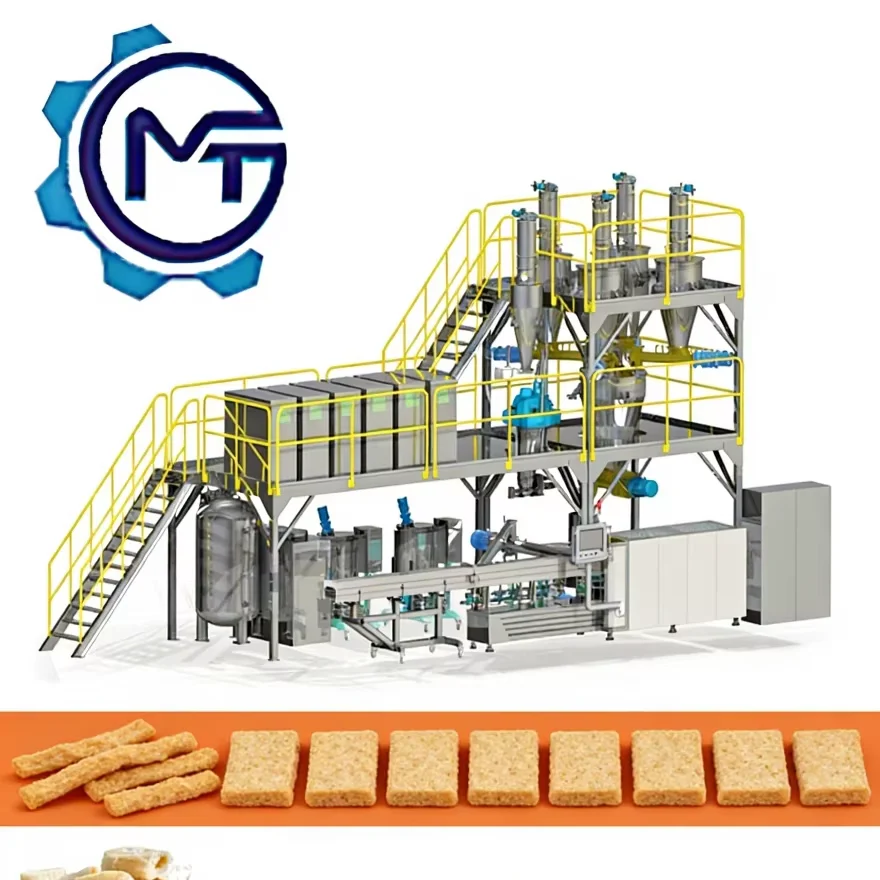
Throughput-Matched Stations — every mixer, extruder, and dryer in this catalogue is sized to the same hourly output so no single machine holds back the rest.
Technical Specifications
| Parameter | Value |
|---|---|
| Product Type | Twin Screw Extruder Line for Textured Soy Protein (Plant-Based Meat) |
| Models Available | MT65, MT70, MT75, MT85 |
| Screw Type | Twin Screw |
| Screw Length | 1050 mm (MT65); 1520 mm (MT70, MT75, MT85) |
| Installed Power | 84 kW (MT65); 160 kW (MT70); 190 kW (MT75); 210 kW (MT85) |
| Power Consumption | 59 kW (MT65); 120 kW (MT70); 140 kW (MT75, MT85) |
| Output Capacity | 100–150 kg/h (MT65); 150–200 kg/h (MT70, MT75); 250–300 kg/h (MT85) (basis not stated in source — confirm raw material type, moisture content, and target format) |
| Main Motor Power | 22 kW / 30 kW / 45 kW (model-dependent) |
| Rotary Cutting Motor | 0.75 kW |
| Feeding Motor | 0.75 kW |
| Pump Motor | 0.37 kW |
| Heating Power | 10 kW (MT65); 14 kW (MT70, MT75, MT85) |
| Overall Dimensions (L×W×H) | 40,000×1,200×2,200 mm (MT65); 41,000×1,500×2,200 mm (MT70); 43,000×1,500×3,200 mm (MT75); 45,000×1,500×3,500 mm (MT85) |
| Mixer Batch Capacity | 20–30 kg / 70–80 kg / 170–180 kg (model-dependent) |
| Mixer Power | 4 kW / 7.5 kW / 15 kW (model-dependent) |
| Mixer Contact Material | Stainless Steel 304 (mixing ruler) |
| Line Stations | Mixer → Screw Conveyor → Twin Screw Extruder → Air Conveyor → Multi-layer Dryer → Cooling Machine |
| Dryer Heating Options | Fuel, Gas, or Electricity (selectable) |
| Dryer Drive | Double-pitch roller chain, round-trip drying |
| Die Configuration | Interchangeable moulds for nuggets, chunks, TVP/TSP |
| Certification | CE |
Application Suitability
| Application | Material or Output |
|---|---|
| Textured vegetable protein (TVP) | Defatted soya flour or low-temperature soya flakes |
| Soya chunks and nuggets | High-protein soya meal with adjustable moisture |
| Plant-based meat analogues | Blended soya protein with starch and fibre binders |
| Cereal and snack variants | Corn grits, rice flour, or blended grain formulations with screw and die changeover |
Why the Downstream Dryer Often Bottlenecks the Whole Line
A twin screw extruder line for plant based meat manufacturer is only as productive as its slowest station — and that station is usually the dryer.
When a buyer sources the extruder from one vendor and the dryer from another, the two machines rarely agree on what "capacity" means. The extruder pushes out wet, freshly expanded protein pieces that must drop to a safe moisture level before cooling or packing. If the dryer cannot handle that volume, half-finished product piles on the conveyor, sticks together, and blocks the entire line downstream. I have watched this exact scenario freeze a freshly commissioned plant within the first shift [NEED_CITE: line balancing principles in continuous food extrusion].
Matching Every Station to the Same Hourly Rate
Each model in the MT65–MT85 range ships with a mixer, screw conveyor, twin screw extruder, air conveyor, multi-layer dryer, and cooling machine sized to the same throughput band. This approach keeps material moving continuously from batching to final cooling without manual buffer bins or re-work loops. Buyers surveying equipment for a full plant-based meat line can review every station on one specification sheet instead of reconciling separate vendor proposals.
Dryer Heating Flexibility Across Markets
The multi-layer dryer supports fuel, gas, and electric heating, selected before production based on local utility costs and availability. A double-pitch roller chain drives the belt in a round-trip path, giving the material multiple passes through the heated zone and extending residence time without increasing the machine footprint. In regions where industrial gas is reliable, many producers prefer gas firing for operating cost reasons; in locations with unstable gas supply, electric heating avoids unplanned stops [NEED_CITE: industrial dryer energy source selection in food processing].
Reading the Specification Sheet for Real-World Impact
Screw length varies from 1050 mm on the MT65 to 1520 mm on the larger models, directly influencing how long the raw material stays inside the barrel. A longer residence time allows more complete starch gelatinisation and protein texturisation, which is essential when processing high-fibre soya blends that need extra shear. The main motor steps from 22 kW up to 45 kW across the range, giving operators enough torque to maintain screw speed even when the recipe becomes denser. Interchangeable dies let the same extruder switch between nugget, chunk, and fine granule formats, so a single platform covers several product SKUs without a second capital outlay. Stainless Steel 304 contact parts in the mixer prevent iron contamination that could discolour light soya protein batches.
The Hidden Cost of Mismatched Upstream Feeding
When the mixer batch size is too small for the extruder’s consumption rate, the screw conveyor runs half-empty, causing inconsistent feed density at the extruder inlet. Fluctuating feed density produces uneven expansion, and some pieces exit the die under-texturised while others over-expand and fracture. Downstream, the cooling machine then receives a mixed batch that cannot be packed to a uniform specification. Selecting a mixer batch capacity that aligns with the extruder hourly rate — and confirming it on the line layout drawing — eliminates this feed-starvation problem before the first trial run [NEED_CITE: effects of feed consistency on twin-screw extrusion output quality].
Why Sourcing the Full Catalogue from One Supplier Matters
Every station listed here is documented with installed power, footprint, and capacity range, so throughput calculations can be verified on a single drawing rather than cross-referenced across multiple quotes. Screw configuration and die design are specified to the buyer’s raw material and target product format before the extruder enters production. The in-house testing workshop runs customer-supplied defatted soya flour or soya flakes through the exact model being ordered, producing a trial run report that confirms texture, density, and output before shipment. Electrical schematics are prepared with the buyer’s confirmed voltage and frequency, preventing commissioning delays on site. Documentation packages — from CE declarations to operation manuals — cover the entire line under one reference number, simplifying customs clearance and future audits.
Documentation & Verification
- Line layout drawing showing matched throughput for mixer, extruder, dryer, and cooler
- Screw and die configuration record matched to your soya flour or soya flake recipe
- Trial run report on your raw material confirming texture and density before dispatch
- Electrical schematic with voltage and frequency confirmed for your local grid
- Operation and maintenance manual covering every station in the line
- Wear parts list identifying screws, dies, and dryer chain components with replacement intervals
Installation, Commissioning & Support
- Foundation plan accounts for the 40 m to 45 m line length and dryer weight load
- Dedicated electrical circuit sized to the model’s installed power, up to 210 kW for the MT85
- Machines ship in modular sections for container loading and on-site reassembly
- First-run parameter setting covers barrel temperature zones, screw speed, and dryer residence time
- Operator training addresses die changeover and double-pitch chain tensioning on the dryer
- Spare screw elements and die plates stocked for first replacement cycle after commissioning
Preparing Your Enquiry for a Fast Line Proposal
Share the specific soya material you plan to run — whether defatted flour, low-temperature flakes, or a custom protein blend — along with the target product format such as chunks, nuggets, or granules. Confirm your local voltage, frequency, and preferred dryer heating source so the electrical schematic and utility layout match your facility from day one. If you have existing upstream mixers or downstream packing machines, provide their throughput data so the new line can integrate without bottlenecks. Requesting a trial run on your own raw material before shipment is always available and recommended.
Frequently Asked Questions
Q: How do I know each station is sized correctly for the extruder output I need?
A: The line layout and capacity calculation document provided with every quotation lists the hourly throughput of the mixer, extruder, dryer, and cooling machine side by side. Each station is selected so its rated capacity meets or slightly exceeds the extruder output, preventing bottlenecks. Buyers can review this document before placing the order and request adjustments if their raw material behaves differently from standard soya flour.
Q: What is the difference in footprint and utility requirement between MT65, MT70, MT75, and MT85?
A: Overall line length ranges from approximately 40 m on the MT65 to 45 m on the MT85, while width and height increase to accommodate larger barrel and dryer assemblies. Installed power climbs from 84 kW to 210 kW, meaning the electrical supply and transformer sizing must be planned accordingly. The layout drawing supplied with each quotation shows exact dimensions and utility connection points for the chosen model.
Q: Can the same extruder line produce both TVP chunks and puffed snacks by changing screws and dies?
A: Yes. The twin screw platform accepts different screw element arrangements and interchangeable die plates, allowing the same extruder to process soya protein into chunks or switch to cereal-based recipes for puffed snacks. Changeover requires a planned stop for screw and die replacement and re-setting of barrel temperature zones. Buyers should confirm both product targets during the quotation stage so the correct screw set is included.
Q: How is the dryer heating source selected — fuel, gas, or electric?
A: Selection depends on local utility pricing, supply reliability, and workshop ventilation. Gas heating suits facilities with a stable pipeline and lower energy tariffs, while electric heating is preferred where gas infrastructure is unavailable or where precise temperature zoning is required. Fuel-based heating is chosen in locations where diesel or heavy oil is the most economical option. The quotation specifies the chosen heating type and its impact on installed power.