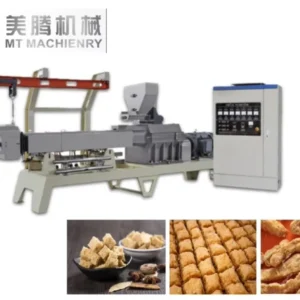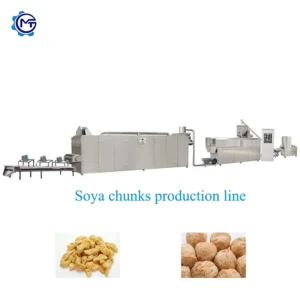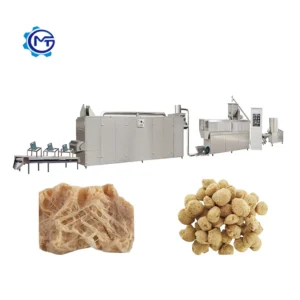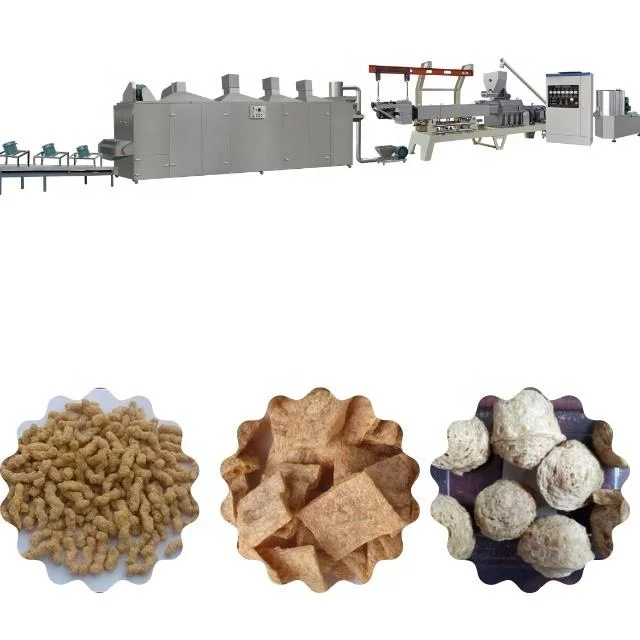
Station-Throughput Alignment — Every mixer, twin-screw extruder, roaster, and cooler is sized so no single unit chokes the line when running actual soybean or peanut meal formulations, verified by pre-shipment trial.
Technical Specifications
| Parameter | Value |
|---|---|
| Product Type | Texturized Vegetable Protein (TVP) Extrusion Line |
| Models Available | MT65, MT70, MT85 |
| Screw Type | Twin-screw (Double Screw Extruder) |
| Installed Power | 85 kW (MT65) / 120 kW (MT70) / 195 kW (MT85) |
| Real Power | 65 kW (MT65) / 90 kW (MT70) / 165 kW (MT85) |
| Output Capacity | 150–200 kg/h (MT65) / 200–300 kg/h (MT70) / 600–800 kg/h (MT85) (basis not stated in source — confirm raw material formulation and moisture content) |
| Overall Dimensions | 18000×1300×2300 mm (MT65) / 20000×1500×2400 mm (MT70) / 24000×3500×4300 mm (MT85) |
| Powder Mixer Tank Volume | 150 kg |
| Powder Mixer Rotary Speed | 385 rpm |
| Powder Mixer Output | 300–600 kg/h (basis not stated in source — confirm batch material and cycle time) |
| High-temperature Roaster Belt Effective Length | 3.5 m |
| High-temperature Roaster Output | 300–400 kg/h (basis not stated in source — confirm product type and moisture reduction target) |
| Cooling Machine Capacity | 200–300 kg/h (basis not stated in source — confirm product format and inlet temperature) |
| Line Stations | Raw material preparation → Mixing → Conveying → Extrusion → Conveying → Drying → Cooling → Packing |
| Control System | PLC and MCC control |
| Material | Stainless steel (all food-contact parts) |
| Voltage & Frequency | To be confirmed per buyer’s site |
| Standards | CE (since 2014), ISO certified |
Application Suitability
| Application | Material or Output |
|---|---|
| Plant-based meat patty and nugget base | Low-temperature soybean meal, defatted soy flour |
| Vegetarian ham and sausage filling | Texturized soy protein with binding agents |
| Canned vegetarian food ingredients | Peanut meal and soybean meal blends |
| Quick-frozen food protein portion | TVP chunks and granules from soy or peanut meal |
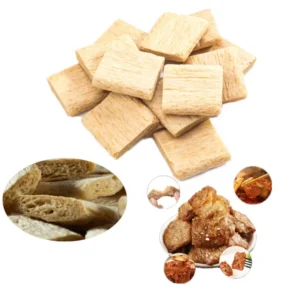
| Protein ingredient for food processors | High-protein meal texturized into fibrous structure |
Why "Nominal Capacity" Rarely Survives First Contact With Your Actual Meal
A line rated on standard soy flour can lose noticeable throughput when the buyer switches to a high-pea-protein or peanut-heavy formulation.
I watched this happen on a Middle East project where the extruder was dialed in for textbook soy isolate. The client’s real recipe leaned heavily on pea protein with different moisture uptake and shear response. Capacity dropped sharply, the downstream forming section ran empty waiting for material, and the whole line rhythm collapsed. The screw configuration had to be completely re-sorted before the plant could hold its target output. A texturized vegetable protein production line equipment for sale should never be quoted on a generic basis without accounting for the buyer’s exact meal blend and moisture profile [NEED_CITE: twin-screw extrusion response to alternative plant proteins].
How Shear and Temperature Rebuild Protein Architecture
Inside the twin-screw barrel, spherical protein molecules open into chain structures under combined high temperature, high pressure, and mechanical shear. The chains reorganize into a layered, fleshy fiber matrix as they pass through the die. Die geometry and screw element sequencing determine whether you get long chunky fibers suited for vegetarian steak strips or shorter granular textures for sausage filling. Getting this right means specifying screw elements and die inserts against the buyer’s actual formulation, not a default build.
Matching Every Station to Prevent Downstream Starvation
A common failure mode on protein texturization lines is an extruder that pushes more wet product than the roaster can dry or the cooler can handle. When the roaster belt cannot carry the volume, half-dried TVP piles up, surface moisture stays high, and microbial shelf life shortens. On the MT65, MT70, and MT85 lines, mixer batch output, extruder throughput, roaster belt length, and cooler capacity are aligned per model so material flows continuously without manual intervention or buffer bins. This station-to-station matching is what makes a texturized vegetable protein production line equipment for sale actually hold its quoted rhythm on a real production floor [NEED_CITE: line throughput balancing in food extrusion plants].
Reading the Specs That Actually Matter
The installed versus real power split — 85 kW versus 65 kW on the MT65, for example — reflects the difference between motor nameplate rating and expected running draw under typical protein load. This gap matters for sizing your transformer and dedicated circuit. The 150 kg mixer tank at 388 rpm is built for dry blending of soy and peanut meals with minor additives before hydration; it is not a high-shear disperser, so liquid fats or emulsifiers should be metered at the extruder feed. The 3.5 m effective roaster belt sets the residence time available for moisture reduction; running the belt faster to chase extruder output means higher residual moisture in the finished TVP. Stainless steel across all contact surfaces keeps the line compliant with food hygiene inspections and simplifies wash-down between formulation changes.
The Cost of Guessing the Screw Profile
When a generic screw configuration meets a formulation it was not designed for, the fiber structure comes out wrong — either under-texturized with a powdery crumb or over-sheared into a rubbery mass that downstream forming equipment cannot handle. Operators then slow the extruder to compensate, which idles the roaster and cooler and wastes energy on partially loaded drives. Re-sorting screw elements after installation means a full barrel teardown, lost production days, and shipping replacement segments internationally. This is the kind of downtime that erases any upfront savings from buying on spec alone [NEED_CITE: screw element replacement lead times in food extrusion].
What Backs This Line Beyond the Brochure
Screw configuration and die design are specified to the buyer’s raw material and target fiber structure rather than copied from a generic catalog build. An in-house testing workshop runs trial production on the buyer’s actual soybean or peanut meal before the line ships, so the trial run report reflects real output and texture rather than theoretical curves. The complete line from batching through packing comes from one supplier, meaning throughput is matched across every station instead of assembled from mismatched vendors. Pre-sales consultation covers line layout, utility planning, and capacity calculation, followed by on-site installation, commissioning, and operator training. Ongoing maintenance support includes wear parts supply so that screw segments and die inserts are available when the first replacement falls due.
Documentation & Verification
- Line layout and capacity calculation matched to your soybean or peanut meal formulation
- Screw and die configuration record specific to your target fiber structure
- Trial run report on your raw material produced in the testing workshop before dispatch
- Electrical schematic with voltage, frequency, and control language confirmed for your site
- CE declaration of conformity and ISO certificate included with shipping documents
- Operation and maintenance manual with wear parts list for TVP extrusion components
Installation, Commissioning & Support
- Foundation must support line length up to 24 m (MT85) with level tolerance for continuous conveying sections
- Dedicated power circuit sized for real running draw of up to 165 kW (MT85) at confirmed site voltage
- Stations ship pre-assembled; final alignment of extruder-to-roaster transfer verified during on-site commissioning
- PLC and MCC control parameters set against your specific meal formulation and target moisture during first run
- Operator training covers screw element inspection, die cleaning, and roaster belt tension adjustment
- Wear parts list with screw segments and die inserts identified for reorder planning
What We Need to Quote the Right Line
Share your base meal type — soybean, peanut, pea, or a blend — along with the protein content and target moisture at the extruder feed. Confirm the daily output target in kilograms and the shift pattern you plan to run. Provide your site voltage, frequency, and preferred control language so the electrical cabinet and PLC interface are configured before production. Let us know if you want a trial run on your raw material in the testing workshop before shipment.
Frequently Asked Questions
Q: How is output capacity verified against my specific soybean or peanut meal formulation?
A: We run your actual raw material in the in-house testing workshop before shipment. The trial produces a report covering throughput, fiber structure, moisture content at each station, and screw configuration used. This confirms the line holds its capacity on your meal blend rather than on a generic reference material.
Q: What screw and die configuration is recommended for my target fiber structure?
A: Screw elements and die geometry are selected based on your protein source, moisture level, and whether you need long chunky fibers or fine granules. The configuration record is documented and included with the line so future reorders of wear parts match the original setup.
Q: How is voltage, frequency, and control system language confirmed before production?
A: During the specification confirmation stage, we collect your site electrical data and operator language preference. The electrical schematic, motor ratings, PLC interface, and MCC labels are all built to those parameters before the line enters production.
Q: Can a trial run on my raw material be conducted before shipment?
A: Yes. The testing workshop runs your meal formulation through the extruder and downstream stations. The trial run report documents real throughput, product texture, and any screw or die adjustments made, so you receive a line already dialed to your recipe.
Q: What spare wear parts are included, and what is the replacement lead time?
A: A wear parts list identifies screw segments, die inserts, and other consumable components. Initial spares ship with the line, and replacement orders are fulfilled against the documented configuration to maintain consistent fiber structure and throughput.