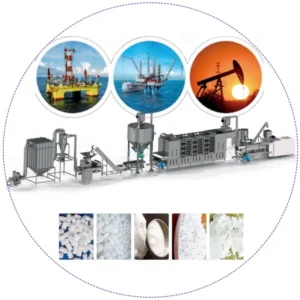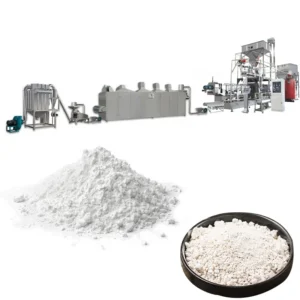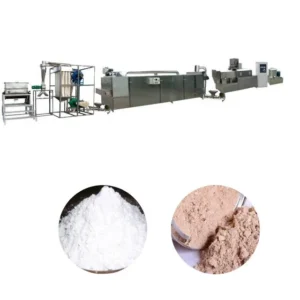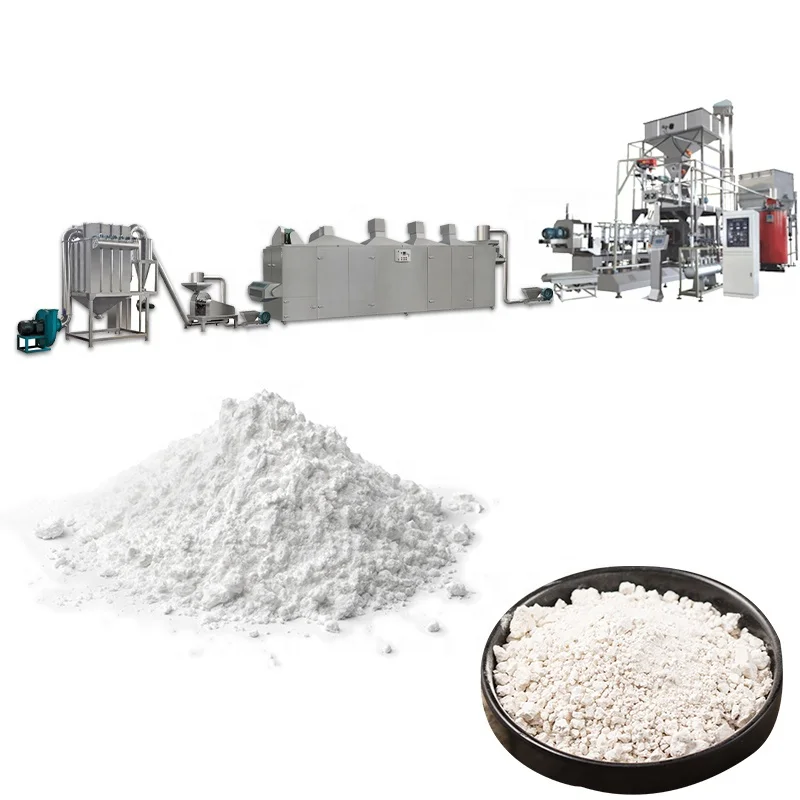
Integrated Throughput Matching — Every station from the 4 kW mixer through the twin-screw extruder to the final grinder is sized to the same basis capacity, so pregelatinized starch output is not bottlenecked by an undersized dryer or air conveyor.
Technical Specifications
| Parameter | Value |
|---|---|
| Product Type | Pregelatinized Modified Starch Extrusion Line |
| Extruder Type | Twin-screw extruder |
| Capacity Range | 80–500 kg/h (basis not stated in source — confirm raw material type, moisture content and target starch modification degree) |
| Raw Materials | Wheat flour, corn starch, potato starch |
| Frame Material | Stainless steel 201 |
| Contact Material | Food grade stainless steel 304 |
| Energy Options | Electricity, gas, diesel, or steam |
| Power Consumption (Electric Heating) | Approx. 100 kW (rated or peak not specified in source) |
| Power Consumption (Gas/Diesel Heating) | Approx. 50–60 kW (rated or peak not specified in source) |
| Voltage & Frequency | Three phase 380V/50Hz; Single phase 220V/50Hz (customizable) |
| Control System | Standard electrical components; Siemens (China-made) or equivalent motors; Delixi or Delta inverter |
| Mixer Motor | 4.0 kW |
| Mixer Output | 3.0–4.0 kg per batch (source value — verify against manufacturer catalog) |
| Mixer Dimensions | 1.2 × 0.9 × 1.4 m |
| Screw Conveyor Motor | 1.1 kW |
| Screw Conveyor Output | 0–150 kg/h (source value — verify against manufacturer catalog) |
| Screw Conveyor Dimensions | 2.5 × 0.6 × 2.3 m |
| Process Flow | Mixer → Screw Conveyor → Twin-screw Extruder → Shifter → Air Conveyor → Dryer → Air Conveyor → Conditioning → Conveyor → Grinder |
| Die Configuration | Interchangeable dies for different product forms |
| Standards | CE |
| Warranty | One year with lifetime technical guidance support |
Application Suitability
| Application | Material or Output |
|---|---|
| Oilfield drilling fluid production | Pregelatinized starch from corn or potato starch meeting API viscosity specifications |
| Food ingredient manufacturing | Modified starch for thickening, stabilising and gelling from wheat flour or corn starch |
| Paper and industrial starch supply | Custom-modified starch with controlled gelatinisation degree from wheat flour or corn starch |
| Nutritional and infant formula blending | Pregelatinized starch base from potato or corn starch for downstream formulation |
What a Nominal Capacity Figure Leaves Out About Your Starch Line
A capacity number means nothing until it is proven on your actual raw material at your target moisture and modification degree.
I remember a project where an oilfield client received a pregelatinized starch line rated at a certain throughput. During the trial, the extruder held output on generic corn starch, but when the client switched to their own blended formulation, viscosity dropped sharply and the batch was unusable. That mismatch was only caught because we ran a mid-scale trial before shipment. Most modified starch processing line manufacturer quotes give you a headline number without stating the raw material basis or the moisture content used. Without that context, the number is a guess. [NEED_CITE: variability of starch gelatinisation behaviour across corn, potato and wheat sources]
Screw Configuration and Gelatinisation Control
The twin-screw extruder at the heart of this line uses interchangeable dies and adjustable screw elements to control shear, residence time and temperature profile inside the barrel. For pregelatinized starch destined for oilfield drilling fluid, the screw arrangement must generate enough mechanical energy to fully disrupt the starch granule structure without degrading the polymer chains that deliver viscosity. The modified starch processing line manufacturer configures the screw profile and die geometry around the specific raw material — corn starch, potato starch, or wheat flour — because each has a different gelatinisation temperature, granule size and amylose-to-amylopectin ratio.
Drying, Conditioning and Grinding as a Single Chain
After extrusion, the wet expanded starch moves through an air conveyor into the dryer, then through conditioning and finally into the grinder. If the dryer is undersized relative to extruder output, moisture remains trapped in the pellet core and the grinder produces uneven particle size. If the grinder is too small, it becomes the bottleneck and the extruder must be throttled back. This line matches throughput across every station so that the capacity you see at the extruder is the capacity you actually get at the packing end. [NEED_CITE: impact of residual moisture on pregelatinized starch particle size distribution after grinding]
How Power Source and Control Choices Shape Daily Operation
The extruder supports electric heating at approximately 100 kW or gas and diesel heating at approximately 50–60 kW, which affects both utility planning and operating cost in different markets. A facility in a region with unstable grid supply may prefer gas or diesel to avoid production stops during voltage dips. The control system uses Delixi or Delta inverters and Siemens (China-made) or equivalent motors, giving operators familiar components that local electricians can service. Voltage and frequency are confirmed before production starts — whether the destination is 380V/50Hz, 440V/60Hz or another local standard — so the line arrives ready to connect without transformer delays.
The Cost of Skipping a Pre-Shipment Trial
When a line ships without a trial run on the buyer’s own raw material, the first real test happens during commissioning on the factory floor. If the starch does not reach the target gelatinisation degree, the screw configuration must be changed, new dies ordered, and weeks of production lost while the correct setup is found. This is not a theoretical risk — different batches of corn starch from different regions can vary in protein content and particle size enough to change extrusion behaviour. Running the buyer’s material through the in-house testing workshop before shipment eliminates that commissioning gamble. [NEED_CITE: influence of raw material batch variation on twin-screw extrusion stability]
Why Buyers Source This Line From One Supplier
The entire process flow — mixer, screw conveyor, twin-screw extruder, shifter, air conveyors, dryer, conditioning unit, conveyor and grinder — comes from a single supplier, which means throughput is calculated across every station rather than assembled from mismatched vendors. Screw configuration and die design are specified to the buyer’s raw material and target starch modification, not copied from a generic build. An in-house testing workshop allows trial runs on the buyer’s actual corn starch, potato starch or wheat flour before the line ships. Pre-sales consultation covers line layout and utility planning, and the same engineering team handles on-site installation, commissioning and operator training. Food grade stainless steel 304 contact materials are used throughout the processing path, meeting hygiene requirements for both food-grade and industrial starch applications.
Documentation & Verification
- Line layout and capacity calculation matched to your raw material type and target modification degree
- Screw and die configuration record specific to your starch formulation
- Trial run report on your actual corn starch, potato starch or wheat flour confirming output and gelatinisation
- Electrical schematic with confirmed voltage, frequency and control language for your facility
- CE declaration of conformity covering the complete extrusion and drying line
- Operation and maintenance manual with wear parts list for screws, dies and conveyor components
Installation, Commissioning & Support
- Foundation and floor space planning based on the full process flow dimensions including the 2.5 m screw conveyor and dryer length
- Dedicated power circuit sizing for the extruder’s 100 kW electric heating load or gas/diesel supply connection
- Assembled line sections shipped with matched air conveyor ductwork for on-site connection
- First-run parameter setting for barrel temperature zones, screw speed and die pressure on your raw material
- Operator training covering screw configuration changes, die swaps and inverter adjustment via Delixi or Delta controls
- Wear parts supply plan for screws, dies and grinder blades with recommended replacement intervals
What to Prepare Before Requesting a Quote
To size the line correctly, share your raw material type and specification sheet, the target pregelatinized starch viscosity or gelatinisation degree, and your daily output requirement. Confirm the local voltage, frequency and preferred energy source — electricity, gas, diesel or steam — so the heating system is built to match. Let us know whether you need a trial run on your material before shipment and what product form the grinder should produce.
Frequently Asked Questions
Q: How is output capacity verified on my specific starch raw material and what is the test basis?
A: Capacity is verified by running your actual corn starch, potato starch or wheat flour through the twin-screw extruder in the testing workshop. The trial records throughput at a defined moisture content, screw speed and barrel temperature profile, and measures the gelatinisation degree of the output. The trial run report is shared before shipment so you can confirm the line meets your specification.
Q: Which screw configuration and die design matches my target pregelatinised starch viscosity?
A: The screw element arrangement and die geometry are selected based on your raw material’s amylose content, granule size and target viscosity. Oilfield drilling fluid starch typically needs higher shear for full granule disruption, while food-grade thickening starch may require gentler treatment. The configuration record is documented and provided with the line.
Q: How are dryer and grinder capacities matched to extruder output to avoid line bottlenecks?
A: Each station is sized during the line layout phase so that the dryer residence time, air conveyor throughput and grinder capacity all align with the extruder’s verified output on your material. This prevents moisture retention in pellets and uneven particle size that occur when downstream equipment is undersized.
Q: Can a trial run be performed on my raw material before shipment and what does the report include?
A: Yes. The in-house testing workshop runs your raw material through the extruder and records throughput, barrel temperature profile, screw speed, die pressure and the gelatinisation degree of the output. The report is reviewed with you before the line is cleared for packing and shipment.