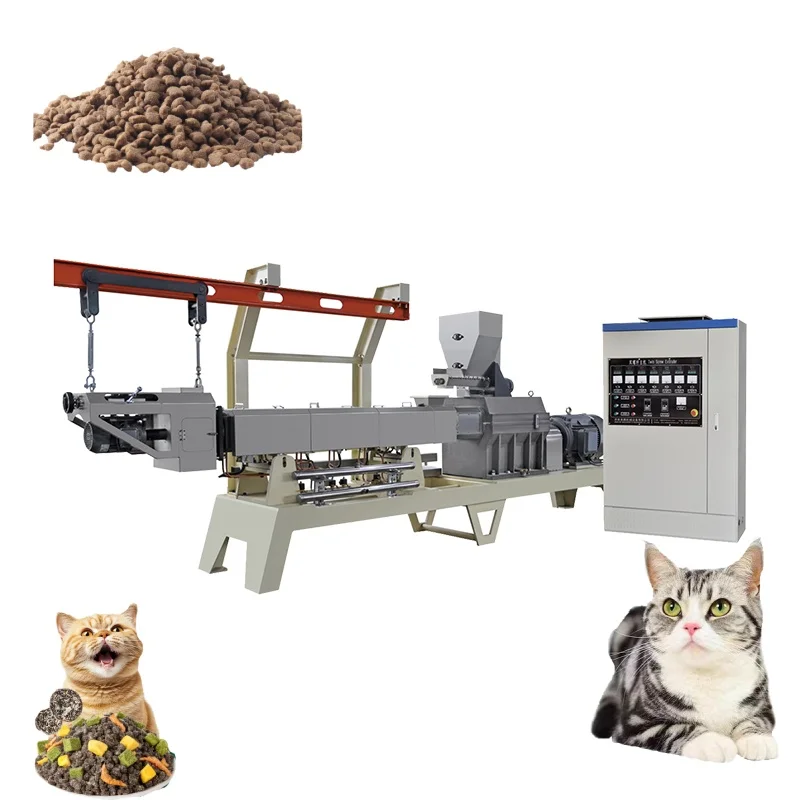
Line-Balanced Throughput — every station from batching to packing is sized against the extruder’s verified output, not a catalogue peak.
Technical Specifications
| Parameter | Value |
|---|---|
| Product Type | Pet Food Extrusion Production Line |
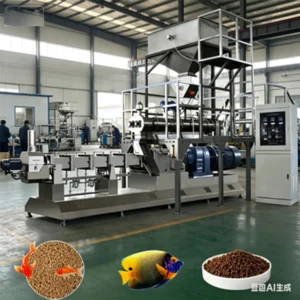
| Application | Dry kibble (dog and cat), aquatic feed (fish) |
| Output Capacity | 3 tons per hour (basis not stated in source — confirm raw material formulation, moisture content, kibble size and density target) |
| Extruder Type | Twin-screw, single-screw options available |
| Control System | PLC and MCC control available |
| Process Documentation | Fish feed process drawing included |
| Warranty | 1-year warranty |
| Contact Materials | Food-grade stainless steel throughout product zones |
Application Suitability
| Application | Material or Output |
|---|---|
| Dry dog kibble production | Corn, poultry meal, meat slurry blends at varying inclusion rates |
| Dry cat food processing | High-protein formulations with fresh meat and fish meal |
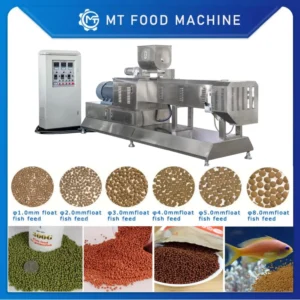
| Floating fish feed pellets | Soybean meal, wheat flour, fish meal with controlled expansion |
| Sinking aquatic feed | Denser formulations for bottom-feeding species |
| Multi-species feed runs | Quick changeover between kibble shapes and die configurations |
Why "3 Tons per Hour" Is the Wrong First Question
Actual throughput depends entirely on what you feed into the barrel.
When buyers compare a pet food making machine manufacturer by nameplate capacity alone, the line often bottlenecks downstream. A dryer rated for nominal output chokes when high-moisture meat slurry enters the extruder, and a flavouring drum cannot keep pace with the real kibble flow. I have watched lines sit idle for weeks because the cooling conveyor was spec’d to a brochure number rather than the actual formulation the customer runs [NEED_CITE: extruder throughput variance with raw material moisture content].
How Each Station Is Sized to Your Formulation
A pet food making machine line only holds its target output when every supporting station matches the extruder’s real throughput on your specific raw material. We calculate dryer belt length, cooler airflow, and drum volume against the confirmed recipe — including moisture entering the barrel and kibble density leaving the die. This keeps the flow continuous without intermediate surge bins that degrade product quality.
From Batching to Packing Without Throughput Gaps
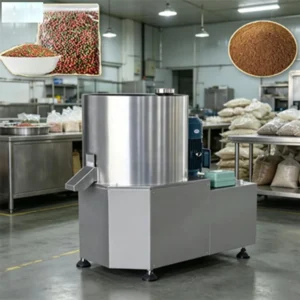
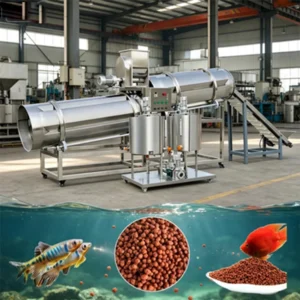
The equipment range covers mixers, screw conveyors, extruders, dryers, flavouring drums, coolers, and packing stations. Each unit is selected so its capacity overlaps the next station’s intake rate. When a line is assembled from separate vendors, these margins disappear and the slowest machine dictates actual output [NEED_CITE: line throughput bottlenecks in multi-vendor food processing installations].
Reading the Specs That Matter
Twin-screw configurations allow higher fresh-meat inclusion and more shear control than single-screw designs, which directly affects kibble texture and expansion. Die geometry determines final shape and density; a round die produces a different bite than a bone-shaped die even at identical moisture levels. PLC control maintains barrel temperature profiles across heating zones, holding batch consistency when ambient workshop conditions shift between seasons.
What Happens When the Dryer Is Undersized
An undersized dryer forces the extruder to slow down, cutting actual output below the rated figure. Kibble leaves the belt with residual moisture above specification, inviting mould during storage and customer rejection at the warehouse. Replacing a dryer later costs more than sizing it correctly before the line ships [NEED_CITE: moisture-related spoilage in dry pet food storage].
Why Buyers Source the Full Range Here
One supplier covers every station from batching through packing, so throughput calculations remain internally consistent. Screw and die configurations are specified to your raw material rather than copied from a generic build. An in-house testing workshop runs trial batches on your actual formulation before the equipment leaves the factory. Electrical schematics confirm voltage, frequency, and control language for your destination market before production begins.
Documentation & Verification
- Line layout drawing with per-station capacity calculation based on your confirmed formulation
- Screw and die configuration record matched to your target kibble shape and density
- Electrical schematic with voltage and frequency locked to your facility supply
- Trial run report generated on your raw material in the testing workshop
- Factory test record capturing actual output before dispatch
Installation, Commissioning & Support
- Foundation load drawings account for extruder weight and vibration isolation pads
- Dedicated electrical circuit sized to total connected load of extruder, dryer, and motors
- Assembled and tested as a complete line, then modularized for container loading
- On-site parameter tuning against local ambient temperature and humidity conditions
- Operator training covers PLC setpoints, screw wear inspection, and die changeover procedures
- Wear parts list with screw element and die specifications for reorder accuracy
What We Need Before Quoting Your Line
Share your raw material formulation, target kibble shape, and desired daily output so we can calculate station capacities. Confirm the voltage and frequency at your facility and the control language your operators need. If you are replacing a single station in an existing line, tell us the upstream and downstream equipment so the new unit integrates without throughput mismatch.
Frequently Asked Questions
Q: How is the output capacity of each station verified against the extruder’s actual throughput on my raw material?
A: We calculate every station’s capacity against the extruder’s confirmed output on your specific formulation, not a catalogue peak. A trial run in our testing workshop measures real throughput, and the dryer, cooler, and packing station are then sized to match that verified flow.
Q: Which supporting equipment matches a given extruder model?
A: Dryer belt length, cooler volume, and flavouring drum diameter are selected based on the extruder’s actual output and your product’s moisture profile. We provide a line layout showing each station’s capacity calculation before production starts.
Q: What screw and die configurations are available for different kibble densities and shapes?
A: Screw element arrangement and die geometry are specified to your target kibble shape, density, and raw material. We record the exact configuration for your line so reorder parts and future product changeovers remain consistent.
Q: Can a trial run be done on my raw material before the line ships?
A: Yes. We run your formulation in our in-house testing workshop before dispatch. The trial report documents actual throughput, kibble density, and expansion so you can verify product quality before the equipment arrives at your factory.