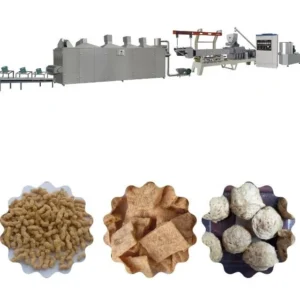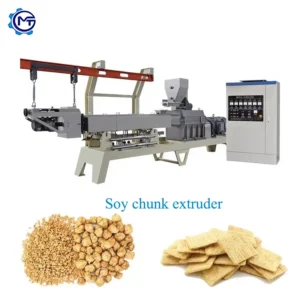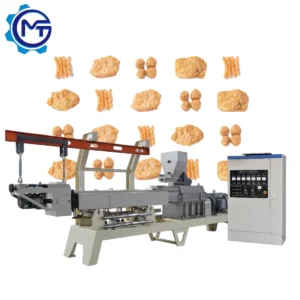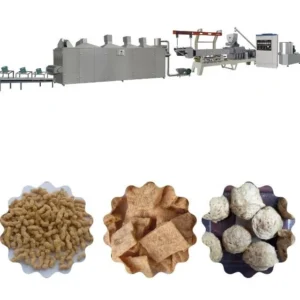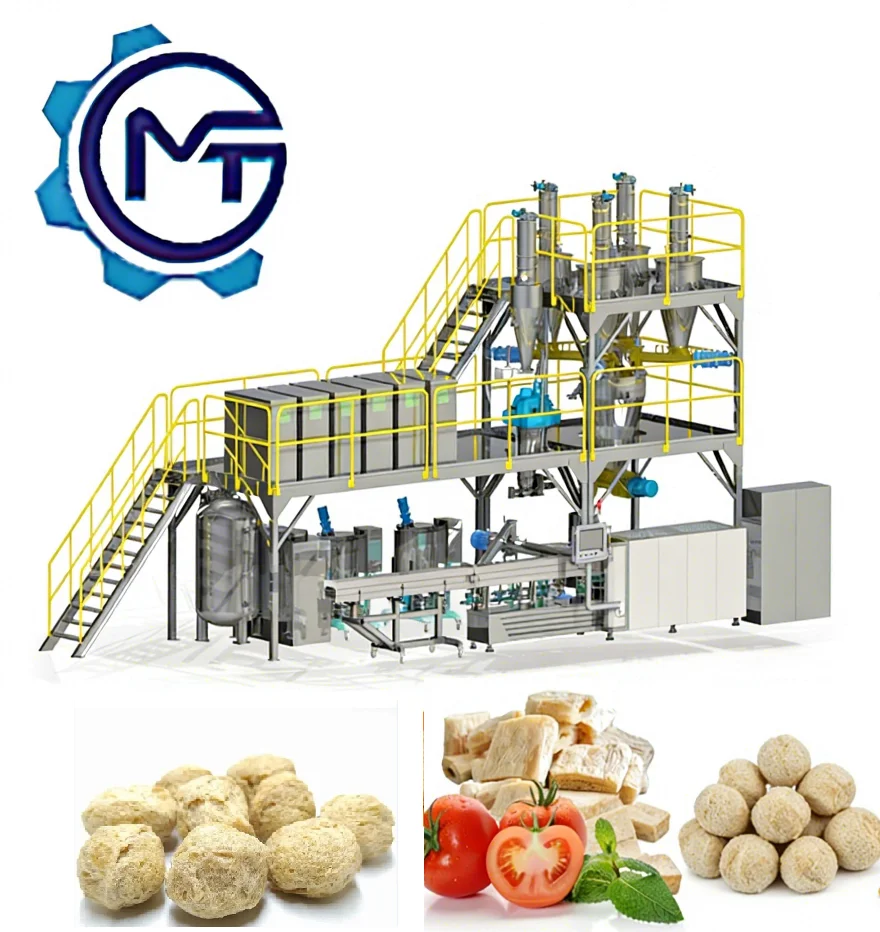
Complete Line Throughput Matching — Every station from the vertical mixer through the multi-layer dryer is sized so the twin screw extruder never starves or floods downstream equipment on your actual defatted soya flour.
Technical Specifications
| Parameter | Value |
|---|---|
| Product Type | Twin Screw Extruder Production Line for Texturized Vegetable Protein (Plant-Based Meat) |
| Model Options | MT65, MT70, MT75, MT85 |
| Screw Type | Twin Screw |
| Screw Length Options | 1050 mm, 1520 mm |
| Main Motor Power Options | 22 kW, 30 kW, 45 kW |
| Installed Power (MT65) | 84 kW |
| Installed Power (MT70) | 160 kW |
| Installed Power (MT75) | 190 kW |
| Installed Power (MT85) | 210 kW |
| Power Consumption (MT65) | 59 kW |
| Power Consumption (MT70) | 120 kW |
| Power Consumption (MT75) | 140 kW |
| Power Consumption (MT85) | 140 kW |
| Output Capacity (MT65) | 100–150 kg/h (basis not stated in source — confirm raw material and moisture content) |
| Output Capacity (MT70) | 150–200 kg/h (basis not stated in source — confirm raw material and moisture content) |
| Output Capacity (MT75) | 150–200 kg/h (basis not stated in source — confirm raw material and moisture content) |
| Output Capacity (MT85) | 250–300 kg/h (basis not stated in source — confirm raw material and moisture content) |
| Overall Dimensions (MT65) | 40000 × 1200 × 2200 mm |
| Overall Dimensions (MT70) | 41000 × 1500 × 2200 mm |
| Overall Dimensions (MT75) | 43000 × 1500 × 3200 mm |
| Overall Dimensions (MT85) | 45000 × 1500 × 3500 mm |
| Rotary Cutting Motor | 0.75 kW |
| Feeding Motor | 0.75 kW |
| Pump Motor | 0.37 kW |
| Heating Power Options | 10 kW, 14 kW |
| Mixer Type | Vertical mixing machine, stainless steel 304 mixing ruler |
| Mixer Power Options | 4 kW, 7.5 kW, 15 kW |
| Mixer Capacity Options | 20–30 kg, 70–80 kg, 170–180 kg (batch cycle time to be confirmed) |
| Mixer Shelf Material | Carbon steel |
| Dryer Type | Multi-layer dryer, double pitch roller chain drive, round-trip drying |
| Dryer Heating Options | Fuel, gas, electricity (customer selectable) |
| Line Stations | Mixer → Screw Conveyor → Twin Screw Extruder → Air Conveyor → Multi-layer Dryer → Cooling Machine |
| Certification | CE (extrusion machinery, since 2014) |
Application Suitability
| Application | Material or Output |
|---|---|
| Texturized vegetable protein (TVP/TSP) production | Defatted soya flour, low-temperature soya flakes |
| Soya nuggets and soya chunks for meat analogues | Defatted soya flour with layer fiber structure |
| Vegetarian fast-food and deep-freeze product inputs | Soybean dregs, peanut dregs blended with soya base |
| Maigre snack and vegetarian food manufacturing | Adjusted screw configuration for cereal and snack formats |
| Plant-based meat ingredient supply for food factories | High-protein soya-based raw materials at varying moisture levels |
Why Nominal Capacity Figures Mislead Buyers on a Plant Based Meat Processing Line Equipment Purchase
The number on the quote sheet only matters if it was measured on your exact raw material at your target moisture.
I spent years replacing worn screws and dies on extrusion lines around the Yangtze Delta manufacturing belt before moving into equipment sales. The most common call I got was from buyers whose plant based meat processing line equipment could not hold the quoted output on their specific defatted soya flour. The extruder was rated for a certain throughput, but the actual protein content, particle size, and moisture of their raw material changed the residence time and shear profile inside the barrel. The result was either under-capacity or product that did not meet the fiber structure specification their market required [NEED_CITE: raw material variability effects on twin screw extrusion throughput]. The lesson was always the same: capacity is not a single number until you run the actual material through the actual screw configuration.
How the Full Equipment Range Connects from Mixer to Cooling Machine
A plant based meat processing line equipment setup only performs as well as its weakest station. The vertical mixer with its stainless steel 304 mixing ruler prepares the defatted soya flour blend, then the screw conveyor meters it into the twin screw extruder at a controlled feed rate. After extrusion, the air conveyor moves the product into the multi-layer dryer, where the double pitch roller chain drive ensures even residence time across the drying bed. Each station is specified so its throughput envelope overlaps with the extruder output range, avoiding the bottleneck that occurs when a dryer is undersized or a conveyor cannot keep pace with the cutting head.
Matching Dryer Heating Source to Your Facility Infrastructure
The multi-layer dryer on this line supports fuel, gas, or electric heating, and the choice affects both operating cost and temperature control precision. Gas heating typically offers rapid ramp-up and is common in facilities that already have a gas main running to other thermal processes. Electric heating provides tighter temperature band control, which matters when you are drying soya chunks to a precise final moisture for shelf stability. Fuel-based systems suit locations where other options are unavailable or cost-prohibitive. The round-trip drying path with adjustable temperature and drying time lets operators fine-tune the profile for different product densities [NEED_CITE: industrial dryer heat source selection criteria for food processing].
Reading the Screw, Motor, and Die Specifications for Actual Production Impact
The twin screw design is central to texturized vegetable protein production because the intermeshing screw elements generate the shear and pressure needed to align protein molecules into a layer fiber structure. The available screw lengths of 1050 mm and 1520 mm determine the residence time inside the barrel; longer screws give the material more time under heat and shear, which influences the degree of protein texturization. Main motor power options of 22 kW, 30 kW, and 45 kW map to different torque requirements — higher-protein raw materials or denser soya chunks generally demand more torque to push through the die. The die configuration is adjustable, meaning you can switch between soya nugget shapes, chunk sizes, and even cereal formats by changing the die plate and screw arrangement. Heating power options of 10 kW and 14 kW across the barrel zones control the temperature profile that drives starch gelatinisation and protein denaturation, both of which directly affect product texture and water absorption capacity in the final application.
What Happens When Extruder and Downstream Equipment Are Mismatched
I once visited a plant in the Yangtze Delta region where the extruder was pushing product faster than the downstream dryer could handle. Wet soya chunks piled up on the air conveyor, blocking the path and forcing the operator to shut the entire line down twice per shift. The buyer had sourced the extruder from one vendor and the dryer from another, and nobody had calculated the moisture removal rate against the extruder output. That plant based meat processing line equipment setup sat idle for days while they scrambled to add drying capacity [NEED_CITE: throughput mismatch consequences in food extrusion line integration]. The hidden cost was not just lost production time but the degraded product that had been partially dried and could not be sold.
Why Buyers Source This Complete Line from a Single Supplier
Every station on this line — mixer, screw conveyor, twin screw extruder, air conveyor, multi-layer dryer, cooling machine — is specified under one roof so throughput is matched across the entire chain rather than assembled from separate vendors. Screw configuration and die design are set to your raw material and target product, not copied from a generic build. The in-house testing workshop runs your defatted soya flour or low-temperature soya flakes through the actual machine before shipment, so product development starts in the factory rather than on your floor after installation. Twin screw expertise covers plant-based meat, pet food, aquatic feed, snacks, cereals, starch, and protein applications, meaning the engineering team has seen how different raw materials behave under extrusion. Pre-sales consultation through engineer design, on-site installation, commissioning, and ongoing maintenance keeps one team accountable from first inquiry through long-term production.
Documentation & Verification
- Line layout and capacity calculation matched to your target soya chunk or nugget output
- Screw and die configuration record specific to your defatted soya flour batch
- Electrical schematic and voltage confirmation for your local power grid standard
- Trial run report on your raw material before the machine leaves the factory
- Operation and maintenance manual covering every station from mixer to cooling machine
- Wear parts list identifying screws, dies, and dryer chain components with replacement intervals
Installation, Commissioning & Support
- Overall line dimensions up to 45000 × 1500 × 3500 mm require confirmed floor space and ceiling height before foundation work
- Installed power up to 210 kW demands dedicated circuit sizing and voltage verification at the facility panel
- Multi-layer dryer with selectable fuel, gas, or electric heating needs utility connections routed before equipment arrival
- Screw configuration and die setup are finalized during on-site commissioning using your production raw material
- Operator training covers barrel temperature profiling, feed rate adjustment, and dryer time-temperature settings
- Wear parts inventory includes replacement screws, die plates, and dryer chain links for first-cycle maintenance
What to Include in Your Inquiry
Tell us which raw material you plan to run — defatted soya flour, low-temperature soya flakes, soybean dregs, or a blend — along with the target product format such as soya nuggets, chunks, or layer fiber sheets. Share your local voltage and frequency so the electrical schematic and control language are confirmed before production begins. If you have existing upstream batching or downstream packing equipment, provide the interface dimensions so the line layout accounts for the connection points.
Frequently Asked Questions
Q: How do I select the right extruder model based on my production target?
A: The MT65, MT70, MT75, and MT85 cover different output ranges, but the actual throughput depends on your raw material and moisture content. We confirm the capacity by running a trial on your specific defatted soya flour or soya flakes in our testing workshop before finalizing the model recommendation and quotation.
Q: What supporting equipment is included and how is throughput matched?
A: The line includes a vertical mixer, screw conveyor, twin screw extruder, air conveyor, multi-layer dryer, and cooling machine. Each station is sized so its throughput envelope overlaps with the extruder output, preventing bottlenecks that occur when equipment is sourced from separate vendors without capacity coordination.
Q: Can the screw and die configuration be customized for my raw material?
A: Yes. Screw elements and die plates are configured to your specific raw material and target product shape. The adjustment covers soya nuggets, chunks, and layer fiber structures. The configuration is documented and tested on your material in the workshop before shipment.
Q: What voltage and control system options are available?
A: Voltage and frequency are confirmed to match your local grid before production. The electrical schematic and control language are verified during the specification stage so there are no delays during on-site commissioning.
Q: What affects the delivery timeline from deposit to shipment?
A: Typical lead times span several working weeks after deposit receipt. The timeline depends on model selection, customization of screw and die configuration, and whether a trial run on your raw material is scheduled before dispatch.