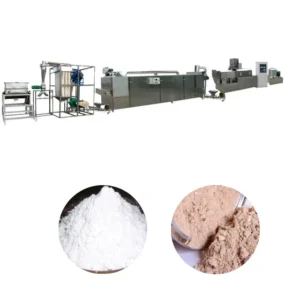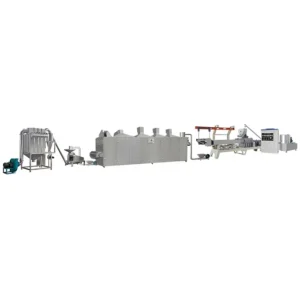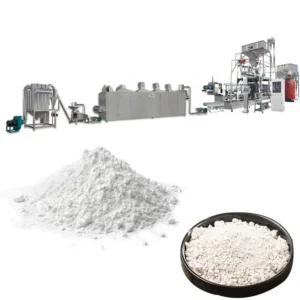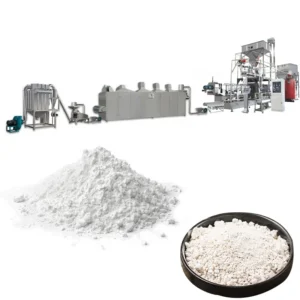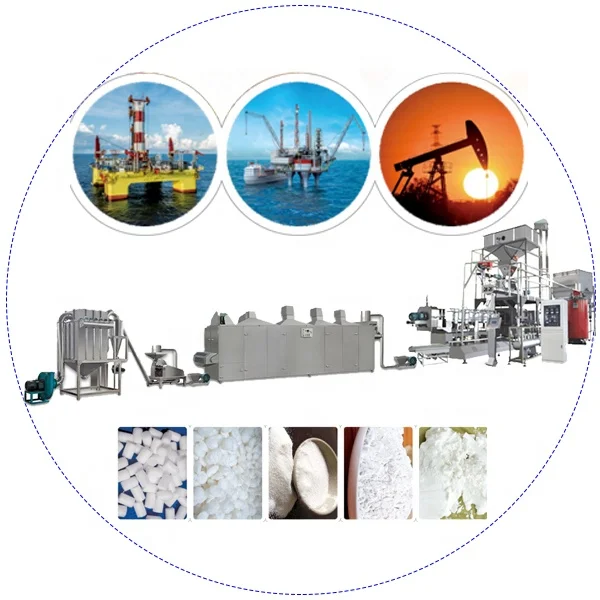
Matched Throughput — every station from the 4.0 kW mixer to the grinder is specified as one integrated line, so the extruder output never waits on an undersized dryer or conveyor.
Technical Specifications
| Parameter | Value |
|---|---|
| Product Type | Automatic Industrial Adhesive Starch Modification Production Line |
| Capacity Range | 80–500 kg/h (basis not stated in source — confirm raw material type, moisture content, and target modification degree) |
| Extruder Type | Twin-screw extruder |
| Frame Material | Stainless steel 201 |
| Contact Material | Food-grade stainless steel 304 |
| Mixer Motor | 4.0 kW |
| Mixer Dimensions | 1.2 × 0.9 × 1.4 m |
| Mixer Batch Output | 3.0–4.0 kg/time (basis not stated in source — confirm raw material density and moisture addition) |
| Screw Conveyor Motor | 1.1 kW |
| Screw Conveyor Dimensions | 2.5 × 0.6 × 2.3 m |
| Screw Conveyor Output | 0–150 kg/h (basis not stated in source — confirm material and inclination angle) |
| Energy Options | Electricity / Gas / Diesel / Steam |
| Power Consumption | approx. 100 kW (electricity heating); approx. 50–60 kW (gas or diesel heating) (rated or peak not specified) |
| Voltage & Frequency | Three-phase 380V/50Hz; Single-phase 220V/50Hz (customizable to local supply) |
| Control System | PLC and MCC (specific configuration per line to be confirmed) |
| Assembly State | Complete production line |
| Standards | CE |
Application Suitability
| Application | Material or Output |
|---|---|
| Pre-gelatinized starch for instant food and nutritional formula | Corn starch, wheat flour, potato starch |
| Industrial adhesive starch modification | Native starch requiring controlled viscosity and gelling properties |
| Food-grade modified starch for processing and paper industry | Starch paste requiring expansion and gelatinization treatment |
| Starch molecular weight and viscosity adjustment | Various starch sources processed through thermal and shear modification |
What "80–500 kg/h" Leaves Out About Modified Starch Processing Line Equipment
Capacity figures mean nothing until they are tied to a specific starch source, moisture addition rate, and target modification degree.
I have watched buyers sign contracts based on a nameplate number that was established on corn starch, only to discover during commissioning that their actual material — perhaps cassava or potato starch — behaves entirely differently under shear and heat. The gelatinization temperature shifts, the expansion ratio drops, and the real throughput falls well below the contracted figure [NEED_CITE: raw material variability in starch extrusion processes]. A modified starch processing line equipment rated at one output on paper can deliver considerably less when the raw material profile changes, which is why the conversation must start with the buyer’s actual flour or starch sample, not a generic catalogue number.
How Each Station Fits the Modified Starch Workflow
The mixing station blends raw starch with water and additives before the screw conveyor feeds a consistent mass into the twin-screw extruder. Inside the extruder, controlled shear and barrel temperature gelatinize and expand the starch paste, which then travels through an air conveyor into the dryer. From drying through conditioning and finally grinding, each piece of modified starch processing line equipment is sized so that moisture load, residence time, and particle reduction do not create a hidden choke point downstream.
Sizing the Dryer and Grinder to the Extruder Output
The twin-screw extruder discharges material at a moisture level that the dryer must remove within a defined residence window. If the dryer is undersized, the modified starch enters the grinder with residual moisture that causes screen blinding and inconsistent particle size. Sizing the dryer belt length and airflow to the extruder’s moisture output, and matching the grinder capacity to the dried throughput, ensures the final powder meets the target mesh specification [NEED_CITE: moisture-content and particle-size relationship in starch grinding].
Reading the Specifications That Matter for Starch Modification
The twin-screw configuration is central because starch modification requires both thermal input and mechanical shear across multiple barrel zones. The 4.0 kW mixer motor and 3.0–4.0 kg batch output define how frequently batches must be prepared to sustain continuous extruder feeding — an undersized mixer forces the extruder to idle between cycles. The screw conveyor’s 0–150 kg/h output range must align with the extruder intake rate; if the conveyor delivers faster than the extruder can process, material backs up in the feed hopper. Energy source selection — electricity at approximately 100 kW or gas/diesel at roughly 50–60 kW — directly shapes the installed utility infrastructure and the ongoing thermal cost per kilogram of modified starch. The food-grade stainless steel 304 contact surfaces are mandatory for any line producing starch destined for food or nutritional applications, where contamination from non-food-grade metals would fail downstream audit requirements.
The Hidden Cost of Unmatched Stations
When the dryer cannot keep pace with the extruder, partially dried starch accumulates in the conditioning stage and the grinder chokes on material that is still too tacky to mill cleanly. Operators respond by slowing the extruder, which means the line runs below its nameplate output every shift [NEED_CITE: throughput bottlenecks in continuous starch processing]. Over weeks, the cumulative lost output far exceeds the savings from choosing a smaller dryer, and the grinder screens wear prematurely from processing semi-wet material.
Why Procurement Through a Single Equipment Range Matters
Sourcing the mixer, extruder, dryer, and grinder from one equipment range means throughput matching is calculated before the line ships, not discovered during commissioning. Screw configuration and die design are specified against the buyer’s starch source rather than copied from a generic build. The in-house testing workshop runs the buyer’s actual raw material before dispatch, producing a trial report that becomes the baseline for on-site startup. Electrical schematics and voltage confirmation are locked in during the specification phase, so the MCC and PLC arrive configured for the local power grid. Food-grade contact materials are documented across every station, supporting audit trails for food and pharmaceutical starch applications.
Documentation & Verification
- Line layout showing throughput calculation between mixer batch cycle, extruder output, dryer residence time, and grinder capacity
- Screw and die configuration record matched to buyer’s starch source and target modification degree
- Electrical schematic with voltage and frequency confirmation for the installation site
- Trial run report on buyer-supplied raw material from the in-house testing workshop
- Factory test record covering each station’s operating parameters before shipment
- CE declaration of conformity for the complete modified starch line
Installation, Commissioning & Support
- Foundation and floor space planning based on the full line footprint from mixer through grinder
- Power supply verification for the 380V three-phase or 220V single-phase requirement and dedicated circuit sizing
- Pre-wired MCC and PLC cabinets configured to the site voltage before dispatch
- First-run parameter setting using the trial report as the baseline for barrel temperatures and screw speed
- Operator training on mixer batching intervals, extruder feed rate, and dryer temperature adjustment
- Wear parts list covering screws, dies, and grinder screens with recommended replacement intervals
Preparing Your Inquiry
Share the specific starch source you intend to process, the target modification degree or viscosity range, and the daily output you need to sustain. Include your local voltage, frequency, and preferred energy source so the electrical and thermal design can be confirmed early. If you have existing upstream or downstream equipment, describe the interface points so the line layout accounts for material handoff.
Frequently Asked Questions
Q: How is throughput verified across each station of the line?
A: Every station — mixer, extruder, dryer, grinder — is calculated against the same target output during the layout phase. The mixer batch cycle must feed the extruder without idle gaps, the dryer must handle the extruder’s moisture discharge, and the grinder must process the dried output at full rate. This matching is documented in the line layout before the quotation stage.
Q: What voltage and control options are available for different markets?
A: The line supports three-phase 380V/50Hz and single-phase 220V/50Hz as standard, with customization available for other local supplies. The PLC and MCC can be configured with the control language required at the installation site, and the electrical schematic is confirmed with the buyer before production begins.
Q: Can screw configuration adapt to different starch sources?
A: Yes. Screw element arrangement and barrel temperature zones are specified based on the buyer’s starch type — corn, wheat, potato, or cassava — and the target gelatinization and expansion profile. A trial run on the buyer’s raw material in the testing workshop confirms the configuration before the extruder ships.
Q: How does energy source selection affect installed power?
A: Electric heating draws approximately 100 kW, while gas or diesel heating reduces electrical demand to roughly 50–60 kW. The choice depends on local utility availability and relative fuel cost. This decision is confirmed during specification so that the correct heaters and control circuits are built into the line.
Q: Is a trial run on our raw material possible before shipment?
A: The in-house testing workshop conducts trial runs using the buyer’s supplied starch sample. The resulting report documents barrel temperatures, screw speed, moisture addition, expansion ratio, and product characteristics, providing a verified baseline that the commissioning team uses during on-site startup.