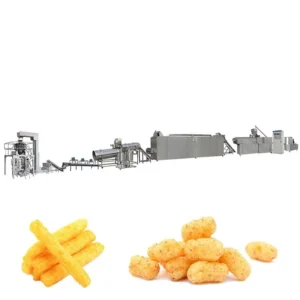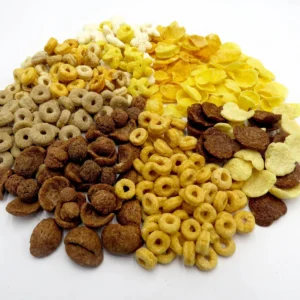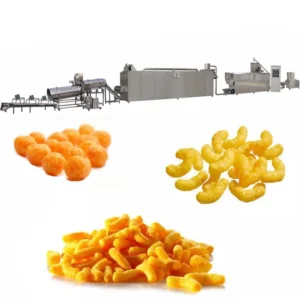
Screw Configuration Matched to Your Recipe — we run your actual corn or rice blend in our testing workshop to lock in the die geometry and barrel profile before building the full line.
Technical Specifications
| Parameter | Value |
|---|---|
| Model | MT65 / MT70 / MT85 |
| Product Type | Corn Flakes and Puffed Snack Extrusion Line |
| Screw Type | Twin-screw |
| Output Capacity (MT65) | 100–150 kg/h (basis not stated in source — confirm raw material / moisture / product format) |
| Output Capacity (MT70) | 150–200 kg/h (basis not stated in source — confirm raw material / moisture / product format) |
| Output Capacity (MT85) | 200–350 kg/h (basis not stated in source — confirm raw material / moisture / product format) |
| Installed Power (MT65) | 86.35 kW |
| Installed Power (MT70) | 90.75 kW |
| Installed Power (MT85) | 121.06 kW |
| Power Consumption (MT65) | 55 kW |
| Power Consumption (MT70) | 57 kW |
| Power Consumption (MT85) | 85 kW |
| Overall Dimensions (MT65) | 21,000 × 1,200 × 2,200 mm |
| Overall Dimensions (MT70) | 23,000 × 1,500 × 2,200 mm |
| Overall Dimensions (MT85) | 28,000 × 3,500 × 4,300 mm |
| Extruder Raw Material Compatibility | Corn flour, rice flour, wheat flour, grain flour |
| Core Injection Capability | Peanut butter, chocolate sauce |
| Cutting Size Range | 2 cm – 20 cm (adjustable) |
| Oven Type | Electric, stainless steel double-layer mesh belt |
| Oven Temperature Range | 0–200 °C |
| Oven Layers Available | 3-layer, 5-layer, 7-layer |
| Seasoning Line Options | Octagonal drum, cylinder drum, single-roller, double-roller; oil spraying, sugar spraying, coating |
| Line Stations | Mixer → Screw Feeder → Twin-screw Extruder → Core Injection Machine → Cutting Machine → Elevator → Multilayer Oven → Elevator → Oil/Spray Seasoning Machine → Coating Roller → Packaging Machine |
| Control System | Configurable to buyer’s voltage and control language requirements |
| Assembly State | Complete continuous line, fully automated |
| Certification | CE |
Application Suitability
| Application | Material or Output |
|---|---|
| Corn flakes production | Corn flour, corn grits, maize blends |
| Chocolate-coated corn flakes | Corn base with sugar or chocolate spray coating |
| Rice crispies and puffed rice crackers | Rice flour, rice grits, rice-based blends |
| Core-filled sandwiched puffed snacks | Grain flour shell with peanut butter or chocolate filling |
| Wheat flaking and bran snacks | Wheat flour, whole wheat, bran mixtures |
| Nutritious breakfast cereals | Multi-grain flour blends with vitamin fortification |
Why "Rated Capacity" Means Nothing Without the Raw Material in Hand
A 200 kg/h nameplate tells you what the motor can spin, not what your flour blend will actually produce.
I started on the workshop floor here in Jinan and learned the hard way that corn flour at 14% moisture behaves completely differently from the same flour at 18%. Buyers who skip the trial run often find their food extrusion processing line full equipment range delivers half the expected tonnage on the first production day. The extruder barrel fills unevenly, the die pressure drops, and the flakes come out dense instead of crisp [NEED_CITE: moisture content effect on twin-screw extrusion throughput].
The same applies to rice-based recipes. Rice flour gelatinises at a different temperature window than corn, so the barrel heating zones and screw pitch that work perfectly for corn flakes will stall a rice crispies run. Without testing your specific blend beforehand, the line configuration is a guess — and guesses cost you commissioning weeks.
Every Station Has a Job — and a Matching Requirement
A food extrusion processing line full equipment range is only as balanced as its weakest station. If the extruder pushes product faster than the multilayer oven can dry it, moisture stays trapped inside the flakes and they go stale on the shelf. The MT65, MT70, and MT85 each pair with a specific oven layer count — 3, 5, or 7 layers — so the residence time inside the drying chamber matches the extruder throughput at the belt speed you need.
The seasoning section works the same way. An octagonal drum suits sugar-coated corn flakes because the tumbling action distributes a thin glaze evenly. A cylinder drum with oil spray fits savoury puffed snacks where fat-based flavouring must adhere to a porous surface. Choosing the wrong drum geometry means uneven coating and rejected batches.
Core Injection Expands the Line Without a Second Extruder
The core injection station sits directly after the extruder die and before the cutter. It injects peanut butter or chocolate sauce into the centre of the extruded rope, which the cutter then seals as it slices. This means one twin-screw base produces both plain corn flakes and filled snack formats on the same shift [NEED_CITE: core-filled extrusion process parameters for peanut butter and chocolate fillings].
Switching between formats takes a die change and a filling pump adjustment rather than a full line reconfiguration. For buyers entering multiple market segments — breakfast cereal shelves and snack aisles — this flexibility matters when planning the product roadmap against a single capital investment.
Reading the Specs Beyond the Nameplate
The installed power figures — 86.35 kW for the MT65, 90.75 kW for the MT70, 121.06 kW for the MT85 — represent the total connected load across the extruder motor, barrel heaters, and feeder. Actual power consumption is lower: 55 kW, 57 kW, and 85 kW respectively. The gap between installed and consumed power reflects the thermal efficiency of the barrel heating zones and the mechanical efficiency of the gearbox under load.
The twin-screw design handles a wider moisture range and more varied particle sizes than a single-screw equivalent. Corn flour, rice flour, wheat flour, and grain blends each have different starch gelatinisation temperatures, and the intermeshing screw flights provide the shear mixing needed to homogenise these blends inside the barrel. The adjustable cutting range from 2 cm to 20 cm lets you dial in flake size for retail packaging or bulk food service formats without changing the die plate.
What Happens When Stations Are Mismatched
I have seen lines where the extruder was right-sized but the oven was one layer too short. The result was a bottleneck that forced the extruder to idle for minutes between batches, dropping overall throughput and burning more energy per kilogram of finished product. Seasoning drums that spin too fast for the product weight cause flake breakage; drums that spin too slow leave uncoated patches [NEED_CITE: coating drum speed and product breakage correlation].
These problems do not show up in a brochure. They surface on the first full production run, when the buyer discovers the line cannot hold the output they planned their business case around. The fix usually means adding or replacing a station after the fact, which costs more than specifying correctly from the start.
Why Sourcing the Full Range Here Makes the Line Work
Every station in this food extrusion processing line full equipment range comes from one configuration responsibility, so throughput is matched across mixing, extruding, drying, seasoning, and packing rather than assembled from separate vendors who each guarantee only their own machine.
Screw configuration and die design are specified to your raw material and target product format, not copied from a generic build. The in-house testing workshop runs your actual flour blend before shipment, producing a trial run report that locks in the parameters. CE certification covers the complete line assembly. Pre-sales consultation continues through installation, commissioning, operator training, and ongoing wear parts supply.
Documentation & Verification
- Line layout and capacity calculation matched to your extruder model and oven layer count
- Machine specification sheet for every station from mixer through packaging unit
- Screw and die configuration record based on your corn, rice, or grain flour sample
- Electrical schematic with voltage and frequency confirmed before production starts
- Trial run report on your raw material conducted in the testing workshop
- Packing photographs and customs documentation support for export shipment
Installation, Commissioning & Support
- Floor space planning based on the MT85 footprint of 28,000 × 3,500 × 4,300 mm or smaller model dimensions
- Dedicated power circuit sized to the MT65 55 kW or MT85 85 kW running consumption
- Multilayer oven belt tensioning and temperature calibration during on-site commissioning
- Screw and die configuration verified against your raw material during first production run
- Operator training covering barrel temperature profiles, cutter adjustment, and drum speed settings
- Wear parts list with replacement screw elements and die plates for your first reorder cycle
What We Need to Configure Your Line
Send your target product format — plain flakes, coated flakes, or core-filled snacks — along with the raw material specification and moisture content of the flour you plan to use. Let us know your local voltage and frequency, the control language your operators need, and whether an existing packing machine must integrate with the line end. If you can ship a sample of your raw material to our Jinan workshop, we will run a trial before finalising the screw and die configuration.
Frequently Asked Questions
Q: How do I choose between the MT65, MT70, and MT85 extruder models?
A: The choice depends on your target throughput and the raw material you will run. Each model has a different installed power, physical footprint, and output range. We confirm the right model by running your flour sample in the testing workshop and matching the screw configuration and die geometry to the result, rather than selecting on nameplate capacity alone.
Q: Which supporting stations come with the extrusion line and where does each fit?
A: The full range includes a mixer, screw feeder, twin-screw extruder, core injection unit, cutting machine, elevators, multilayer oven, seasoning and coating stations, and a packaging machine. Each station is sized so its throughput matches the extruder output, preventing bottlenecks at the oven or coating stage.
Q: How is the oven layer count matched to extruder throughput?
A: The multilayer oven is available in 3, 5, or 7 layers with a stainless steel mesh belt and 0–200 °C temperature control. More layers increase the drying residence time, which is necessary when a higher-capacity extruder pushes more product per hour. We specify the layer count during the line layout phase based on your product moisture target.
Q: What seasoning and coating options are available for different snack formats?
A: Options include octagonal and cylinder drums, single-roller and double-roller configurations, plus oil spraying, sugar spraying, and dry coating systems. The choice depends on whether you are producing sugar-glazed corn flakes, oil-based savoury puffed snacks, or chocolate-coated breakfast cereals.
Q: Which utility requirements must be confirmed before placing the order?
A: You need to confirm local voltage and frequency, available floor space against the line dimensions, power supply capacity for the running consumption of your chosen model, and the control language for the operator interface. These details are locked in during the specification confirmation step before production begins.